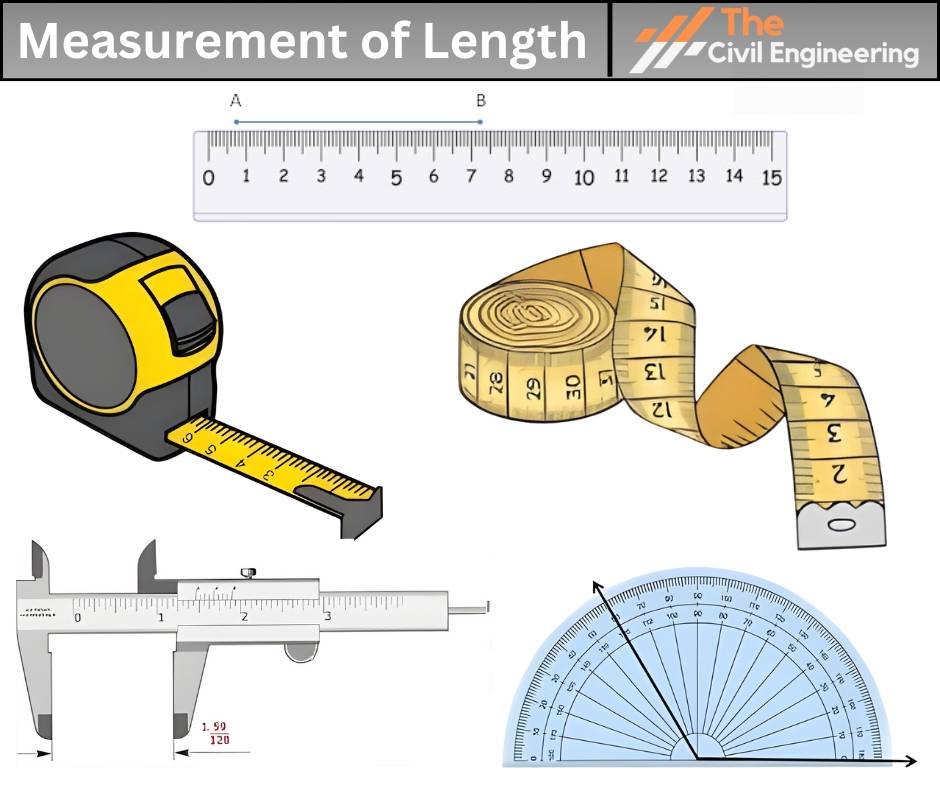
Engineering Measurement Isn't as Precise as You Think
I spent seven years on a bridge inspection project where our laser distance meters kept drifting by four millimeters over a hundred meter span. Turns out thermal expansion of the housing material was the culprit, not calibration drift. The manufacturer's spec sheet said ±1mm. That wasn't lying, exactly, but it was written under laboratory conditions at twenty degrees Celsius. Out on the site in July, the steel casing heated to nearly fifty degrees and the internal optics stretched just enough to throw off every reading. We ended up using a baseline steel tape for the long runs and only the lasers for spot checks, which cut our survey time in half while actually improving accuracy. That kind of thing happens constantly when you work with measurement terminology. People memorize definitions from a textbook and then walk into a shop floor or field environment where none of those clean definitions hold up anymore. Here's what I've learned about the terms that show up most often, and more importantly, what they actually mean when the rubber hits the road.
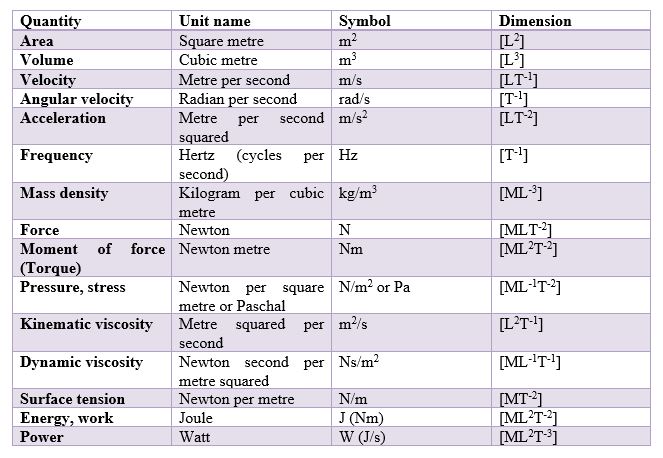
10 Common Terms Used In Engineering Measurement
Resolution vs Accuracy — They're Not the Same Thing
This is the term pair that causes the most problems I see in practice. Resolution is the smallest increment your instrument can display. If a caliper reads to 0.01mm, that's its resolution. Accuracy is how close that reading is to the true value. You can have a device with spectacular resolution that's wildly inaccurate. I've seen technicians get fooled by a digital micrometer reading 0.001mm increments when the actual error budget was ±0.02mm because of zero drift and thermal effects. The extra digits are essentially theater at that point. The practical workaround is straightforward. Before you buy anything, define what accuracy you actually need for your application, then look at the manufacturer's error curve across the full measurement range, not just the best-case specification at a single point. A gauge that's accurate within ±0.005mm at the center of its range but drifts to ±0.015mm at the extremes is useless if you're measuring near those limits. I always ask for the full uncertainty table before ordering instruments. Most vendors will provide one if you push for it, and a lot won't, which tells you something about their confidence in the product.
Calibration and Traceability
Calibration means comparing your instrument against a known standard and documenting the difference. Traceability means that chain of comparisons links all the way back to an internationally recognized reference, usually a national metrology institute like NIST or PTB in Germany. Without traceability, your calibration certificate is just a piece of paper. I had a situation once where a vendor sent us a certificate for a block gauge set, and when I checked the traceability chain, it went through a third-party lab that listed its own reference as "calibrated against internal standards." That's not traceable. That's circular reasoning with paperwork. The ISO 17025 standard exists specifically to prevent this. Any lab claiming traceable calibrations should be accredited under that standard, and you can verify that accreditation on the accrediting body's website. It takes about three minutes to check. Don't skip it. The cost of a bad calibration certificate shows up later when you reject a batch of parts that were actually fine, or worse, ship parts that are out of tolerance.
Get the Full Details

Tolerance and Tolerance Stack-Up
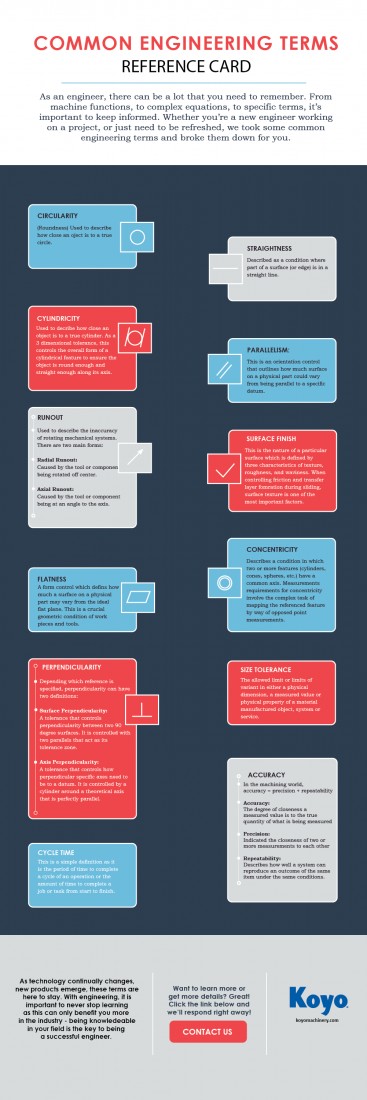
Tolerance is the allowable variation from a nominal dimension. A shaft called 25.00mm with a tolerance of ±0.05mm can be anywhere between 24.95 and 25.05 and still pass. Simple enough. The hard part comes when multiple tolerances interact in an assembly, and that's where tolerance stack-up analysis lives. Every component in a multi-part assembly has its own tolerance, and those variations add up, sometimes in the worst possible direction. I worked on a hydraulic manifold assembly where we had twelve mating surfaces, each with a flatness tolerance of 0.02mm. The worst-case stack-up was 0.24mm of cumulative deviation. The design called for a maximum gap of 0.05mm between the plates. We were going to fail every single unit if we built to spec. What we ended up doing was selecting the plates by measured thickness and shimming the stack, which cut our rework rate from about forty percent down to under five percent. You can also use statistical tolerance analysis instead of worst-case. It assumes most parts cluster near nominal rather than sitting at the extremes, which is usually true if your process is stable. That approach gives you a much smaller predicted stack-up, but it requires actual process data, not just nominal and limit values from a drawing.
Repeatability and Reproducibility
These two terms get lumped together as GR&R studies in quality work, and they mean different things. Repeatability is the variation you get when the same operator measures the same part repeatedly with the same instrument under unchanged conditions. Reproducibility is the variation when different operators measure the same part, or the same operator uses different instruments. In my experience, reproducibility is almost always the larger source of variation. People interpret "measure here" differently, even when there's a marked reference point on the part. A good rule of thumb: if your GR&R study shows measurement variation above ten percent of the tolerance band, you have a problem. Above thirty percent, the measurement system is unacceptable for process control. Between ten and thirty percent is a gray zone where you might accept it for some applications but not others. I keep a simple spreadsheet where I track GR&R results across all our measurement systems. It helps spot trends, like when a particular operator consistently reads high on a specific gauge, which usually means they're applying force differently or reading at a slight angle.
Linearity and Bias
Linearity describes whether your instrument's accuracy stays consistent across its entire measurement range. A gauge that's accurate at one end of its range but drifts at the other end has poor linearity. Bias is the systematic offset between your instrument's average reading and the true value. Both are important, and both can coexist. I once inherited a CMM that measured within spec at the origin point but drifted by eighty microns at the far edges of its travel. The linearity error was caused by a loose guideway that only became apparent under load at maximum extension. Fixing it required a full re-level and replacement of two linear guide blocks, which cost about three thousand dollars in parts and two days of downtime. A linearity check using a step gauge or calibration bar at multiple points across the range would have caught this during routine calibration. Stability is your instrument's ability to maintain its calibration characteristics over time. Drift is what happens when stability fails. Temperature changes, mechanical wear, electronic component aging, and even humidity can cause drift. I've seen optical encoders on CNC machines slowly lose position accuracy over months because the scale factor shifted as the LED source aged. The machine didn't alarm. It just started making parts that were two hundred microns too long, and nobody noticed until quality caught it on a first-article inspection. The fix was replacing the encoder assembly, but the real lesson was that we should have been doing periodic confirmation checks with a known artifact, not just relying on the machine's own error compensation. The industry standard for tracking drift is a control chart on calibration results. Plot your instrument readings against known standards over time, and you'll see the trend before it becomes a problem. Some shops do this automatically through their lab information management system. Others still do it on paper, which works fine if someone actually looks at the data instead of filing it away.
Sensitivity and Threshold
Sensitivity is how much the instrument's output changes for a given change in the measurand. A dial indicator with 0.001mm per division is more sensitive than one with 0.01mm per division. Threshold is the smallest change in input that produces a detectable change in output. For a digital scale, this might be the minimum weight change needed to toggle the last displayed digit. These two concepts are related but distinct, and confusing them leads to bad instrument selection. I've seen people buy a high-resolution digital caliper for a job that required measuring surface roughness, not because the resolution was insufficient but because the instrument's response time and sampling characteristics were wrong for the application. Resolution alone doesn't tell you whether a tool is suitable. Fidelity describes how faithfully an instrument reproduces the input signal. Dynamic response is how quickly the instrument reacts to a changing measurand. For static measurements like checking a machined dimension, dynamic response rarely matters. For vibration analysis or, it's everything. I worked on a project where we were measuring tool wear on a milling machine by monitoring spindle vibration. Our accelerometer had a natural frequency of fifty kilohertz, which was fine for most cutting operations, but when we switched to high-speed machining at twenty thousand RPM with a small end mill, the relevant frequency content pushed past sixty kilohertz. The accelerometer was still functioning, just attenuating the signal we actually needed. Upgrading to a sensor with a two hundred kilohertz natural frequency solved it immediately. The lesson was that checking the datasheet for bandwidth matters more than checking resolution when you're dealing with dynamic measurements. Hysteresis is the phenomenon where your instrument gives a different reading depending on whether you're approaching the measurement from above or below. A spring-based force gauge is a classic example. When you load it slowly, the spring deflects one way. When you unload it, the spring doesn't return to exactly the same position because of internal friction and material memory effects. The difference between the loading and unloading curves is the hysteresis error. In precision engineering work, hysteresis can dominate your uncertainty budget if you're not aware of it.
The workaround is simple: always approach a measurement from the same direction. For calipers and micrometers, this means closing the jaws onto the part rather than opening them away. For coordinate measuring machines, it means following a consistent probe approach vector. Most people do this instinctively after enough experience, but it's worth noting explicitly because hysteresis is invisible in a single reading. You only see it when you compare approach directions.
Uncertainty and Confidence Intervals
Measurement uncertainty is the quantitative expression of how much doubt exists about a measurement result. It's not the same as error, which is the difference between a measured value and the true value. Uncertainty characterizes the dispersion of values that could reasonably be attributed to the measurand. The GUM, or Guide to the Expression of Uncertainty in Measurement, is the international framework for calculating and reporting uncertainty. It distinguishes between Type A evaluation, which uses statistical analysis of repeated observations, and Type B evaluation, which uses other information like manufacturer specifications or calibration certificates. In practice, most engineers I work with don't calculate full uncertainty budgets for every measurement. They should, but they don't. A practical middle ground is to treat the instrument's stated accuracy as a rectangular distribution and divide by the square root of three to get a standard uncertainty component. That's approximately correct for many practical situations and takes about thirty seconds to compute. For critical measurements, you need the full GUM approach with all uncertainty sources identified and quantified. I keep a template for this that lists common sources: instrument resolution, calibration uncertainty, thermal effects, operator influence, and environmental factors. Filling it out for a new measurement task usually takes fifteen to twenty minutes and prevents a lot of headaches later.