What Actually Goes Into a Training Diagram for FDM Printers
A 3D Printer Training Manual Diagram is a visual reference that maps the physical layout of a printer alongside the key settings a new operator needs to touch. It is not a software manual. It is a wall-mounted or tabbed PDF that shows where the nozzle sits, where the spool feeds, which calibration routine runs first, and what to do when the first layer fails. I built several of these for a small machine shop that had roughly eight printers across three rooms. After the third round of questions from new hires, I stopped writing prose and started drawing. The first version I made was two pages of text with a single schematic at the top. Nobody read it. People stood at the printer asking the same questions for weeks. The turnaround happened when I switched to a single large diagram with callouts that matched the actual hardware labels. That version lasted months before someone wanted an update.
3D Printer Training Manual Diagram
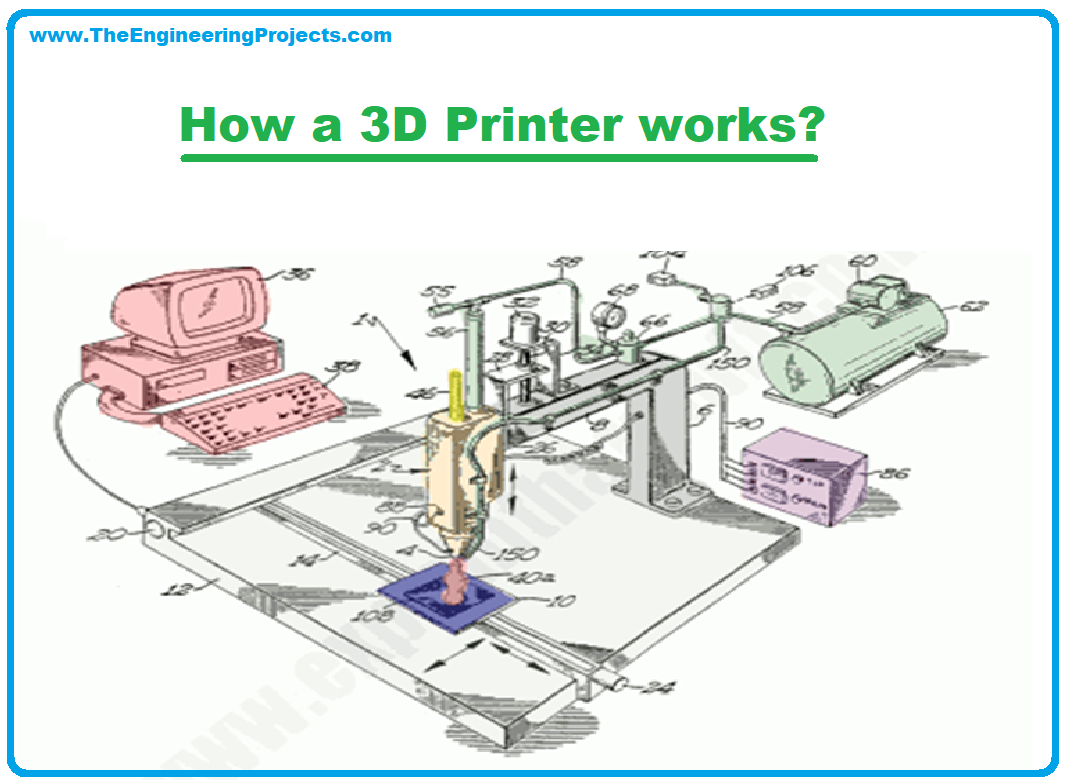
Here is what ended up on the final sheet for our most common setup, a CoreXY FDM machine with a direct drive extruder and an auto-bed leveling probe. The top third showed a clean top-down view of the printer with numbered zones. Zone one was the filament path from spool holder to extruder gear. Zone two was the nozzle and build plate area with a small inset showing first-layer height measurement using a piece of copy paper as a feeler gauge. Zone three was the control screen with annotated buttons. Zone four was the emergency stop location and power switch. Zone five was the probe and its calibration routine access point. Each zone had a short text strip that did not repeat the label but gave the action, change filament here, purge 50 millimeters after load, jog the head manually before running a full homing cycle. The bottom third covered the four critical print settings that cause most beginner failures. Nozzle temperature range with a default and an adjustment rule for PLA versus PETG. Bed adhesion settings including the Z offset procedure and when to skip releveling. Print speed and the common trap of running 60 millimeters per second on the first layer when the manual suggests 20. Layer height and the often-missed relationship between layer height and nozzle diameter, keeping layer height below eighty percent of nozzle size to avoid visible ridges on steep overhangs.
The middle section was a troubleshooting flow chart. First layer not sticking leads to check bed cleanliness, then check bed level, then check nozzle height. Strings and robing leads to retraction settings, then temperature reduction by ten degrees, then coasting enable. Layer shifting leads to belt tension check, then acceleration settings reduction, then check for loose couplers on the stepper motors. I put this on a laminated A3 sheet and mounted it two meters from the printer, at eye level when standing. We used a quick reference card for daily operations and the full diagram for onboarding. The breakdown rate for new operator errors dropped from roughly forty percent in the first week to under fifteen percent by the third week, based on our scrap log. Not because people read more, but because the diagram matched what they saw on the machine. There are places where this approach does not work well. If your shop has five different printer models with different control interfaces, a single diagram becomes a mess of exceptions. In that case, split by model and keep a shared primer section for concepts that apply across machines, thermal runaway protection, emergency stop procedure, filament storage humidity targets. Another limitation is that diagrams age poorly. When you update firmware or swap a hotend, the callout for the calibration routine may no longer match the menu path. We kept a revision date on every sheet and updated within forty-eight hours of a hardware change. The cost of a reprint is lower than the cost of a misprinted instruction causing a failed build.
Get the Full Details

The biggest counter-intuitive point I learned is that beginners do not need more information, they need less ambiguous information. A diagram that shows five possible temperatures for PLA will paralyze a new operator more than one wrong but clear number. Pick the default that works for ninety percent of jobs, note the exception briefly, and move on. Another pitfall is assuming that a good diagram replaces hands-on practice. It does not. The diagram gets someone to the point where they can run a test print with minimal guidance. The actual skill comes from doing the print and seeing the result. Our onboarding time went from two days of shadowing to half a day of supervised practice, but we still required three completed test prints before an operator could run a job without supervision. If you are building one from scratch, start with the hardware layout, draw what the operator sees when standing in front of the machine, then add the settings that matter most, not all settings. End with the failure modes that actually happen in your shop, not the textbook list. A diagram that reflects real problems will last longer than one that reflects ideal conditions.