Converting Millimeters to Inches Without Losing Your Mind
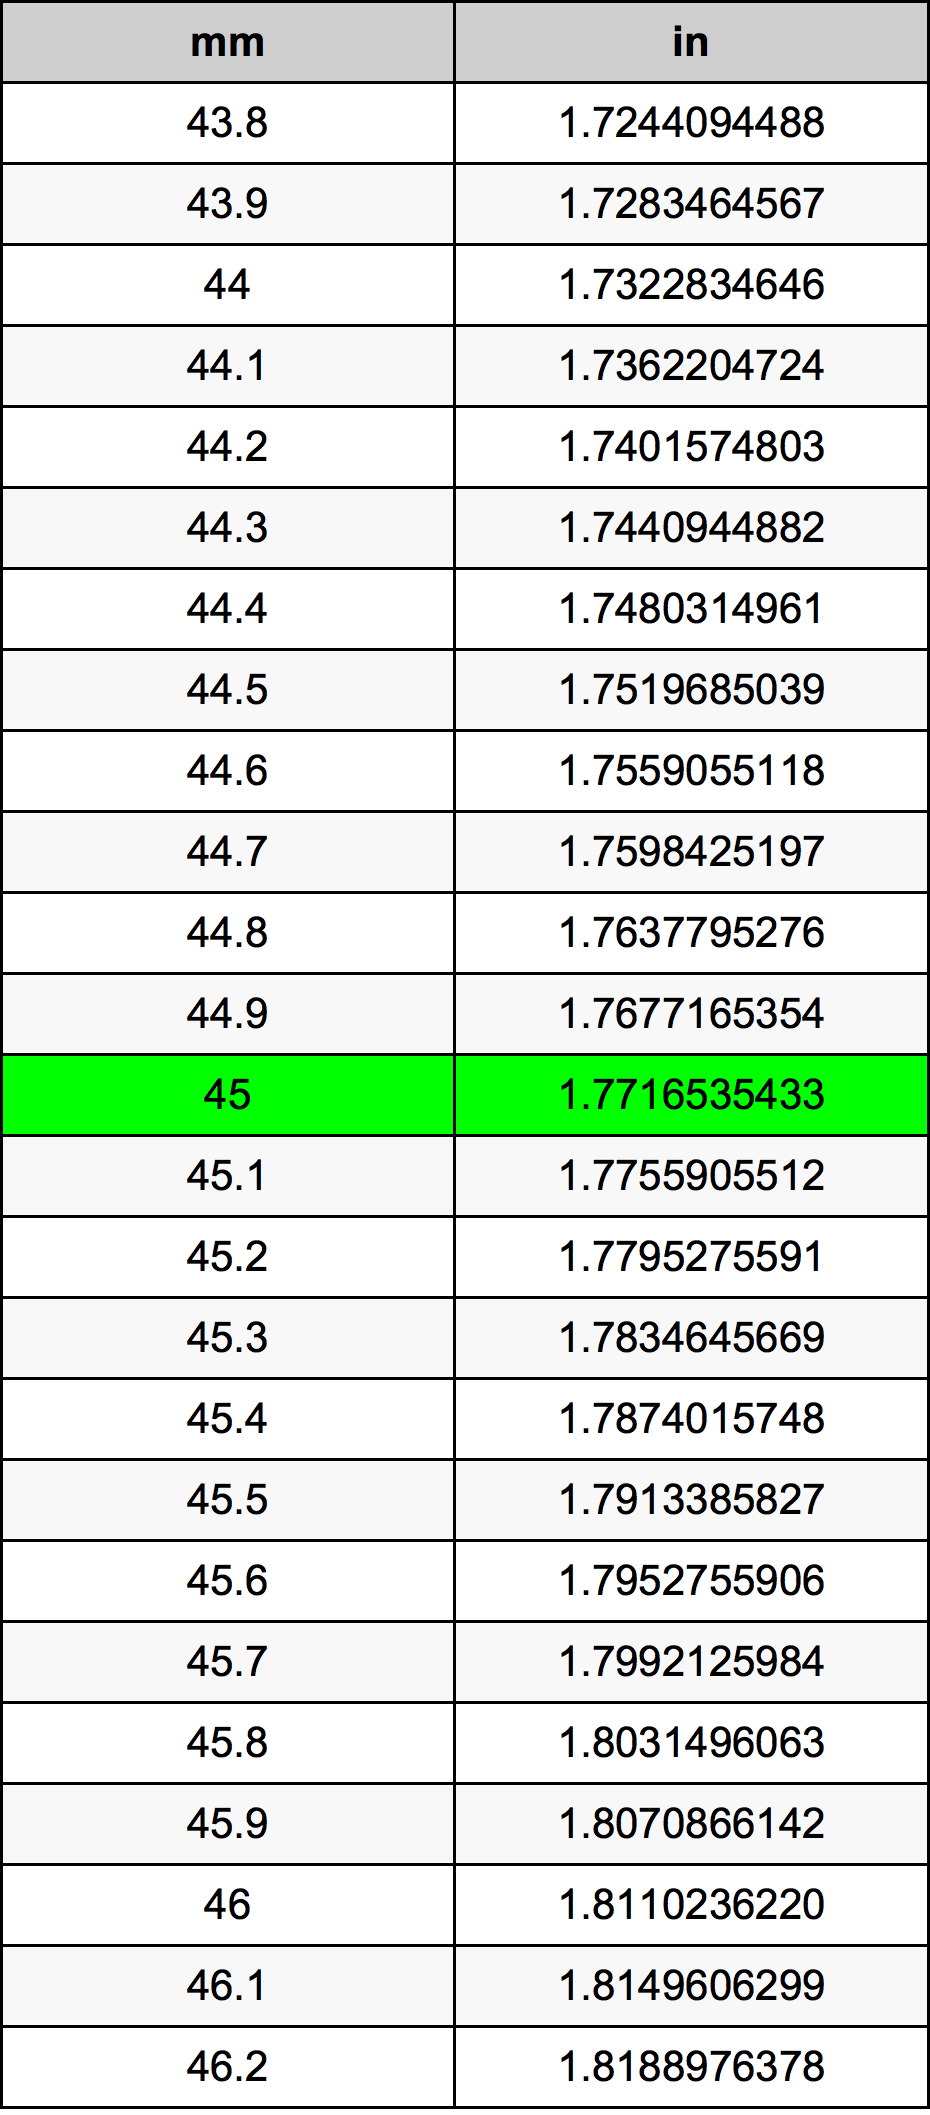
The conversion factor is simple enough: divide your millimeter value by 25.4 to get inches. That's the whole mechanism behind it. One inch is defined as exactly 25.4 millimeters, established internationally in 1959, so there's no rounding ambiguity if you're working with exact numbers. I deal with this conversion constantly because a lot of my tooling and stock arrives in metric while the prints and CNC programs I'm running off are imperial. The actual math for 45 Mm To Inches gives you 1.77165 inches. On paper that looks precise, but in practice you'd round it to 1.77 or 1.772 depending on your tolerance stack. Most people I see online round too aggressively and end up with parts that don't fit together. A difference of 0.002 inches sounds negligible until you're trying to press-fit a shaft into a bearing and it won't go in.
How to Actually Calculate 45 Mm To Inches
There are three ways I've found to handle this without second-guessing myself. The first is manual division: take 45 and divide it by 25.4. That gives you 1.7716535... You can do this in your head if you're fast with long division, which I am not, so I rarely bother. The second way is a spreadsheet formula, which is what I actually use most of the time. Cell A1 contains your metric value and Cell B1 runs =A1/25.4. The benefit here is that when the drawing changes from 45 mm to 46 or 44, you don't recompute anything. It just updates. This cuts down the conversion time from probably 30 seconds to nearly zero per measurement across an entire BOM. The third way is a conversion calculator or app. There are dozens free online. I'll be honest and say I avoid these for anything beyond quick lookups because I've had calculators give me wrong results when I was in a hurry once. Not this specific conversion, but the principle stands. If you're submitting a part to a client or posting tolerances on a print, double-check with a different method.
Here's something most people miss: the 25.4 factor only applies cleanly when you're converting linear measurements. If you're converting area or volume, you need to square or cube the factor. Converting 45 square millimeters to square inches isn't 45 divided by 25.4. It's 45 divided by 645.16, which equals roughly 0.0698 square inches. I've seen machinists mess this up and order the wrong sized sheet material because they applied the linear factor to an area calculation. That mistake costs real money. Another thing nobody tells you about this kind of conversion is how fractional inches work in practice. Machine shops in the US still prefer fractions over decimals on drawings. 1.77165 inches doesn't mean much to someone working at a bench with fractional calipers. You'd want to express it as a fraction. 1.77165 is approximately 1 and 25/32 inches, or more precisely 1 and 45/254 if you want to be exact. The closest standard fractional drill bit would be 1-25/32, which is 1.78125 inches. That's about 0.01 inches off, which might be fine for a clearance hole or it might be unacceptable for a precision fit. You have to decide based on the application, not the conversion itself. I ran into a real problem last year with a 45 mm bore that needed to convert cleanly to a bearing seat. The bearing was specified as 1.77 inches, but standard imperial bearings don't come in that size. The metric bearing at 45 mm would fit if I bored the housing out slightly, but the housing was already machined to 1.77 inches by the original design. I ended up sourcing a metric 45 mm bearing and lightly honing the housing to 45.05 mm to get a light interference fit. The conversion itself was trivial. The real issue was that the design didn't account for the gap between what exists in metric and what exists in imperial standard sizes. That kind of misalignment happens way more often than people expect.
Get the Full Details
If you're doing this kind of work regularly and need a reference, the NIST conversion tables are the authoritative source. They publish the exact definitions and a full lookup table. You can find them at nist.gov/pml/weights-and-measures/si-conversion. It's free and it's the official US government standard. I've cited it directly on engineering submittals before when someone questioned a conversion. The main limitation with any manual or calculator-based conversion approach is that you're only as accurate as your input. If the original 45 mm measurement came from a cheap caliper with plus or minus 0.02 mm error, your converted inch value inherits that same uncertainty. No amount of decimal places in the conversion factor fixes that. You should report your final result with the same number of significant figures as your least precise measurement. For 45 mm, which has two significant figures, the proper converted value is actually 1.8 inches, not 1.77165. Writing out all those decimals implies a precision you don't actually have.
Common Mistakes When Converting 45 Mm To Inches
The biggest error I see is people multiplying by 25.4 instead of dividing. That gives you 1143 inches for 45 mm, which is obviously wrong but happens far more often than you'd think, especially under time pressure. Another is forgetting which direction to go: millimeters to inches means the number gets smaller, so if your result is bigger than your input, something is backwards. A less obvious mistake is assuming that because 45 mm converts to about 1.77 inches, you can swap them interchangeably on a drawing without noting the change. Tolerance analysis changes when you switch systems. A ±0.1 mm tolerance on a 45 mm feature is not the same feel as a ±0.1 inch tolerance on a 1.77 inch feature, even though they're close in absolute terms. The relative tolerance differs. Always recheck your tolerances after converting.