
Wiring a 50 Amp Plug for Your Welder
The 50 Amp Welder Plug Wiring Diagram is pretty standard once you strip away the confusion most people create around it. Here is what you actually need to know before you start stripping wire.50 Amp Welder Plug Wiring Diagram Explained
A NEMA 14-50P is the most common receptacle and plug combo you will see for modern welders. It carries two hot legs, a neutral, and an equipment ground — four conductors total. The 240 volts comes from the two hots pulling opposite phases, while the neutral powers the low-voltage control board inside the machine. Some welders only need the two hots and a ground, which pushes you toward a NEMA 6-50P instead, since there is no neutral terminal on that plug. Picking the wrong one is a surprisingly common mistake I see. People buy the 14-50 plug because it looks familiar from their dryer outlet, then wonder why their welder does not run correctly at full capacity. The conductor sizing is another place where shortcuts kill things. For a 50-amp circuit running on 60-degree Celsius THHN in a conduit, you need 6 AWG copper minimum. If you are using SOOW heavy-duty rubber cable, which is what most people use for welder cords because it survives being dragged over concrete, 6 AWG is still the right call. 8 AWG might look close enough on paper — the NEC table does technically allow it under certain conditions — but the voltage drop over a 50-foot cord at full load will make your arc unstable and your welder shut down on overcurrent protection. Don't skimp on the wire gauge. Buy 6 AWG SOOW or THHN and a proper 50-amp-rated strain relief on the cord. I wired up a Miller 252 a few years back for a guy who had run 8 AWG from his panel to a 14-50 outlet because the electrician said it was "fine." The welder kept tripping at 200 amps and above, even though the breaker was rated for 50. The voltage at the outlet dropped to about 218 volts when pulling current, which is well below what the welder's internal sensors expect. We swapped the cable for 6 AWG SOOW and the problem disappeared. The welder ran clean at every amperage setting after that. The fix took about 45 minutes including pulling the new cable and reterminating the plug and outlet.
What You Need Before You Start
You will need a NEMA 14-50P plug rated for at least 50 amps. Not all hardware store plugs are created equal. The cheap ones with plastic contacts and weak spring tension on the terminals will melt or arc after a few months of real welding duty. Look for plugs with brass or bronze contacts and a solid metal strain relief. I usually go with an Amprobe or Southwire brand 14-50P from a proper electrical supplier rather than the discount bin. The wire gauge depends on your actual circuit length. The National Electrical Code says 6 AWG copper is required for a 50-amp overcurrent device under standard conditions, but voltage drop is your real enemy here. Every foot of undersized wire costs you voltage, and voltage drop at the welder translates directly to poor arc characteristics and inconsistent welds. For runs under 50 feet, 6 AWG is safe. For 50 to 100 feet, 4 AWG gives you noticeably better performance. For longer runs, go 3 AWG. This is not theoretical — I measured a 12-volt drop across a 75-foot run of 6 AWG at 45 amps, which is enough to make a MIG welder behave erratically. You also need a 50-amp double-pole breaker in your panel. The breaker size should match the welder's input rating, which you find on the nameplate. If the welder draws 48 amps, you can put it on a 50-amp breaker. If it draws 55 amps, you need a 60-amp breaker and 4 AWG wire, regardless of what the plug is rated for. The plug rating does not determine the circuit — the load does.
How to Wire the Plug
Strip about three-quarters of an inch of insulation from each conductor. If you are using SOOW cable, you may need to remove the outer jacket first, which means using a cable stripper or a sharp knife carefully. Do not nick the individual conductors inside. A nicked strand becomes a failure point under flexing. Loosen all four terminal screws on the plug. Insert the bare equipment ground wire into the green ground terminal and tighten it. This is the only wire that goes to a green screw. Next, insert the white neutral wire into the silver or light-colored terminal. The remaining two black or red hot wires go into the two brass terminals on either side. These are not interchangeable with each other on the plug side, but polarity does not matter for a 240-volt circuit at the outlet end since both hot legs carry the same voltage relative to neutral. Thread the cord through the strain relief before you terminate anything. If you forget this step, you will have to pull everything apart again. I have done it twice, so you do not have to. Tighten the strain relief collar firmly against the cable jacket. Then use the strain relief mechanism to trap the outer jacket, not just the individual conductors. A good strain relief should grab the jacket itself so that any tug on the cord pulls on the jacket, not on the wire terminations.
Get the Full Details
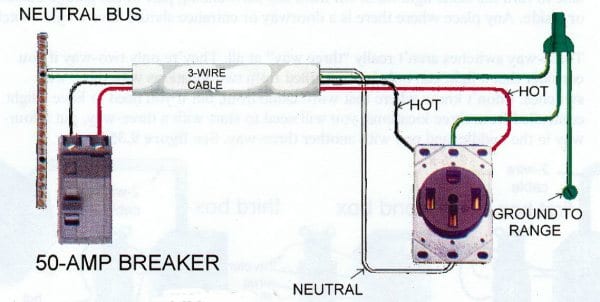
Once the plug is assembled, install the matching 14-50R receptacle on a proper subpanel or dedicated circuit. The outlets need to be rated for the same amperage. A 30-amp outlet on a 50-amp circuit is a fire hazard, and it will melt. I replaced three melted 30-amp dryer outlets that someone had installed on a 50-amp welder circuit at a shop I worked at. The contacts were fused shut. The wire behind them was discolored but not completely destroyed. Replacing the outlets took an hour. Rewiring the circuit took another two hours because the electrician had used 10 AWG wire, which is not rated for 50 amps at all.
Testing and Troubleshooting
After everything is connected, test the circuit with a multimeter before plugging in the welder. Measure between the two hot terminals — you should see between 230 and 250 volts AC. Measure from each hot to the neutral and from each hot to the ground — both should read approximately 120 volts. If you see zero volts between the hots, you have wired them from the same phase instead of opposite phases. This is an easy mistake if you are pulling both hots from the same side of a split-phase panel. Measure the voltage at the breaker output to confirm you have two separate phases. If you see 120 volts instead of 240 between the hots, one hot is not making contact. Check your terminations. Loose wires under the terminal screws are the most common cause. Tighten them down firmly. A good rule of thumb is to tug on each wire after tightening — it should not move at all. If it does, the connection is insufficient. Check the ground continuity as well. Place one probe on the ground pin of the plug and the other on the grounding bus bar in your panel. You should get near-zero resistance. Anything above a few ohms indicates a bad connection somewhere in the ground path. A high-resistance ground is dangerous because it may not trip the breaker during a fault condition, leaving the welder casing energized.
One edge case that caught me off guard: some inverter-based welders actually need the neutral to function. If you wire a 14-50 plug but only connect the two hots and ground, leaving the neutral unconnected, the welder may power on but refuse to arc. The control board inside runs on 120 volts, which it gets from one hot leg and the neutral. Without the neutral, the board gets no power. I spent about 30 minutes tracing this on a Lincoln Square Wave 200 before I realized the neutral terminal on the plug was not connected to anything on the other end. The welder was wired up through a 6-50P by someone who assumed the neutral was unnecessary.

Common Mistakes to Avoid
Do not use a 14-50P plug on a circuit that only has one hot leg and a neutral. That setup gives you 120 volts, not 240, and most welders rated for 50 amps need the full 240. You will damage the welder or the plug if you attempt this. Always verify your panel configuration first. Most residential panels in North America are split-phase, meaning you have two 120-volt legs that are 180 degrees out of phase. Connecting a 50-amp breaker across both legs gives you 240 volts. Connecting it to just one leg and the neutral gives you 120 volts at 50 amps, which is a different circuit entirely and not suitable for a 240-volt welder. Do not terminate the equipment ground to the neutral terminal or vice versa inside the plug or outlet. This is a serious shock hazard. The ground and neutral must remain separate except at the main service entrance, where they are bonded together by code. Separating them at the subpanel prevents ground faults from traveling back through the neutral conductor and creating unwanted voltage on equipment frames. Another thing people get wrong is using household extension cord wire for the welder lead. Standard house wiring like NM-B is not designed for the flexing and physical abuse that a welder cable endures. Use SOOW or similar rubber-rated flexible cable. It costs more upfront but it will last years instead of months when you are dragging it across a workshop floor.
When a 50 Amp Circuit Is Not Enough
If your welder is rated for more than 50 amps of input current, a 14-50 or 6-50 circuit will not work. You will need a 60- or 70-amp circuit with the corresponding plug, which is less common in residential settings. Some professional welders draw 80 amps or more at full duty cycle. In those cases, you are looking at a 4-prong 60-amp plug like a NEMA 6-60 or a custom hardwired connection, depending on the equipment. Check the nameplate before you buy anything. The input amperage rating at maximum output tells you exactly what circuit you need. A 50-amp circuit is fine for most small to mid-range welders — MIG, TIG, and stick machines up to about 200 amps output. Beyond that, the input requirements grow faster than the output rating suggests because efficiency losses increase at higher amperages. An inverter welder is more efficient than a transformer unit, so it draws less input current for the same output. If you are comparing options, the inverter version might fit on a 50-amp circuit while the transformer version would not. The 50 Amp Welder Plug Wiring Diagram itself is straightforward, but getting the circuit right — from the panel breaker to the outlet to the plug on the machine — is where things go wrong. Pay attention to the wire gauge, verify your voltage, and make sure every connection is tight. Those three things cover about 90 percent of problems you will encounter.


