Understanding Gas Turbines in the 60MW Range
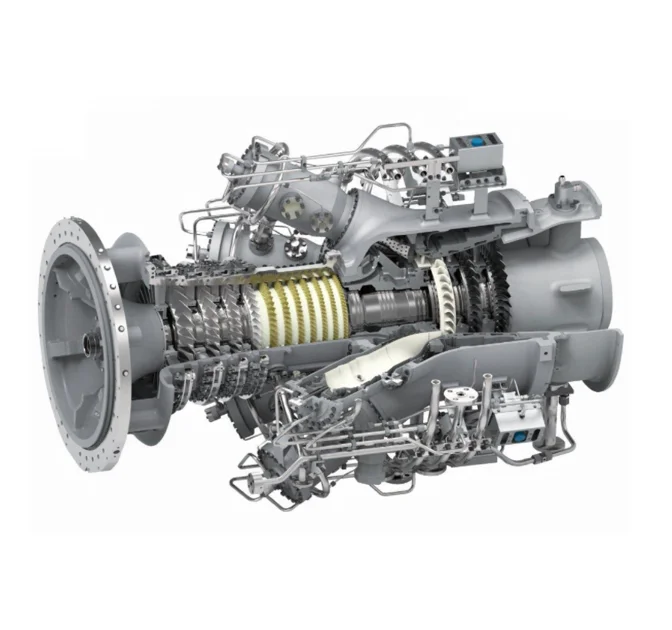
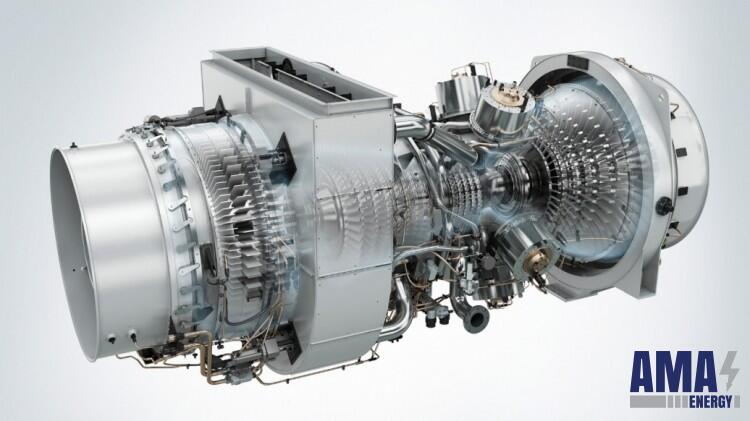
If you're working with gas turbines around the 60-megawatt class, you're looking at heavy-duty industrial units like the GE 6HA or similar frameworks from Siemens and Mitsubishi. These are the workhorses for power plants, oil and gas facilities, and cogeneration sites. They're not small by any means, and they don't tolerate sloppy maintenance schedules. The 60 Gas Turbine category generally refers to machines in that power band. You'll see them deployed in simple cycle configurations or paired with heat recovery steam generators for combined cycle operation. The distinction matters because it changes your operational approach entirely. Simple cycle is straightforward—intake, compression, combustion, expansion, exhaust. Combined cycle adds a whole other layer of complexity with steam generation, turbine extraction points, and thermal management that you need to account for in your downtime windows.
Starting Up a 60 Gas Turbine: The Practical Sequence
Hot shutdowns are where most people get burned, literally. If you've just tripped the unit and it's still thermally stressed, going straight into a restart without checking bearing clearances and rotor expansion can cause seal damage or blade rubbing. I had a unit trip on high vibration at 42 megawatts during a summer shift. The operator wanted to hot start it within 20 minutes. The manufacturer's window said minimum 4 hours for a cold start transition. I ran the numbers on the rotor thermal profile and convinced them to wait. Two hours later we found a worn lube oil seal that would have failed catastrophically under thermal stress. Worth mentioning that waiting saved us a four-day outage. The normal startup sequence runs through several phases. First you verify auxiliary systems—lube oil pressure, control air, fuel gas conditioning. Then the turning gear engages while you monitor rotor bow. Once the shaft rotation stabilizes, you begin cranking. The ignition sequence follows, with flame detection verification before fuel continues to flow. From there you accelerate through the transition curve, watching exhaust gas temperature spread across all thermocouples. A spread exceeding 30 degrees Fahrenheit at rated load usually indicates a fuel nozzle issue or compressor fouling. Don't ignore that.
Load Maneuvering and Thermal Fatigue
Modern 60 Gas Turbine controls allow reasonably aggressive ramp rates, but your component life is eating into that capability with every rapid transition. The first stage rotor and nozzle guide vanes take the highest thermal cycling damage. If your plant is cycling daily between base load and peaking duty, plan on replacing those components at roughly half the standard interval. The manufacturer might quote 80,000 hours for a fixed-base installation. For a cycling application, you're looking at 40,000 to 50,000 hours before inspection is warranted. I once saw a site running aggressive ramps of 15 megawatts per minute just to chase spot prices. Within 18 months, they had multiple cracks in the first stage nozzles. The OEM's stress model hadn't accounted for their particular ramp profile. They ended up doing an out-of-service inspection at half the expected interval, which cost them roughly 300,000 dollars in lost revenue alone. The fix was recalibrating their ramp limits to 8 megawatts per minute and adding intermediate hold points during significant load changes. It hurt their dispatch flexibility but saved them from emergency overhauls.
Get the Full Details

Fuel Quality and Combustion Dynamics
Gas turbines in this class are typically designed for natural gas, but many operate on distillate fuel as a backup or primary source. Liquid fuel changes everything about your maintenance schedule. Combustor liners, transition pieces, and exhaust casings accumulate deposits differently. Fuel nozzle coking becomes a real problem if your fuel isn't properly filtered and heated to specification. I've seen sites run with fuel temperatures 15 degrees below the recommended range and wonder why they were getting lean blowout issues during startup. Dry low NOx combustors add another constraint. These systems operate with very lean fuel-air mixtures to minimize emissions, which makes them more susceptible to combustion instability. You'll see pressure oscillations in the 15 to 40 Hertz range that can damage thermocouple wells and flame detectors over time. If your unit has a DLN combustor and you're seeing elevated vibration during part load operation, check the fuel split between the pilot and main zones. An improperly calibrated fuel manifold will push the mixture into an unstable region even when the control system thinks everything is nominal.
Compressor Washing and Performance Recovery
In-line compressor washing is the single most effective performance restoration method available to operators. A typical 60MW unit that hasn't been washed in six months will lose approximately 2 to 3 percent of its firing temperature and corresponding power output. That's 1.2 to 1.8 megawatts gone for no reason. Online washing recovers about 60 to 70 percent of that degradation. Offline washing with specialized solutions gets you back to nearly full recovery, but it requires taking the unit offline for 4 to 6 hours. The frequency depends entirely on your inlet air quality. Coastal installations with salt exposure may need washing every two weeks. Inland sites with good filtration can stretch to 60 to 90 days between cycles. I track a simple metric: heat rate degradation per day of operation. When I see the heat rate creeping above the baseline by more than 0.5 percent over a week, it's time to schedule washing regardless of the calendar interval.
Vibration Monitoring and What It Actually Tells You
Most operators watch the absolute vibration level on the shaft probes. That's useful but incomplete. The phase angle between probe measurements tells you far more about the actual problem. A consistent phase change during acceleration points to a rub or misalignment. Random phase shifts suggest aerodynamic instability or bearing issues. I spent three days chasing a vibration alarm on a 62-megawatt unit that only appeared between 75 and 85 percent load. The absolute level never exceeded the alarm setpoint, but the phase trace was erratic. We ended up finding a partial annular seal rub that only engaged under specific thermal conditions. The fix was adjusting the seal clearance during the next outage, which cost nothing beyond a few hours of labor. Exhaust gas temperature profiling deserves equal attention. Twelve or more thermocouples span the exhaust casing. The spread between the hottest and coldest reading is your primary indicator of combustion efficiency. A spread widening beyond normal operating range usually means one or more fuel nozzles are partially blocked or the compressor is approaching surge. Don't wait for the high temperature alarm to trigger. Watch the trend.

Common Pitfalls for Operators New to the 60 Gas Turbine Class
One mistake I see repeatedly is underestimating the importance of inlet air filtration maintenance. A clogged filter doesn't just reduce airflow—it changes the pressure differential across the intake system, which affects compressor map positioning. Sites that skip filter changes to save money often find themselves dealing with compressor surge events that damage blades. The filters cost a fraction of what a compressor repair does. Another issue is ignoring the control system's auxiliary input limits. Many modern 60 Gas Turbine platforms accept external signals for emissions override, dispatch commands, or auxiliary load shedding. If you're integrating with a SCADA system or a grid management platform, make sure the signal conditioning matches what the turbine controller expects. I've seen mismatched voltage levels fry input cards and cause unexpected trips during routine operations. There's also a tendency to treat the manufacturer's maintenance manual as gospel without considering site-specific conditions. The baseline intervals assume clean air, stable fuel, and normal cycling patterns. If your reality diverges from those assumptions, adjust your intervals accordingly. The manual will not do that for you. Keep your own records, track degradation trends, and make decisions based on your data rather than a generic schedule.
The 60 Gas Turbine class is mature technology, which means there are plenty of published resources, but the gap between textbook knowledge and field reality is where problems actually develop. Pay attention to trends, document anomalies, and don't rush restarts after unexpected trips. The unit will run reliably for decades if you give it consistent, informed care. Neglect shows up fast and expensive.