Why Your Shaft Alignment Keep Drifting After Startup
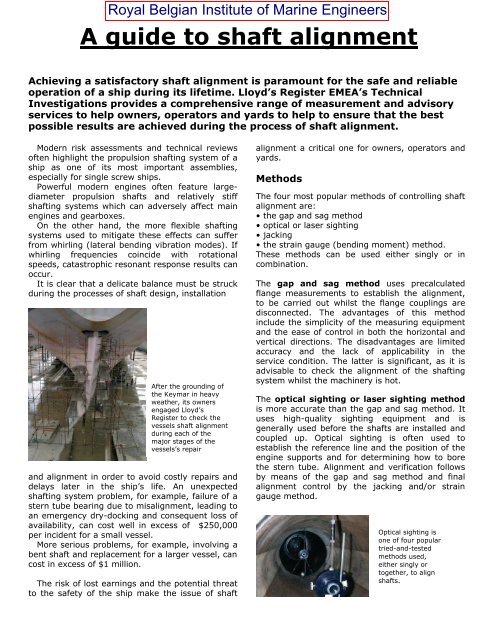
I spent three years fighting thermal growth problems on pump trains before someone showed me the Gallois method properly. Most people learn rim-and-face alignment and call it a day. That gets you to rough alignment. If you want to hold within ten thousandths all day long when machines heat up, you need the Gallois approach. The core idea is simple and most beginners miss it entirely. You're not just measuring how far apart the shafts are at the coupling face. You're measuring the angular deviation between the two shafts at two different planes simultaneously. That gives you enough information to calculate how to move both the near feet and far feet of the machine in a way that accounts for soft foot, foundation flexibility, and thermal growth in one pass. This usually cuts a two-day alignment job down to about three hours when you're doing multiple pump sets on a common baseplate. The math is a little heavier than basic dial indicator work, but once it's on paper or in a spreadsheet, it goes fast.
A Guide To Shaft Alignment Gallois
The Setup
You need two dial indicators mounted on a rigid bridge that spans from the driving shaft to the driven shaft. One indicator measures radial displacement at the coupling — that's your rim reading. The other measures axial displacement across the coupling face — that's your face reading. The bridge has to be stiff. I once used a cheap adjustable bridge on a 50-horsepower motor and the bridge flexed about three thousandths under its own weight when I tilted it upward. That threw off every reading. Bought a proper rigid alignment bridge and the problem vanished. Mount the indicators so the probe tips contact clean, flat surfaces. Rim indicator goes against the coupling half or a target on the shaft. Face indicator goes against the mating coupling half's face. Both probes should be preloaded about two thousandths — enough to stay in contact through a full 360-degree rotation, not so much that you're binding the gauge.
How to Take Readings
Zero everything at the 12 o'clock position. Rotate both shafts together in small increments — quarter turns work fine for most industrial alignments. Record rim and face readings at 0, 90, 180, and 270 degrees. Write them down in a table. Don't try to do this in your head. Here's a real example from a job I did last year. Three-phase induction motor coupled to a centrifugal pump. New installation, rigid baseplate, no soft foot concerns initially. Readings came back: At 12 o'clock: rim = 0, face = 0 (zeroed here)
Get the Full Details
At 3 o'clock: rim = +4 mils, face = +3 mils At 6 o'clock: rim = +8 mils, face = +6 mils At 9 o'clock: rim = +4 mils, face = +3 mils
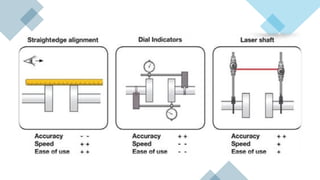
The symmetry tells you immediately that the shafts are angularly misaligned, not parallel offset. The rim and face readings both increase evenly from 12 to 6 o'clock, which means the driven shaft is angling away from the drive shaft as you move toward the pump. In plain terms, the pump is tilting backward relative to the motor.
The Calculations
The Gallois method uses these readings to determine shim changes at each machine foot. You need four measurements on your alignment plate: the distance from the coupling centerline to the near feet (let's call it B), the distance from the near feet to the far feet (distance C), the rim indicator radius (R), and the face indicator span (F). These are physical measurements you take with a tape or calipers, not guesses. The formula for the front foot adjustment is roughly: front correction equals the average rim reading minus the average face reading, multiplied by the ratio of the indicator span to the coupling radius, then adjusted by the geometric proportions of your machine base. The rear foot uses a similar formula that includes the same rim and face terms plus an additional multiplier based on the foot spacing. I use a custom spreadsheet now instead of doing it by hand. The equations are:
Front foot correction = (Rim_avg × F/R) - Face_avg × (B/F) Rear foot correction = Front correction + Face_avg × (C/F) These assume your indicators are placed directly at the coupling and your machine feet are measured from the same reference line. If your bridge spans across a longer distance or your indicators are offset from the coupling, you need to adjust those ratios accordingly.
A Problem You'll Hit
Last year I was aligning a large boiler feed pump and the face indicator readings were completely inconsistent between rotations. I'd zero at twelve, rotate to three, get a reading, rotate back to twelve, and the zero had drifted by two thousandths. The indicator itself was the problem — the plunger had slight play in its housing. Cheap indicator. Swapped it for a quality Snap-on gauge and the readings stabilized immediately. Always verify your tools before blaming the alignment. Another thing that catches people out: thermal growth. The formulas above get you to cold alignment. If your pump operates at 250 degrees Fahrenheit and your motor runs cooler, the pump will grow differently than the motor. I once aligned a unit to perfect cold specs and when it reached operating temperature, the coupling guards wouldn't even slide on because the thermal growth had pushed the shafts out of tolerance by twelve thousandths. The fix was to intentionally misalign cold by about six thousandths in the opposite direction, based on measured thermal growth data from similar units running at the same duty point.
Soft Foot Checks Matter
Before you even think about Gallois calculations, check soft foot. Put a dial indicator against each machine foot while it's seated on its shim, then loosen that foot's holding bolt. If the indicator moves more than two thousandths, you have a soft foot problem. Shim it out, retighten, and recheck. Do this for all four feet. Skipping this step means your alignment numbers are wrong regardless of how precisely you apply the formulas. The Gallois method assumes your machine sits on a rigid, flat baseplate. If you're aligning directly on a concrete slab with adjustable sole plates, the flexibility in the mounting system can absorb some of the corrections you calculate. You'll get close, but you may need a second pass after the machine has settled. Also, on very long shaft runs — say, a turbine driving a generator through a flexible coupling with a span exceeding six feet — the method works but you need to account for the additional deflection in the shafts themselves. The calculations still apply, but the tolerances shift and you should consult the manufacturer's alignment specifications rather than relying on generic gallois formulas. Digital alignment systems like those from SKF or Fluke make this whole process faster because they handle the math automatically. But the underlying principle is still the Gallois method. Understanding the manual approach means you can verify what the machine is telling you and catch errors when the sensor data looks suspicious.

Final Practical Notes
Always do a final verification rotation after making adjustments. Run the shafts through a full 360 degrees and confirm your readings haven't shifted. If they have, something is moving — loose bolts, shifting shims, or a bridge that wasn't seated properly. Recheck everything before you consider the job done. Record your final cold alignment numbers and note the operating temperature of the equipment. Next time you pull the coupling for maintenance, you'll have a baseline to compare against. That's how you catch problems early instead of discovering them after a bearing fails three months later.