What AOI Logic Analysis Actually Looks Like on the Floor
AOI logic analysis is the part of automated optical inspection that takes raw image data and turns it into a go/no-go decision. You capture a solder joint, a component placement, or a PCB trace, run it through the system's classification engine, and get a result. That sounds simple until you're staring at a board that the machine flagged as suspect, and it's not immediately obvious whether the flag is real or noise. I spent a few years calibrating AOI systems for mixed-signal boards, and the logic analysis side is where most of the headaches live. The hardware gets most of the attention during setup, but the logic tuning is what separates a system that catches actual defects from one that throws false calls all day and eventually gets reclassified as a "maintenance issue" by production.
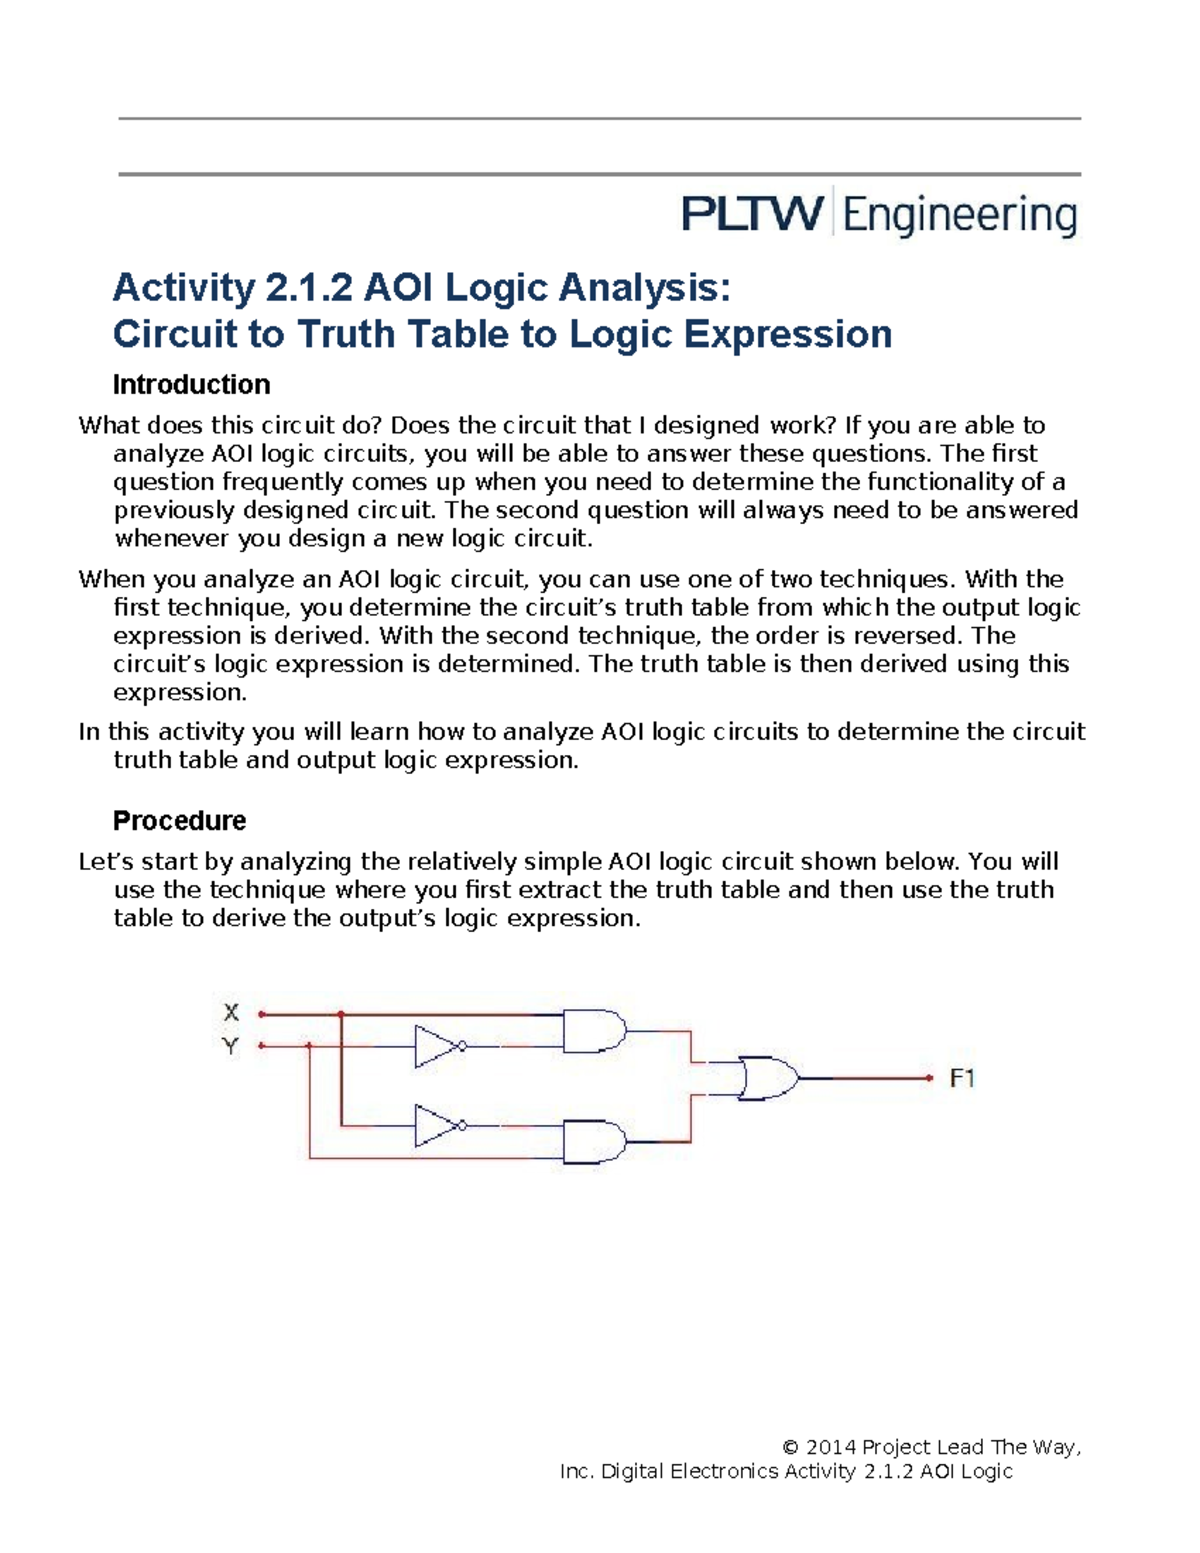
Activity 212 Aoi Logic Analysis
When I refer to Activity 212 Aoi Logic Analysis, I'm talking about the structured approach to interpreting and refining how AOI systems classify inspection results. It's not a single product name — it's a methodology that teams use when they need to systematically work through false call reduction, defect classification accuracy, and logic parameter tuning. Different shops call it different things, but the practice is consistent across the industry. The core workflow runs like this. You pull a sample set of boards — somewhere between 50 and 200 units depending on your production volume and defect rate. You run them through the AOI system at full inspection speed. Then you go through every flagged location manually, classifying each one as a true defect, a false call, or an inconclusive result that needs a second look. That manual classification is the ground truth you build your logic adjustments around. Most people stop there and accept the numbers. The next step — the part that actually moves the needle — is analyzing the failure modes. You look at which categories of defects are being missed and which non-defects are being caught. Solder bridges on fine-pitch components tend to show up consistently because the geometry is distinct. But paste deficiency under a BGA can be nearly invisible to optical inspection unless you're using 3D AOI with proper lighting angles. That gap between what the camera sees and what actually matters is where the logic tuning happens.
I worked on a project last year where our initial AOI pass rate was sitting at about 82% after we accounted for manual re-inspection. The problem wasn't the optics — the system had good resolution and stable illumination. The problem was that the logic parameters were tuned too aggressively on sensitivity for the paste deposit inspection zone. Every slight variation in board surface texture or solder mask shade triggered a false call. We spent three days adjusting the zone thresholds and the classification confidence levels, and the effective pass rate climbed to roughly 96% with no increase in escaped defects. That was a realistic improvement for that particular line. One thing that catches people off guard is that logic analysis isn't a one-time setup task. You have to revisit it whenever you change materials, switch component suppliers, or move to a different board design. I learned this the hard way when we introduced a new solder paste from a different manufacturer. The chemistry changed the reflectivity slightly, and suddenly our false call rate on paste deposit inspection jumped from about 4% to 18%. The system was still functioning within its specified parameters — it had just been calibrated for a material that was no longer in use. Here's another counter-intuitive point that most beginners miss. Tightening your logic to reduce false calls doesn't automatically improve defect detection. In fact, it often does the opposite. When you raise the sensitivity threshold to eliminate noise, you also start letting small but real defects slip through. The trade-off is real and measurable. You can plot it — it's essentially a receiver operating characteristic curve, just like in any classification problem. There's a point of diminishing returns where further tuning only shifts the balance between false calls and missed defects without improving overall quality.
Get the Full Details

The practical workaround for that is to use a tiered logic approach instead of a single threshold. Run a first-pass scan with moderate sensitivity to catch the obvious problems, then route suspicious areas to a second-pass inspection with higher resolution and more conservative thresholds. This is built into most modern AOI platforms, but a lot of teams don't configure it properly because the default settings are adequate for basic compliance testing, not for actual production quality control. If you're starting with Activity 212 Aoi Logic Analysis on a new line, here's the sequence I'd recommend based on what's actually worked for me. Start with the manufacturer's baseline configuration and run a panel of representative boards. Don't adjust anything yet. Just collect the data. Document the false call rate by category, document the escape rate if you have any known defects on your sample set, and note which inspection zones are generating the most issues. That baseline tells you where you stand before you start making changes. Then work through each inspection zone individually. Solder paste inspection first, because that's the highest-volume check and the one most sensitive to material and process variations. Component placement next, since misalignment and tombstoning are geometrically straightforward for the system to detect. Then solder joint inspection for through-hole and leaded components, which tends to be the most inconsistent area due to the variety of joint shapes and materials involved. Finally, board-level checks like silk screen presence and gross damage.
Each zone has its own set of parameters — thresholds, comparison windows, classification weights, and confidence levels. Changing one parameter often affects multiple zones because the inspection programs share some of the same image processing pipelines. I've seen engineers adjust a threshold in one area and wonder why the false call rate in an unrelated zone spiked ten minutes later. The system isn't broken. The zones are coupled through the common image processing chain. Documentation matters more than most teams realize. Every parameter change, every date, every board revision, and every material lot change should be logged. Six months from now when your false call rate mysteriously climbs again, you'll want a paper trail that shows you changed the solder paste supplier on March 12th and that the tuning for Zone 3 hasn't been revisited since February. Without that record, you're guessing instead of troubleshooting. There are tools that help with this. Most AOI manufacturers provide their own analysis software — KLA, Koh Young, Omron, — and they all include report generation and trend tracking features. Third-party options exist too, but they're usually overkill for small shops and underkill for high-volume operations. The built-in tools are sufficient if you actually use them instead of letting the reports pile up unread.
One scenario where AOI logic analysis simply cannot help you: concealed defects. Things like internal delamination, subsurface cracks in multilayer boards, or voiding inside solder joints under BGA packages. Optical inspection can't see through materials. No amount of logic tuning will fix that limitation. If your product requires that level of inspection, you need X-ray or ultrasonic testing, not better AOI parameters. I've seen teams waste weeks trying to tune AOI to catch something the physics of the technology can't detect. The bottom line is that Activity 212 Aoi Logic Analysis is a disciplined process of data collection, classification, parameter adjustment, and verification. It's not glamorous. It doesn't make the news. But the teams that do it well consistently outperform the ones that treat AOI as a black box and hope the machine handles everything. The machine handles the inspection. You handle the logic.