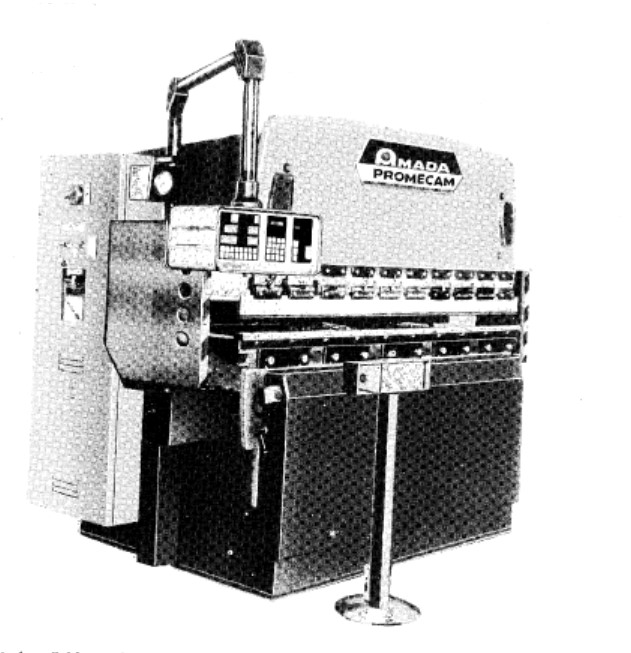
Getting Started With the Amada Promecam Press Brake Controller
The Aplus 5 and Aplus 7 controllers are what most people are running on their Amada Promecam press brakes these days. They're decent machines but they have quirks that aren't obvious unless you've actually spent time with them. I've been working with these for years, mostly on 100-ton and 200-ton capacity machines, and the manual covers the basics but leaves a lot of practical gaps. Let me fill those in. The manual itself is split into several sections. You've got the hardware overview, the software interface walkthrough, the bend calculation engine documentation, and then the maintenance schedules. Most operators only read the first two sections and skip the rest, which is a mistake. The bend calculation section is where you'll find things like the K-factor defaults and how the Y1/Y2 axis compensation actually works under different material conditions. The interface uses a windowed layout similar to older Windows applications. Don't let that throw you. It's not ancient technology, it's just deliberately conservative. The screen is divided into bend sequence lists, axis readouts, and a numeric keypad area. Everything is touch-capable but I've found that a stylus or even just a clean fingertip works better than trying to use greasy operator gloves.
One thing the manual doesn't make clear enough: the default bend tables are calibrated for mild steel at about 20 degrees Celsius ambient temperature. If you're bending cold-formed steel or working in a shop that drops below fifteen degrees in winter, your angle accuracy will drift by roughly half a degree per ten-degree temperature shift. That might sound small until you're doing precision aerospace brackets and your second piece comes out wrong. I ran into a specific issue last year with an Aplus 7 controller on a PB200-3 machine. We were running a high-volume job for a fabrication shop, about four hundred identical bends across three different sheet thicknesses. After about seventy-five parts, the backgauge fingers started producing angles that were consistently two degrees off on the last station of the sequence. Nothing in the alarm logs. No error codes. The machine thought everything was fine. The problem turned out to be thermal drift in the linear scale sensor on the Y2 axis. The controller compensates for this in its standard routine, but the compensation table only updates every three hundred seconds. On a fast cycle job with twenty-second bends, that meant the machine was running with outdated correction data for most of the shift. I ended up adding a manual zero-point calibration on both Y axes between each material thickness change. It added about forty seconds per changeover but kept us within tolerances for the rest of the run. The fix worked and we finished the order without a single customer complaint about angles.
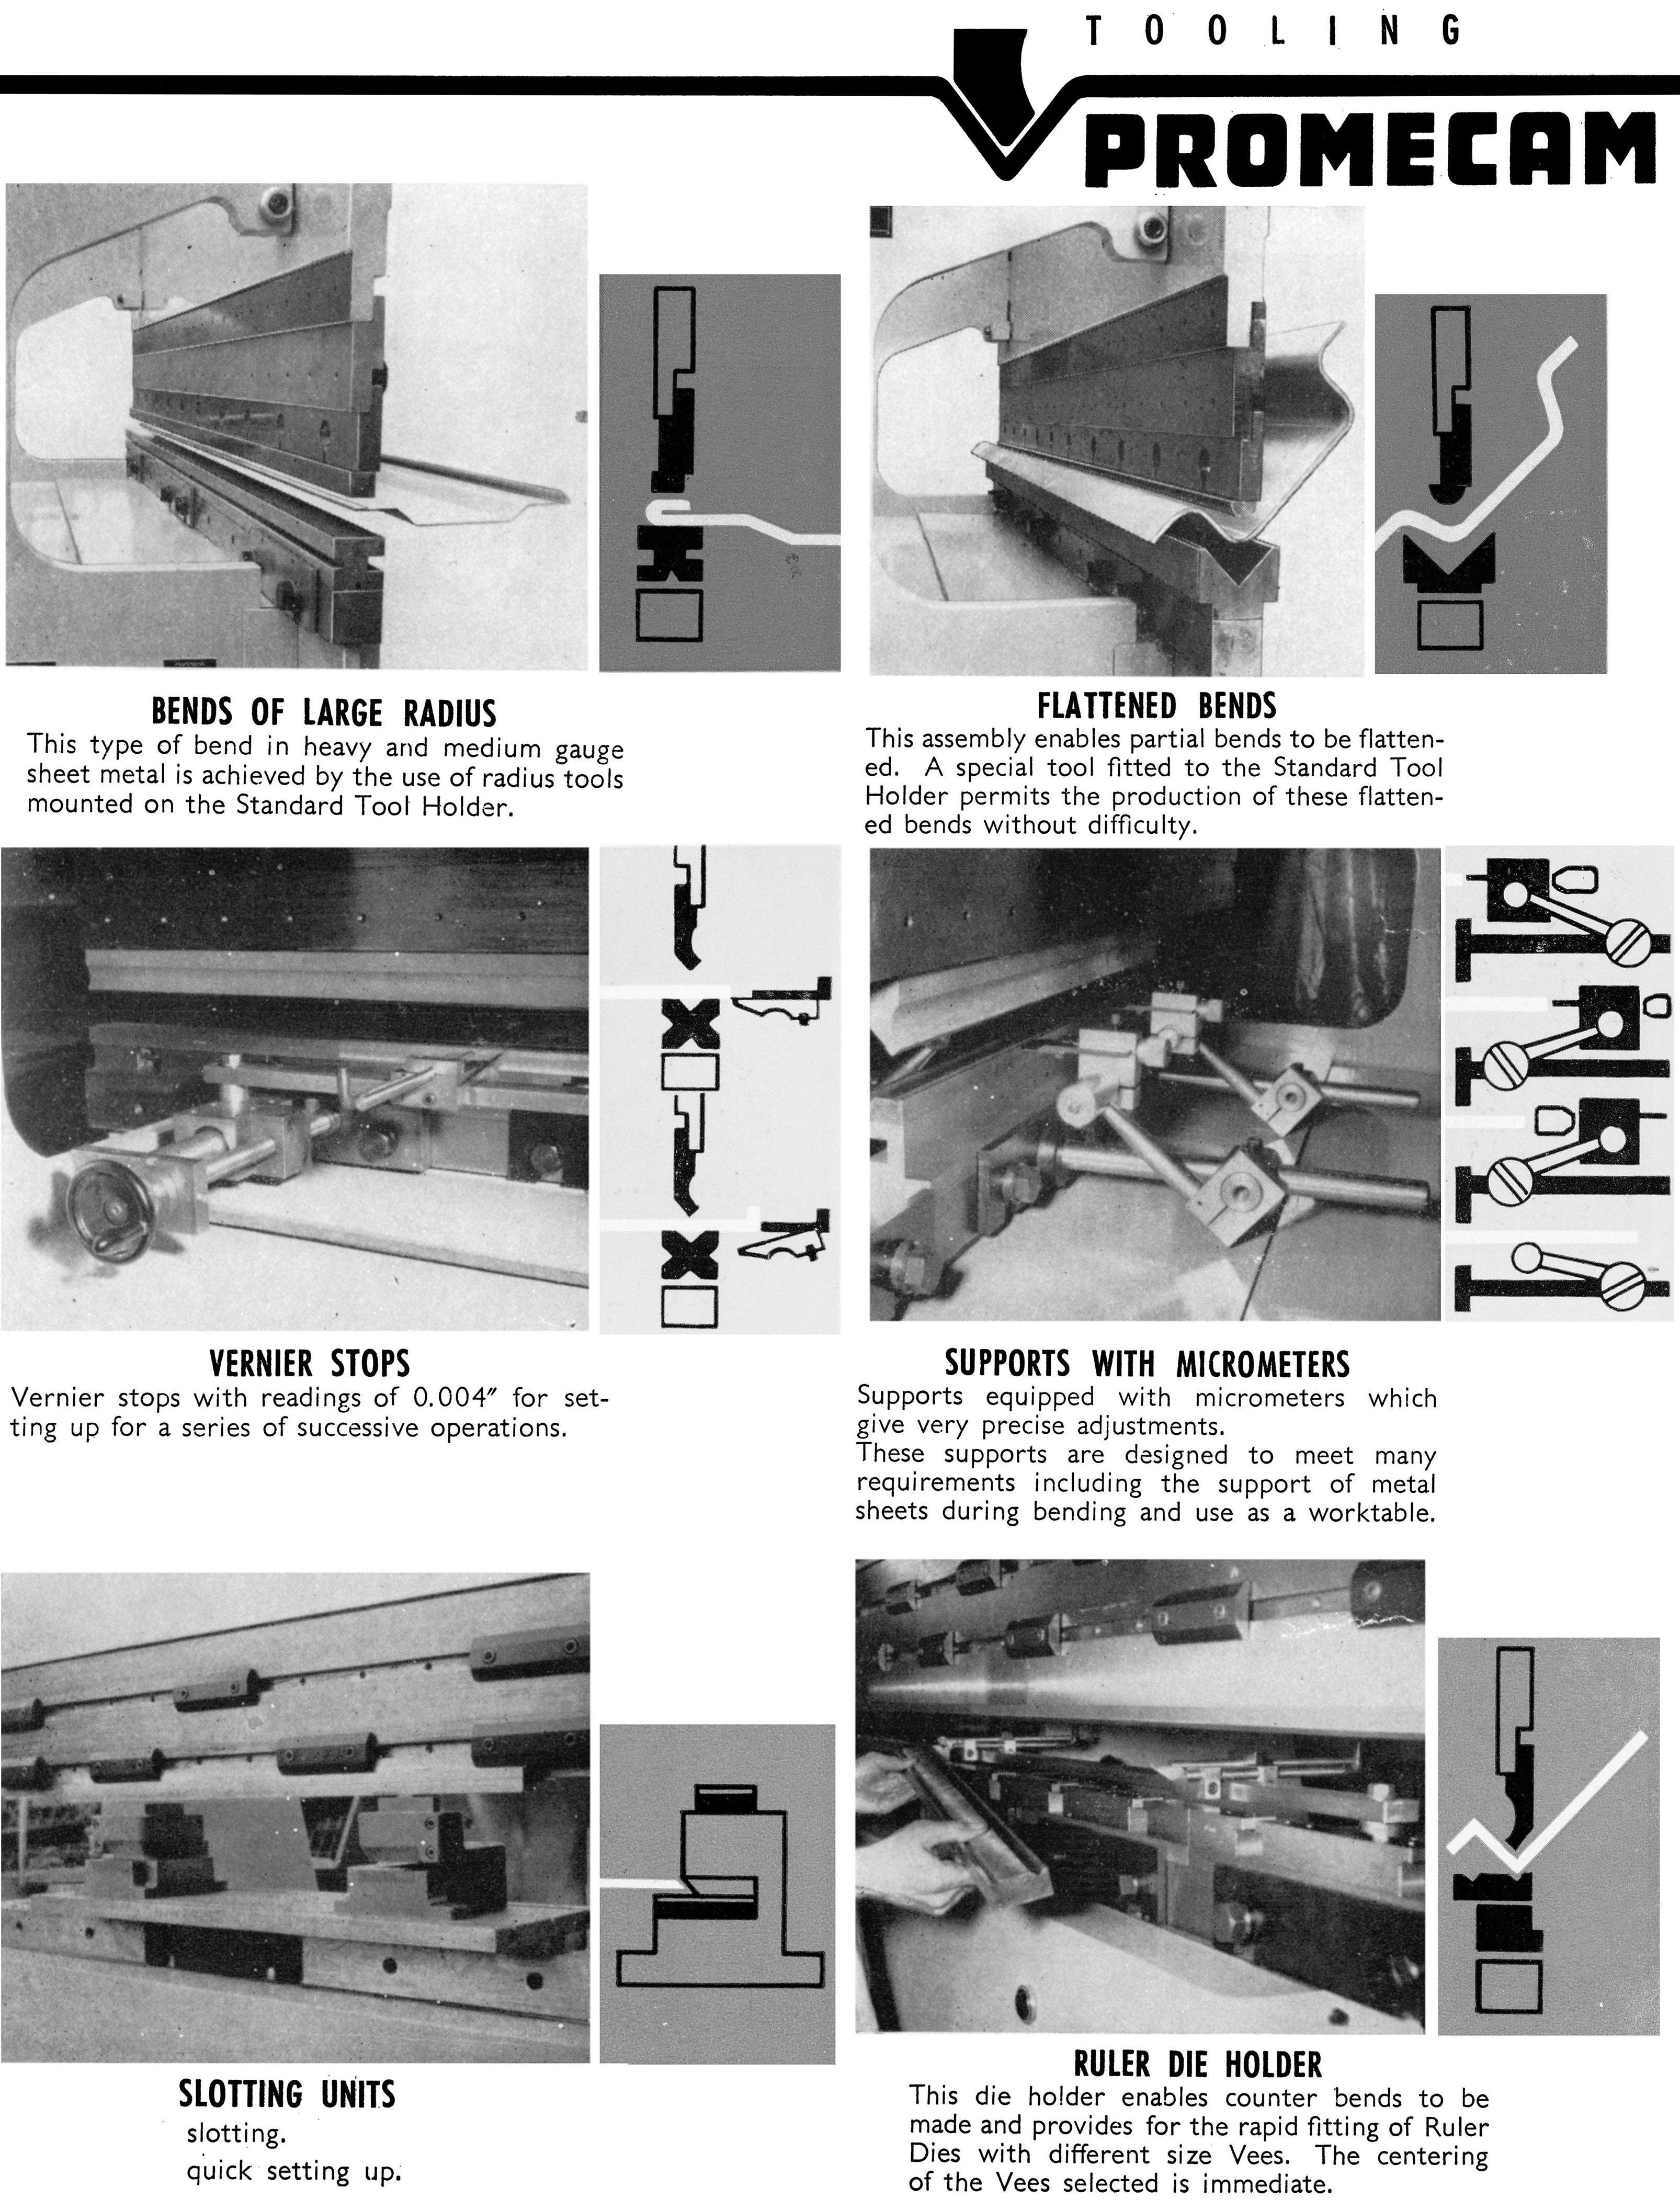
Here's something nobody tells you about the bend calculation engine: the V-die opening selection isn't as straightforward as the old rule of thumb suggesting eight times the material thickness. On the Promecam controllers, the built-in calculation uses a modified formula that accounts for springback differently depending on whether you're doing bottom bending or air bending. The manual mentions this briefly but doesn't show you the actual equations. For mild steel in air bending, the controller tends to underestimate springback on materials over three millimeters thick by about twelve to fifteen percent if you're using a standard 80-degree V-die. I usually add a couple degrees of overbend manually in those cases rather than trying to fight the algorithm. The tooling library is another area where experience matters more than the documentation. You can import your own tooling profiles through the service menu, which requires a password most operators don't have. If you're ordering replacement tooling from Amada, make sure you give them the exact drawing number and ask them to encode it into your machine's database during installation. Generic entries often lack the correct radius parameters, which throws off your tonnage calculations and can lead to tool failure if you're pushing near the machine's rated capacity. Programming a bend sequence follows a logical progression but there are shortcuts worth knowing. You can define a bend sequence using either the absolute position method or the incremental method. Absolute is more forgiving for beginners because you're telling the machine exactly where each backgauge position should be. Incremental is faster once you know what you're doing but a single typo in the offset value can send your part completely off-spec. I recommend starting with absolute positioning until you've done at least fifty bends on the same machine model.
Get the Full Details
The angle correction feature is probably the most useful tool on this controller and also the most underutilized. After making a test bend, you can enter the measured angle and the machine will automatically adjust the ram depth for subsequent parts. The correction is applied to both Y axes independently, which matters because any misalignment between Y1 and Y2 will show up as a twist in the final part. I always verify the correction by measuring with a protractor gauge before committing to full production, especially on thicker materials where the springback curve isn't linear. Backgauge positioning has its own set of complications. The standard BG1 through BG4 axes are servo-controlled and generally accurate to within plus or minus zero point zero five millimeters. But the R-axis on the backgauge fingers, which controls the tilt of the fingers themselves, can develop play over time. On my machines, I check the R-axis backlash quarterly. If you notice your bent flanges aren't parallel to each other even though the bend angle checks out, the R-axis is usually the culprit. A simple shim adjustment under the finger support brackets fixes most cases. When it comes to material selection in the software, don't just pick "mild steel" and move on. The controller has separate entries for low-carbon steel, high-strength low-alloy steel, stainless, aluminum, and copper. Each material has a different modulus of elasticity value baked into the bend calculation. If you're running HSLA steel but have mild steel selected, your bend angle will be consistently shallow because the controller is calculating for a softer material. Always double-check the material selection before hitting cycle start. I've made this mistake more times than I care to admit, especially during setup changes.
The manual also covers hydraulic system maintenance but it's pretty generic. What it doesn't mention is that the oil temperature sensor on the Aplus systems can give false readings if it's not cleaned regularly. I've had situations where the machine thought the hydraulic fluid was overheating and would shut down mid-cycle. Turns out the sensor just had metal chips caked onto it from nearby grinding operations. Wiping it down with a lint-free cloth and some isopropyl alcohol resolved it immediately. Schedule this check every time you change hydraulic fluid, which should be roughly every two thousand operating hours. For downloading reference materials, the official Amada Promecam manual is available through their dealer network. Your local distributor should have access to the latest firmware revision documentation as well. Sometimes the online versions are outdated compared to what your machine is actually running, so always cross-reference the revision number printed on the controller's main screen with whatever document you're reading. Mismatches between firmware version and manual content are surprisingly common and can lead to confusion when menu options don't match what's described in the documentation. If you're working with older Aplus 5 units, be aware that the flash memory modules used for program storage degrade over time. I've seen controllers lose saved bend programs after about eight years of normal operation. Always keep a backup of your most frequently used programs on an external USB drive or your shop's network. The manual mentions backup procedures but the warning about memory degradation comes from actual field experience, not from the documentation itself.
The tool length measurement feature is another area where people tend to overcomplicate things. You can measure tooling manually by lowering the ram until the punch contacts the die and recording the position. This takes about three minutes per tool set but gives you accurate compensation values. Automated measurement exists on newer firmware revisions but it's slower and more prone to errors if your tooling surfaces aren't perfectly clean. I prefer the manual method because it forces you to inspect the tooling contact surfaces at the same time, and I've caught chipped punches and worn die corners this way that would have caused problems later in the production run. One final note about the safety interlocks. The controller monitors guard status, light curtain integrity, and two-hand control operation. If you bypass any of these for any reason, you're not just violating safety regulations, you're also risking damage to the machine. I had a shop where an operator kept tripping the light curtain because the reflectors were dirty. Instead of cleaning them, someone patched the sensor wire. The machine ran fine for three months until the patch failed during a high-tonnage bend and the ram came down with the backgauge still in position. The repair bill was about eight thousand dollars and it took two weeks to get the replacement components. Just clean the reflectors every morning. It takes thirty seconds.