API 571 Second Edition — what it actually is and how people misuse it
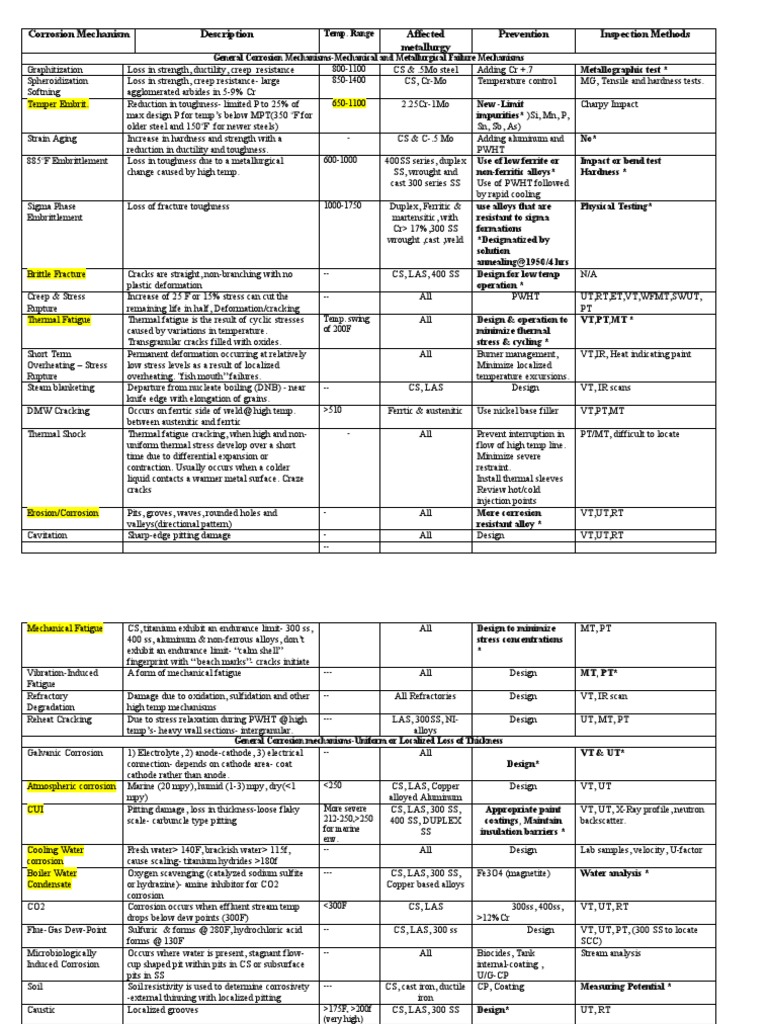
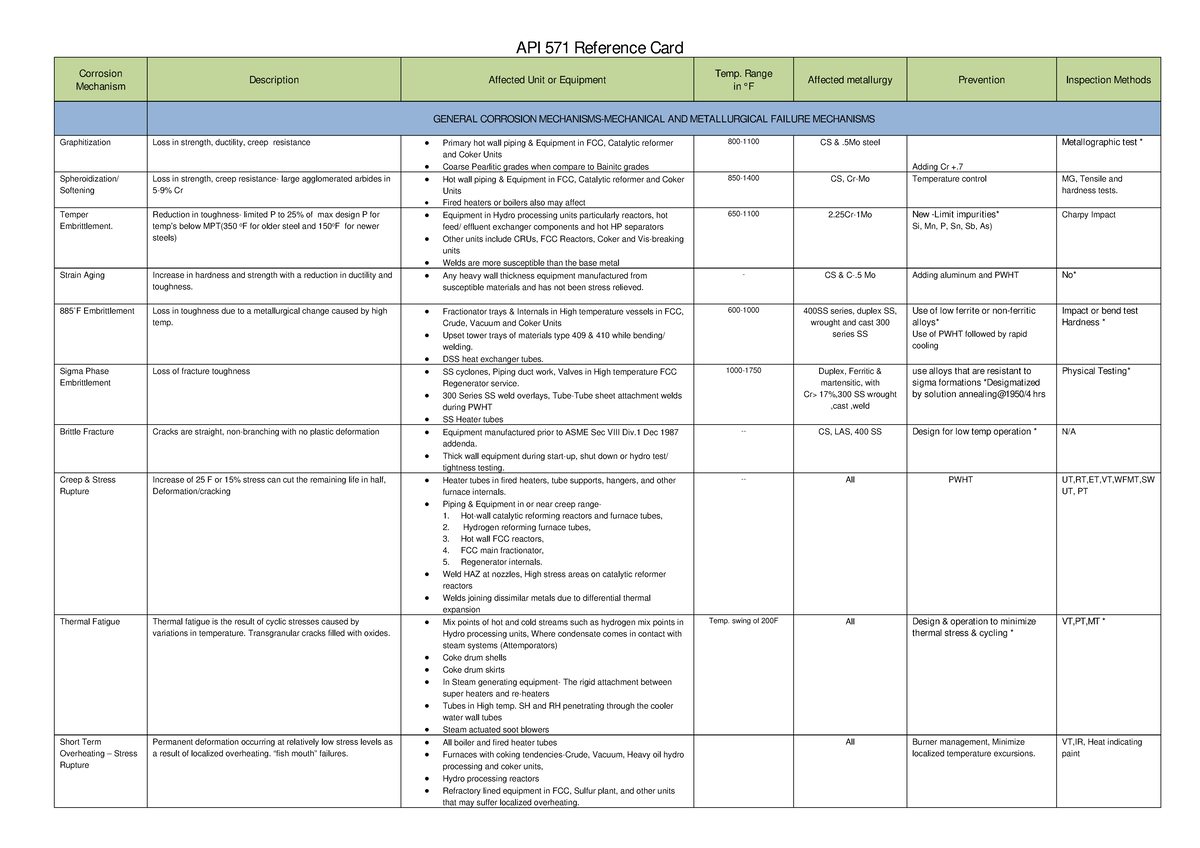
API 571, full title "Damage Mechanisms Affecting Fixed Pressure Widely Operated Plants," second edition, published April 2011, is essentially a reference catalog. It describes the failure modes you see in refineries, petrochemical plants, and similar facilities — creep, fatigue, corrosion under insulation, brittle fracture, sour water corrosion, and so on. It does not tell you how to run your inspection program. It tells you what a damage mechanism looks like, where it tends to appear, and what mitigation looks like in practice. The only legal copy sits on the API website. It is a paid standard, not free PDF material. If you see it offered as a free download on some random site, that is a copyright violation and a quality risk — edited versions, truncated pages, and misnumbered sections circulate constantly. Buy it direct from api.org or through an authorized reseller. The price is steep, but the alternative is building a risk assessment on a text you did not read end to end. Most engineers treat API 571 like a textbook. They do not. The standard is designed to be used alongside API 570 (inspection) and API 579 (fitness for service). The three documents form a sequence: API 571 identifies the mechanism, API 570 tells you where and how often to inspect, and API 579 evaluates whether the damage found is acceptable. Jumping straight to API 579 without walking API 571 first is where people miss subtleties and produce evaluations that look sound but are built on incomplete assumptions.
The practical workflow goes like this.
- Step 1: Pull your process design data. Temperature, pressure, fluid composition, carbon content, weld procedure history. None of this is in API 571. You bring it to the table.
- Step 2: Match the service conditions to a damage mechanism. API 571 gives you tables and flowcharts. The Nadeau diagram for graphitic corrosion, the Temper Embrittlement curves, the CUI temperature range. Use them, but verify your material grade and heat treatment against the actual MTRs, not the generic tables.
- Step 3: Confirm susceptibility. A stainless steel vessel operating at 350°C in a dry H2S environment looks fine on paper. Your mill certs show 0.04% sulfur. That pushes you into stress corrosion cracking territory the moment moisture shows up. API 571 flags this. Most people stop reading at the heading.
- Step 4: Set inspection points. This is where API 570 takes over, but API 571 gives you the recommended locations. Flange faces, weld heat-affected zones, downstream of stream diverts, areas with known impingement.
- Step 5: Evaluate using API 579 when needed.
I ran into this last year on a hydrocracker outlet header. The spec said 2¼Cr-1Mo, operating at 420°C. The Nadeau diagram in API 571 suggested minimal creep risk at that temperature. The actual MTR showed the material was on the low end of the carbon range and the service had seen two upset runs where temperature spiked above 450°C for roughly 80 hours each. API 571 does not explicitly address short-term excursions in its main charts, so I cross-referenced the creep rupture data from the material supplier and applied a cumulative damage factor using Miner's rule. That pushed the remaining life estimate down by about 30 percent compared to a straight reading of the diagram. The original inspection plan from the previous turn-around had not accounted for it. People quote API 571 without checking the revision date. The second edition from 2011 superseded the first, but some plants still pull old copies from their document management systems. The differences between editions are not trivial. The CUI section got substantially expanded, the temper embrittlement guidance was refined, and several damage mechanisms received new metallurgical context. Using the first edition for a current risk assessment means you are missing updates that reflect real field failures from the past decade. Another mistake: treating API 571 as a decision tree with a single correct answer. It is not. Several mechanisms overlap. High-temperature hydrogen attack and temper embrittlement can coexist in the same vessel if the thermal history supports both. The standard acknowledges this but does not give a prioritization algorithm. You have to do the engineering judgment yourself, which is why the document keeps saying "consult the inspector" and "use engineering assessment." That is not bureaucratic filler.
Get the Full Details

A third one worth mentioning: the assumption that API 571 covers every corrosion mechanism in your plant. It does not. It covers the widely observed ones. Custom solvent units, unusual feedstocks, niche catalytic processes — those can introduce damage modes not in the standard. I worked a unit where chlorides from a non-standard feed caused intergranular stress corrosion cracking in 321 stainless at temperatures well below the usual 60°C threshold. API 571's SCCE section gave the general guidance but not that specific scenario. The workaround was pulling literature from NACE/AMPP proceedings and correlating it with metallurgical lab results.
What API 571 does not do
It does not give inspection intervals. That is API 570. It does not give acceptance criteria for flaws. That is API 579. It does not tell you how to write a procedures manual. It describes mechanisms. If you need actionable inspection or evaluation guidance, you must pair it with those other documents. Using API 571 alone for anything operational is incomplete by design. It also does not address mechanical damage, external fire exposure, or earthquake effects. Those fall outside the scope. Some engineers try to stretch it to cover impact damage on carbon steel, and while the general principles of brittle fracture discussion can be loosely applied, the standard was written for pressure equipment damage from service conditions, not physical abuse. Keep the scope clean.
Practical tip on using the tables
The tables in API 571 are dense. The Mitigation and Control table for each mechanism is the part people skip, but it is often the most useful section. It lists what actually works in the field versus what is theoretical. For example, the table for SO corrosion of refractories recommends aluminum-containing castables and proper sealant application. It does not say "use alumina refractory" because that is a different problem. Read the mitigation column carefully before you specify a control method. When I do damage mechanism reviews now, I print the relevant sections, highlight the susceptibility criteria, and cross-reference with the actual operating logs. A lot of the mechanistic descriptions are accurate but generic. The real value comes from matching the description to your specific temperature profiles, startups, shutdowns, and feedstock changes. That matching step is where experience matters more than the document itself.
Final note on scope and limitations
API 571 is a reference standard, not a procedure. It will not solve your problem if your baseline data is wrong. If your material certifications are missing, if your operating history is incomplete, or if your inspection records go back only one turn-around, API 571 cannot fill those gaps. It describes what can go wrong. It cannot tell you what is wrong with your specific equipment without good input data. The standard is only as useful as the information you bring to it.