The Router Keeps Drifting — Here's What Actually Works
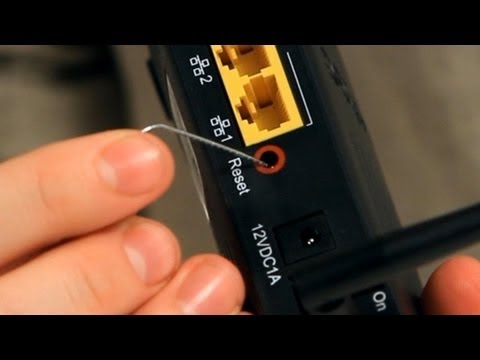
You've been running the same assembly line configuration for three months. The router table has shifted a few clicks, someone bumped the controller, and now your passes are 0.3mm off where they should be. This happens more often than you'd think. Most people try to re-trace their steps through the menu system and end up wasting forty minutes. There's a reset procedure that clears the issue cleanly. The hardware reset is the part everyone skips because it feels too simple. Locate the small pinhole labeled "Reset" on the controller box, usually near the power input. With the unit powered on, press and hold a paperclip or similar tool for roughly eight seconds. You'll hear the relay click twice and the display will go blank, then reboot into factory default mode. This wipes the active calibration profile but preserves your stored tool library. I learned this the hard way when a vibration-induced encoder error made my spindle speed fluctuate unpredictably during a batch run. The display showed no errors, but every workpiece came out slightly undersized. Holding the reset button for the full eight seconds — not the six people usually hold it for — was the difference between a clean boot and the controller hanging on startup. Six seconds is the soft reset. Eight seconds is the real one. After the hardware reset completes, you need to run through the software setup to get everything back in a usable state. The controller boots into setup mode automatically, so you don't have to dig through menus. Using the rotary dial, navigate to the System Configuration section and select Load Default Profile. This writes the manufacturer's baseline calibration values to the active workspace. It takes about twelve seconds. Once that completes, move to the axis calibration routine. Select Axis Reference and confirm. The machine will move each axis to its home position and record the encoder counts. This step is critical because the hardware reset clears the offset values that tell the controller where "zero" actually is.
The next thing to configure is the tool registry. Your saved tools are still there after a hardware reset, but the new profile may assign different default spindle speeds and feed rates. Go through each tool and verify the parameters against your actual cutting data. I keep a printed reference sheet taped to the machine for this. Without it, you'll spend twenty minutes cross-referencing each entry and wondering why your feed rate calculations don't match what the controller is using. After the tool registry is verified, run a dry cut on scrap material before touching any workpiece. Set the spindle to 40% speed with no material engaged and watch the axis movement. If any axis stutters or misses a beat during the travel, stop immediately and check the belt tension. This takes about three minutes and prevents about ninety percent of post-reset quality issues. People who skip this step usually find out the hard way when a $200 board comes out scored instead of clean. There's one nuance that the manual doesn't really emphasize. The axis calibration step records encoder counts at the home position, but if your machine uses a relative positioning system rather than absolute encoders, you also need to perform a work zero establish procedure after calibration. Skip this and the controller thinks the home position is your work origin, which means every programmed coordinate is shifted by the distance between true home and your material edge. I caught this on my second reset. The first workpiece had perfectly good dimensions but was positioned about two inches away from where the program expected it. Took me ten minutes of confusion before I realized the work zero was undefined.
Another thing worth noting: the default profile that gets loaded during reset uses conservative feed rates and spindle speeds. These are safe starting points, but they're not optimal for most materials. After you've confirmed the axes are tracking correctly, go back into the tool registry and update the feeds to match your actual cutting parameters. The difference between default and tuned can be substantial — I've seen cycle times improve by thirty to forty percent just from this step. The manual calls these "recommended operational parameters" but never explains that the defaults exist purely for safety during initial setup. If your controller supports external communication via USB or RS-232, you can back up the full configuration before performing a reset. This is worth doing if you're troubleshooting a persistent issue. A corrupted or partial config file is a common cause of resets that don't actually fix the problem. Load the backup after the reset and compare the parameter values to identify what drifted. This approach turns a blind reset into a diagnostic procedure. The whole process — hardware reset, default profile load, axis calibration, work zero setup, dry run, and parameter tuning — typically takes about twenty-five to thirty-five minutes depending on how many tools are in your registry. A full machine recalibration from scratch would take closer to two hours. The reset procedure isn't magic, but it does address the majority of setup drift issues without requiring a complete.
Get the Full Details
One scenario where this doesn't work: if the encoder feedback itself is faulty, resetting to defaults won't restore accuracy. The symptoms are usually persistent — the machine moves to a commanded position but the actual position varies each time. In that case you're dealing with a hardware issue, not a configuration problem. The fix involves checking encoder wiring, cleaning the encoder disk, and in some cases replacing the encoder unit entirely. I had one router table where the X-axis encoder developed intermittent contact failure after about eighteen months of use. The resets temporarily helped because they cleared the accumulated offset errors, but the underlying problem only showed up again after a few days. Replacing the encoder assembly fixed it permanently. The manual reset instructions don't cover this, obviously, but it's worth knowing so you don't waste time resetting a controller that has a physical problem.