Understanding Automated Bar Measurement in Machining Operations
When you are running CNC lathes or turning centers with bar feeders, the measurement cycle is where most people lose time and scrap material. I have spent years troubleshooting why parts come out consistently out of tolerance on the second operation, and it almost always traces back to how the machine handles measurement data. The core concept is straightforward enough in theory. The machine probes or measures a feature on the workpiece, compares that reading against the programmed dimension, and automatically adjusts the tool offset to compensate for wear or thermal drift. But the practice is messier than any textbook makes it sound. I ran into this exact problem last year on a batch of 340 parts for an automotive client where our diameter was drifting by 0.02mm every 50 pieces. The machine had probing enabled, but the offsets were not being applied to the correct coordinate system, so every correction was happening on paper instead of in reality. The fix was mapping the probe routine to the G54 work offset rather than the machine coordinate system, which took about twenty minutes and saved us from scrapping the entire run.
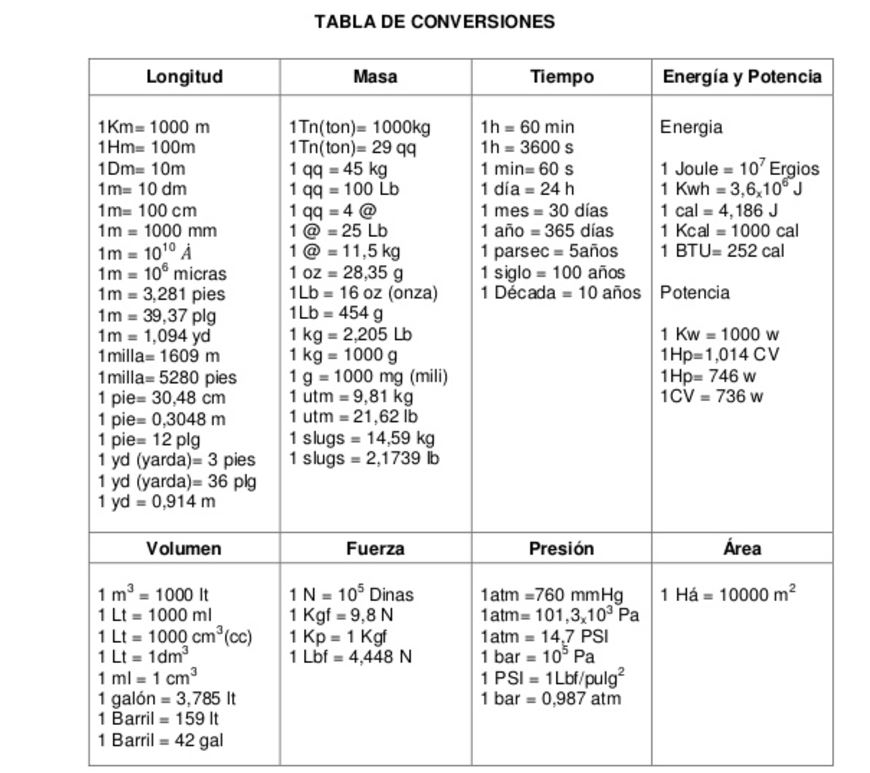
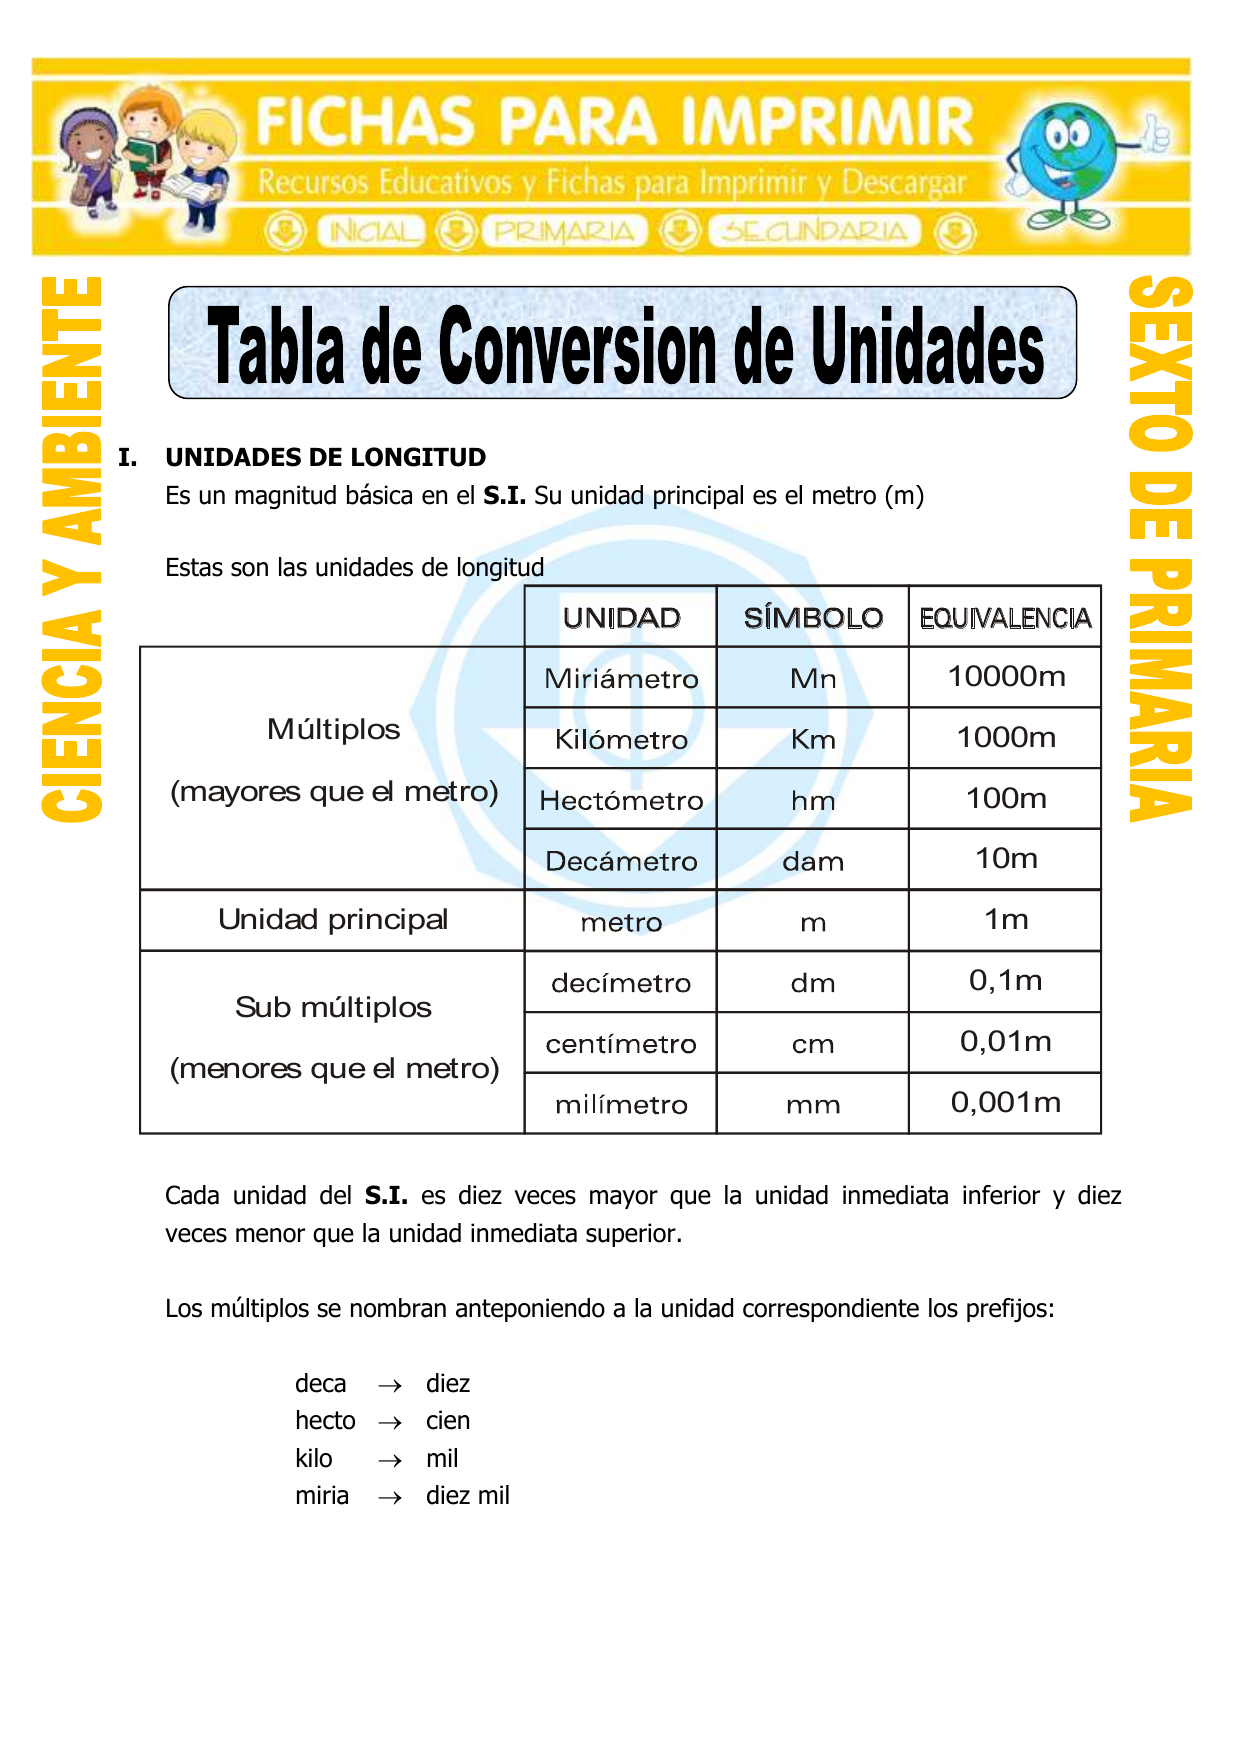
Autobaremacion Ejemplo Unidad De Medida
Here is a practical example using metric units on a typical CNC turning center with a probing cycle. Say you are machining a shaft with a target diameter of 25.400mm using a digital probe like a Renishaw A5003 or equivalent. Your part program calls a probe cycle before the final finishing pass. The probe touches the workpiece at three points around the circumference, averages them to account for out-of-roundness, and returns a measured value of 25.412mm. That is 0.012mm oversize. The control system should then adjust the wear offset for that tool by subtracting 0.012mm from the current tool diameter offset. Most operators miss a detail here. The probe does not just measure diameter, it also catches concentricity errors. If your raw bar stock is bent or poorly centered in the chuck, a single probe touch will give you a reading that looks correct but masks a true eccentricity problem. I learned this the hard way on a job where our first article measurements were within spec, but the second article was consistently out by 0.05mm. The part was not actually undersized. The bar stock had about 0.03mm bend, and the probe was compensating for the high side while ignoring the low side of the rotation. The workaround was adding a rough probe check after the stock was centered but before any cutting began, then comparing the probed rough profile against expected stock dimensions to flag a bar before we wasted time and tools on it. Another counter-intuitive point that beginners consistently overlook is thermal growth compensation. When you first power up a machine and start probing, the readings will drift for the first twenty to thirty minutes as the spindle and structural components warm up. If you establish your measurement baseline cold and then run production warm, your offset corrections will be fighting against a moving target. The best practice I found is to run a thermal warm-up cycle with the probe active, take three consecutive readings at fifteen-minute intervals, and only begin production once those readings stabilize within 0.003mm. This adds about forty minutes to your startup time but eliminates the most common source of late-night callouts from operators who thought their machine was broken when it was just cold.
The unit of measurement setting on your control is critical and often handled carelessly. If you are mixing imperial and metric programs on the same machine, a G20 versus G21 error will throw off every measurement and offset calculation instantly. I once debugged a problem where a subcontractor kept producing parts that were exactly 25.4mm instead of 1 inch on an imperial drawing. The program had a G21 in it from a previous metric setup that was never canceled. The probe readings looked perfect because they were all in millimeters, but the drawing called for inches and the operator was verifying against the wrong scale. Always double-check the active unit mode before and after any program change, regardless of how simple the program looks. One more thing worth noting about the limitations of this approach. Automated measurement and offset correction only works reliably if your process is stable. If your cutting parameters are wrong, your tool geometry is poor, or your coolant concentration is off, no amount of probing will save you. The probe corrects for variations, not for fundamental process errors. I have seen shops run probing cycles on setups that should never have been running in the first place, expecting the automatic compensation to handle bad feeds and speeds. It does not. It just keeps adjusting offsets until your tool wears out or your part dimensions bounce around too much to maintain consistency. If you are dealing with high-volume production where part variation exceeds your process capability index, the better move is investing in in-process gaging with closed-loop feedback to the CNC controller rather than relying on manual probe cycles between parts. This typically reduces measurement overhead from about three minutes per part down to under thirty seconds and gives you continuous data logging for statistical process control. But for smaller runs or job shops where full automation is not cost-effective, mastering the probe cycle and offset workflow remains the most practical approach available.
Get the Full Details