Why Your VFFS Line Keeps Stopping and What Automation Actually Solves
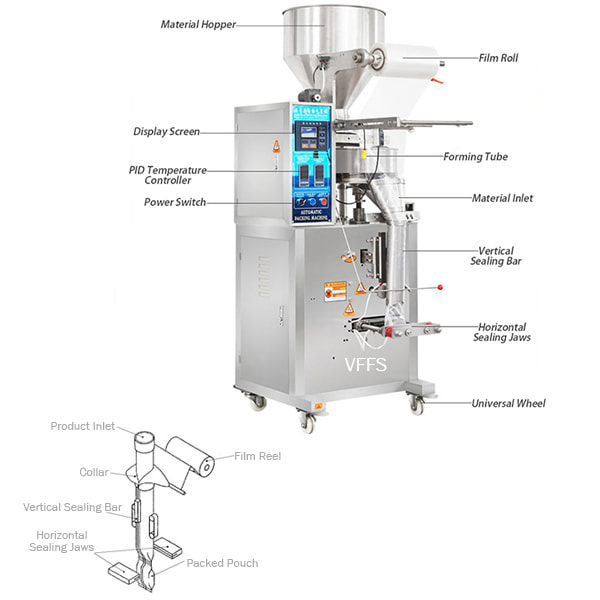
I spent three years troubleshooting a 12-station packaging line before I stopped fighting the equipment and started automating the right things. Vertical Form Fill Seal machines are the workhorses of food, pharma, and consumer goods packaging, but they are also one of the most misunderstood areas in production automation. People buy into promises of "turnkey solutions" and then wonder why their downtime didn't improve. Automation Of VFFs Machine isn't a single piece of software or one gadget you bolt on. It is a systems-level integration that touches the film handling, the forming collar, the vertical sealing jaws, the horizontal sealing and cutting station, and the product dosing system. Every one of those subsystems has its own controller, its own feedback loop, and its own failure mode. The automation layer sits above all of them and decides what happens when something goes wrong.
The Real Work: Integration Before You Touch a Single Sensor
Most people start by adding a vision system or an auto weight corrector and call it automation. That is not automation. That is sensor substitution. Real automation means the machine can detect a fault, isolate the root cause, adjust parameters within closed-loop tolerances, and resume operation without a technician holding a tablet. The first step is mapping your current signal architecture. You need to know exactly which inputs and outputs are already exposed on your PLC. Most modern VFFS controllers from manufacturers like Bosch, Ishida, and Cleverpack run on either Omron, Mitsubishi, or Beckhoff platforms, and each has a different communication stack. If you are integrating third-party equipment—bulk weighers, checkweighers, metal detectors, labelers—you need to know whether your machine speaks EtherNet/IP, Profinet, Modbus TCP, or just hardwired discrete I/O. The mismatch here is the number one reason integration projects stall. I have seen lines where the automation team added a high-speed vision inspector downstream and then wondered why the machine rejected 40 percent of good product. The issue was not the vision system. It was that the reject logic had no coordination with the film tension control upstream. When the inspector fired a reject, the machine kept pulling film at the same rate, creating a bubble that distorted the next seal. The fix was a simple handshaking protocol between the vision PLC and the VFFS main PLC that temporarily slowed the film servo during any rejection event. That cut rejections from 40 percent to 3.2 percent in two days.
How to Actually Build an Automation Layer for VFFS
Start with the process map, not the hardware catalog. Draw every step from film unwind to bag ejection. For each step, note the desired cycle time, the tolerance band, and the fault condition. This document becomes your requirements specification and the single point of truth when vendors start proposing solutions that solve problems you do not have. Film is where most automation failures begin. A VFFS machine running at 80 to 120 bags per minute requires micron-level tension consistency. Open-loop tension control using brake pads and springs will not hold within acceptable tolerance once ambient humidity changes or you switch film rolls. The automation layer must include closed-loop tension management using load cells or encoder feedback on the unwind and rewind stands, with PID loops tuned to the specific film stock you are running. I ran a project where we were switching between 80-micron laminated film and 60-micron LDPE on the same line. The original tension settings worked fine for the laminated film but the thinner LDPE kept wrinkling at the forming collar. Instead of manually retuning every time, I built a recipe system where each film type had its own tension profile, servo acceleration curve, and forming collar speed offset. The operator selects the film type from the HMI, and the PLC loads the entire profile. Changeover time went from about 25 minutes to roughly four. That is a realistic automation win, not a vendor demo win.
Get the Full Details

Forming and Sealing Geometry
The forming collar creates the bag shape before the film enters the sealing zone. If the automation system does not account for film memory—the tendency of the material to spring back after being bent around the collar—you will get inconsistent bag dimensions and seal defects. The correction is usually a combination of servo-controlled film feed length adjustment and a thermal preconditioning zone near the collar that softens the film slightly before forming. Seal temperature, pressure, and dwell time are interdependent variables. Increase seal temperature and you can reduce dwell time, but only up to the point where the film starts to degrade. The automation layer needs real-time thermocouple feedback at each sealing jaw, not just the setpoint reading from the heater controller. I learned this the hard way when a batch of products failed seal integrity testing three days after production because the thermocouple on jaw two had drifted 12 degrees Celsius from the actual jaw temperature. The display read correct. The jaws were 12 degrees cold. The seal looked fine to the naked eye but failed the peel test. After that, every automation spec I wrote included redundant RTD placement at the jaw surface, not just in the heater block.
Dosing and Filling Integration
This is where most people underestimate the complexity. A bulk weigher feeding a VFFS is not a simple "drop product when weight is reached" operation. The weigher has its own cycle time, its own reject handling, and its own communication latency. If your VFFS automation does not account for the time lag between the weigher's "ready to drop" signal and the actual product entering the tube, you will get overfills or underfills depending on the conveyor speed. The workaround I used was implementing a predictive fill trigger. Instead of reacting to the weigher signal, the VFFS PLC calculates when the product stream will reach the filling point based on belt speed and distance, then fires the fill initiation signal proactively. This is straightforward math but almost never gets implemented correctly because the distance and speed variables need continuous recalibration. A laser encoder on the product conveyor or a simple photoeye array spaced at known distances can provide the speed data. Once I added that, weight accuracy improved from ±3.5 grams to ±0.8 grams on a 200-gram product.
What Automation Cannot Fix
I need to be blunt about this because vendors will not be. Automation of a VFFS line will not compensate for poor mechanical condition. Worn forming collars, degraded sealing jaw surfaces, misaligned film guides, and stretched drive chains will cause problems that no amount of software can resolve. The automation layer can detect some of these issues through trend analysis—seal temperature requiring higher setpoints over time, for example—but it cannot repair them. Scheduled maintenance is still mandatory. Another limitation is film variability from supplier to supplier. Even within the same gauge and material type, different batches can have different coefficients of friction, different static charge characteristics, and different seal initiation temperatures. An automated line running only one film batch from one supplier at one constancy will perform well. Switch suppliers without updating your material database and you will see performance degrade within hours. The workaround is maintaining a material library with test-run parameters for every film lot you receive.

Human-Machine Interface Design That Actually Works
The HMI is where operators interact with your automation. Most VFFS HMIs are over-engineered. Operators do not need to see every PID loop parameter on the main screen. They need three things: current cycle status, any active faults with clear instructions, and quick access to the current recipe. Everything else should be one or two menu levels deep. I designed an HMI layout that showed the operator a simple color-coded flow diagram of the machine. Green meant normal. Amber meant a parameter was out of tolerance but the machine was still running. Red meant a fault requiring intervention. Each color zone was clickable and brought up the relevant diagnostics. This reduced mean time to recovery by approximately 60 percent compared to the previous scrolling-menu interface because operators could instantly see where the problem was instead of hunting through alarm histories.
Recommended Approach for a New Installation
If you are starting from scratch, do not try to automate everything at once. Phase it. Phase one is basic PLC logic with standard fault handling and recipe management. Phase two adds closed-loop tension and fill weight control. Phase three introduces vision inspection, predictive maintenance alerts, and production data logging. Each phase should run stably for at least two weeks before you move to the next. Rushing this process is how you end up with a system that does everything poorly instead of something core functions well. For existing machines, the highest-return automation upgrades in order of priority are: closed-loop film tension control, predictive seal parameter monitoring, and dosing synchronization with the fill cycle. These three alone typically reduce waste by 15 to 25 percent and cut changeover time in half. After that, vision systems and data analytics provide diminishing returns unless you are running high-volume commodity products where every percentage point matters.
A Note on Vendors and Third-Party Integration
Do not assume your VFFS OEM will seamlessly integrate with third-party equipment. Many do not. Some will charge substantial fees for open API access or refuse to share proprietary communication protocols. In those cases, you have two options: build a gateway using a universal PLC like a Siemens S7-1500 or a Beckhoff CX series that sits between the VFFS and your peripheral equipment, or work with an integrator who has done this specific combination before. The second option is usually faster and cheaper than reinventing the communication stack yourself, but finding one requires checking their project history, not their sales deck. One more thing that nobody tells you: document everything. Every parameter change, every recipe modification, every fault log entry. Six months from now when the line starts acting weird and you have no record of what changed, you will wish you had. I keep a simple spreadsheet for each line with date, change description, old value, new value, and who authorized it. It takes ten minutes per change and has saved me from making the same mistake twice in the same week on at least three occasions.