Reading the Code Without Losing Your Mind
The AWS D1.1 Structural Welding Code is a living document that welders, inspectors, and engineers are expected to reference constantly. It covers steel structures — buildings, bridges, towers, platforms, you name it. The current edition is D1.1:2020, and if you're working on anything that requires a stamp or insurance sign-off, your jurisdiction likely mandates a specific revision year. Using an outdated copy gets you a failed inspection every time, usually on pages you haven't read in three years. It is published by the American Welding Society and structured in a way that trips up people who aren't used to legal-technical writing. The code is split into mandatory and informative annexes, which means some sections are enforceable and others are just guidance. Nobody tells you this clearly at first. You'll see a requirement flagged with a footnote saying it's not mandatory and assume you can skip it, then get cited anyway because your AHJ (Authority Having Jurisdiction) decided that annex was binding for this project. I spent two weeks on a municipal parking garage project where the structural engineer specified D1.1:2015 but the fabricator had the 2020 revision on the shop floor. The 2020 edition added updated requirements for prequalified welds in certain material groups and revised the impact testing thresholds for temperatures below minus 30 degrees Fahrenheit. We caught it during a pre-weld conference, but only because the CWI on site actually read the foreword and note sections instead of diving straight into Chapter 3. That note alone saved us from welding six hundred joints under the wrong procedure.
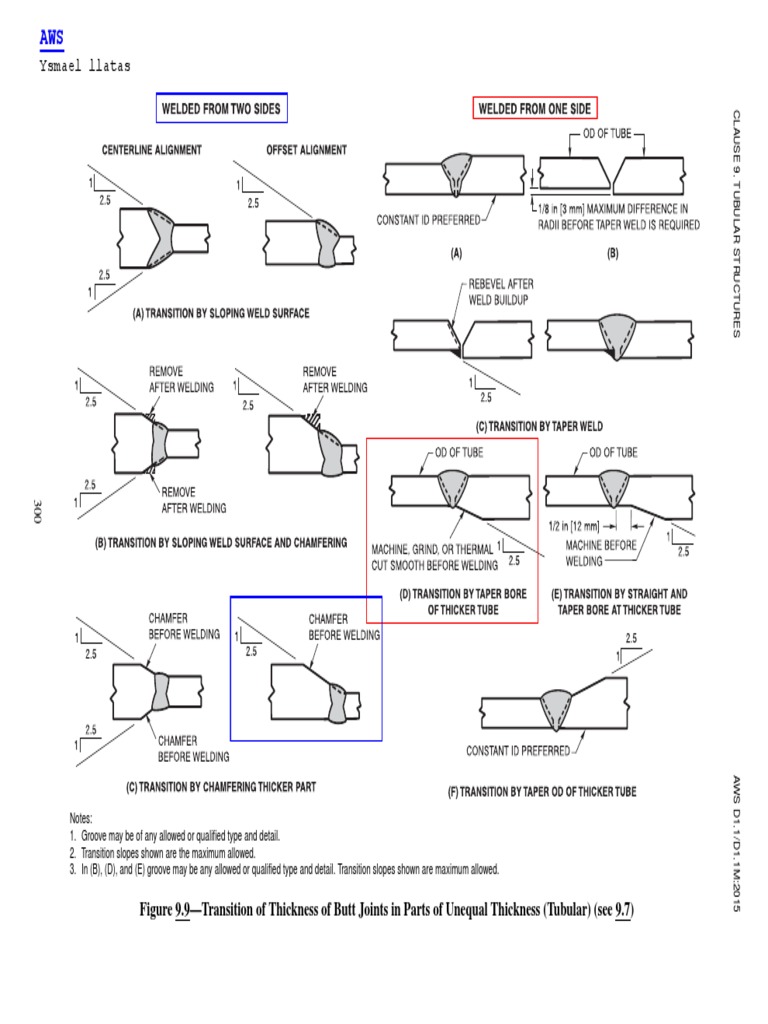
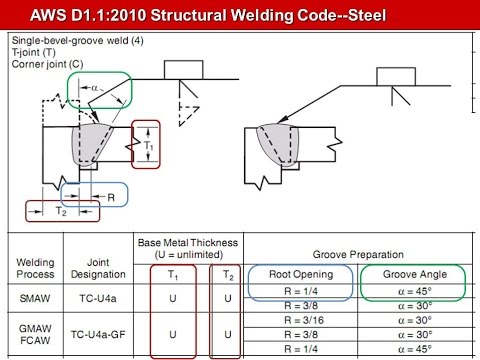
The code itself isn't free. AWS sells it directly, and printing companies resell it at markup. You can find the table of contents and preview chapters on aws.org, but the full document requires a purchase. Some universities and engineering firms have institutional licenses. If you're a solo welder or small shop owner, sharing a single copy with your team is common practice, but the code explicitly says the document must be readily available at the point of work. That means the shop floor copy needs to be current, not some waterlogged 2018 edition someone found in a storage closet. Here is what most people miss about the practical application. Chapter 3 — Prequalified Welding Procedures — is where the majority of fabrication shops live and die. The prequalified list lets you weld without developing a full WPS through testing, which saves significant time and money. But the prequalification has strict boundaries. If your material falls outside the specified thickness ranges, your joint design doesn't match one of the drawings in the code, or you're welding a material group that isn't listed, you cannot use the prequalified path. Period. I've seen guys try to bend the rules on thicker plates by claiming their groove geometry was close enough. It never works. The inspector will measure your bevel angle and root opening with calipers and call you out if it doesn't match the drawing exactly. There is no gray area in the prequalified tables. Another thing that catches people off guard is the relationship between D1.1 and the accompanying Commentary. The Commentary is not enforceable, but it explains why certain limits exist. For example, the code limits shielded metal arc welding (SMAW) interpass temperature to a maximum of 250 degrees Fahrenheit for certain material groups. The Commentary explains that this isn't arbitrary — it's tied to heat input control and the risk of coarse grain formation in the heat affected zone. Without understanding that, you might just see a random number and question whether it matters. It matters. Skip it and you're risking mechanical properties in the final joint.
Let me give you a specific edge case I dealt with last year. We were welding a series of moment connections on a steel frame renovation, using E7018 electrodes on A992 steel at thicknesses around three-quarters of an inch. The code's prequalified procedures for double-V grooves assumed a certain backing bar configuration. Our detail required a continuous weld all the way through without a backing bar, which technically fell outside the prequalified geometry. The engineer wanted to avoid the cost and lead time of qualifying a new WPS. I pointed out that the code has a section on special welding procedures that allows fabrication of a test coupon under actual conditions when a prequalified procedure doesn't fit. We ran the qualification — two tension tests, two bend tests, and visual plus NDE on the coupons — and had a valid WPS within ten days. Cost was roughly four thousand dollars including labor and consumables, versus an estimated eighteen to twenty-five thousand if we had gone the full procedure qualification route. The whole thing took about two weeks from start to weld-on approval. Inspection under D1.1 is another area where practice diverges sharply from what the text says. The code outlines requirements for welder performance qualification in Chapter 4, which is separate from the welding procedure qualification in Chapter 3. A welder can have a qualified WPS but still fail if they cannot produce sound coupons. I once had a welder who was excellent on production work but consistently cracked his impact test specimens during the notch toughness portion. His gouging technique for preparing the Charpy V-notch was too aggressive, leaving tool marks that acted as stress concentrators. He wasn't producing bad welds — the issue was entirely in his sample preparation. We switched him to electrolytic cutting for the notches, and his pass rate went from zero to full compliance. The code doesn't tell you that story, but any inspector who has been doing this for a while has seen it. One blunt limitation of D1.1 that nobody advertises: it does not cover aluminum, stainless steel, or cast iron. Those materials fall under other AWS codes like D1.2 for aluminum or D1.6 for stainless. If you're reading D1.1 and wondering why your stainless steel requirements aren't addressed, that's why. Also, the code assumes ambient temperature fabrication conditions unless otherwise specified. Cold weather welding requires additional precautions outlined in the code, but the baseline procedures don't account for sub-zero environments without supplemental clauses. I worked a winter job in Montana where the ambient temperature dropped to minus fifteen. We had to implement heated enclosures, preheat the base metal to the minimums specified in the code's cold weather tables, and extend the holding time between passes. Production dropped to maybe forty percent of normal output for three weeks. The code allows it, but it doesn't make it easy.
Get the Full Details
If you're trying to get started with the code, the fastest path is not reading it cover to cover. That takes months and you'll forget everything by page two hundred. Instead, identify your application — what material, what thickness, what joint type, what environment — and go directly to the relevant chapter and tables. Use the index to find your specifics. Cross-reference with the Commentary for context on the requirements that matter. Keep a bookmark or highlighter handy so you can flag the sections that apply to your current project. The code is dense enough that skimming gets you in trouble. For the download question, the official source is aws.org. You can purchase the current edition there, and they occasionally offer digital versions at a discount. Third-party sites that claim to offer free PDFs are either outdated, illegally distributed, or both. Using an unauthorized copy won't hold up if an auditor asks to verify your revision. The engineering liability side of things makes that a real risk, not just a legal technicality. The practical takeaway is that the code is a minimum standard, not a maximum. Many projects, especially those with structural engineers who understand welding, will add requirements on top of D1.1. NDE percentages, additional impact testing, stricter fit-up tolerances — all of that is common and perfectly legal. The code sets the floor. Your contract and drawings set the ceiling.