Understanding Bechtel Manufacturing And Technology
Bechtel Manufacturing And Technology represents the engineering firm's shift toward modular construction, prefabrication, and digital integration for large-scale infrastructure and energy projects. If you're trying to implement or work within their framework, you need to understand both the physical fabrication side and the software layer that holds it together. The core of their manufacturing approach is site-modular construction. Instead of building everything piece-by-piece at the project location, you design components in a controlled yard environment, fabricate them as assemblies, then ship and erect them on site. A typical power plant module—say, a complete electrical switchgear room with all cabling, conduit, and terminations pre-installed—can reduce field labor by 40 to 60 percent compared to traditional stick-building. That's not a theoretical reduction. I watched a client project in the Gulf Coast where the modular approach cut the instrument and control installation phase from roughly eleven weeks down to about three and a half weeks of actual field time. The technology side runs through what they call a digital thread. Everything starts in a federated 3D model—usually delivered in Navisworks or similar coordination formats, though increasingly moving toward common data environments with ISO 19650-based information management. Model-driven takeoffs feed directly into procurement. Each fabricated piece carries a serialized tag that links back to its position in the model. When you install it, the as-built status updates in the system. It's meant to eliminate the classic construction problem where what got built doesn't match what was documented.
Implementation Process For A New Facility Project
Here's the practical sequence you'd follow if your team is committing to this approach on a greenfield project: Phase one is design-for-fabrication. You don't just design normally and then decide to modularize later. The geometry, weight limits, lift points, and transport constraints are baked into the design from day one. Every component needs to fit within standard shipping envelopes or require special routing permits. I've seen projects stall for months because someone designed a vessel assembly that was four feet too wide for highway transport and nobody caught it until the shop drawings were nearly finalized. Phase two is the virtual build. Before anything gets cut, you run a 4D simulation—meaning the 3D model is tied to the construction schedule. You walk through the entire erection sequence virtually. This catches crane placement conflicts, material delivery sequencing problems, and temporary support requirements. On a recent combined cycle plant project, the 4D review revealed that two major modules couldn't be installed in the planned sequence because the crane radius overlapped in a way that wasn't obvious from the static model. Reworking the lift plan in the virtual environment took a week. Doing it after steel was already in place would have taken six.
Phase three is the fabrication yard execution. You need a shop environment that matches the quality and documentation standards the site will enforce. This is where the digital thread becomes critical. Each fabricated subassembly gets a unique identifier. Material certifications, weld records, and inspection results are logged against those identifiers in real time. If you fall behind on documentation in the shop, the site team cannot verify what they're installing, and that creates a bottleneck that will eat into your critical path faster than any fabrication delay. Phase four is transportation and site erection. Logistics planning here is non-negotiable. You need route surveys, bridge weight assessments, and traffic control plans well before the modules leave the yard. On a refinery project I was involved with, we had a module that required an escort vehicle convoy and a temporary traffic pattern change at three intersections. Getting municipal approval for that took eight weeks, and we hadn't planned for it because we assumed standard oversize load permits would cover it. They didn't.
Get the Full Details
Software And Documentation Standards
Bechtel's technology stack typically centers around Autodesk platforms for modeling and coordination, with SharePoint or a dedicated CDE for document control. Specific tools you'll encounter include: Navisworks for clash detection and model review. This is standard across the industry now, not unique to Bechtel, but it's the primary vehicle for the coordination process. You'll receive models in NWC format for viewing and in intermediate formats for clash analysis. P6 or equivalent scheduling software for the 4D integration. The schedule must be detailed enough to support daily erection sequencing. A high-level milestone schedule won't work here. You need activity durations tied to specific model elements.
A document management system that supports transmittal workflows with mandatory fields for revision level, source system, and approval status. This sounds administrative but it's where most projects fail. I've seen deliverables returned for resubmission three or four times because the transmittal metadata didn't match what the system expected. The workaround I found was to create a pre-transmittal checklist that matched every required field in the CDE before anything went through the formal review process. It eliminated about ninety percent of those administrative rejections.
Common Pitfalls And Where The Approach Breaks Down
Modular construction with this level of technology integration does not work for every project type. It fails when the design is not sufficiently advanced before fabrication begins. If you start building modules while the P&IDs are still being finalized, you're going to have rework. Serious rework. Not the kind that a punch list fixes. I worked on a water treatment facility where the process vendor changed the piping layout after modules were already in production. We tore out and rebuilt approximately fourteen thousand dollars per linear foot of installed piping because the module design had locked in the support structure and penetration locations. The approach also breaks down when the client organization isn't set up to handle the documentation flow. The digital thread requires real-time updates from multiple stakeholders. If your field superintendents are still filling out paper inspection requests and scanning them in days later, the model stays stale and the as-built record becomes unreliable. I've seen teams try to compensate by assigning a dedicated document controller to each module, but that adds significant cost and often isn't sustainable on smaller projects. Transportation constraints are another area where people consistently underestimate the impact. The cost of special permits, escort vehicles, and route modifications can run into six figures for a single large module on a complex route. I had a project where the initial logistics budget was based on standard oversize load costs. The actual route included two low-clearance overpasses that required temporary removal and reconstruction. That added approximately fourteen hundred thousand dollars to the transportation line item and two months to the schedule. The route survey should have been completed during the design phase, not during procurement.
Cost And Timeline Realities
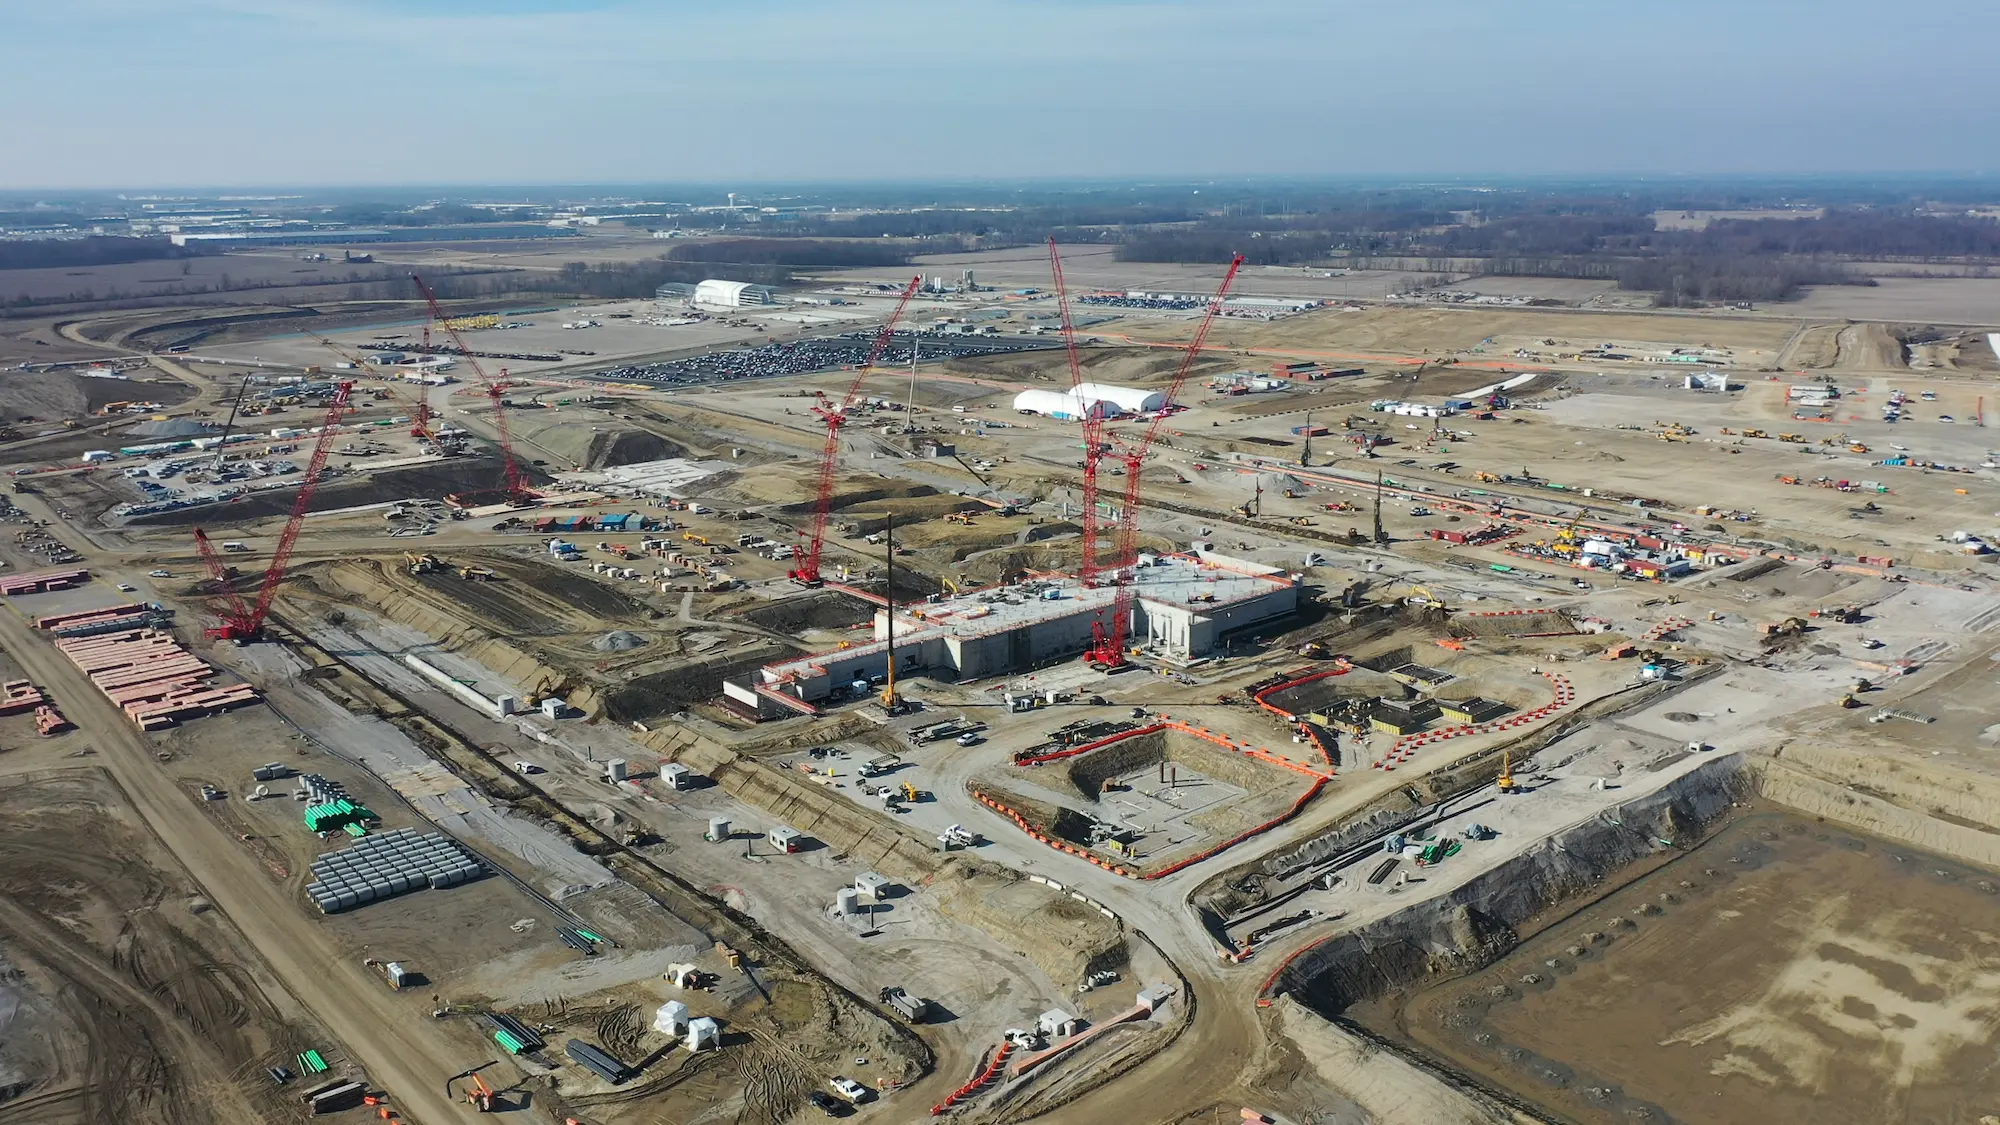
The financial case for Bechtel Manufacturing And Technology depends heavily on project scale and complexity. For large industrial facilities—power plants, refineries, chemical complexes—the modular approach typically delivers a 10 to 20 percent reduction in total project duration and a 5 to 15 percent reduction in total installed cost. The savings come from reduced field labor, shorter commissioning timelines, and better quality control in the shop environment. But these numbers assume the design is complete before fabrication starts and the logistics are properly planned. For smaller or more custom projects, the economics reverse. The upfront engineering cost for design-for-fabrication is higher than conventional design. The fabrication yard overhead gets amortized over fewer modules. Transportation costs per unit of installed capacity are significantly higher when you're moving smaller batches. In those cases, a hybrid approach makes more sense—modularize the most complex systems like electrical and instrument rooms, but stick to conventional construction for structural steel and piping racks where the site conditions are straightforward.
Practical Steps To Get Started
If you're evaluating whether this approach fits your next project, start with a modularity assessment. Review the project design packages and identify systems that would benefit from prefabrication. Typically, process skids, electrical switchgear rooms, instrument cabinets, and pre-piped machinery skids are the strongest candidates. Systems that are highly customized to site-specific conditions or that require frequent field modification during commissioning are poor candidates. Then build a detailed logistics plan before you commit to the fabrication schedule. Route surveys, permit timelines, and crane access analysis should all be complete and documented before you issue fabrication orders. This step alone will catch the issues that derail most modular projects. Finally, align your documentation requirements with your client's CDE expectations early. Define the exact data fields, file formats, and transmittal procedures in the project execution plan. Don't wait until the first deliverable is rejected to figure out what the system requires. The team that solves this problem in week one saves months of administrative friction over the following year.