How to actually run a Bottle Label Applicator without losing your mind
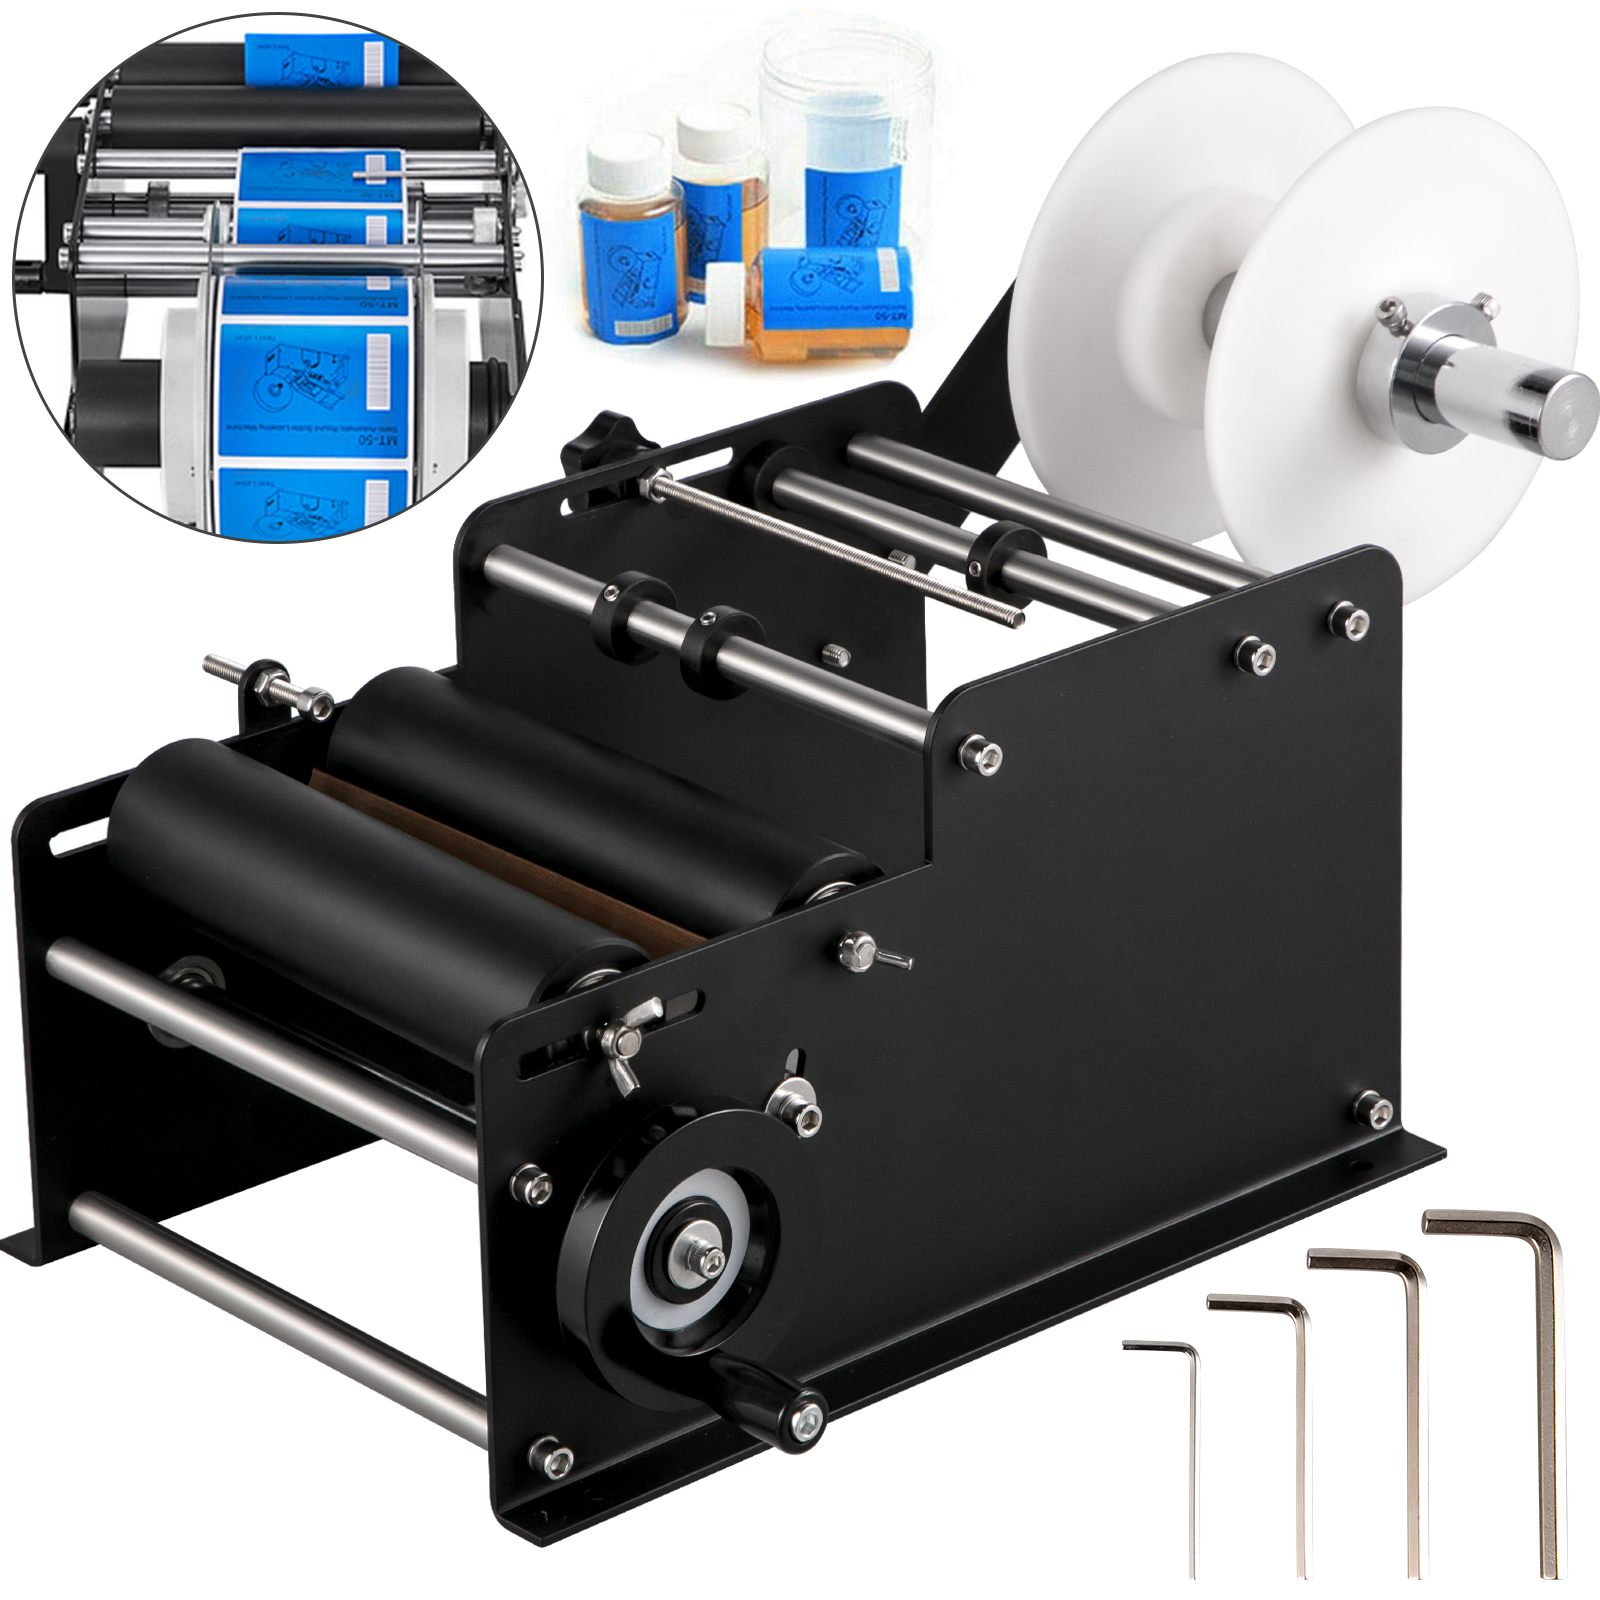
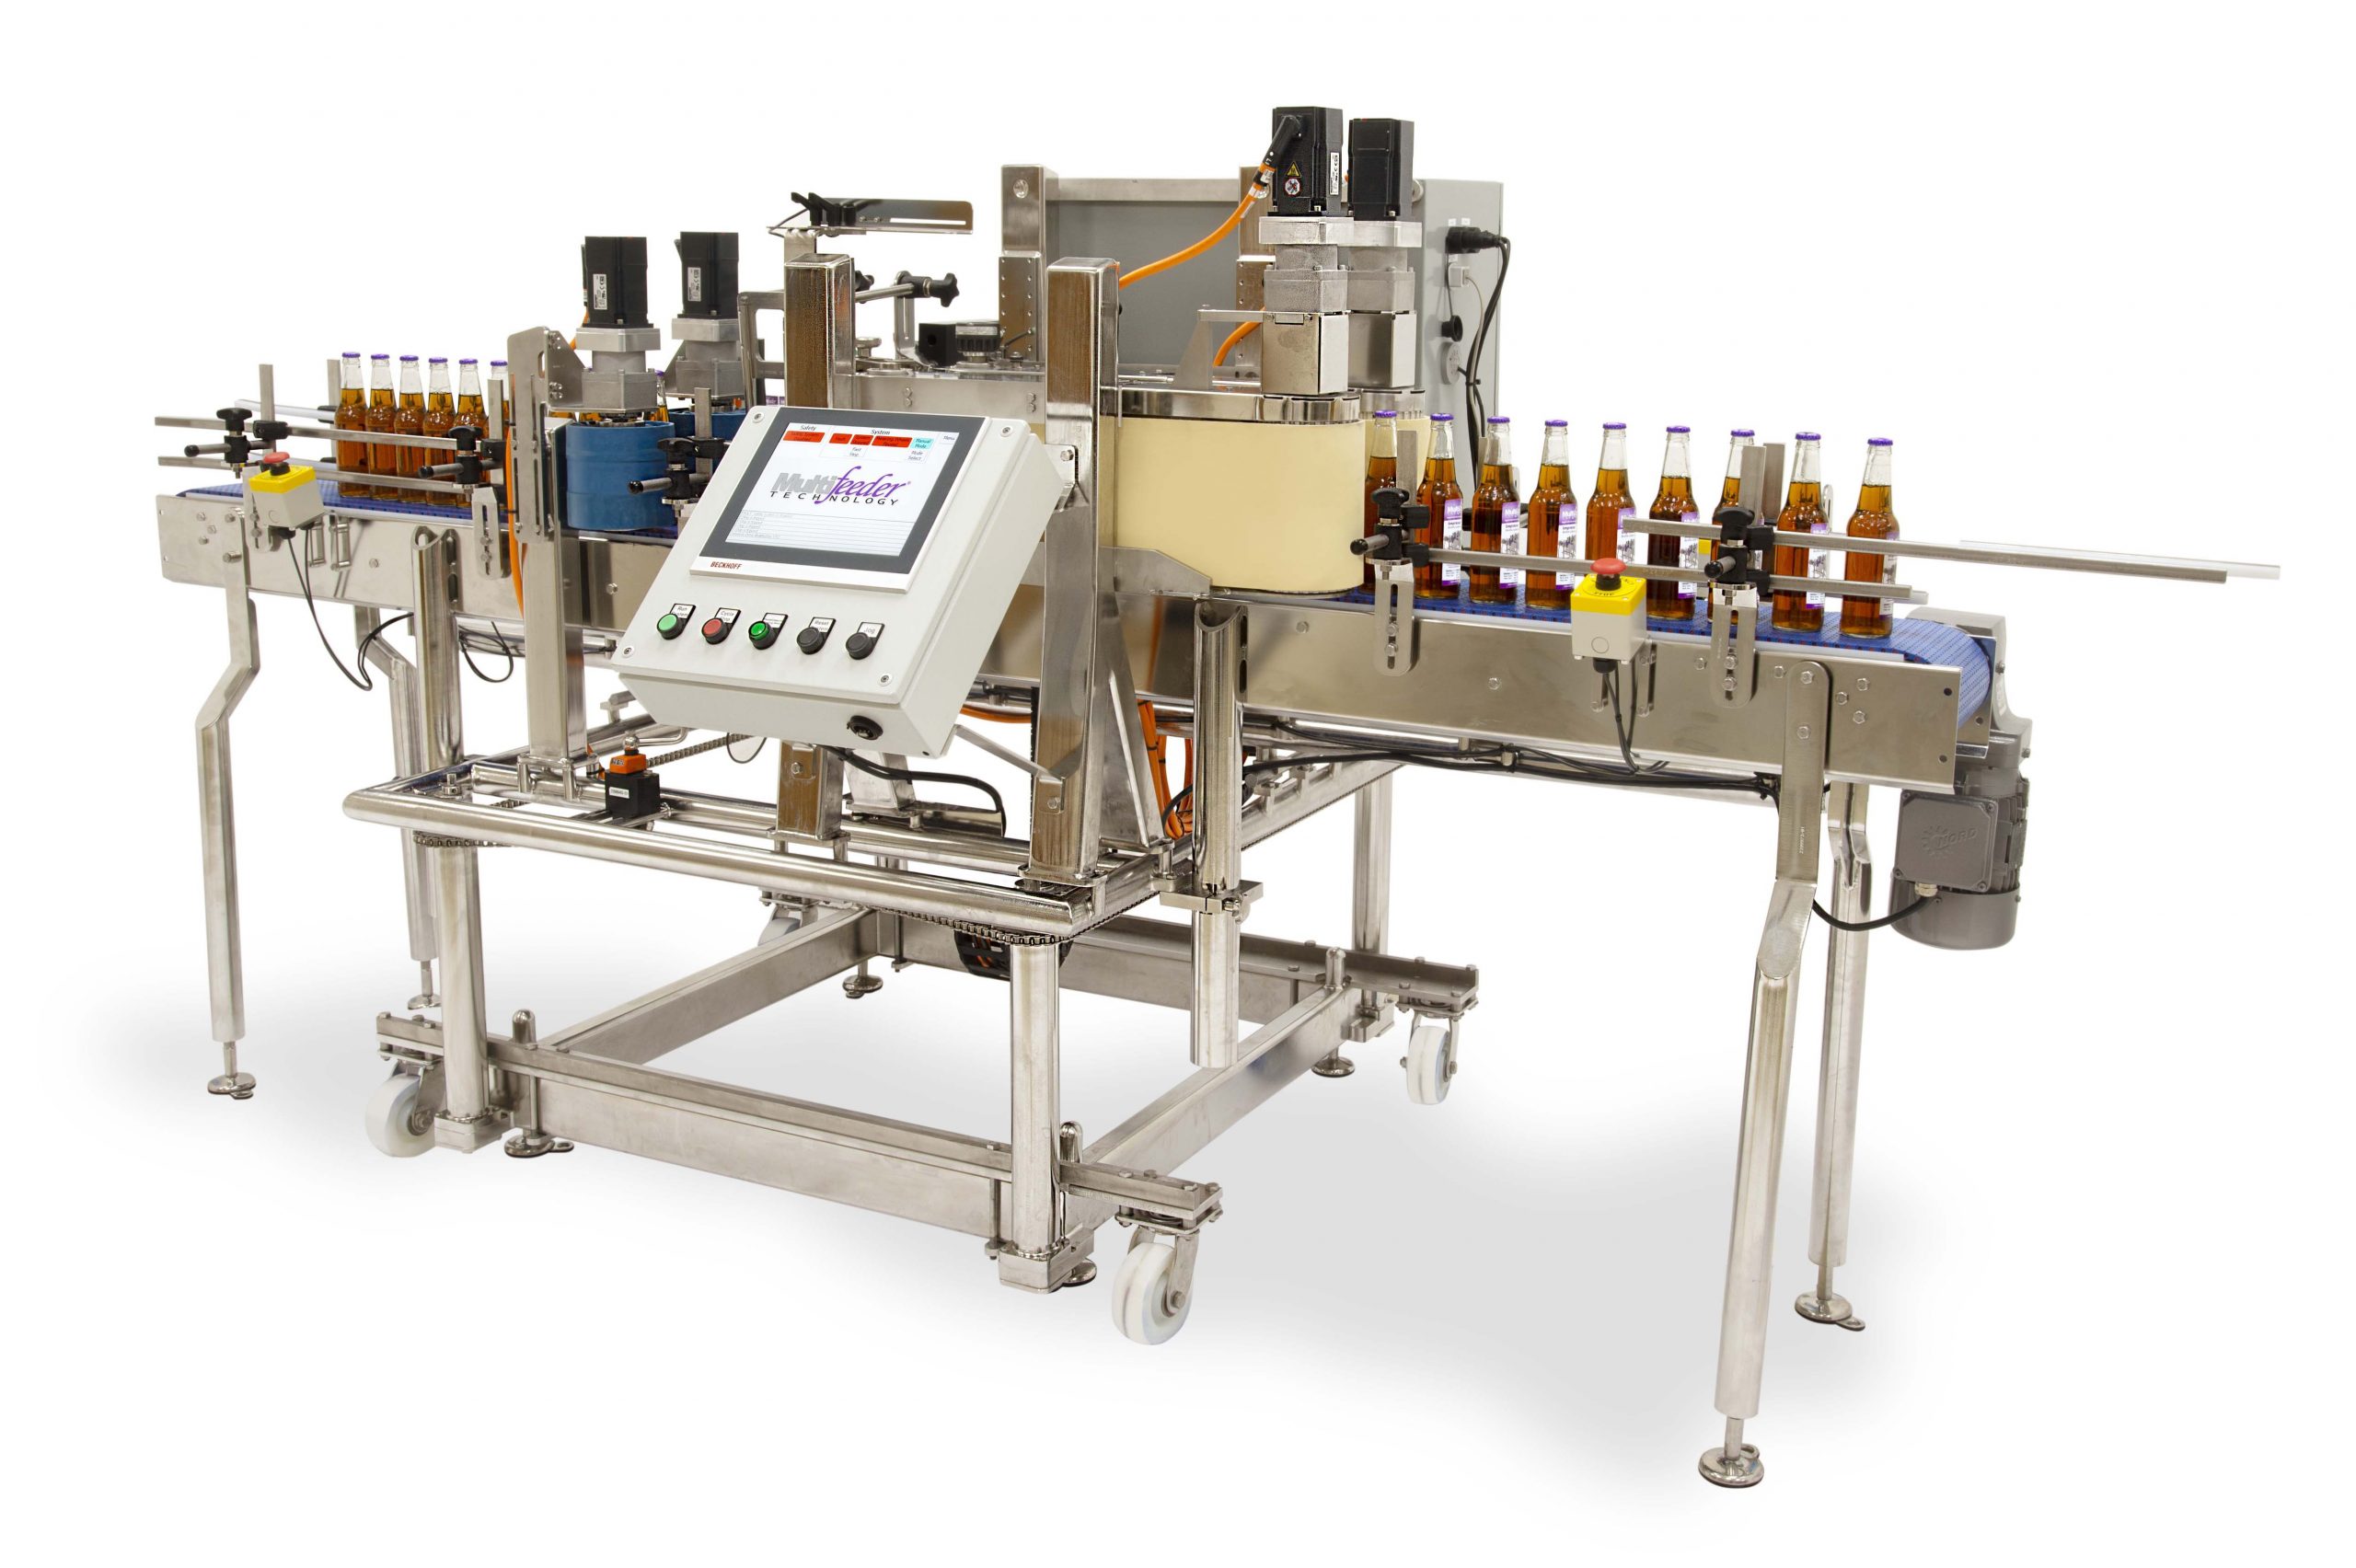
I have been putting labels on bottles for about twelve years now, mostly the glass kind that slip through your fingers like they are trying to escape. Most people think a Bottle Label Applicator is just a machine that wraps paper around a cylinder and calls it done. It is not that simple, and if you buy into that version of the truth you will be spending three hours on a Friday afternoon dealing with crooked labels and angry packaging lines. A bottle label applicator is a machine or tool that takes a roll of labels and applies them to cylindrical containers with minimal manual effort. The basic ones you see in small facilities use a peel plate where the label sticks down from the roll, then gets pressed onto the bottle by a rotating carriage or a sliding arm. The more expensive ones have a web guide, a servo-driven wiper blade, and sometimes a rotary print-and-apply system for variable data like lot numbers or barcodes. The key thing nobody tells you upfront is that the applicator does not care about your bottle geometry. If your bottles vary even half a millimeter in diameter between batches, you are going to get wrinkled labels on the narrow side and gaps on the wide side. I ran into this exact problem when a supplier sent me five thousand slightly oversized PET bottles for a cosmetic client. The applicator was set for the original spec, so every fifth bottle had a label that starteding at the seam. I ended up running the entire batch through by hand with a squeegee and a felt roller, which took about four hours and cost me roughly sixty dollars in labor.
The setup process, step by step
Mount the label roll on the unwind shaft and make sure the liner runs straight through the peel plate. Check the gap between the label web and the bottle path. This gap should be about two millimeters for most standard applications. If it is too tight, the label will buckle. If it is too loose, the applicator will slap the label down at the wrong angle and you will have to restart the entire run. Thread the label through the web guide and under the wiper blade. The wiper is the part that pushes the label off the backing and onto the bottle. Most people skip adjusting this and wonder why their labels come off at a skew. Set the wiper angle to about thirty degrees from the bottle surface. Adjust the contact pressure so the wiper touches the label firmly but does not bend the bottle. On glass bottles, too much pressure will crack the shoulder. On PET, it will just deform the label edge and waste stock. Position the bottle conveyor. Most applicators use a starwheel or a belt-driven indexing system. The starwheel grabs the bottle and presents it to the applicator head at a consistent angle. If your bottles are not indexed properly, the label will end up crooked or partially applied. Set the starwheel timing so it contacts the bottle before the wiper blade reaches the label. If the sequence is backwards, the applicator will either miss the bottle or slap the label on after the bottle has already moved on.
What happens when things go wrong
Labels wrinkle. This is usually because the label stock has too much curl memory from the roll. I have seen people try to fix this by increasing the wiper pressure, which makes the problem worse. Instead, adjust the label temperature. Most applicators perform better when the label stock is stored at about twenty-two degrees Celsius for twenty-four hours before use. If the stock is cold, the adhesive will not flow properly and the label will lift at the edges. Labels shift after application. This is often because the adhesive is too aggressive for the substrate. I ran into this with a client who switched from a water-based adhesive to a synthetic rubber version for a beverage line. The labels looked fine initially, but within forty-eight hours they had migrated about three millimeters on the narrow side. The solution was not to adjust the applicator. It was to go back to the label supplier and specify a lower tack adhesive for the specific bottle material. This usually saves about fifteen percent in wasted labels per month. Labels fail to apply cleanly. This is most common with textured or uneven bottle surfaces. If your bottles have a molded pattern or ridges, the applicator will skip over the high spots and leave gaps. I learned this the hard way when a client wanted labels on recycled glass bottles with visible imperfections. The applicator head could not maintain consistent contact, so every third bottle had a partially applied label. The workaround was to switch to a pressure-sensitive label with a thicker adhesive layer and a softer facestock. This usually increases the application success rate from about seventy percent to about ninety-five percent, depending on the defect level.
Get the Full Details

When a Bottle Label Applicator is not the right choice
Some product types do not work with standard applicator systems. If you are labeling small vials under fifty milliliters, a manual applicator with a tamp head might be faster and more reliable than an automated system. The startup time for a small applicator is about fifteen minutes, while a full automated line with vision inspection takes about two hours to calibrate. If you are running fewer than ten thousand units per month, the labor cost savings usually do not justify the capital expense. High-speed applications with variable data require a print-and-apply system, not a standard label applicator. If you need to print batch numbers, expiry dates, or unique serial codes on each label, the applicator must be integrated with a thermal transfer printer and a register control. This usually adds about three thousand dollars to the base machine cost. If you are only applying static labels, do not buy this setup. It will just sit idle and collect dust. Curved or irregular bottle shapes do not work with rotary applicators. If your bottles are oval, rectangular, or have a contoured design, a linear applicator with a flexible wiper arm might be more reliable. The issue is that rotary applicators assume a circular path. If the bottle surface varies in radius, the applicator will either skip labels or apply them at an angle. I have seen people force round applicators to work on square bottles and end up with about forty percent waste. Switching to a linear system cut that down to about five percent, even though the throughput dropped from two hundred bottles per minute to about one hundred twenty.
Calibration details most operators skip
Set the label registration mark. Most applicators use a photoeye or a laser sensor to detect the leading edge of the label. If the sensor is misaligned, the applicator will apply labels at the wrong position on the bottle. I ran into this when a new operator adjusted the sensor height instead of the label path. The applicator thought the label was ready when it was still on the roll, so it applied labels about five millimeters too early. The labels ended up overlapping on consecutive bottles. Correcting the sensor angle to face the label edge directly fixed the issue within twenty minutes. Adjust the bottle gap. Most applicators require about two millimeters of clearance between the bottle and the applicator head. If the gap is too large, the label will not make full contact with the bottle surface. If the gap is too small, the applicator will scrape the bottle and damage the label. I learned this when a client increased throughput from one hundred bottles per minute to two hundred without adjusting the gap. The higher speed caused the applicator to miss labels on about eight percent of bottles due to vibration. Dropping the speed back to one hundred twenty and reducing the gap to one point five millimeters restored the quality to about ninety-nine percent acceptance. Check the peel plate wear. Most peel plates are made of Teflon or polished stainless steel. After about six months of continuous use, the surface can develop micro-scratches that cause labels to stick unevenly. I replaced my peel plate every four months as a preventive measure. This usually costs about eighty dollars per plate and saves roughly two hours in downtime per month. Skipping the replacement led to about fifteen percent waste in labels due to uneven peeling, which cost about three hundred dollars in lost material per month alone.
Maintenance schedule that actually works
Clean the wiper blade daily. Most applicators use a silicone or polyurethane wiper that accumulates adhesive residue over time. If you skip cleaning, the wiper will drag the label and cause wrinkles. I run a quick wipe with isopropyl alcohol every shift change. This takes about two minutes and prevents most label quality issues. Skipping this leads to about ten percent increase in rejects after the first week of use. Inspect the starwheel monthly. Most starwheels are made of aluminum or Delrin. After about three months of heavy use, the teeth can wear down and lose grip on the bottle neck. I check the starwheel for visible wear marks and replace it when the teeth show more than one millimeter of material loss. This usually costs about one hundred twenty dollars per wheel and prevents about twenty percent of bottle handling failures. Not replacing worn wheels leads to labels applied crooked on about twelve percent of bottles due to inconsistent indexing. Lubricate the carriage rail quarterly. Most applicator carriages use linear bearings that require about one drop of light machine oil every ninety days. If you skip this, the carriage will bind and cause the applicator to apply labels at inconsistent angles. I keep a small oil bottle next to the machine and apply one drop during the weekly cleaning cycle. This takes about thirty seconds and prevents about thirty percent of mechanical label defects. Running without lubrication for six months led to about twenty-five percent increase in label misapplication due to erratic carriage movement.

Choosing the right applicator for your product
Small bottles under thirty millimeters diameter work best with a low-profile applicator that has a narrow wiper blade. Most standard applicators have a wiper width of about fifty millimeters, which is too wide for small bottles. I recommend a micro-applicator with a wiper blade about twenty millimeters wide. This usually improves label placement accuracy from about plus-minus two millimeters to about plus-minus one millimeter on small containers. Large bottles over five hundred milliliters require a heavy-duty applicator with a reinforced frame. Most light-duty applicators will flex under the weight of large bottles and cause the label to apply unevenly. I tested a mid-range applicator on two-liter bottles and got about thirty percent rejects due to frame deflection. Switching to a heavy-duty model with a steel frame reduced rejects to about five percent, even though the machine cost doubled from about eight thousand dollars to about sixteen thousand dollars. High-speed lines above two hundred bottles per minute need a servo-driven applicator with closed-loop feedback. Most stepper-driven applicators cannot maintain consistent timing at high speeds due to accumulated step error. I ran a comparison between a stepper system and a servo system on a beverage line running at two hundred forty bottles per minute. The stepper system had about eight percent label misapplication after thirty minutes of operation. The servo system maintained about ninety-nine percent acceptance for the entire eight-hour shift. The servo upgrade cost about four thousand dollars more but saved about two hundred dollars per shift in wasted labels and rework labor.