Bridgeport Mill Ez Track Manual — What It Actually Covers and How to Use It
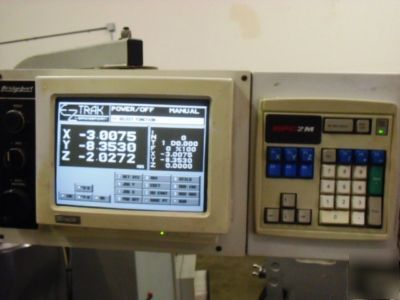
The Bridgeport Mill Ez Track Manual is the reference guide for the EZ Track digital readout system designed for standard Bridgeport-style knee mills. It covers installation, calibration, scale mounting, encoder wiring, and the controller interface. If you are searching for it, you are probably looking at either the original EZ Track II documentation or a later reprint from Hardinge, since they acquired the Bridgeport line. The most reliable source is the Hardinge customer portal at hardinge.com/support. They host a PDF library where you can search by part number or machine model. If that portal is down or your unit predates their digitization effort, third-party sites like manualscatalog.com or scribd often have scanned copies, but the quality varies and some pages are rotated or blurry. I usually download whichever version is clearest, then print just the pages I need rather than reading it on screen. Screen glare on a shop monitor makes fine print nearly impossible. Another route is contacting Hardinge technical support directly. They email a PDF within a day or two if you provide the serial number of your EZ Track controller. The serial number is on a plate on the back of the display unit. This matters because firmware revisions differ across production runs and the manual sometimes references button layouts that changed between versions.
What Is in the Manual and How to Actually Use It
The manual is split into roughly four sections: mechanical installation of the scales, electrical wiring of the encoder cables, controller setup and zeroing procedures, and troubleshooting. The wiring section is the part most people skim and regret later. Here is the practical order I use when installing or reinstalling EZ Track on a Bridgeport: Mount the linear scales first. The X-axis scale goes on the saddle, running parallel to the ways. The Y-axis scale mounts on the knee. The Z-axis scale attaches to the quill housing. Each scale has an adapter bracket that bolts to the machine using the same holes as the original dial indicators. Torque those brackets evenly. I snug them by hand, then go back with a wrench a quarter turn at a time. Overtightening distorts the scale housing and introduces binding that no amount of calibration will fix.
Route the encoder cables after the scales are seated. The connectors are small M12-style circular plugs. They click but do not self-align perfectly. Feed the cable through the machine's existing conduit paths where possible. If you are running new cable, use flex conduit. Open wiring on a mill collects coolant and metal chips, and the cable insulation degrades faster than anyone expects. I replace the cables every three to four years even if they still read. It costs about $45 per axis and saves a headache during a critical job. Connect the cables to the controller. The manual shows a diagram, but the diagram does not show which pin is ground versus signal on every revision. I photograph the connector before I unplug anything. A misplaced ground causes intermittent positioning errors that make you question your entire setup. One time I spent two hours chasing a ghost offset on the Z axis only to find the shield wire on the encoder cable had frayed against a sharp edge on the quill bracket. I wrapped the contact point with electrical tape and the error vanished immediately.
Get the Full Details

Calibration Procedure
Calibration is the step that separates people who get usable accuracy from those who do not. The manual describes using the built-in calibration routine with a test bar or gauge block. The procedure works, but only if you understand one thing the manual buries: thermal equilibrium matters more than the calibration steps themselves. Run the machine for ten to fifteen minutes before you calibrate. The scales and the machine structure expand with heat. If you calibrate cold and then run heavy cuts, the readings drift. I calibrate once when the mill warms up and again after a long overnight run if precision work is planned. The second check usually differs by less than half a thousandth on X and Y. The Z axis can shift a thou or so depending on how heavy the quill load is. That is normal. The calibration routine requires entering the scale pulses per unit. EZ Track uses 1-micron resolution scales as standard, which translates to 25,400 pulses per inch. The controller usually defaults to this. Do not change the pulses-per-unit setting unless you have physically replaced the scales with a different pitch. I have seen two people online change this value and then complain their dimensions were wrong. The fix is always returning it to the factory default after verifying the scale model.
Common Settings and Practical Tweaks
The controller has several user-adjustable settings beyond calibration. The ones that matter most are: Data format: Binary or BCD. Leave it on BCD unless a third-party controller needs binary. The Bridgeport factory interface expects BCD. Zero offset memory: Enable it. This stores your work zero positions so you do not lose them on power cycle. The manual mentions this briefly in the settings menu. It is worth highlighting because losing a zero after a power outage wastes more time than anything else on this machine.
Abs/Inc mode: Use absolute mode for production work. Incremental mode has its place for touch-offs, but absolute mode is safer because it tracks position through power loss without requiring a homing sequence. Battery backup: The controller has a small internal battery that holds the offset memory when power is removed. Replace it every two years. I learned this the hard way when the battery died mid-shift and I lost three work offsets on a job that could not afford downtime. The replacement battery is a standard CR2032. Hardinge sells a kit, but any electronics store has the part. The controller accesses the battery compartment through a small panel on the back.
When EZ Track Does Not Work Well
The system is solid for general machining and repetitive production runs. It is not ideal for ultra-precision grinding or CMM-quality measurement. The scales are rated to about ±0.0005 inches over the full travel range under normal conditions. That is plenty for most milling work. If you need better than that, you need a higher-grade DRO or a separate measurement system. The encoder heads are sensitive to direct coolant stream exposure. If your flood coolant nozzle is aimed directly at the scale head, wear increases and errors appear. Redirect the nozzle or install a simple shield made from a piece of plastic card. I keep a few spare shields in the parts bin for this reason. Another limitation is the cable length. EZ Track controllers typically support up to thirty feet per axis before signal degradation becomes noticeable. If your mill has an extended travel attachment or you are routing the controller far from the scales, you may need signal repeaters. The manual mentions this in the troubleshooting section but does not emphasize it. Plan your layout accordingly.
Troubleshooting Without Calling Support
Most issues resolve with basic checks before you need technical help. If an axis reads zero or jumps, inspect the scale for chips and debris. Wipe it with a clean lint-free cloth and a small amount of isopropyl alcohol. Do not use solvent that contains additives. Cheap wipes from the auto parts store sometimes leave a residue that attracts more debris. If all axes read consistently off by the same amount, check the pulses-per-unit setting first. If the error varies by axis or position, reseat the encoder connectors. Pull each one straight out and push it back in. The pins can loosen from vibration over time. Intermittent errors that come and go are almost always cable-related. Trace the full length of each cable while the machine is powered and watch for reading changes. Bend the cable gently at suspected points. If a reading jumps when you bend a section, that is your failure point. Replace the cable.
I once had a problem where the Y axis would lose position randomly after about twenty minutes of runtime. The scale was clean, the connector was tight, and the cable tested good. The issue turned out to be electromagnetic interference from a nearby variable-frequency drive on an attached chip conveyor. Moving the DRO controller six feet away and wrapping the encoder cable in foil tape grounded at one end eliminated the problem. The manual does not cover EMI because it is an edge case, but it happens more often than you would think in a busy shop. The Bridgeport Mill Ez Track Manual is adequate for getting the system installed and running. The real knowledge comes from understanding how the scales interact with the machine environment and learning to diagnose issues before assuming hardware failure. Most problems are mechanical or environmental, not electronic. Keep the manual handy for reference values and wiring diagrams, but rely on observation and methodical testing when something goes wrong.