Why Most BCP Templates Fall Apart on the Floor
A manufacturing business continuity plan template for Manufacturing is a document that tells your plant what to do when something breaks. That's it. Most companies fill one out once a year, file it somewhere, and assume they're covered. When the line goes down three weeks later, nobody can find it or figure out who calls whom. The gap between a document and an actual plan is usually the difference between an hour of downtime and a week of it. I spent the better part of a decade working through this stuff on the floor, watching templates fail in ways that had nothing to do with how they were written and everything to do with who actually uses them. The people who need the plan during an incident are the shift supervisors and maintenance leads, not the people who filled out the form last January. If your template doesn't account for that, it's just paperwork.
Building a Business Continuity Plan Template For Manufacturing That Actually Works
Start with the operations, not the document. Walk the floor and identify every single point where production stops dead if something goes wrong. Not the theoretical points. The actual ones. I learned this the hard way at a mid-sized automotive parts facility where our template listed a "backup generator" as a recovery resource. The generator existed, but it only powered the office HVAC and the break room microwave. The CNC machines, the compressors, the conveyor system — none of it. We found that out during a three-day blackout in 2019, which was not a fun experience for anyone involved. After that incident, we rebuilt the template from scratch. Here's what actually goes into it, structured the way it needs to be for real use:
Section 1: Critical Process Identification
List every process step that directly impacts product output, safety, or regulatory compliance. Don't group them into vague categories like "production" or "shipping." Be specific. "CNC mill line 3", "powder coat curing oven", "final QA inspection station 2". If a process can't be named with enough specificity that a new hire could point to it on a floor map, it's not specific enough. I used to see templates that included a column for "criticality rating" scored 1 through 5. Nobody knew what those numbers meant. I replaced it with a simple three-tier system: Tier 1 means the line stops immediately if this is down. Tier 2 means output drops but doesn't stop. Tier 3 means this is a support function that enables Tier 1 or Tier 2 processes. It took three meetings instead of three hours, and every shift supervisor understood it by the end.
Get the Full Details
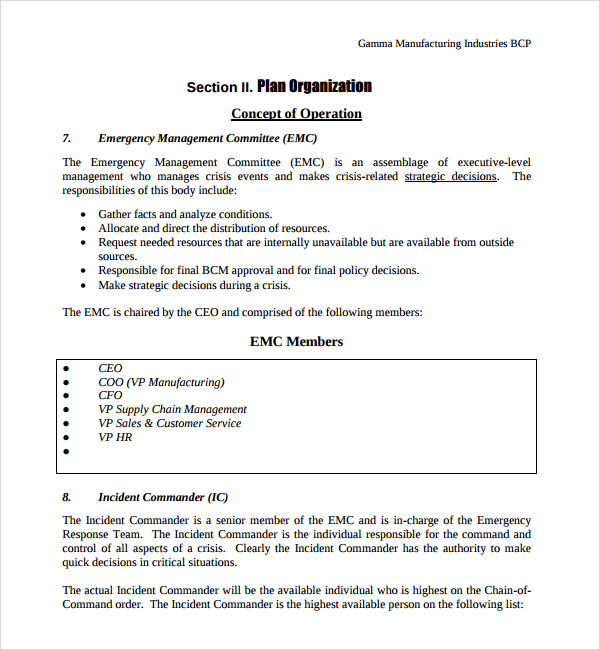
Section 2: Impact Analysis
This is where most templates go soft. They ask you to "estimate potential losses" which gives you a spreadsheet full of guesswork. Instead, calculate the actual cost per hour of downtime for each critical process. Your machine rate, your labor cost per hour on that line, your material waste rate, your customer penalty clauses if deliveries slip. Multiply it out. $47,000 per hour of downtime on Line 2 sounds very different from "$significant financial impact" when you're trying to make a case for capital expenditure on a backup system. The counter-intuitive part here is that your highest-cost downtime risk is rarely your largest machine. It's usually the one component that feeds ten other lines. At that parts facility I mentioned, our biggest single point of failure wasn't a $2 million press. It was a $12,000 vacuum pump that supplied three different molding stations. Replace that pump and the entire assembly section shuts down. The template needed to flag that clearly, and it didn't. We fixed it by adding a dependency map next to each critical process.
Section 3: Recovery Procedures
This is the section that matters most and gets written worst. Every recovery procedure needs to be something a person can follow at 2 AM on a Tuesday when they've only been on the job for six months. That means no paragraphs. No references to "see attached supplementary documentation." Step one, step two, step three. Contact this person. Press this button. Call this vendor. Check this gauge. If it can't be done in under thirty steps, break it into sub-procedures. I ran into a situation once where our recovery plan for a coolant system failure required replacing a specific filter cartridge. The part number was in the plan. The vendor contact was there. What wasn't there was the fact that the filter had been discontinued six months earlier and replaced with a different model that fit the same housing. The plan said to order the old part, wait four days for it to arrive, and watch the line stay dead the whole time. We ended up using a universal filter adapter we kept in the spare parts cabinet for unrelated jobs. The workaround worked, but nobody had updated the template in over a year. That's probably the single most common failure mode I've seen across every facility I've worked in. The plan exists on paper but doesn't reflect the current state of the shop floor.
Section 4: Communication Protocol
List every person who needs to be notified during an incident, in order, with their phone number, email, and alternate contact method. I mean actual phone numbers, not extensions. The person who gets called first when the PLC crashes at 11 PM is not necessarily the same person who should be notified at 7 AM the next day when you're assessing whether you'll miss a shipment deadline. Separate the urgent contact list from the notification list. They're different. I've seen plans where the emergency contact was the plant manager's direct line and the shift supervisor's cell number was nowhere to be found. Include your key vendors and contractors too. Equipment suppliers, spare parts distributors, temporary staffing agencies, waste disposal companies if your process generates hazardous material. When a hydraulic line bursts at 3 PM on a Friday, the person who can actually help might not be on your primary vendor list. You need the number for the company that services that specific make and model of hydraulic unit, not the generic equipment leasing office.

Section 5: Recovery Time Objectives
Define how long each critical process can be down before the impact crosses from inconvenient to catastrophic. This isn't a guess. It's based on your inventory buffer, your customer lead-time commitments, and your raw material shelf life. A food processing plant has very different RTOs than a precision machining shop. The food plant can't wait three days for a conveyor repair because the product in the line is perishable. The machining shop might have six months of finished goods in stock and can tolerate a week for certain repairs. The standard industry terminology here is RTO, RPO, and MTPD. Recovery Time Objective is how fast you need to be back up. Recovery Point Objective is how much data or process state you can afford to lose. Maximum Tolerable Period of Disruption is when the business actually ends. Most templates I've reviewed conflate these three or leave them out entirely. They're not optional sections. They're the framework that determines everything else in the document.
Section 6: Testing and Maintenance Schedule
A template without a testing schedule is a template that will become obsolete before you finish filling it out. Tabletop exercises once a quarter. Full simulation at least annually. After every incident, update the plan within two weeks. Not "soon." Within two weeks. The memory of what went wrong fades fast, and the people who lived through it move on to other projects. Here's the part most people skip: assign a named owner to each section of the plan. Not "the safety team" or "operations management." A specific person's name. When that person leaves, the new owner updates the relevant section within thirty days. I've seen plans where the contact for a critical chemical supplier was someone who retired four years earlier. The plan had the right structure. It just had dead links everywhere.
What This Template Won't Fix
A Business Continuity Plan Template For Manufacturing doesn't replace good maintenance practices. It doesn't fix chronic equipment failures or understaffing or supply chain fragility that no amount of paperwork will solve. If you're running a preventive maintenance program that skips more than twenty percent of scheduled jobs, your plan is going to look great on paper and fall apart in practice because the assumptions it's built on are wrong. It also won't help if your team doesn't know it exists. I've walked into facilities where the plan was stored on a server that went offline during the exact type of incident the plan was designed for. The server needed a manual reboot from a terminal in the basement, and nobody knew where the terminal was except the IT guy who wasn't on-site. Keep a printed copy at every supervisory station. Keep a digital copy on a cloud service. Keep it somewhere that doesn't depend on your primary network. The real value of a solid BCP template in manufacturing isn't the document itself. It's the conversation you have while building it. The production manager and the maintenance lead and the quality engineer sitting in a room figuring out exactly what happens when the CNC program corrupts mid-run and the backup workstation is already down. That conversation takes longer than filling out any template. But it's the only thing that actually prepares you for the incident.