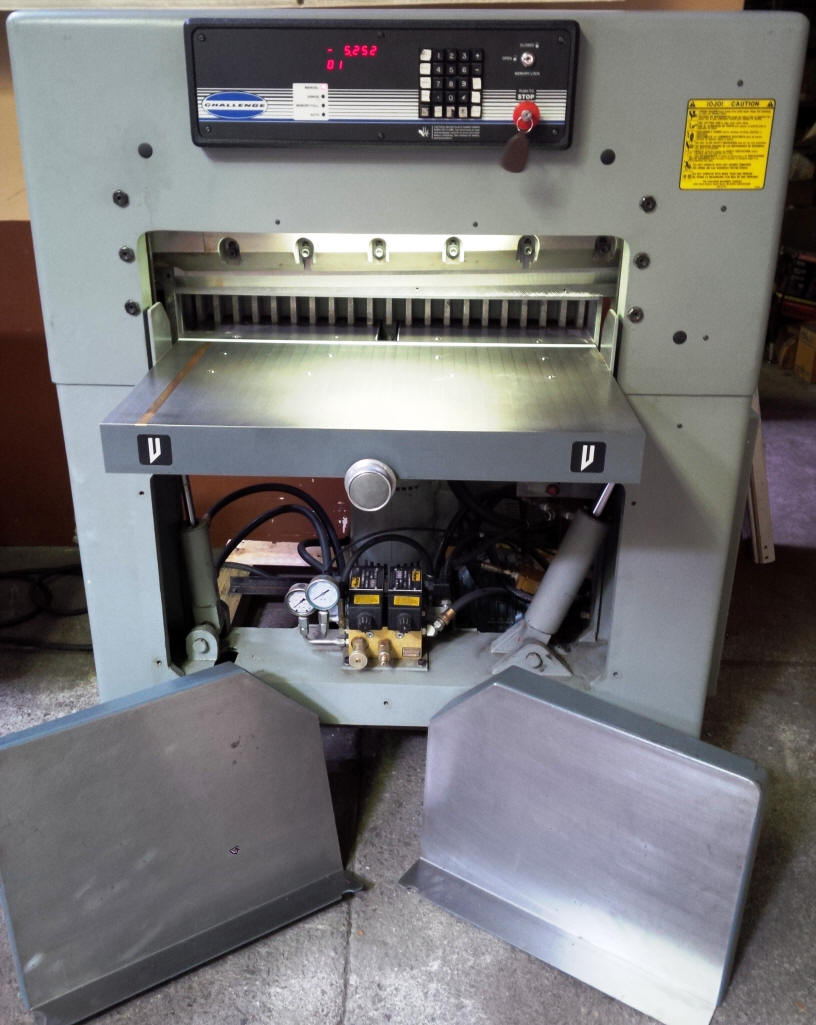
Getting the Challenge Mpx Paper Cutter Working Without Losing a Finger
The Challenge Mpx is a hydraulic trailing arm paper cutter you will find in a lot of commercial print shops. It is built like a tank, not exactly intuitive from the factory, and the manual that comes with it is a rough translation at best. Most of what operators actually need is not in that book. Challenge Machinery does not maintain a living website anymore. The original manual is archived and scattered across print industry forums and document hosting sites. Look for the file titled "Challenge MPX Series Operating Manual" or search for "Challenge Mpx Paper Cutter Manual" on industry sites like Printweek archives or specialized binding/cutting equipment groups on Reddit. The PDF is usually around 4-6 megabytes, mostly images with a few pages of actual text. You will need a PDF reader that handles scanned documents well because a lot of the pages are low-resolution photos of the machine. I will say this about the manual itself. It covers basic operation, blade change, and hydraulic bleeding. It does not cover common failure modes. If you buy one of these used like I did, expect to figure things out by reading the thing and watching how it moves.
How the Machine Actually Works
The Mpx is a hydraulic trailing arm guillotine cutter. You set your material against the back gauge, pull the clamp down to secure the stack, then pull the cutting arm toward you. The blade drops the last millimeter of the stroke automatically. The hydraulic cylinder sits under the table and provides the force. There is a foot pedal for the clamp and a manual lever for the cut. The back gauge moves via a handwheel on the right side. It has a digital readout on later models, but the early ones just have a scale. The scale is approximately accurate. For anything within two millimeters, trust the readout. Beyond that, measure a test cut and adjust. One thing the manual barely mentions is that the hydraulic system uses ISO 46 hydraulic oil, not 32 and not 68. I found this out the hard way when a shop in my area ran the wrong viscosity through a friend's Mpx in winter. The clamp was slow to engage, the arm dragged on the return, and the whole cycle took twice as long as it should have. Drained the reservoir, flushed it, filled with ISO 46, and the machine ran normally again. That was three years ago and we have not had another issue since.
Setting Up for Your First Cut
Before you run any material through, do this sequence. It takes about ten minutes and saves you from making bad cuts for the first hour. Check the blade sharpness first. The standard blade is a straight edge, roughly 500 millimeters long for the 1000 series. Look at the edge under a light. If you see any nicks or rolling, the cut will be rough and you will need to index or replace the blade. Rotate the blade to a fresh edge by loosening the two cap screws on either end, sliding it forward, and retightening. Do not overtighten. Hand snug plus a quarter turn is enough. Next, check the clamp pressure. With the machine off, pull the clamp lever down and hold it. It should meet firm resistance. If it feels soft or spongy, the hydraulic system needs bleeding. Open the bleed screw on the clamp cylinder, pump the clamp lever a few times until fluid comes out clean without bubbles, then close the screw. This is documented in the manual but the diagram is too small to read clearly.
Get the Full Details

Set the back gauge to your desired measurement. Run a test piece of scrap paper through, cut it, measure it, and adjust. The gauge has a slight play in it that varies by model year. Earlier machines tend to have more slack in the worm drive. If your readout says 210 millimeters and your actual cut comes out 208, that is normal wear, not a malfunction. Compensate by measuring a known width and noting the offset.
The Problem I Ran Into and How I Solved It
Last year I was running a batch of 300-lb cover stock on a Challenge Mpx 1100 and the clamp would not hold the stack down during the cut. The material would shift about four millimeters before the blade even touched it. The hydraulic pressure was fine, the clamp pads were in good shape, and the manual had nothing useful beyond "check hydraulic fluid level." The issue was the clamp shoe was worn on the bottom edge. Not the pad, the actual metal shoe. After years of use, the leading edge of the clamp developed a flat spot where it met the paper, and that flat spot was catching the top sheet instead of pressing it down evenly. I resolved it by placing a thin layer of vulcanized rubber shim material under the existing clamp pad, which restored even pressure distribution across the stack. A few cuts later and the shifting stopped completely. This is not something anyone writes about in the manual. You only learn it by seeing the machine fail.
Blade Replacement Procedure
Remove the two end cap screws. Slide the old blade out. Wipe the blade channel clean with a cloth and some mineral spirits if there is paper residue or adhesive buildup. A dirty channel is what causes blade wobble, and blade wobble is what causes jagged edges on the cut. Insert the new blade ensuring it sits flat against the bottom guide, not tilted. Tighten the cap screws finger-tight, then use a wrench and give each one a quarter turn alternately. Do not crank them down hard. The blade expands slightly when it gets warm from friction during cutting, and overtightened screws bind it and cause premature dulling. A standard blade costs between thirty and sixty dollars depending on thickness and coating. Carbide-coated blades last roughly three to four times longer than uncoated on heavy stocks. If you are cutting more than a few reams a day, the coated blades pay for themselves within a month.

Hydraulic Maintenance Schedule
The manufacturer recommends changing the hydraulic fluid every two years or 2,000 cycles, whichever comes first. In practice, if the machine is in a dusty environment like a bindery that also handles glossy sheet stock, change it every year. Dust gets into the reservoir vent and degrades the fluid over time. The fluid level should be checked weekly through the sight glass on the side of the reservoir. Keep it at the center line, not at the top. Overfilling causes leakage past the seals when the fluid heats up during operation. The filter inside the reservoir is a simple mesh screen. Remove it during each fluid change and wash it in solvent. If it is torn or excessively clogged, replace it. These screens are generic and available from hydraulic supply houses for about five dollars. I have seen shops run their Mpxes for years without ever touching this filter and then wonder why the clamp pressure drops after a long run.
Common Mistakes That Will Damage the Machine
Clamping and cutting oversized stacks beyond the rated capacity is the fastest way to bend the arm. The Mpx 1100 is rated for about 100 millimeters of cut capacity depending on paper density. If you push 120 millimeters through regularly, the arm will flex and you will start getting uneven cuts across the width. You will not notice it immediately because the first few inches will look fine, then the far edge will be off by a millimeter or two. By the time you realize what is happening, the arm is already bent and replacement is the only fix. The second mistake is using the machine as a measuring station. Some operators rest their pencil or marking gauge on the table near the blade path. One stray mark from the blade and you have a new scratch in the cast iron table. Those scratches eventually catch on material and cause registration errors. Keep the table clear. A third one that is worth mentioning because it seems minor: never leave the clamp down when the machine is idle for extended periods. The constant pressure on the hydraulic seal leads to premature seal compression and slow leaks. Raise the clamp when you are done for the day. It takes two seconds and extends seal life significantly.
What the Manual Does Not Tell You
The hydraulic schematic in the manual is labeled with part numbers that do not match current catalogs. Challenge Machinery reorganized their numbering system around 2015 and the printed diagrams were never updated. If you need to order a seal kit or a specific valve, reference the serial number plate on the side of the reservoir housing and call a parts dealer directly rather than cross-referencing the manual. The serial number is stamped into a metal tag near the hydraulic pump. You will need it for any parts order. Another thing left out entirely is the procedure for resetting the back gauge encoder on digital models. If the power goes out or the machine is moved, the digital readout can lose its zero reference. The fix is simple but not documented: turn the machine on, move the back gauge all the way to the left stop, hold it there for five seconds while powering on, then release. The display should reset to zero. If it does not, check the encoder cable connection behind the handwheel assembly. It is a Molex connector that works loose over time from vibration.

Limitations You Should Know About
The Challenge Mpx is not a precision cutter in the same class as a Regal or a Polar. The tolerances are acceptable for general production work, maybe plus or minus half a millimeter on a full run, but if you need sub-millimeter registration you will need to calibrate the gauge per batch and verify with test cuts. The trailing arm design also means the cut angle varies slightly depending on blade sharpness and material thickness. A fresh blade on standard text weight gives a clean square cut. The same machine cutting 200-pound cover with a worn blade will produce a cut that angles slightly toward the operator. Not enough to reject the job, but enough to notice if you are holding tight specs. For high-precision work, a beam cutter or a rotary trimmer is the better tool. The Mpx is designed for speed and volume, not micro-adjustment. It excels at breaking down large sheets into manageable increments and handling bulk stacks efficiently. What it does not do well is delicate single-sheet trimming where every tenth of a millimeter matters. If you find yourself running a lot of jobs that require extreme accuracy, consider pairing the Mpx with a digital caliper gauge or a laser positioning system. These are aftermarket additions and the wiring can be finicky on older machines, but they do improve consistency noticeably. I installed a basic digital position indicator on one of our Mpx 850s about four years ago. It cost around two hundred dollars and reduced our setup time for repeat jobs from about eight minutes down to two or three. The initial investment paid for itself in the first month of saved labor.
")