Getting Channel Letters Bended Without Losing Your Mind
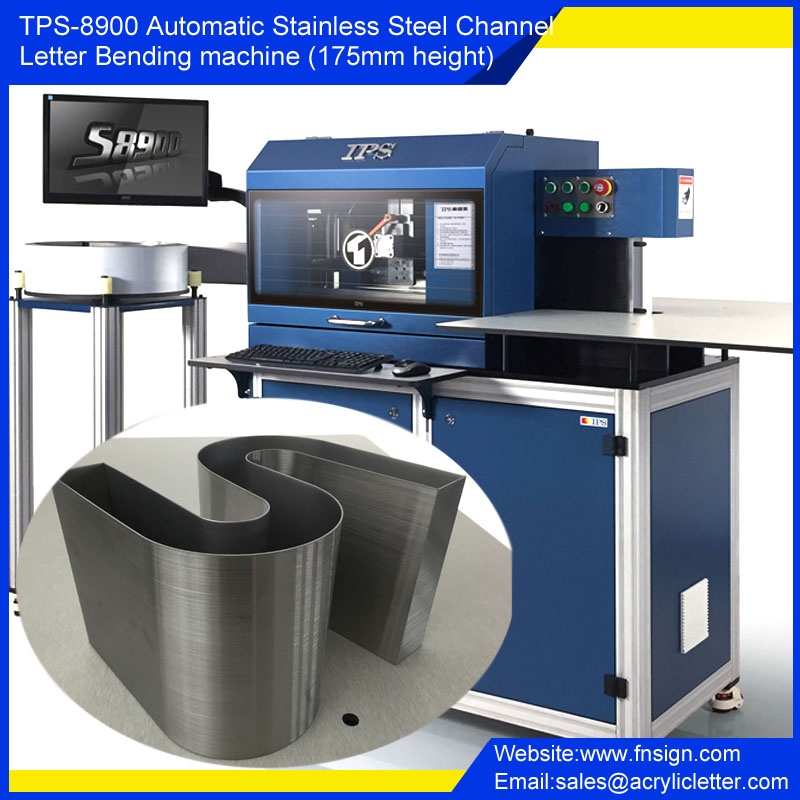
A channel letter bender is a machine, a tool, or a jig that takes flat aluminum or steel coil stock and bends it into the three-dimensional box shapes that make up channel letters for exterior and interior signage. Some are hydraulic press brakes with custom dies. Others are manual brake setups built from angle iron and locking pliers. The cheaper ones are also called letter benders or slot-and-fold benders, and they all do the same basic thing: they hold a strip of metal, make precise bends at calculated intervals, and let you form a face, return, and soffit without hand-forming every corner. I spent years running a sign shop on the East Coast before moving to fabrication consulting, and the single most consistent headache I saw was people buying the wrong bender for their volume, or worse, trying to force a manual bender to do production work it wasn't built for. Let me walk through how this actually works on the floor, where things go wrong, and what to look for if you're setting up or upgrading.
Channel Letter Bender: How It Actually Works
The process starts with a flat pattern. You take the dimensions of your letter, account for the material thickness and bend radius, and lay out where each fold line goes. A typical 6-inch channel letter made from .040 aluminum with a 3/8-inch bend radius will have a face dimension, two return heights, and a soffit width. Your bender needs to hold that strip, apply force at exactly the right locations, and ideally give you repeatable angles. Most benchtop benders use a fixed male die and a female receiver. You slide the pre-cut blank into the tool, lock it down, and pull or press down on a lever arm. The metal wraps around the die, creating the bend. More expensive CNC benders automate this with programmable stops and multiple bending stations, which matters when you're running 200 letters a week instead of 10 a month. The critical detail nobody mentions upfront is the K-factor. This is the neutral axis shift that happens when you bend metal. On .040 aluminum, the bend adds approximately .040 to .060 inches of effective length per 90-degree bend depending on your die geometry and material temper. If you ignore this and calculate your flat pattern by simply adding face plus returns plus soffit, every letter will come out too short. I had a guy email me last year showing me letters that were a quarter inch undersized across the board. We recalculated using a proper bend allowance table and the second run was perfect. Spend two hours learning bend deduction math before you cut a single foot of material. It will save you hundreds in scrap.
Material choice matters more than most operators realize. 5052-H32 aluminum is the standard for a reason. It has good formability, holds its shape after bending, and doesn't spring back excessively. Some shops try to save money using 1100-O temper, which is softer and easier to bend by hand, but the letters don't hold their squareness and will drift over time, especially in temperature changes. Then there's 6061-T6 aluminum, which is way too hard for most benchtop benders and will crack at the bend if you push it. And don't get me started on stainless steel unless you have a hydraulic press rated for it and experience with work hardening. It doubles your cycle time and eats your dies. Here is a practical problem I ran into repeatedly that probably isn't in any manual. When you're bending wide letters, say 18 inches or taller, the return flanges tend to bow outward slightly during the bend because the material wants to twist. The fix isn't to hammer it back. That warps the face. Instead, I designed a simple auxiliary support bar that rests on the bench and contacts the return about two inches from the bend line. It keeps the flange from rolling as you apply force. Made it from a piece of 1x2 aluminum channel, drilled three mounting holes, and clamped it to the work surface. Cost about eight dollars in materials and solved a problem that was eating up twenty minutes of correction per letter.
Get the Full Details

Choosing the Right Setup for Your Volume
If you're doing fewer than fifty letters per month, a manual brake with interchangeable dies or even a well-built custom jig will handle it. You are trading time for money, but at low volume the math works. You spend maybe thirty to forty-five minutes per letter forming by hand, but your tooling cost stays under a thousand dollars. At fifty to two hundred letters per month, a powered bender makes sense. These usually have a hydraulic or pneumatic ram with quick-change die sets. Cycle time drops to about five to eight minutes per letter, and the consistency is significantly better because you're not relying on human force application. Expect to spend three to six thousand dollars for a decent used unit, or eight to fifteen thousand new. The sweet spot is usually a used unit from a shop that upgraded and knows it was well maintained. Above two hundred letters per month, you're in CNC territory. These machines automate the entire bending sequence. You load a flat pattern file, the machine indexes through each bend station, and the operator just monitors. Cycle time can be under two minutes per letter for standard sizes. Tooling cost runs fifteen to forty thousand dollars depending on capacity and features like automatic material handling. The ROI only works if you have the volume to justify it, which most small sign shops don't. I see too many owners buy these thinking they need to compete on price. They don't. They need to compete on turnaround time and consistency, and a mid-range powered bender with a good operator beats a poorly managed CNC any day.
Dies are where the hidden costs live. Every different return height and material thickness combination may require a different die set. A full die library for a single bender can run two to four thousand dollars. Some manufacturers sell universal dies that cover a range of letter heights, but they compromise on bend accuracy at the extremes of that range. I recommend starting with the die sets for your most common letter sizes, then adding specialty dies as jobs demand them. Don't buy every die the manufacturer offers upfront unless you have a committed order book that proves you'll use them.
Common Pitfalls That Waste Time and Money
Springback is the first thing that will bite you. Aluminum doesn't fully recover after bending, but it does recover enough to throw off your angles. A bend that looks like 90 degrees when you release the bender might settle to 87 or 88 degrees after a few minutes. The workaround is to slightly overbend, typically by one to two degrees past your target angle, and then check with a square after the metal has relaxed for about thirty seconds. I keep a digital angle finder on the bench for this. It costs forty dollars and has saved me from reworking whole batches of letters. Scratching and marring the face of the letter is extremely common, especially with polished or painted finishes. The bender jaws contact the material during the bend, and if there's any debris or worn pads on the contact surfaces, you'll leave marks. The solution is simple: use protective film on the die faces and always lay down a scrap piece of soft aluminum or nylon between the jaw and your finished material. I also recommend ordering dies with polished or anodized contact surfaces rather than raw machined aluminum. The difference in surface finish transfer is dramatic. Bending sequence matters more than you'd think. For a standard rectangular channel letter, the recommended order is: first bend one return, then the opposite return, then the soffit, and finally close the face. If you bend both returns first, the soffit bend can cause the returns to twist out of alignment. I learned this the hard way on a batch of 48 letters where I bent in the wrong order and spent three hours truing them up with a mallet and a flat surface. Reordered the bends and the next batch of 48 took twenty minutes.

Coil stock versus cut blank is another decision point. Coil stock feeds continuously and is more economical per foot, but it requires a decoiler and a leveler, which adds footprint and setup time. Cut blanks are slower to handle individually but give you more control and require less equipment. For a shop doing a mix of custom letters and standard sizes, I'd recommend starting with cut blanks. You can always add coil handling later if the volume justifies it.
What to Do When the Bender Won't Cooperate
Sometimes the tooling just doesn't work for a particular job, and you need to adapt. I had a project last winter where we needed to form channel letters from .063 aluminum because the client specified a heavier gauge for wind load resistance. The manual bender we were using was rated for up to .050, and every bend was cracking near the edge. Rather than renting a larger press brake for what turned out to be a 12-letter job, I split the bend. I made the first bend at about 80 degrees, then came back and finished it to 90. The material had work-hardened from the first pass but was still formable, and the second pass completed without cracking. It took twice as long per letter but eliminated the scrap that would have resulted from forcing it in one bend. Another issue that comes up occasionally is inconsistent material thickness across a coil or batch. Some suppliers ship .040 that actually measures .037 to .043 depending on where you sample. This variation changes the bend radius and the final letter dimensions. The workaround is to measure every coil before you start bending and adjust your die spacing accordingly. It sounds tedious but a single micrometer measurement at the start of a job prevents an entire batch from being out of tolerance. If you're running a Channel Letter Bender and the bends are consistently off, check your stop blocks before you blame the machine. Most issues trace back to material not seating against the stops consistently. Clean the stops, make sure they're square to the bending axis, and verify that the operator is laying the blank down the same way every time. Inconsistency in loading causes more bad parts than any mechanical failure I've encountered in twenty years of this work.
Where to find resources and parts: Most bender manufacturers have technical documentation, die catalogs, and replacement parts on their websites. Sign supply companies like National Sign Supply, Sign Supply Group, and various regional distributors carry both OEM and aftermarket bender tooling. Online forums like SignForum and the sign-making sections of Reddit still have active discussions where experienced operators share setup tips and troubleshooting advice. For flat pattern calculators, several free options exist online, but nothing beats building your own spreadsheet with your specific material thicknesses and bend radii factored in. Custom bend tables tend to be more accurate than generic ones because they account for your actual tooling geometry. That is basically how channel letter bending works in practice. It is not particularly glamorous, and most of the learning comes from making mistakes and adjusting. The tools are straightforward. The skill is in understanding how the material behaves and developing consistent habits around setup, bending sequence, and quality checks.


