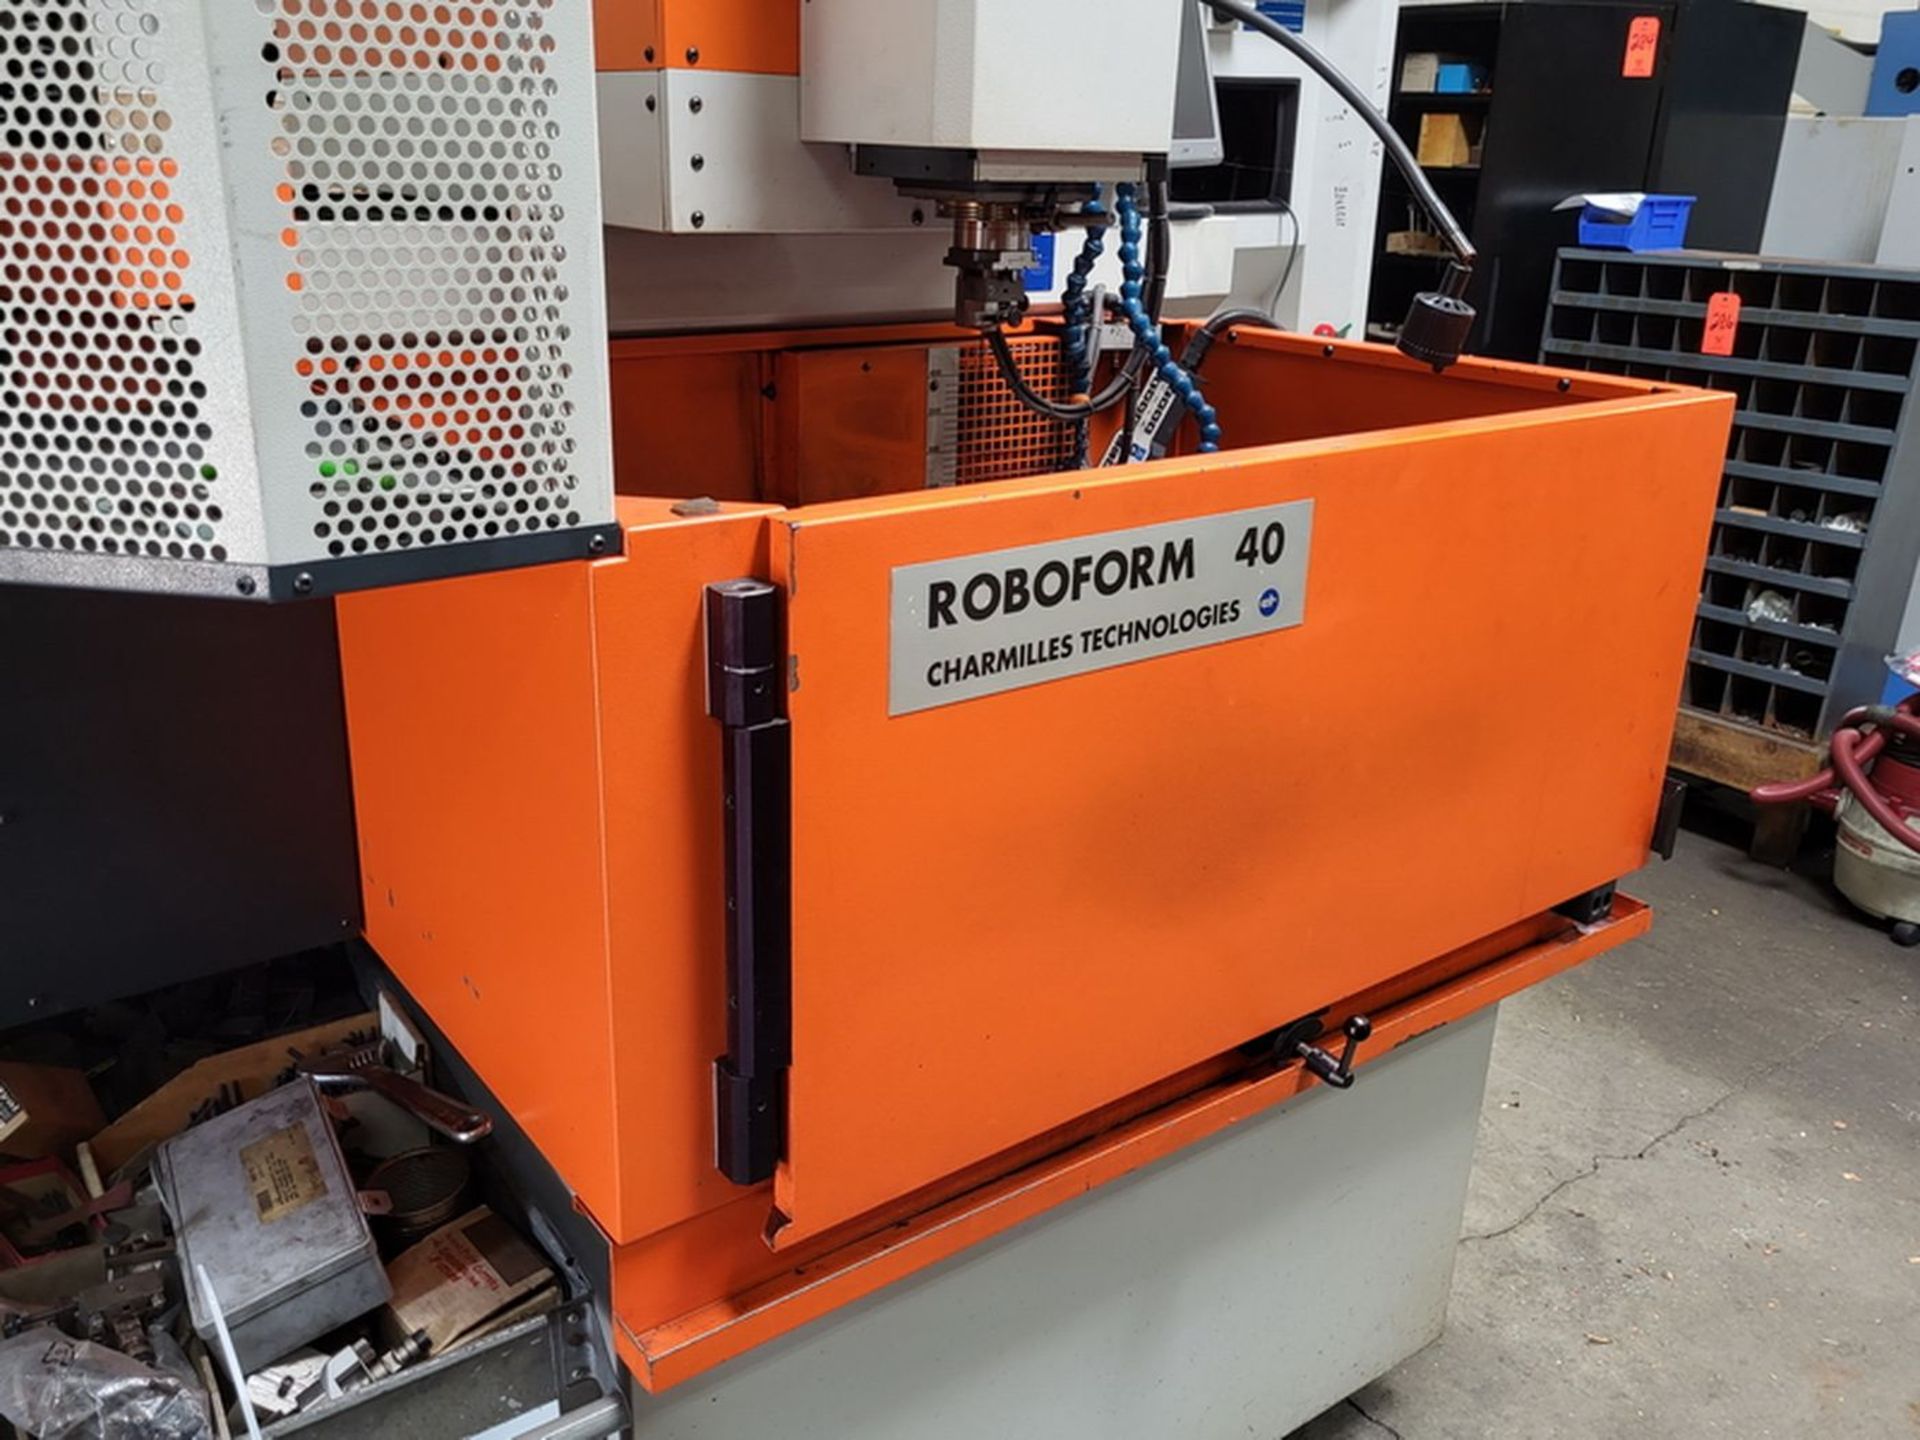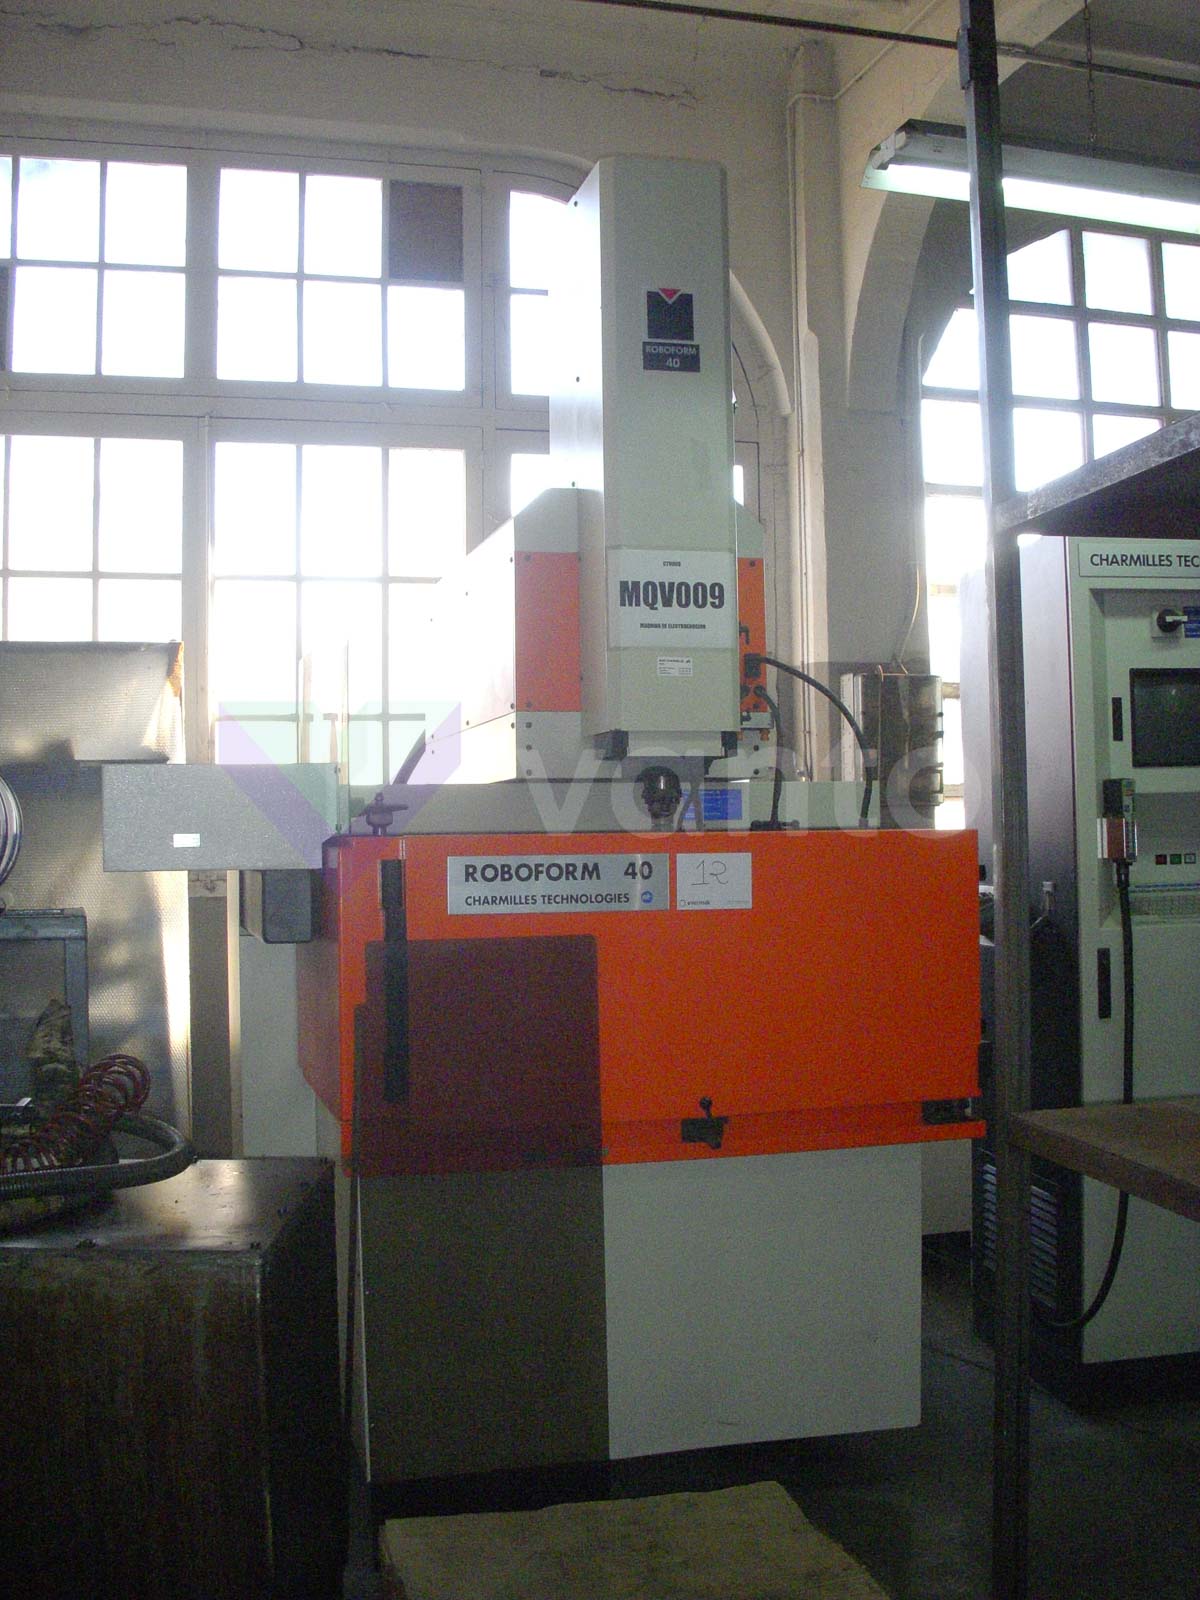
Getting Your Head Around the Charmilles Roboform 40
The Charmilles Roboform 40 is a wire EDM machine that Charmilles (later become part of AgieCharmilles, then GF Machining Solutions) made back in the late 90s and early 2000s. It was their workhorse for medium-precision wire cutting. If you have one running in your shop and you need the manual, good luck finding an original paper copy. They are out of print andGF has archived most of the old documentation. Here is what you actually need to know about it. The most reliable source right now is the GF Machining Solutions archive. They moved their legacy documentation to a portal that requires free registration. You can find it by going to gf-machining-solutions.com, navigating to Support, then Documentation, and searching by machine series. The Roboform falls under the Wire EDM category. If that route fails for some reason, secondhand markets like eBay or used-machine dealer sites occasionally list digitized PDFs, but the quality of those scans varies wildly. Some are complete, some are missing the electrical schematics section. There is also a Usenet archive where someone uploaded a ~40MB PDF of the full operator and maintenance manual around 2012. It is not officially endorsed by GF, but it covers the R-40 control system, electrode tension setup, dielectric fluid circulation, and the standard maintenance intervals. The index at the front is broken in places, so I usually just search the PDF for the specific section I need rather than flipping through the table of contents.
What the Manual Actually Covers
The Roboform 40 uses the Charmilles ACOMAT control system with a touchscreen interface. The manual is split into several functional blocks. The operator section handles daily startup procedures, wire threading, workpiece setup, and basic programming through the built-in CAM post-processor. The maintenance section breaks down the wire guides, tension assembly, tank drain-and-fill cycle, and dielectric filter replacement schedule. The troubleshooting section is honestly the most useful part because it maps error codes to likely causes. Error code E-27, for instance, is a wire break detection fault that most people immediately blame on the upper guide bearing, when it is often just the sensing electrode gap being too wide after a routine cleaning. I spent three years running a Roboform 40 before moving to a newer AgieGemini. One thing the manual does not emphasize enough is the wire tension calibration procedure. The spec says 180 newtons for 0.30mm brass wire, but in practice you need to adjust based on your material thickness and cut speed. When I was cutting hardened tool steel at 400 HV around 8mm thick, running at the rated tension caused excessive wire whip and a rough surface finish. Dropping the tension to about 150 newtons and slowing the feed rate by roughly 15 percent gave me a clean Ra of around 0.8 micrometers instead of chasing 2.5. The manual mentions the tension range but does not walk you through the tradeoff between stability and cutting efficiency in any real detail.
Common Maintenance Issues the Manual Misses
The dielectric fluid system on this machine is a closed loop with a recirculation pump and paper-band filters. The manual tells you to change the filters every 200 hours and flush the tank every six months. That is correct for light production. If you are running continuous overnight shifts cutting abrasive material like composite or carbide, those intervals drop to roughly 80 hours for filters and monthly for flushing. I learned this the hard way when a clogged filter caused the tank pressure to drop below the minimum threshold during a 12-hour cut. The machine shut down with a pressure fault code and left an incomplete cut surface that required re-setup and re-measuring. After that, I tightened the filter schedule without waiting for the manual interval to arrive. Another thing nobody warns you about is the upper and lower guide assembly wear. The diamond guides on the Roboform 40 are replaceable but not cheap. After about 3,000 to 5,000 cutting hours, the inner diameter starts to widen enough that wire tracking becomes inconsistent. The control system has a wire tracking adjustment parameter, but it can only compensate so much before the guide itself needs replacement. I replaced the upper guides on my machine at around 4,200 hours and the surface finish improved immediately on subsequent cuts, even though the machine had not thrown any errors or warnings about guide wear. The manual lists guide inspection intervals but does not tie them to measurable surface finish degradation.
Get the Full Details
Programming and Post-Processing Notes
The ACOMAT control runs a proprietary CAM environment. If you are programming externally and sending G-code via USB or network, you need to use the correct post-processor. Charmilles supplied a generic wire EDM post for Esprit, and GF later updated it for PowerMill. The robot file format they use is .RFB. Getting the post right matters because the Roboform 40 expects specific command syntax for pulse parameters, wire offset compensation, and arc start-stop routines. A malformed arc command will cause the machine to either alarm out or make an incorrect compensation pass, and neither situation is obvious until the part is already cut. One practical tip that the manual buries somewhere in the programming appendix: you can set a lead-in distance of as low as 2mm for tight clearance cuts, but anything below 3mm on materials thicker than 10mm tends to leave a small uncut island near the entry point due to the initial pulse stabilization period. The workaround is either increasing the lead-in slightly or using a pilot hole if your part geometry allows it. This applies to through-cut operations primarily. Perforation cuts behave differently and the manual covers that in a separate section that most operators skip.
The Real Limitations of This Machine
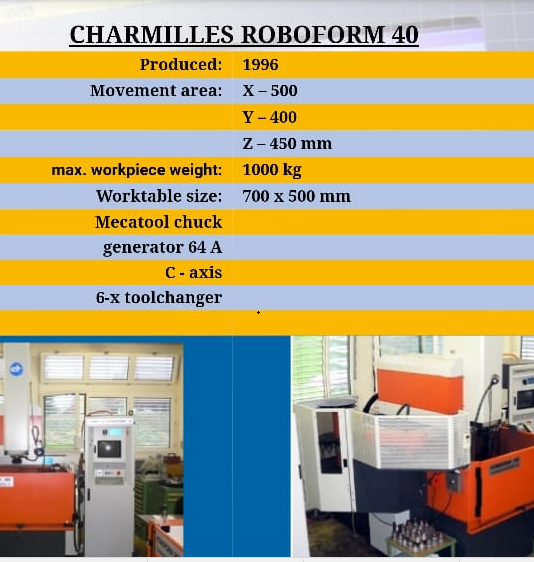
The Roboform 40 is a solid machine for its era, but it has clear bottlenecks. The table travel is 400mm by 300mm, which means anything wider than that requires a second setup or a different machine entirely. The maximum workpiece height is 300mm, and the taper range is plus or minus 5 degrees. That sounds adequate until you need a compound taper on a thick part, at which point you will notice the lower guide assembly struggling with angular stability past 3 degrees on heavy cuts. The machine is also notoriously slow on thick-section roughing passes compared to newer generation wire EDMs. If you are cutting 50mm stainless at full speed, expect it to take roughly twice as long as a modern AgieCut or Mitsubishi system would. Another honest limitation is the spares situation. Charmilles parts are no longer manufactured as a standalone line. GF sources some components through their legacy parts division, but lead times for things like control board replacements, touchscreens, and certain sensor assemblies can stretch to eight to twelve weeks. I had a machine down for nearly three weeks once waiting on a replacement ACOMAT control module. Keeping a backup of the control parameters and machine settings on an external drive is genuinely important because if the control fails and you do not have a recent backup, you are rebuilding the entire machine configuration from scratch. The manual includes a parameter backup procedure, but it is easy to overlook during a rush. If you are considering using this machine for high-volume production, it can handle it, but you need to budget for downtime related to guide wear and older electronics failures. For toolroom work, prototyping, and low-to-medium volume production, it remains capable. The key is understanding what the manual does not tell you about wear patterns, setting realistic maintenance intervals based on actual usage, and keeping your machine parameters backed up. That is the practical reality of working with equipment that is over two decades old now.