
What You Actually Need Before You Start Pouring Resin Into Keycap Molds
Most people start with the assumption that making keycaps at home is just about buying some UV resin and a silicone mold. That works for three caps before they realize the tolerances required for a keyboard to actually function are brutal. A single keycap needs to sit within maybe 0.1mm of its intended position, and that includes the stem that clips onto the switch, the dome it rests on, and the overall profile. If you have ever pulled a finished cap off a mold only to find the stem flexes too much and the switch feels mushy, you already know why this checklist exists. Materials and tools: UV-cured resin (preferably low-viscosity, around 500-800 cP at 25°C)
Silicone molds, single-cavity or multi-cavity depending on batch size Isopropyl alcohol 90%+ for degreasing Microfiber cloths, lint-free
UV cure station or a 405nm LED lamp, minimum 30W output per square centimeter of surface area Digital calipers (0.01mm resolution) Pin vise or fine rotary burrs for stem trimming
Get the Full Details

Masking tape or low-tack painter's tape (for handling uncured pieces) Post-cure oven or continued UV exposure rig Surface preparation: acetone for ABS/PBT test samples, or isopropyl for resin-only workflows
I spent about six months burning through resin before I stopped getting stems that were too short. The issue was not the mold. It was that I was not accounting for resin shrinkage during cure. Most manufacturers list a shrinkage rate between 2-4% linearly. That means a 14.5mm tall keycap might shrink down to 14.1mm or worse, and when it clips onto a Cherry MX-compatible stem, it sits 0.3mm too low. The fix was simple: I started designing my molds at 15.0mm with the stem length dimensioned at 15.2mm instead of the standard 14.8mm. After the first cured batch, I measured everything and adjusted downward from there until the fit was acceptable. It took three iterations and roughly $40 in wasted resin. Pre-pour surface prep:
Clean silicone molds with IPA and let them dry completely. Any residual oil from handling will cause pinholing along the dome surface. Inspect the mold cavities under bright light at a 45-degree angle. Even tiny dust particles left from the last pour will create a bump on the keycap bottom that prevents flat seating. Warm the mold slightly before pouring. A hair dryer on low for about 20 seconds brings the silicone to around 30°C, which reduces resin viscosity just enough to let it flow into the corners without agitating air into the mix.

Making Custom DIY Resin Keycaps: Making Space Themed Keycaps - YouTube Mixing and degassing: Measure resin and hardener by weight, not volume. A cheap digital scale accurate to 0.01g removes the guesswork. The ratio is usually 1:1 by weight for most DIY UV resins, but check the batch datasheet because some formulations vary. Stir slowly for at least 90 seconds. Fast stirring introduces microbubbles that survive the pour and cure as visible defects on the keycap surface. I learned this the hard way on a batch of 10 caps where six had tiny white specks you could see even after sanding.
If you have access to a vacuum chamber, degas at -0.8 bar for 3 minutes. Without one, let the mixed resin sit undisturbed for 5-8 minutes after stirring to let bubbles rise to the surface. Skim them off with a toothpick before pouring.
- /p
Pouring technique: Pour from a height of about 5cm into the center of the cavity. This breaks the stream and reduces air entrapment compared to placing the nozzle directly against the mold wall. Fill each cavity slowly. Do not overfill past the rim. The resin will self-level and settle into the stem channel on its own.
Tap the mold gently against a soft surface three times after filling to dislodge trapped air. One tap is never enough. Four taps is excessive and risks shifting the mold on your work surface. Curing: UV cure for 3-5 minutes per side under a 405nm lamp at the recommended intensity. Flip the mold halfway through. Undercured resin remains tacky and will degrade within weeks. I once finished a full custom set and used them for two weeks before the stems became brittle and cracked under normal typing force. The caps looked fine. They failed internally.

Post-cure in a warm environment at 60°C for 10-15 minutes if possible. This completes the cross-linking and improves hardness. Skipping this step saves about 15 minutes but reduces the glass transition temperature of the finished piece by roughly 10-15°C. Demolding and finishing: Pry the cap from the mold edge using a plastic spudger or thin fingernail. Metal tools scratch the dome. Start at the stem area where the wall thickness is thinnest.
Inspect the stem bore with a magnifying glass. If the burr from the mold seam is visible inside the bore, remove it with a fine needle file or a 0.5mm carbide burr in a pin vise. This takes about 30 seconds per cap. Test fit each cap onto your switch before considering the batch done. Click it on and press down. It should seat flush with no wobble. If it rocks, the stem is too wide and needs careful filing. If it slides off too easily, the stem is undersized and the cap is unusable for typing. Quality check before committing to a full set:
Measure the stem height with calipers. Compare against your switch specifications. Cherry MX stems require 14.8mm ±0.2mm from the underside of the cap to the top of the stem bore. Check the dome height. Typical profiles range from 11mm (low) to 14mm (tall). If your measurement is off by more than 0.5mm from the intended profile, the typing experience will feel inconsistent across the set. Test the finish durability. Run your fingernail across the dome surface. If it scratches easily, your cure time was insufficient or the resin formulation is too soft. Most DIY cured resins should resist light scratching under normal fingernail pressure.
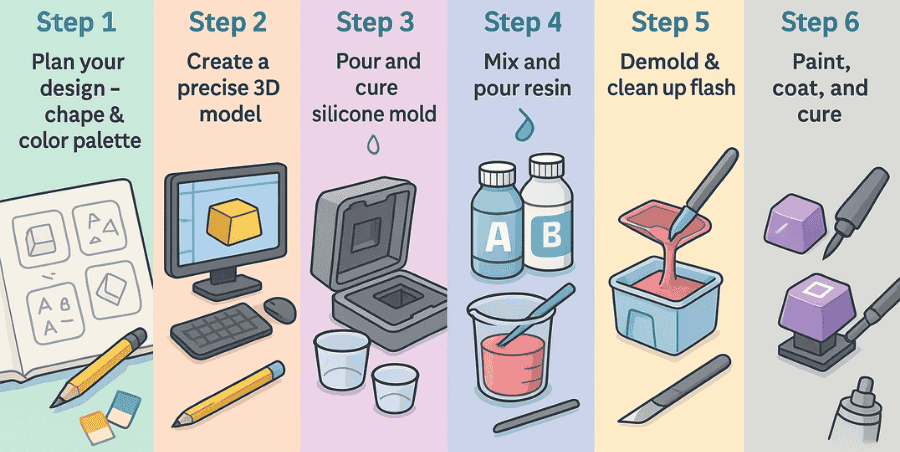
There are real limitations to this approach that the hobby literature rarely mentions. The primary one is consistency. Even with careful technique, you will get variance between individual caps in a single pour. A well-made commercial injection-molded set has stem dimensions that vary by less than 0.05mm across hundreds of pieces. Hand-poured resin caps typically vary by 0.2-0.4mm. This matters most on the spacebar and enter key where stem alignment is critical. If two stems on a wide key are even slightly different heights, the key will tilt under your finger and feel unstable. Another problem is resin yellowing. Cheap UV resin exposed to ambient light will turn amber within 6-12 months. If you want lasting color stability, you need resin with UV stabilizers rated for that purpose, which costs roughly 40-60% more per liter. The workaround I use is applying a thin clear coat of scratch-resistant spray after curing. It adds a layer that slows UV degradation, though it also changes the tactile feel of the dome slightly. For people who find the manual pour method too inconsistent, the alternative is CNC-milled acrylic keycaps. They are machined from solid rods and require no resin, no curing time, and produce stems that are dimensionally consistent to within 0.02mm. The downside is the upfront cost of equipment and the time per cap, which is closer to 10-15 minutes per piece on a basic 3-axis mill. If you are making ten caps, hand-pouring is faster. If you are making fifty or more, the mill pays for itself in consistency alone.
The one edge case I have not seen discussed anywhere is the interaction between resin and switch spring material. Some switches use uncoated steel springs that can react with residual uncured monomers on the keycap stem over time, causing a greenish deposit inside the bore after several months. It does not affect function, but it is visually unpleasant and difficult to clean out. I discovered this on a set of black PBT keycaps I paired with a batch of switches from a budget manufacturer. The fix was simply wiping the stem interior with IPA before installation and using switches with coated springs, which are available from most mid-tier keyboard component suppliers at a modest premium. This process will get you functional custom keycaps. It will not get you results that match industrial manufacturing quality, and for most users that gap is acceptable. The real value is in the ability to experiment with shapes, colors, and profiles that do not exist in the commercial market without paying a premium for a limited-run group buy.

