What Actually Happens When Food Gets Processed
Most people think food engineering is just recipes scaled up. It isn't. The real work starts where you can't taste the product anymore and every variable becomes a number on a spreadsheet. I spent years working on continuous pasteurization lines and downstream separation, so I'm going to skip the textbook definitions and tell you what the job actually looks like. Chemical engineering in the food industry is the application of unit operations to food materials. Heat transfer, mass transfer, fluid mechanics, and separations form the core toolkit. But food materials are messy. They're non-Newtonian, they change phase, and they degrade under conditions that work fine for petrochemical streams. That difference matters more than anything else you'll read about this topic.
Chemical Engineering In Food Industry: The Real Scope
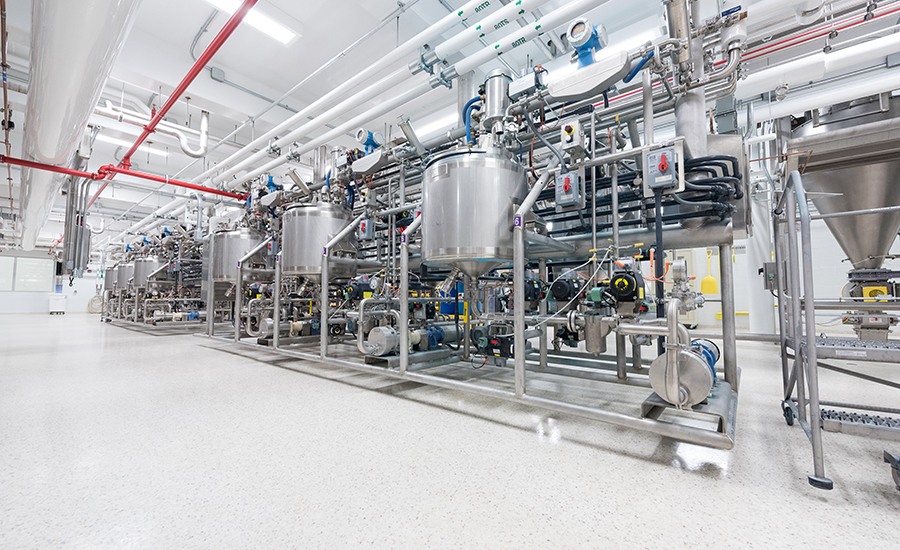
The scope covers everything from upstream ingredient preparation to final packaging. Processing steps include milling, extraction, concentration, pasteurization, sterilization, fermentation, drying, and extrusion. Each of these relies on the same fundamental equations that govern any chemical process, but the boundary conditions are completely different because you're dealing with biological matter rather than refined hydrocarbons. Downstream processing is where most projects live or die. Separating proteins from whey, clarifying fruit juice, recovering essential oils, or removing water from a slurry to reach shelf stability. These aren't glamorous operations. They're unit operations that require precise control over temperature, pressure, flow rate, and residence time distribution. Get any one of those wrong and you lose product yield, create a safety hazard, or produce something that tastes like cardboard.
Unit Operations You Actually Use
Heat exchangers are everywhere in food processing. Plate heat exchangers handle most pasteurization work because they're easy to clean and open for inspection. Shell and tube designs show up in high-viscosity applications where plate channels would clog. The trick isn't picking the right exchanger type. It's understanding fouling. Milk protein deposits on heat transfer surfaces at a rate that depends on temperature, pH, and how long the product sits at elevated temperatures before the next cleaning cycle. I've seen lines drop from 85 percent thermal efficiency to under 60 percent in a single shift because someone adjusted the preheating zone by three degrees without recalculating the CIP schedule. Centrifuges separate components by density difference. Horizontal bowl centrifuges clarify apple juice. Disc stack centrifuges separate cream from milk. The counter-intuitive part is that flow rate isn't the main control variable. G-force and pool depth determine separation efficiency far more than throughput. Running a disc stack at maximum rated flow while under-gravitating it will give you cloudy filtrate and a lot of wasted energy. Run it at 70 percent flow with proper bowl intensity and you'll get cleaner product with less fouling. Evaporation and concentration remove water under reduced pressure. Multiple-effect evaporators reuse vapor from one stage as the heating medium for the next stage. A typical four-effect system uses one kilogram of steam to remove roughly three point five kilograms of water. The limitation is thermal degradation. Heat-sensitive compounds like vitamin C or certain flavor volatiles break down faster than you'd expect from Arrhenius calculations alone because they concentrate as water leaves the system. The local concentration at the heating surface can be two or three times the bulk concentration, and that changes the degradation kinetics completely.
Get the Full Details

Fluid Behavior That Breaks Your Assumptions
Food fluids rarely behave like water. Tomato paste follows a power law model with a flow behavior index around 0.3. That means it's strongly shear-thinning. Pump selection matters enormously here. A centrifugal pump rated for water will perform completely differently with tomato paste, and the head-flow curve you pull from the manufacturer's catalog is useless unless they tested it with your specific product at your target concentration. Pipe velocity calculations need to account for apparent viscosity, not just density. Reynolds number in non-Newtonian systems requires a modified definition. The Metzner and Otto approach works for stirred tanks. For pipe flow, the Rabinowitsch correction adjusts the wall shear rate calculation. If you skip that correction and design your piping based on Newtonian assumptions, your pressure drop estimates will be off by a factor of two to four in most cases. I ran into this exact problem on a dairy processing line where we were transferring a high-fat intermediate product through 150 meters of 50-millimeter pipe at what we calculated should be laminar flow. The pressure gauge at the discharge showed triple our prediction. Turns out the fat had partially crystallized in the transfer line because the ambient temperature in that section of the plant dropped below the fat's solidification range during a night shift. We fixed it by adding trace heating banding and insulating the line, but the initial investigation took two days because everyone was looking at rheology instead of temperature.
Mass Transfer in Food Systems
Drying is the most common mass transfer operation in food processing. Spray drying converts liquid into powder in seconds. The liquid feed enters a chamber where hot gas flows either co-currently or counter-currently. Outlet air temperature typically ranges from 70 to 90 degrees Celsius for most food products. The particle leaves the chamber as a dry powder and gets collected in a baghouse or cyclone separator. The critical parameter isn't the inlet air temperature. It's the wet bulb temperature of the drying gas. That determines the maximum evaporative cooling that can occur at the particle surface. If the drying gas can't absorb moisture fast enough, particles stick to the chamber walls and form buildup. I've seen spray dryers shut down every six hours for cleaning because the operator chased higher throughput by increasing feed rate without adjusting atomizer speed or gas flow. The product came out fine on paper. The chamber coated itself solid within a week. Fermentation processes rely on oxygen transfer rates that most food engineers underestimate. The volumetric mass transfer coefficient, KLa, depends on agitation speed, sparging rate, broth viscosity, and surface-active compounds in the medium. Food fermentation broths contain proteins and polysaccharides that act as surfactants. These compounds stabilize foam and reduce the effective interfacial area for oxygen transfer. Antifoam additions help with foaming but can coat bubble surfaces and further reduce KLa. The net effect is that your dissolved oxygen readings might look fine while the actual oxygen transfer rate is half of what your correlations predict.
Common Pitfalls That Cost Real Money
Scaling up from pilot to production is where most projects lose time and budget. The standard approach of keeping constant power per unit volume or constant tip speed doesn't work reliably for food processes. Non-Newtonian mixing behavior means that scale-up requires matching the mixing time distribution, not just average energy input. I worked on a project where we scaled a fruit puree homogenization process from a 50-liter batch to a 2000-liter production vessel. We matched the tip speed exactly. The product quality was inconsistent between batches because the residence time distribution in the larger vessel was four times wider than in the pilot unit. We ended up installing a recirculation loop with a bypass to narrow the distribution, which added capital cost but eliminated the batch-to-batch variation. Clean-in-place systems are another area where assumptions cause failures. The standard CIP validation uses conductivity, temperature, and time as pass/fail criteria. Those parameters don't tell you whether biofilm has been removed from dead legs or low-flow zones. I encountered a situation where a juice processing line passed every CIP test but still had recurring microbial spoilage in packaged product. The issue traced back to a 2-meter section of piping downstream of a valve that had near-zero flow during normal operation. The CIP spray balls couldn't reach that zone effectively. We solved it by adding a purge loop that maintained minimum flow through that section during production, which eliminated the stagnant zone and stopped the spoilage events entirely. Ingredient variability is another quiet killer. Suppliers change raw material composition seasonally. Mango puree from one region in one season has different pectin content than mango puree from another region. That pectin difference affects viscosity, which affects pumping power, heat transfer coefficients, and filtration rates. Plants that don't adjust their process parameters for ingredient variation end up with inconsistent product texture and higher waste rates. The workaround is establishing specification ranges for key quality attributes and having standard operating procedures that adjust equipment settings when incoming material falls outside the middle range.
Tools and Software You'll Actually Need
Process simulation software like Aspen Plus or UniSim can model food processes, but the property packages matter. Standard petroleum-oriented packages fail with food systems because they don't account for non-Newtonian behavior, biological degradation reactions, or the multi-component nature of food matrices. You need custom property methods or simplified models built around experimental data for your specific product. For heat exchanger design, HTRI or manual calculations using appropriate corrections for food fluids work adequately. The key is using the right viscosity correlation at the operating temperature. Food viscosity changes exponentially with temperature. A correction factor based on the Arrhenius-type temperature dependence of viscosity is necessary for accurate heat transfer predictions. Data acquisition and monitoring systems are non-negotiable for modern food processing. SCADA systems with recipe management allow operators to switch between product grades without rewriting control logic. Alarm management tied to process deviation detection catches problems before they become recalls. I recommend starting with a basic PLC-based system if you're setting up a new line. Don't buy into the idea that you need a full MES layer from day one. Get the basic process controls right first. Add the higher-level systems once you've validated the underlying unit operations.
When Chemical Engineering Approaches Fail
Not every food processing problem has a clean engineering solution. Fermentation products with complex sensory profiles sometimes resist optimization through standard process variables alone. The relationship between processing parameters and consumer acceptability isn't always linear or predictable. In those cases, you need sensory panels and statistical design of experiments work alongside the engineering analysis. The engineering sets the feasible operating range. Sensory science determines what's commercially viable within that range. Regulatory constraints also limit what you can do. Thermal processing must achieve commercial sterility for low-acid canned foods, which means meeting specific F-value requirements. Those requirements dictate minimum processing temperatures and times that may be worse for nutrient retention and flavor than what your heat transfer calculations would optimize for. You're working within a regulatory box, not an open optimization problem. Understanding those constraints upfront saves time that would otherwise be wasted on designs that can't be approved. Newer technologies like high-pressure processing and pulsed electric fields offer alternatives to thermal processing for certain products. They preserve sensory qualities better than conventional heat treatment. But they come with their own limitations. High-pressure equipment is expensive. Pulsed electric field treatment works well for conductive liquids but has limited penetration depth for solid or semi-solid foods. Neither technology replaces conventional processing across the board. They're niche solutions for specific product categories where the quality premium justifies the capital cost.