Choosing the Right Vessel for a Slurry That Turns Into Concrete at 80 Degrees
I spent three weeks last year troubleshooting a jacketed kettle that kept tripping on low vacuum alarms during a crystallization step. The process spec sheet said the heat transfer coefficient should be around 250 W/m²K. The vendor's selection software had sized it that way. What they hadn't accounted for was that the product phase changed viscosity from 30 cP to over 4,000 cP as crystals formed, and the standard half-pipe coil was essentially acting as a baffle at that point. We ended up pulling the coil out, reconfiguring to a helical baffle on the inside, and using an external recirculation loop with a gear pump. The heat transfer held steady for the rest of the run. This is the kind of thing that happens when Chemical Process Equipment Selection And Design treats the initial fluid properties as static and doesn't model the in-process changes.That experience has shaped the way I approach equipment sizing more than any textbook did. It's not about following a decision tree from inlet conditions to final selection. It's about understanding what the process actually does to the material while it's inside the vessel or pipe or exchanger.
Starting from Chemistry, Not Catalogs Every mistake I've seen in equipment selection traces back to one of two errors: people size based on the nameplate conditions instead of the actual trajectory, or they pick equipment because it looks right and then fight the process to make it work. Neither approach works long-term. The first step is always a mass and energy balance that covers the full operating envelope. Not just the design point. I've seen engineers submit PFDs with a single flow condition and be told it was a complete specification. That document is insufficient for any major vessel. You need the off-normal states, the startup transient, the shutdown purge, and the intermediate composition ranges that occur between feed switches. Equipment behaves differently at each point. A distillation column with a variable reflux ratio will have a completely different diameter requirement than one running at constant boil-up. The reboiler duty curve is not linear with feed composition either.
The second step is identifying the controlling phenomenon. Is it heat transfer? Pressure drop? Flooding? Weeping? Erosion? Fouling? Corrosion? Foaming? Most people jump to the first one that comes to mind and design around it. If you're dealing with a corrosive service and the heat transfer is borderline, your material choice drives everything downstream including the wall thickness, the tube count, the shell diameter, and eventually the procurement lead time.
Heat Exchangers Are Where Most Selections Go Wrong
Shell and tube exchangers get selected on software defaults more often than anyone admits. The software picks a TEMA type, a tube count, a baffle spacing, and calls it done. Then the process hits and the exchanger either chokes on pressure drop or fails to meet duty because the fouling factor was set too low. Here's what the software won't tell you: a 2-4 exchanger with two shell passes and four tube passes is not inherently better than a 1-2 arrangement just because the temperature cross looks tighter on paper. The temperature profile along the length determines the actual mean temperature difference, and if the shell-side fluid is the one crossing, the correction factor drops fast. I once sized a reboiler where the LMTD correction factor was 0.68. The vendor's software reported the exchanger was adequate. It wasn't. We ended up switching to a forced circulation reboiler with a separate kettle vaporizer. The footprint doubled but the reliability improved enough to justify it.Fouling is the real issue. The TEMA recommended fouling factors are conservative for clean services and wildly optimistic for ones that actually foul. Food processing streams, polymerizing monomers, cooling water with high alkalinity, flue gas condensates. Pick your poison. The rule I use is simple: if the process has ever made sludge, scale, or deposit in anything resembling this service, double the TEMA factor and verify with the operator's actual history, not the textbook table.
Get the Full Details
Pumps Require More Than NPSH Calculations
Centrifugal pump selection is straightforward until it isn't. The basics are the same: flow, head, NPSH available versus required, power, impeller material. The traps are in the details that the datasheet never captures fully. Viscosity changes the performance curve. The Hydraulic Institute standards give correction factors for viscosity above about 1 cP, but most people skip them unless the fluid is clearly syrupy. A 50 cP hydrocarbon stream will lose roughly 15 percent of its head and see a 20 percent rise in power compared to water at the same flow. If your pump is already near the end of its curve, viscosity push can move the operating point into an unstable region where the head drops sharply with small flow changes. Suspensions and solids are another category. Positive displacement pumps handle these better but they wear fast on abrasive media. Centrifugal pumps with open impellers or channel volutes can pass solids but efficiency suffers. The compromise I usually land on is a recessed impeller centrifugal for moderate solids and a progressive cavity pump when the fluid is truly paste-like. I've had gear pumps fail in under two weeks on a stream with 2 percent silica sand by weight. Not the gear teeth. The bearing ends. The seals blew because the bearing housing wasn't designed for the axial thrust component of a slurry. That one cost me a weekend and an embarrassed phone call to the vendor.Parallel versus series pump arrangements matter more than people think. Two smaller pumps in parallel give you turndown flexibility. A single large pump is cheaper upfront but harder to control. For processes with variable feed rates, parallel pumping almost always wins over the life cycle despite the higher capital cost. The energy savings during low-load operation offset the extra equipment within two to three years in most cases.
Vessels Need Better Than Good Intentions
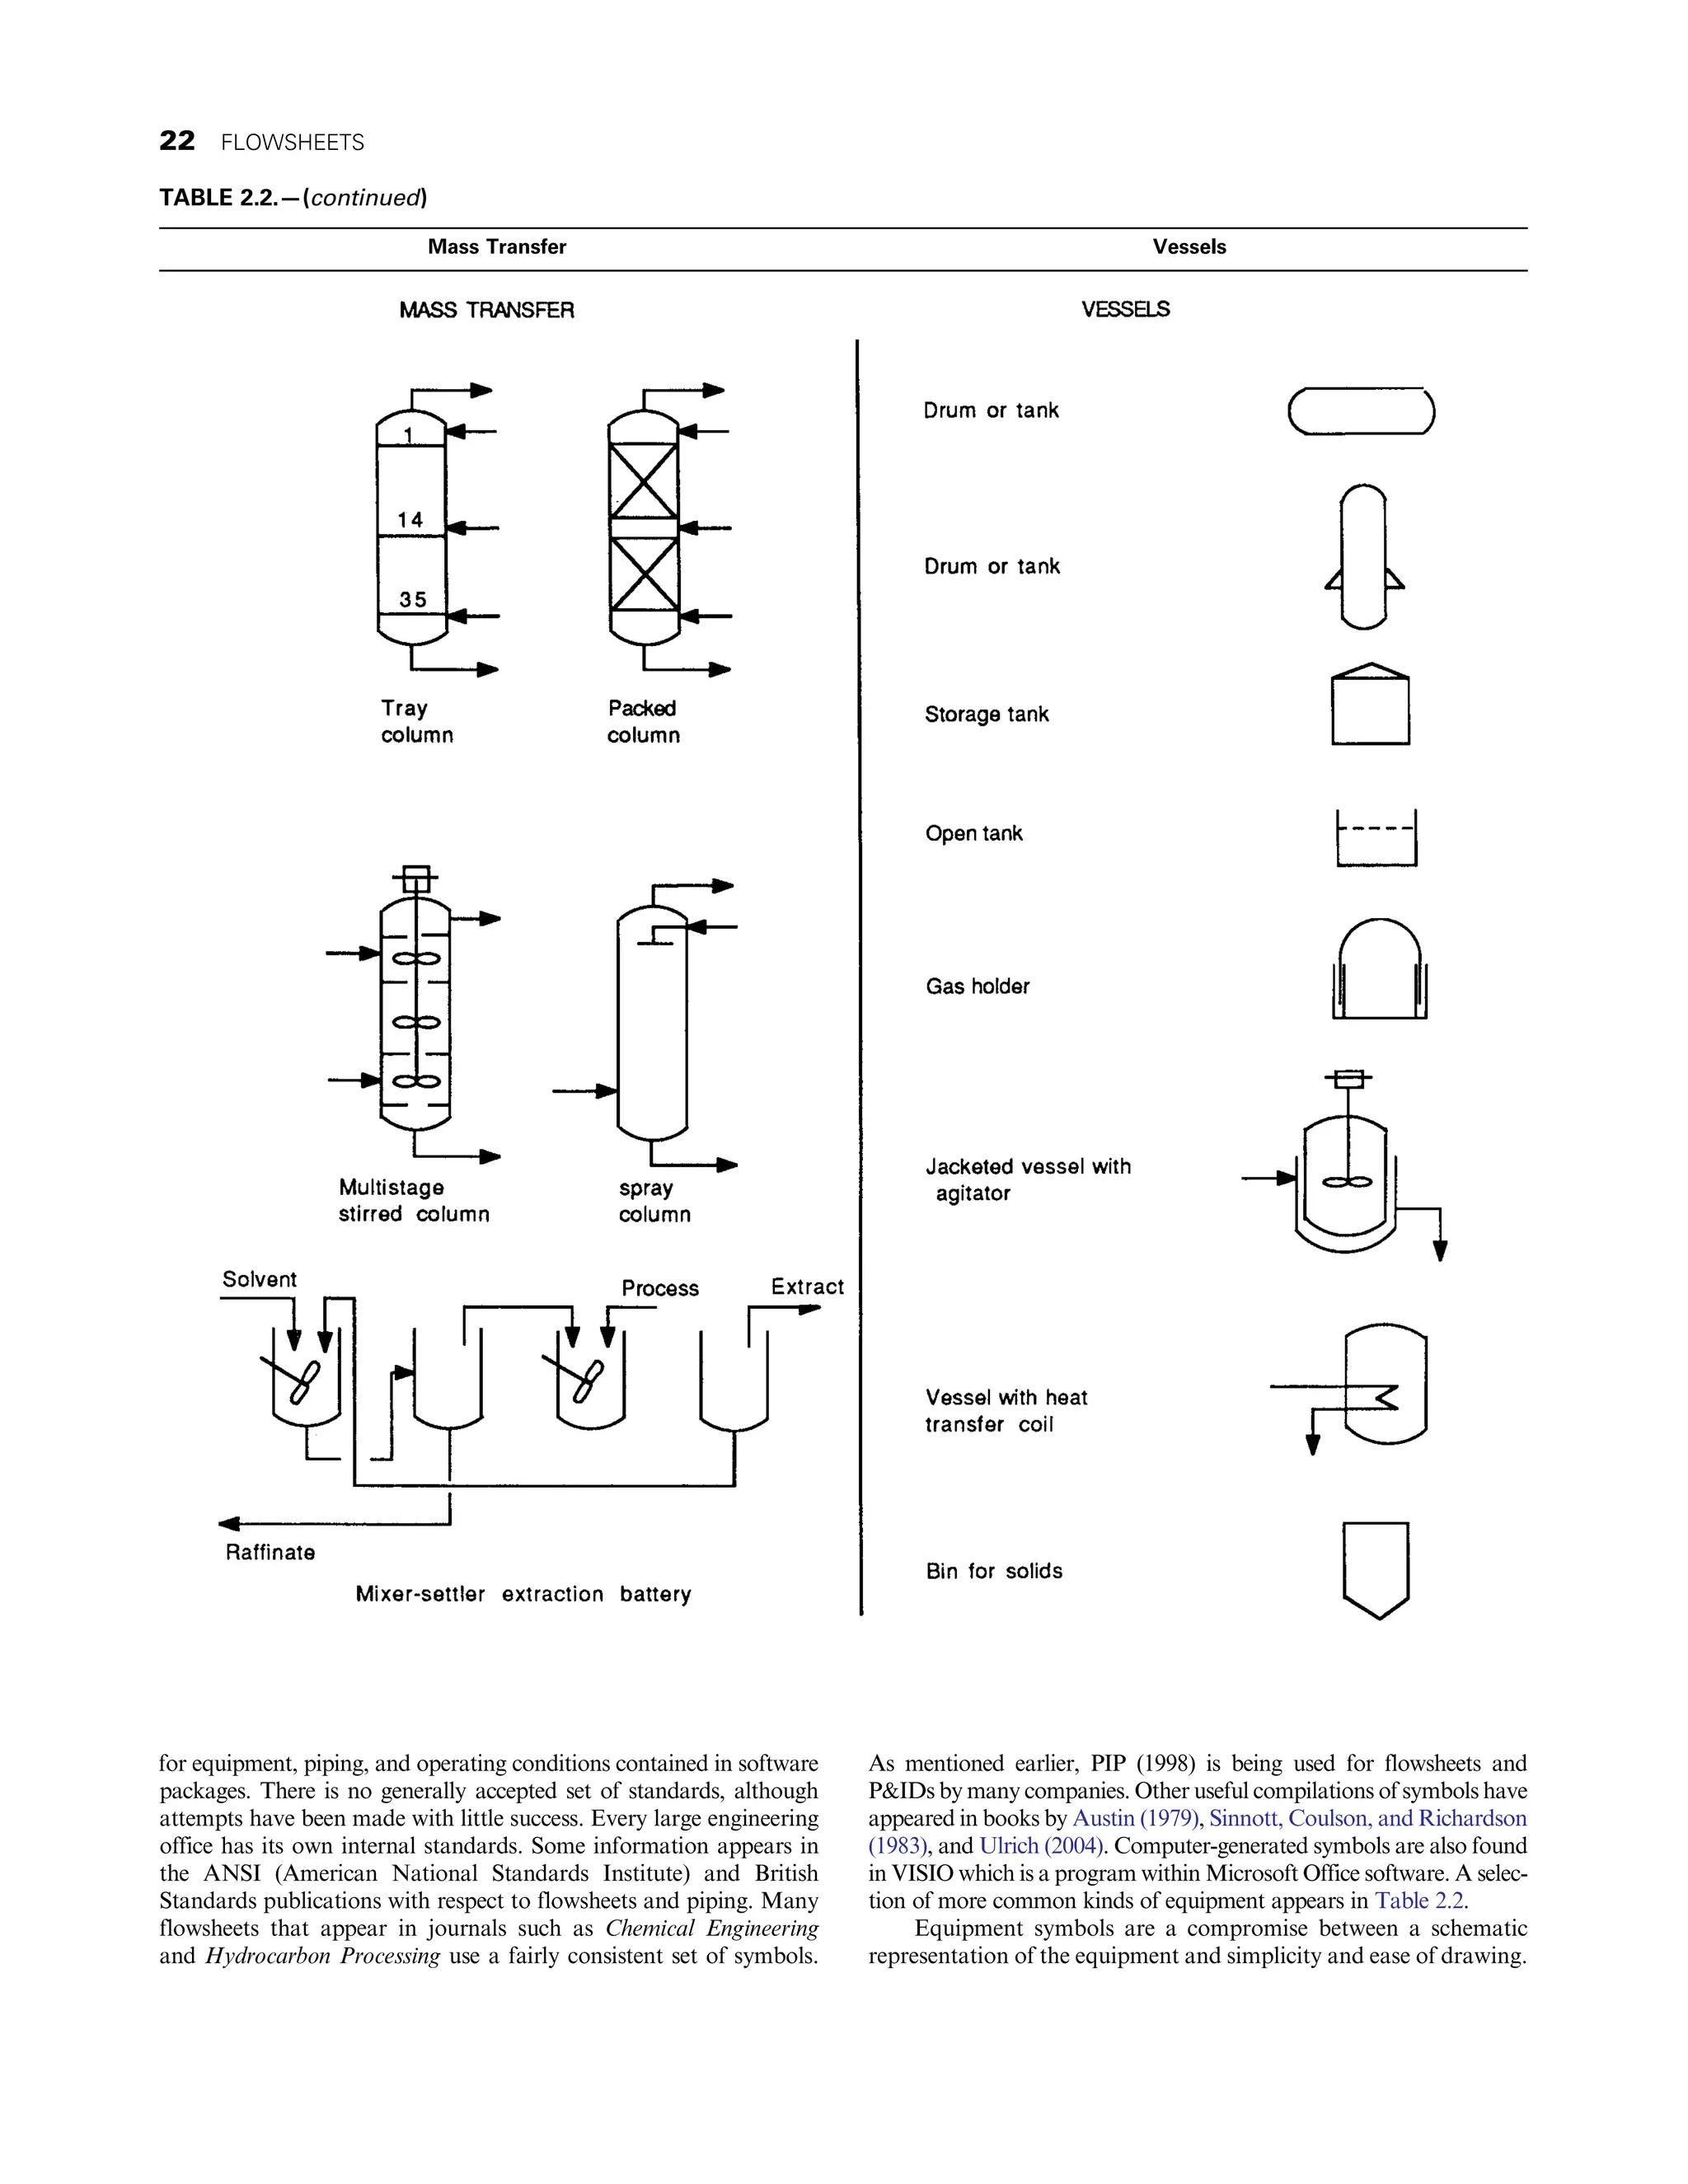
Pressure vessel design is governed by code. ASME Section VIII Division 1 is the standard in the United States. EN 13445 covers Europe. The code tells you how thick the shell needs to be, what the joint efficiency should be, how to handle nozzles and openings, and when you need hydrotest versus pneumatic test. It doesn't tell you whether the vessel will perform as intended in the process. Knockout drums are simple in theory. Gas enters, liquid drops out, gas leaves. The internal mist extractor handles the entrainment. The level controller manages the liquid. In practice, the gas velocity through the drum must stay below the Souders-Brown limit to prevent re-entrainment, and that velocity changes with gas density, which changes with pressure and temperature. A knockout drum sized for ambient conditions can become useless at design pressure if the gas density triples. The vessel might still hold pressure fine. It just won't separate properly.Agitated vessels introduce a whole separate set of variables. The impeller type determines flow pattern. The power number determines motor size. The Reynolds number determines whether you're in laminar or turbulent regime. At low Reynolds numbers, which you hit with viscous polymers or highly filled slurries, standard Rushton turbines generate almost no bulk flow. You need a helical ribbon or anchor impeller. The power requirement jumps because the torque increases with the square of the viscosity. Motor selection needs to account for startup torque, not just running torque. I've seen motors burn out during startup because the selection assumed the fluid was already moving.
Column Diameter Is About Vapor Velocity, Not Just Separation Stages
Distillation column sizing follows a standard sequence. You calculate the number of theoretical stages from Fenske-Underwood-Gilliland or equivalent. You determine the reflux ratio. Then you size the column diameter based on the maximum vapor load, which occurs at the point of highest molar flow. That's usually the rectifying section near the feed for a conventional column, but not always. If you have a side draw or a multiple feed, the peak can shift. The vapor velocity is calculated from the flooding correlation. The most common is the ( is not relevant here, I mean the General Electric or Fair correlation). The key input is the capacity parameter, which depends on the square root of the density ratio between liquid and vapor. As the pressure increases, vapor density rises faster than liquid density, and the allowable vapor velocity increases. This means a column sized for atmospheric operation may need a significantly larger diameter at higher pressure than a naive calculation suggests. The reason is that the density ratio term in the capacity parameter changes non-linearly.Packed columns have a different sizing logic. The packing type determines the pressure drop per meter. Random packing like Pall rings has lower pressure drop than structured packing for the same capacity. Structured packing gives better separation efficiency but you need to check the flood point carefully. I worked on a vacuum distillation unit where the structured packing was selected for its high efficiency, but the pressure drop across the bed was so high that the bottom pressure rose above the design limit. We switched to a random packing with slightly lower efficiency but acceptable pressure drop, and the column met its separation targets anyway because the reflux ratio compensated.
Materials of Construction Are a Decision, Not a Checklist The material you pick affects the cost, the weldability, the corrosion rate, and the thermal expansion mismatch with gaskets and bolt materials. Carbon steel is cheap and welds easily but fails quickly in acidic service. Stainless steel handles oxidation and mild acids but succumbs to chlorides. Duplex steels offer good chloride resistance but are expensive and difficult to fabricate without proper heat treatment. High alloys like C-276 or 625 handle aggressive conditions but cost five to ten times more than duplex. The decision matrix should include the specific corrosion mechanism: uniform attack, pitting, crevice corrosion, stress corrosion cracking, intergranular corrosion, erosion-corrosion. Each mechanism has different susceptibility depending on temperature, concentration, pH, and presence of oxidizers. A material that survives uniform corrosion at 60 cpm may fail in two weeks from stress corrosion cracking if the residual stresses from fabrication aren't relieved. Post-weld heat treatment is not optional for sensitized grades in chloride service. It's mandatory.
I once specified 316L for a hydrochloric acid service at 50 degrees Celsius. The initial corrosion rate looked acceptable from the chemical resistance chart. Six months in, the shell thickness had dropped by nearly 3 mm at the vapor space where the acid concentration was highest due to water evaporation. The chart I used didn't account for the concentration gradient. The lesson was straightforward: always verify the actual service conditions against the material data, not just the nominal ones.
Instrumentation Often Gets Added After the Fact
A well-selected vessel or exchanger is useless if you can't control it. Temperature sensors need proper immersion length. Pressure transmitters need wetted materials compatible with the process. Level instruments face challenges with foaming, turbulence, or dense products. Control valves need proper sizing coefficients and trim materials. These are not accessories. They are integral to the system performance. The most common failure I see is inadequate sensor placement. A temperature well placed immediately after an elbow in a pipe will read incorrectly because the flow profile is asymmetric. A level transmitter installed at the wrong elevation on a vessel with internal baffles will oscillate or give false readings. Control valves with an installed character that doesn't match the process dynamics will hunt or lag. I've spent hours diagnosing control loops that were actually instrumentation problems masquerading as tuning issues.The recommendation is simple: specify the instrument package as part of the equipment selection, not after. Include the sensor types, the insertion lengths, the tap locations, and the valve sizing calculations in the original datasheet. This prevents last-minute field modifications that degrade performance and add cost.
A Practical Selection Workflow
Here is the sequence I follow when designing equipment: Start with the process simulation. Use Aspen HYSYS or ChemCad to generate the stream data across all operating conditions. Not just the design point. Generate at least five points: low load, design, high load, startup transient, and shutdown. Next, identify the governing physics for each unit. Heat transfer dominates exchangers. Hydraulic constraints dominate pipes and columns. Mechanical strength dominates vessels. Mass transfer dominates absorption and stripping. Then, select the equipment type based on the governing physics, not the catalog. A falling film evaporator is better than a kettle reboiler for viscous products. A plate exchanger beats a shell and tube for clean, low-fouling services with tight temperature approaches. A screw compressor replaces a centrifugal one when the pressure ratio per stage exceeds about 3:1. Size the equipment using the appropriate correlations and codes. Verify the assumptions. Check for marginal conditions. Finally, specify the materials, instrumentation, and accessories together. Include the corrosion allowance, the NDE requirements, the hydrotest pressure, and the instrument package in a single specification document.This sequence takes longer upfront than skipping steps. The time savings come later when the equipment performs as expected during commissioning instead of requiring field adjustments, retrofits, or replacements.
What This Approach Doesn't Cover
Equipment selection is not an exact science. There are uncertainties in every step. The heat transfer coefficients from correlations have typical errors of ±20 percent. The pressure drop predictions for packed beds vary with packing quality and channeling. The corrosion rates from charts are averages, not guarantees. The pump performance curves from manufacturers are based on water tests, and the actual performance with process fluids can differ, especially with viscosity or gas content. Recognizing these limits is important. It means building in margins where it matters and not over-designing where it doesn't. It also means planning for monitoring and maintenance from the start. An exchanger with a removable cover for cleaning is better than one that requires hot tapping to inspeck the tubes later. A vessel with a manway at the right height saves time during inspection. These details are not glamorous but they determine whether the equipment stays operational or becomes a maintenance burden.The bottom line is that equipment selection is a practical exercise, not an academic one. The best selection is the one that meets the process requirements reliably over the design life without excessive maintenance or unexpected failures. That requires understanding the process deeply, applying the right correlations carefully, and respecting the limitations of every calculation and assumption.