Getting Started With Plasma Etching Without Losing Your Mind
Plasma processing sounds complicated because the equipment looks complicated, but the actual chemistry happening inside a chamber is usually three reactions maximum when you're doing something standard. The problem is that everything else around those reactions adds enough variables that a process which works fine on Tuesday morning fails by Wednesday afternoon if your base pressure drifted two milliTorr. I spent about six months debugging a photoresist ashing process where the only variable changing was the humidity in the building. Turns out the O2 plasma source was pulling in slightly more atmospheric moisture through the vacuum line seals than it could pump out, and that moisture changed the radical balance enough to shift etch rates by roughly 18% between high and low humidity days. The fix wasn't fancy. We just added a small molecular sieve trap on the gas line before the mass flow controller and stopped arguing about whether the chamber itself was the problem.
The Reality Of Chemistry And Plasma Processing
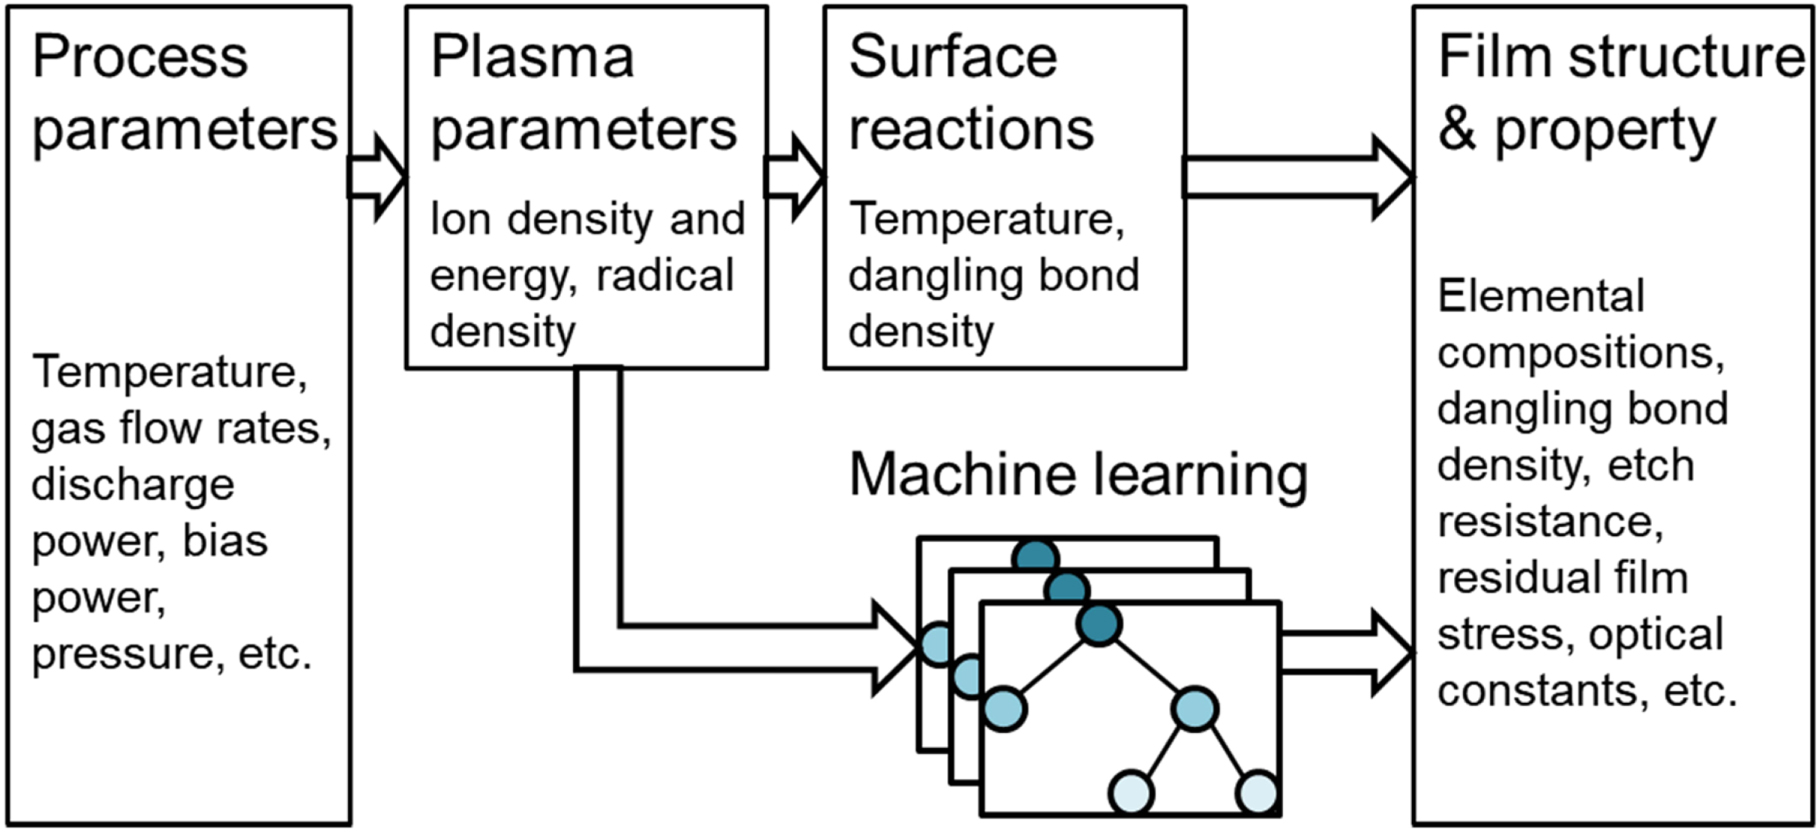
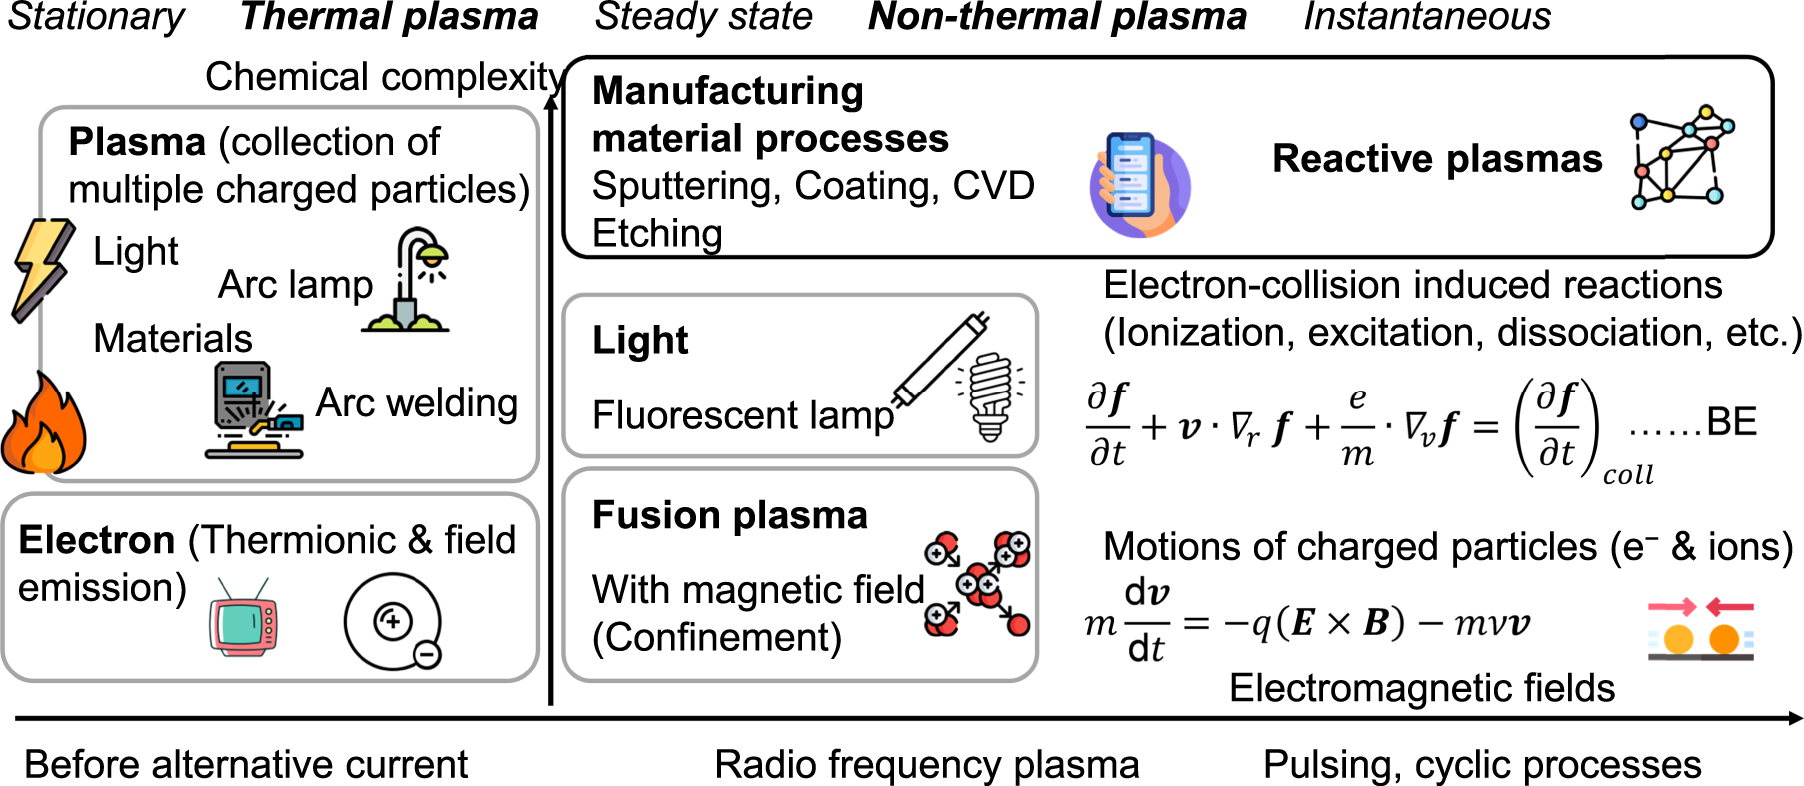
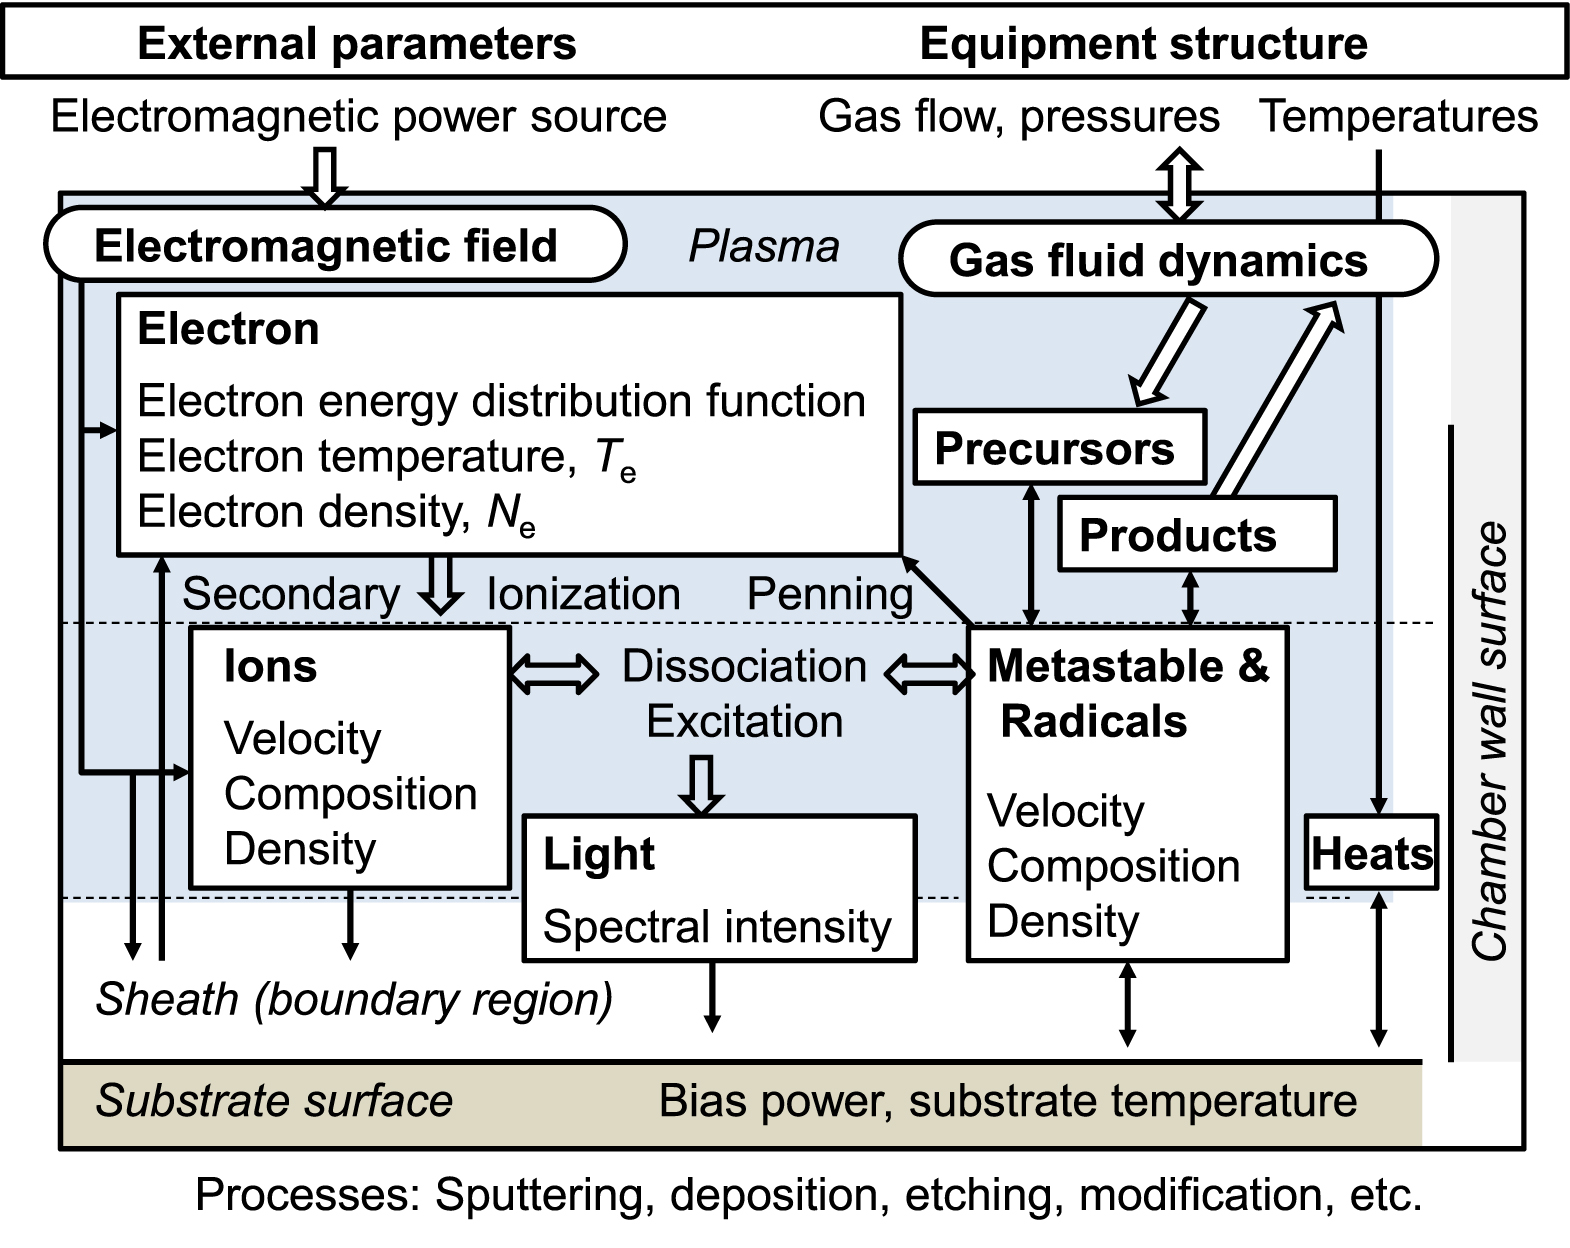
Most people learning this come from semiconductor fabrication or materials science backgrounds and treat plasma like a black box where you enter gas flows and exit with cleaned surfaces. It isn't a black box. The plasma zone itself has temperature gradients, radical density gradients, and the sheath voltage at the wafer surface changes depending on what's already been deposited there. So your first wafer in a batch etches differently than your last one even when the machine reads the same numbers. The standard starting point for dry etching is setting up your gas mixture. For silicon dioxide etching, CHF3 or C4F8 with some O2 added is common. The fluorocarbon provides the fluorine radicals that break the SiO bonds, and the oxygen adjusts the carbon deposition rate on the chamber walls. Too much carbon builds up and starves the reaction. Too little and you get non-selective etching that eats through your mask. The usual starting ratios I see in the literature are around 80:20 CHF3 to O2 by sccm, but that is a starting point, not a destination. Your actual ratio depends on chamber conditioning state, pressure, and power level. Pressure matters more than people expect. Lower pressure means longer ion mean free path, which gives you more directionality but lower throughput. Higher pressure gives you faster etch rates but more lateral attack on your features. For high aspect ratio trenches below 100 nanometers, you're usually running in the 5 to 15 milliTorr range with RF power somewhere between 200 and 600 watts depending on the reactor design. The exact numbers will vary by tool, obviously, but that's the operational window most people land in.
One thing nobody tells you when you're new to this is that chamber conditioning is not a one-time setup step. Every time you run a new film type or change gas chemistry significantly, the wall coatings shift. A chamber that was conditioned for oxide etch will introduce hydrocarbon contamination into a nitride etch process until it re-equilibrates, which can take anywhere from thirty minutes to two hours of purge and pump cycles. I learned this the hard way when my selectivity between Si3N4 and SiO2 dropped from 8:1 to about 2:1 after switching processes without a proper recondition cycle. The selectivity recovered after about an hour of running blank wafers, but we lost a full production lot in the meantime. Another counter-intuitive detail: higher RF power doesn't always mean higher etch rate. At some point, increasing power increases ion damage and redeposition faster than it increases radical generation, and your net etch rate plateaus or even drops. I've seen this specifically with C4F8 plasmas where the polymer formation rate increases disproportionately above 500 watts on certain reactor geometries. The workaround is usually to raise the pressure slightly or add a small amount of helium to spread the power density without increasing the ion energy hitting the surface. If you're doing plasma enhancement for chemical vapor deposition rather than etching, the approach flips. Now you're trying to generate reactive species at lower substrate temperatures than thermal CVD would require. The typical setup uses either an upstream plasma source where the plasma is generated away from the wafer and radicals flow downstream, or an inline source where the plasma forms right above the substrate. Upstream is cleaner for the gas lines because the plasma isn't interacting with the showerhead, but radical loss to wall recombination reduces efficiency. Inline gives better utilization but contaminates the hardware faster.
Get the Full Details
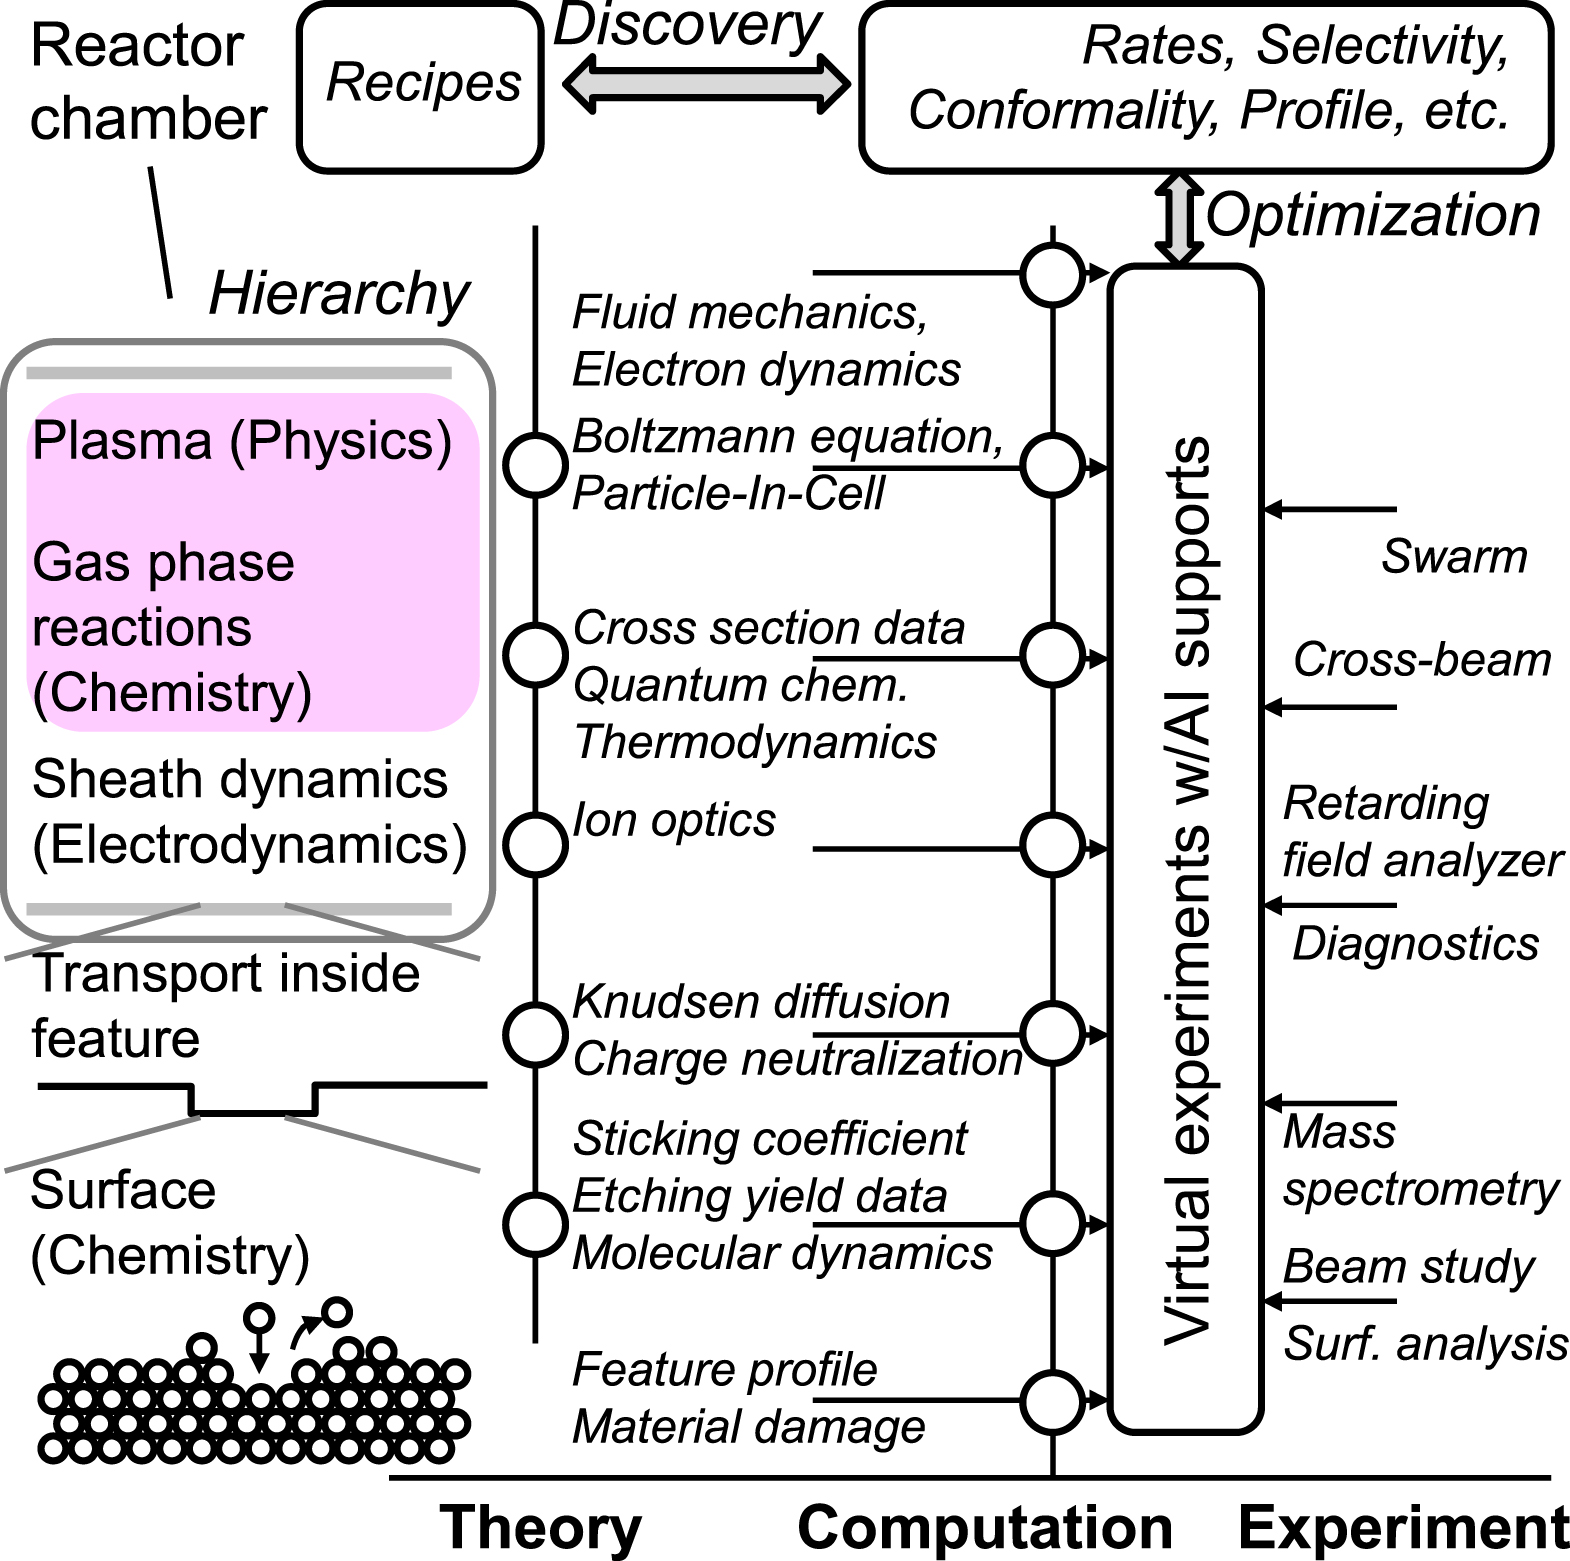
The main failure mode people run into with plasma processing is endpoint detection failure. Optical emission spectroscopy works reasonably well for simple etch-through scenarios where a new species appears at the interface, but it breaks down when you're etching through layers that produce similar emission signatures. In those cases, you're better off using reflectometry or measuring the RF impedance shift across the matching network. The impedance method picks up the dielectric constant change as the film thickness changes and is often more reliable for multi-layer stacks. A few practical notes that might save you some time. Always monitor your base pressure before every run. A rising base pressure usually means a leak or degraded pump oil, and neither of those gives you consistent plasma chemistry. Check your mass flow controller calibration quarterly at minimum. Drift in a single MFC by five percent can shift your etch profile enough to fail a critical dimension spec. And keep a log of every process change, even the small ones. The humidity incident I mentioned earlier would have been trivial to solve if I'd had records showing that the etch rate variation correlated with outside temperature rather than any internal parameter. For those looking to actually run plasma processes rather than just read about them, most major equipment manufacturers offer simulation packages that model the plasma chemistry and transport. Sentaurus Process and TCAD tools from Synopsys handle this reasonably well for semiconductor applications. There are also open-source options like COMSAC or custom MATLAB scripts that people share on forums like Semiconductor Digest and EUV Lithography community boards. Nothing replaces running actual wafers, but the simulation helps you narrow the parameter space before you waste material.
The field moves fast enough that older references become stale within a few years. The fundamental chemistry hasn't changed, but the reactor designs and diagnostic tools have. If you're working with newer high-k dielectrics or advanced node patterns, the traditional etch recipes will need significant adjustment. The principles stay the same though: control your radicals, manage your ion energy, and pay attention to what the chamber walls are doing.