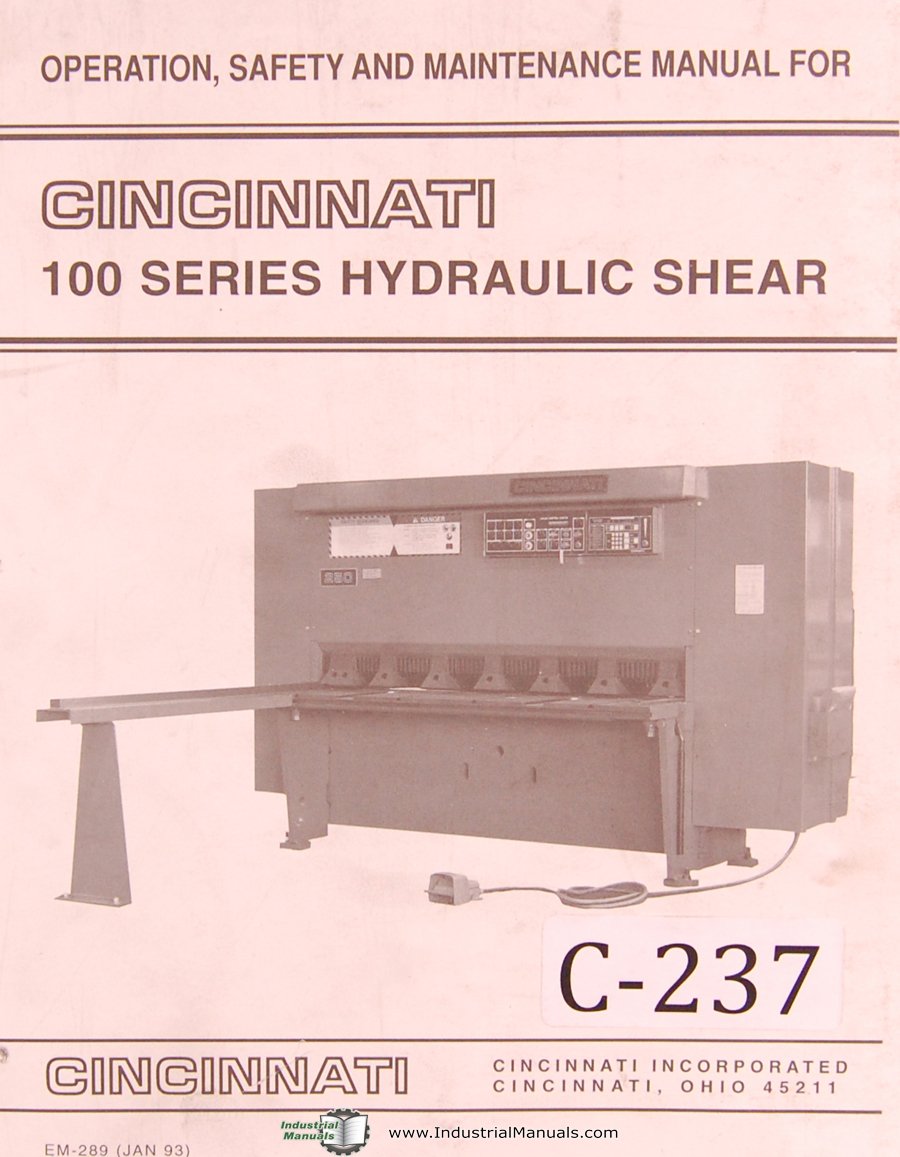
Working With the Cincinnati 250 Hydraulic Shear Manual
The Cincinnati 250 is a hydraulic plate shear, usually configured as a bench or floor-standing unit depending on your shop setup. If you're looking for the manual, you're probably dealing with one of three things: a maintenance schedule, a troubleshooting guide, or parts identification. Most people end up needing all three at once. Original paper manuals from Cincinnati subsume several revisions. The machine itself was produced across multiple decades, and the manual changes depending on whether you have the early single-cylinder setup or the later dual-cylinder variant. You'll find the most complete copies through industrial equipment resellers, machine tool archives, and sometimes directly from OEM successor organizations that absorbed Cincinnati's asset libraries. The manual typically contains the hydraulic schematics, torque specs for the shear bed bolts, blade gap adjustment procedures, and the pump pressure chart specific to your model year. I spent an afternoon last fall trying to track down a clean copy for a customer who had a 1978-era 250 with no documentation. What I ended up using was a scanned manual from a 1985 revision. It covered 95 percent of what we needed, but the pump pressure specs were slightly different between the two years. I cross-referenced with a parts diagram and a hydraulic cylinder bore measurement from the actual machine to confirm the correct operating pressure. That process took about forty minutes and saved the customer from running the pump at an incorrect setting.
The hydraulic system on these shears runs on a gear pump driven by a three-phase motor. The reservoir is typically integrated into the frame base, which means sediment and metal fines settle at the bottom over time. That's not a design flaw, it's just physics. The manual will show you the filter location and the recommended fluid type — usually an ISO 46 or ISO 68 hydraulic oil depending on your ambient temperature range. I've seen shops run these units on cheaper synthetic blends without immediate failure, but the seals tend to degrade faster, especially the piston rod seals on the cutting ram cylinders. One thing the manual doesn't always make obvious is the blade adjustment sequence. You don't just loosen the bed bolts and push the blade into position. The shear has a tolerance stack-up that matters. I learned this the hard way on a unit where someone had replaced the lower blade without torquing the locating dowels first. The cut angle was off by about two degrees across a four-foot shear length, and it wasn't until I ran a test piece through and measured the exit angle that I noticed it. The workaround was straightforward — clean the mating surfaces, reinstall the dowel pins, torque the bolts in the sequence printed in the manual (cross-pattern, starting from the center), and then recheck the gap with a feeler gauge at three points along the blade length.
Blade Gap Adjustment — The Part That Actually Matters
The blade gap is the single most important setting on this machine. Too tight and you'll heat the blade edges, accelerate wear, and increase the load on your hydraulic cylinders. Too loose and you'll get a ragged edge, excessive burr formation, and you'll be re-shearing material instead of doing it once. The manual gives a starting point based on material thickness, but the real adjustments come from understanding how the top blade overtravel works and how the backgage position interacts with your cut length. For mild steel up to a quarter inch, a gap around 0.005 to 0.010 inches per thousandth of material thickness is a reasonable starting range. So for a quarter-inch plate, you're looking at roughly 0.015 to 0.020 inches. I usually set it on the tighter side when I'm cutting clean scrap with minimal scale, and open it up slightly when the material has rust or mill scale on it. The scale acts like a lubricant in some cases, and a slightly larger gap lets it slide through without grabbing. The adjustment mechanism varies by production year. Some models use shim packs between the blade holder and the clamp plate. Others use a threaded adjustment screw at each end of the blade holder with a lock nut. The shim approach is more precise but slower to change. The threaded adjuster is faster but easier to get out of square if you don't check both ends equally. I always measure the gap at the front, middle, and back of the blade after any adjustment, not just at the ends where it's easiest to reach.
Get the Full Details

Hydraulic System Maintenance
The hydraulic system is straightforward but not forgiving if you neglect it. The main failure points I've encountered are the cylinder rod seals, the pump inlet strainer, and the valve section where the directional control solenoid sits. A clogged inlet strainer will cause cavitation that sounds like gravel running through the pump. You'll hear it immediately. I replaced a strainer on a unit that had been running with a partial blockage for six months — the pump housing had slight scoring inside, but it was still within acceptable tolerance. The replacement cost was about eighty dollars for the strainer element and two hours of labor. Fluid changes should happen every six to twelve months depending on usage intensity. If you're running the shear daily in a fabrication shop, six months is more realistic. If it's a occasional-use unit in a maintenance department, annual changes are fine. Always check the fluid condition before you change it. Dark, opaque fluid with a burnt smell means the seals are degrading and you might have contamination already inside the system. In that case, flush the reservoir and replace the filter before refilling. The manual includes a hydraulic schematic that shows the valve manifold layout. One thing to note is that the counterbalance valves on the ram cylinders are factory-set and shouldn't be adjusted unless you've replaced a cylinder seal or the ram is drifting downward when the machine is idle. If the ram drifts more than a quarter inch over ten minutes with the machine off and no load on the blade, that's a seal issue, not a valve adjustment issue. Opening the counterbalance valve to compensate for worn seals just creates a safety problem and doesn't fix the root cause.
Common Pitfalls and Where the Manual Falls Short
The Cincinnati 250 Hydraulic Shear Manual is solid for baseline information, but it assumes a level of mechanical intuition that new operators rarely have. It doesn't walk you through diagnosing a soft cut versus a hard cut, or explain how to distinguish between a hydraulic issue and a mechanical binding issue. Both can cause similar symptoms — the ram slows down or stalls during the cut — but the causes are completely different. A hydraulic issue usually presents as a gradual loss of power across multiple cycles, often accompanied by a warm reservoir or frothy fluid. A mechanical issue tends to be consistent and localized — same spot every time, same resistance pattern. If you're fighting binding at a particular point in the stroke, check the guide shoes and the parallelism of the ram to the bed. Worn guide ways will create uneven lateral force on the ram, which increases friction and makes the hydraulic system work harder than it should. Another area where the manual is thin is on blade sharpening and replacement. These shears use replaceable blade sections, not one continuous blade. The manual shows you how to remove and install them, but it doesn't address the reality that after sharpening, the blade thickness decreases and you may need to adjust the gap setting. I've seen operators set a new blade and forget to reduce the gap accordingly, which led to premature edge chipping within a few hours of cutting. The fix is to measure the removed blade thickness, compare it to the new or ground blade, and adjust the gap proportionally. A rule of thumb: if the blade lost more than 0.020 inches of thickness from grinding, reduce the gap by about half that amount.
Parts and Sourcing
Replacement parts for the Cincinnati 250 are available but the supply chain has gaps depending on how old your specific unit is. Hydraulic cylinders, seals, and valves are generally available through industrial hydraulics suppliers who carry generic replacements. The shear blades are more model-specific. I've sourced replacements through specialty metalworking parts distributors and occasionally through salvage yards where other shops have decommissioned units. Electrical components like the solenoid valve and the proximity switches on the backgage are standard industrial parts. You don't need a Cincinnati-branded component for those. I replaced a solenoid on a 1982 model with a standard Atlas Valve replacement that cost less than half the OEM price and performed identically. The key is matching the voltage, coil resistance, and port size. If you're dealing with a structural issue — a cracked weld on the frame, a bent shear bed, or a worn pivot pin — those are harder to replace. The frame components are fabricated from thick plate and the geometry isn't easily replicated. In those cases, machining a repair sleeve or having a qualified welder build up and re-machine the worn surface is usually the only viable path. I've done this with pivot pins on two separate units, and the repaired pins have held up for years when machined back to original specifications.

What This Machine Can't Do
It's worth being clear about the limitations so you don't try to make the Cincinnati 250 solve problems it wasn't designed for. This is a straight-blade shear for cutting mild steel plate and bar stock. It handles annealed and normalized material well. It struggles with hardened steel, stainless in thicker gauges, and abrasive materials like galvanized sheet where the zinc accelerates blade wear significantly. If you're cutting galvanized material regularly, expect to sharpen or replace blades at least twice as often as you would with mild steel. The maximum cut capacity listed in the manual is a best-case number under ideal conditions. Real-world capacity drops when the material has a thick oxide scale, when the shear is older and the hydraulics have some internal wear, or when you're making repeated cuts in the same spot without allowing the tool to cool. I've seen operators exceed the rated capacity by pushing wide plates through at the edge of the bed, which creates a lever effect that adds lateral load to the ram guides. That's a quick way to bend a ram or damage the cylinder mounting. If you need to cut irregular shapes, perforated material, or conduct repeat high-precision production runs, this machine isn't the right tool. A plasma cutter, a laser, or a CNC turret punch will serve you better for those applications. The Cincinnati 250 is a workhorse for straight-line cuts on plate and bar. Treat it like one and it will give you consistent results for a very long time.

 1984 Cincinnati 250 Hydraulic Shear - Pic 2.jpg "1984 Cincinnati 250 Hydraulic Shear (#4839)")
 1998 Cincinnati 250 HS 12 Hydraulic Shear - Pic 1.jpg "1998 Cincinnati 250 HS 12' Hydraulic Shear (#4385)")
