Working with Amada Laser Controls
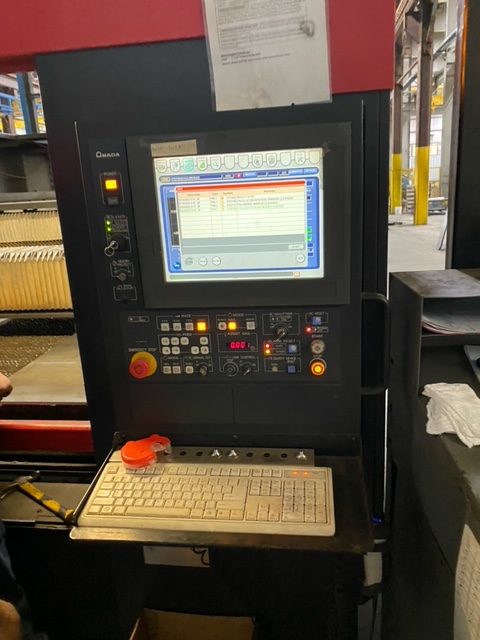
Amada machines don't use G-code in the way you might expect from a typical CNC mill. Their systems run on a proprietary control language that sits on top of the Genesis CAM platform, and getting started means understanding the architecture before you even touch the controller. The Cnc Laser Machine Amada Programming Manual isn't just a reference book—it's the thing that separates people who program these machines efficiently from people who waste half their shift hunting through menus. The official Amada documentation comes in a few forms. The primary manual for any given machine model—say, the FF-3015AJ or LS-1613—is a thick binder of control procedures, parameter tables, and error code listings. There's also the Genesis Software Manual if you're running post-processed jobs through their CAM system. Both are essential, but most people I talk to only keep the machine-specific one on hand. The Genesis stuff you can look up online when you need it. I keep a printed copy of the manual next to each machine I program. Digital versions get lost in email chains and corrupted PDFs. The paper copy survives chip coolant, dropped tools, and general shop floor abuse.
Getting the right manual starts with your machine's serial number. Amada updates firmware across production runs, and a manual for a 2015-era controller won't match a 2022 model even if the machine looks identical. Check the control panel label, find the exact model code, and order from Amada's parts documentation department or an authorized dealer. It costs money, usually between two and five hundred dollars depending on how many volumes your system requires, but it saves you from guessing at parameters that aren't publicly documented. The actual programming workflow runs like this. You generate your cut paths in Genesis or import a prepared file, then load it onto the machine controller. The controller handles nesting, power settings, frequency adjustments, and assist gas selection based on your material and thickness database. What most beginners miss is that the manual's parameter section isn't optional reading. If you're cutting stainless steel at three millimeters and your kerf compensation keeps drifting, the fix is in the parameter tables, not in tweaking your lead-in lines. I spent about four hours last year chasing a consistent edge quality issue on a 250-watt fiber unit only to find the focal position offset parameter was stored at a different memory address than the manual's index suggested. The manual had been updated in a later revision, but the shop still had the original printed copy. I cross-referenced the firmware version number against Amada's online documentation updates and found the corrected address. Took about twelve minutes to fix once I knew where to look. One thing the manual doesn't make clear enough is how the assist gas logic actually works under the control system. You can set O2 for carbon steel and N2 for stainless in your material database, but the machine will still attempt to fire the gas based on the program's gas override settings, not just your material selection. If someone runs a manual override during a job and switches to oxygen on a stainless part, the controller doesn't throw a hard stop. It just proceeds with the wrong gas. I learned this the hard way on a run of four-millimeter austenitic stainless. The part looked fine until I measured the kerf and found oxidative slag built up along the entire cut path. The operator had bumped the gas selector during a tool change. Now I check the gas mode display before every unattended run.
Another thing nobody tells you about Amada controllers: the parameter write protection. Some parameters are locked behind a service access code that isn't published in the manual. If you need to adjust focus tracking compensation or modify the pierce delay algorithm, you might find yourself unable to enter a new value even though the manual says the parameter is editable. Amada service technicians have the master code, and for most shops that means calling them in, which is a minimum four-hour window charge plus parts if anything needs replacing. Before you call, double-check that you're actually locked out and not just on the wrong parameter page. The controller has multiple parameter screens that look identical but belong to different subsystems. I've wasted phone calls on this. If you're doing a lot of custom programming outside the Genesis workflow, you should know that Amada controllers support a limited direct code entry mode. It's not full G-code. It's more like a structured instruction set where you define cut segments, power levels, and gas modes in sequence. The manual covers this in a section that most people skip because it looks dense. It's actually useful for simple fixtures or one-off parts where loading a full CAM job is overkill. The tradeoff is that you lose automatic nesting and kerf compensation, so you're manually accounting for cut offset on every string. For a batch of ten identical brackets, that's about twenty minutes of extra work per part. For a single custom mount with three unique cut profiles, it takes about five minutes total versus thirty to set up in Genesis. There's also the diagnostic mode, which the manual dedicates several chapters to. Error codes like E-2047 or E-3102 will tell you what failed, but not always why. A lens contamination alarm might mean the lens is dirty, or it might mean the air pressure sensor for the assist gas is reading low and triggering a cascade fault. The manual gives you the decision tree, but it's dense and easy to misread under time pressure. I keep a laminated quick-reference card at each machine with the top twenty error codes and their most common causes. It's saved me at least two downtime incidents per month that would have otherwise required a service call.
Get the Full Details
The manual will also cover maintenance intervals, nozzle inspection procedures, and lens replacement. These sections are worth reading straight through when you first get the machine, because the recommended intervals vary significantly between models and between fiber and CO2 systems. A fiber laser's maintenance schedule is considerably less aggressive than an older CO2 unit's, but the manual doesn't always make that distinction obvious if you're comparing documentation across different machine generations. Bottom line, the Cnc Laser Machine Amada Programming Manual is the foundation, but it's not a substitute for understanding how the controller actually executes a job. Read the parameter sections carefully. Keep a current copy. And don't assume the machine will protect you from operator errors—it won't, not consistently.