What actually happens when a CNC machine starts misbehaving
You are at the machine. It is throwing alarms on a Tuesday afternoon and your part is already scrap. Panic is not a troubleshooting method. The most useful thing you can do at that moment is slow down and read what the screen is telling you before you start slamming reset buttons or guessing at wiring problems. A proper Cnc Machine Troubleshooting Guide is not a list of symptoms and random fixes. It is a structured way of isolating where the failure lives. Every CNC problem comes from one of four places: the code, the machine hardware, the controls, or the material setup. If you check all four in order you will find the real cause almost every time instead of swapping parts until something random stops happening.
How to build a Cnc Machine Troubleshooting Guide for your own shop
Start by writing down the exact alarm code and the moment it appeared. Did it happen during tool change? On a rapid move? After a specific line in the program? That timing tells you more than most people realize. I spent three hours once replacing a faulty spindle encoder because the machine kept throwing a position-following error, and the real issue was a single loose ground wire on the Y-axis servo drive that only made contact when the axis vibrated during acceleration. Three hours of parts and one torque wrench if I had checked that first. Program errors cause roughly half of all reported CNC faults, but most operators do not check them properly. Open the program and run it in dry-run mode with the spindle off and the tool height offset reduced to something safe. Watch the rapid moves. Look for any Z-axis motion that drops below your clearance height. Check that your G-code modal state makes sense. G90 versus G91, G20 versus G21, and fixed cycle returns can silently ruin a job if they were changed somewhere earlier in the program. Another common issue is improper tool length compensation application. If your machine uses G43 Hxx and the tool table entry is wrong, the control will drive the spindle to a position that does not exist in physical space. The alarm will fire, but the root cause is a bad tool offset entry, not a broken axis. Write down every tool length and set value before you ever start production on a new job. It takes two minutes and saves three days of confusion later.
Step two: isolate mechanical issues from control issues
When alarms point toward an axis problem, you need to determine whether the control is asking for movement and the machine is refusing, or whether the machine is moving and the control thinks it is somewhere else. Back off the servos carefully and run each axis manually through the full travel using the hand wheel or jog keys. Listen for binding, grinding, or sudden resistance changes. A worn ball screw or a ways wiper dragging into chips will show up immediately as uneven drag, usually worse in one direction. Check backlash with a dial indicator if your machine allows it. Some controllers have a backlash compensation parameter, but it only works if the wear is consistent and within specification. I had a vertical machining center that started losing .003 inches of accuracy on the X-axis during long programs. The spindle thermal growth was normal, the code was fine, and the alarms never triggered. The root cause was a ball screw nut that had just barely exceeded its preload spec. Backlash compensation masked the symptom for a while, but the part was still out of tolerance every time. You have to know your machine's actual condition before the compensation parameters become useful.
Get the Full Details

Step three: power and grounding problems that nobody expects
This section is where the expensive mistakes happen. CNC controls are sensitive to ground loops and voltage sag. If your machine is on a shared circuit with anything inductive, you will see intermittent faults that make no sense on paper. VFDs for chillers, contactors, solenoid valves, and spot welders can all create noise that corrupts encoder feedback or confuses the servo amplifiers. Check your earth ground first. A floating or high-resistance ground will cause random alarms that come and go with humidity or nearby equipment cycling. Measure the resistance between the machine frame and your facility ground point. It should read close to zero ohms. Anything over a few ohms is a problem that will not resolve itself through software tuning. Also check cable integrity. Drag chains accumulate stress. I found a nearly-severed shield on an encoder cable after a machine had been throwing sporadic axis fault alarms for two weeks. The shield was intact enough to carry signals most of the time, but microfractures opened up under vibration. Replacing the cable cost less than one day of downtime. Inspect every cable that runs through a moving chain at least once a year.
Step four: coolant, lubrication, and thermal issues
Low lubrication causes more damage over time than immediate catastrophic failure. Check the way lube reservoir and verify that the pump is cycling. Many machines have metering valves that can clog with old synthetic oil residue. If one axis is consistently underlubricated while others look fine, clean the individual metering valves. They are inexpensive and save you from replacing guideways later. Coolant concentration matters more than most shops track. Too dilute and you get poor chip evacuation and accelerated tool wear. Too concentrated and you get bacterial growth that degrades the fluid and clogs nozzles. Test your concentration weekly with a refractometer, not by taste or guesswork. Spindle thermal growth is also a real factor in precision work. A machine that has not been warmed up will drift until the spindle reaches operating temperature. If you are holding tolerances tighter than .0005 inches, warm up the spindle at idle for at least fifteen minutes before starting production programs. Skipping this step is not a trick that works consistently.
Common alarms and what they usually mean
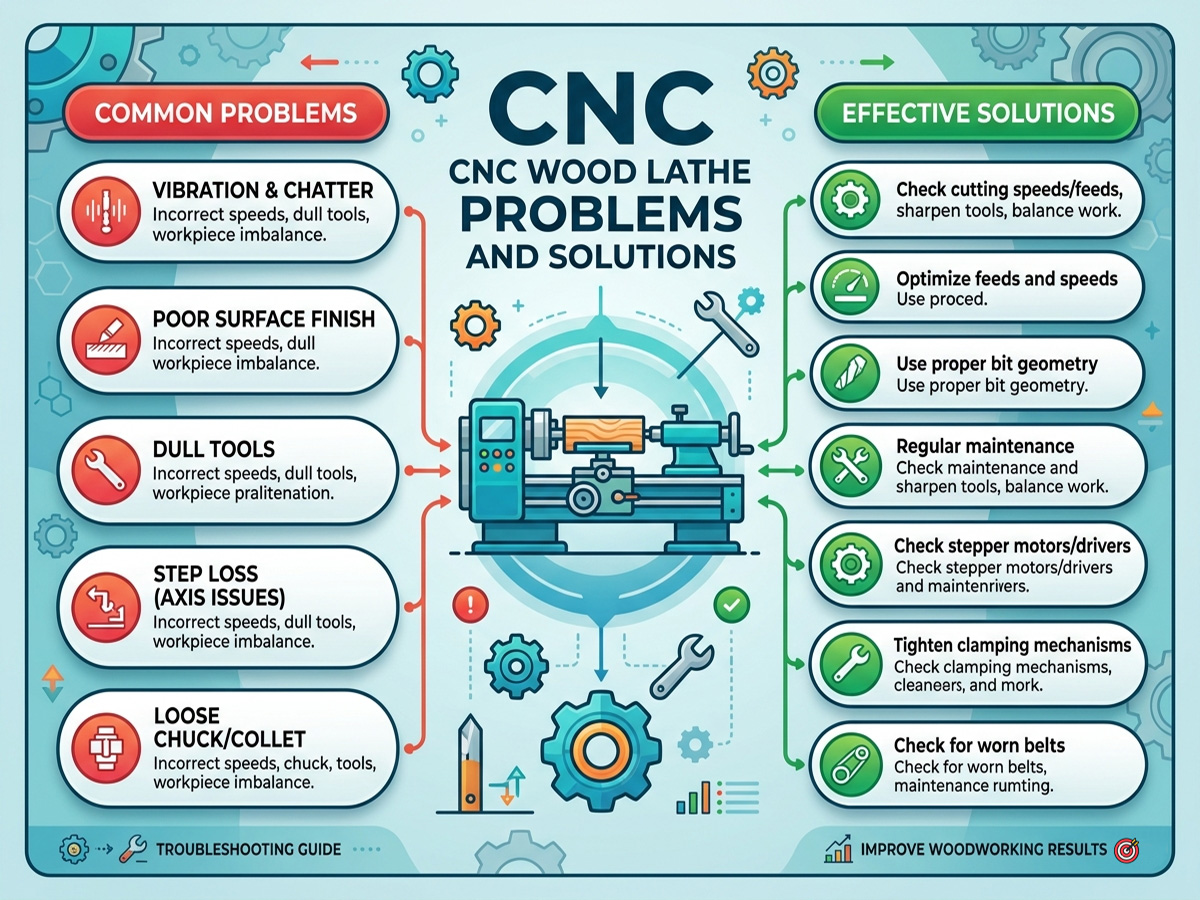
Overtravel alarms happen when the machine hits a hard limit, but they also trigger when the servo loses sync. If you get an overtravel alarm after a rapid move, check for servo load feedback errors or coupling slippage on the motor. Interference alarms between axes usually indicate a collision detection threshold issue or a mechanical binding problem, rarely both axes being genuinely out of position simultaneously. Spindle orientation faults often trace back to a dirty or failed spindle encoder, but they can also come from a loose keyway connection between the encoder and the spindle shaft. Torque overload alarms during cutting point to feed rate being too aggressive for the material or a worn drive component. Do not just reduce the feed and keep running. Find out why the alarm triggered in the first place.
When a Cnc Machine Troubleshooting Guide will not help you
There are failures that no amount of systematic checking will catch quickly. Controller board failures, intermittent connector issues inside a cramped electrical cabinet, and firmware bugs that only appear under specific motion profiles fall into this category. In those cases you need either the machine manufacturer's diagnostic mode with live signal monitoring or a controlled swap of suspected components. Writing your own guide will not substitute for having the service manual and the schematics for your specific model. Every machine brand handles error logging differently. Some store the last thousand alarm events with timestamps and axis positions. Others clear everything on a power cycle. Check what your machine actually records before assuming you have data to work with. The single most useful tool you can add to your workflow is a logbook. Not a spreadsheet, just a notebook next to the machine where you write down the alarm, the conditions, and what you changed to fix it. Six months later when the same alarm returns you will already know what it was. That habit is worth more than any downloaded troubleshooting guide you will ever find online.