What CNC Router Bits Actually Are and How to Pick Them Without Losing Money
Picking the right CNC router bits has nothing to do with buying the most expensive set on Amazon. It has everything to do with understanding chip load, flute geometry, and what your spindle can actually sustain under load. Most people I see wasting money are running solid carbide bits at speeds that would melt a cheaper coated bit, or choosing flute counts based on finish quality when the real issue is chip evacuation. Before you look at any product page, you need to know two things about your machine: the maximum RPM your spindle delivers under load, and the torque curve. A 3HP router that spins at 24,000 RPM on no load will slow to 12,000 the moment it hits dense hardwood. That slowdown changes everything about which bits work and which ones just burn. I had a customer who spent $400 on a set of premium bits for his 12,000 RPM spindle, then couldn't get acceptable feeds because the bits were designed for 24,000 RPM operation. The workaround was buying a set of 1/4" shank bits instead, which run stable at lower RPMs and still remove material aggressively when you respect the chip load numbers.
Cnc Router Bits Guide
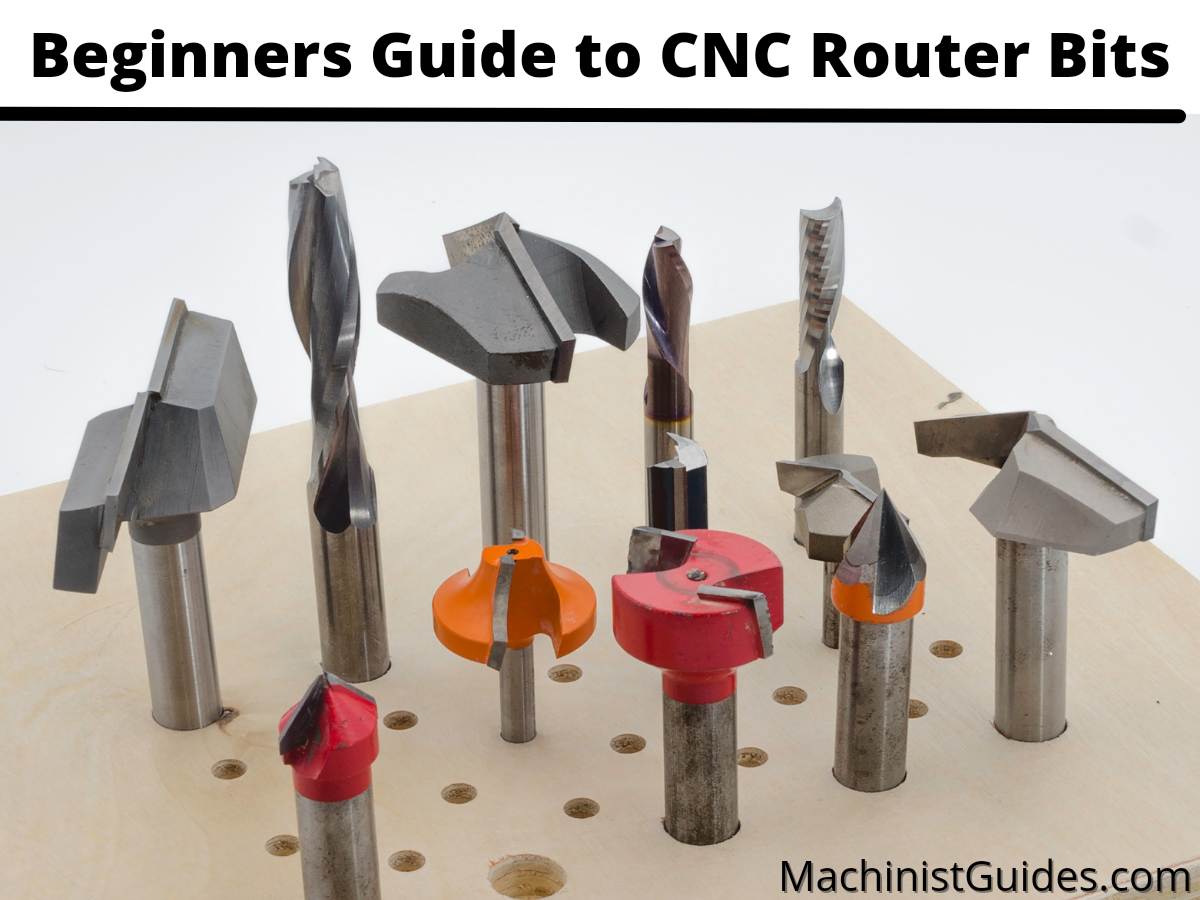
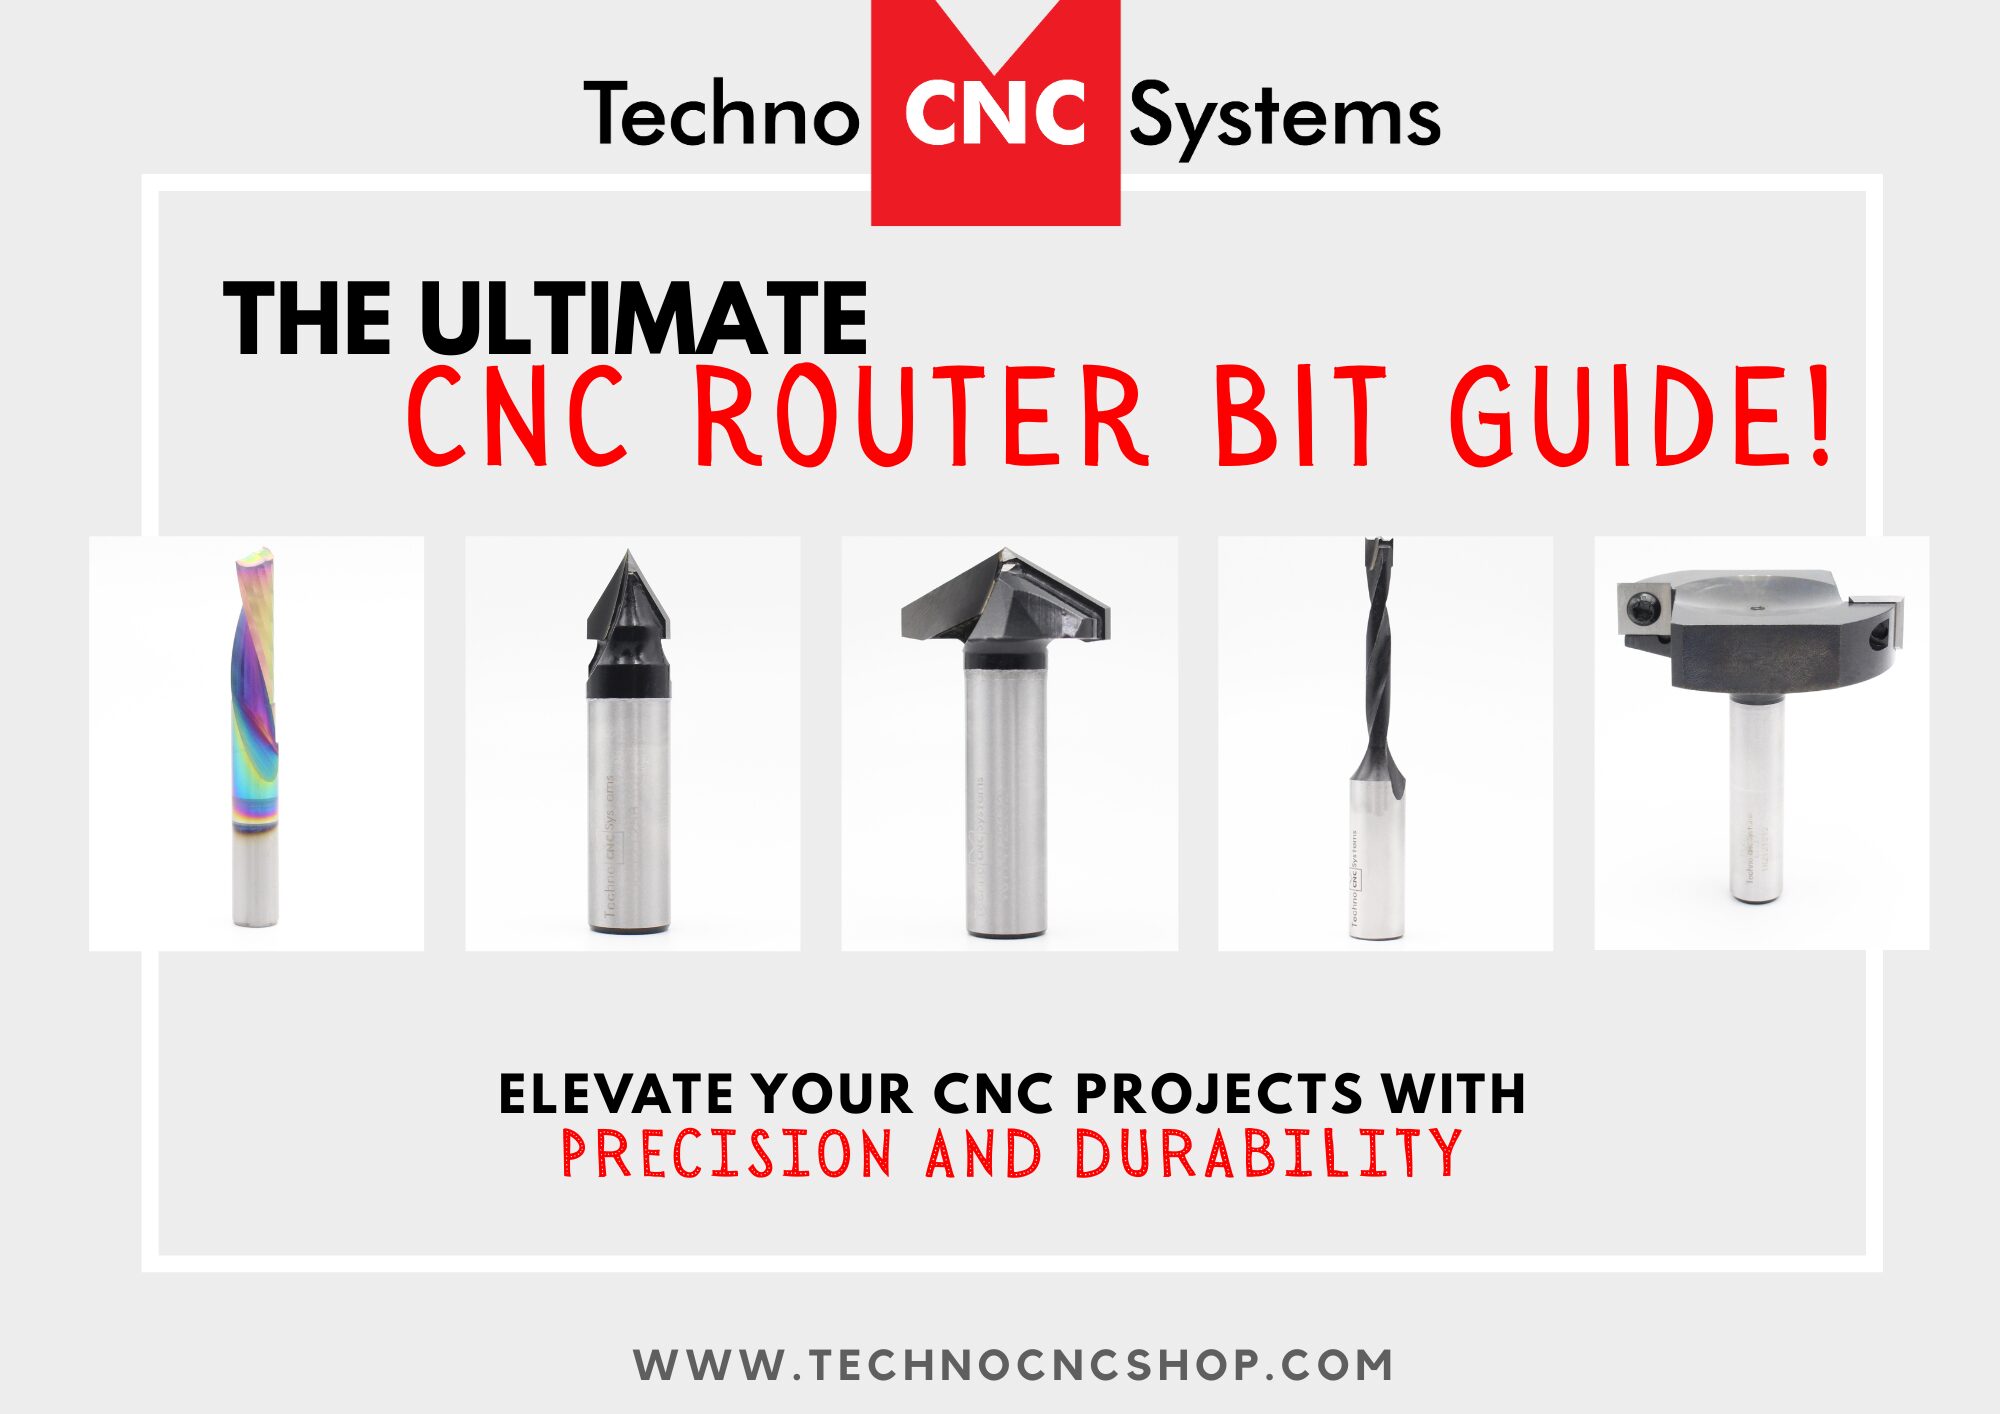
Let's start with the three spiral bit types you'll encounter, because this is where 80% of mistakes happen. Up-cut spiral bits pull chips upward and out of the kerf. They are the default for soft materials like MDF, pine, and most plastics. The trade-off is that they tear the top surface of the workpiece as they exit. This is why up-cuts are fine for pocketing or dadoes where the top grain doesn't matter, but a terrible choice for laminates or decorative edge work where the top face needs to stay clean. Down-cut spiral bits push chips downward. The result is a clean top surface, which sounds ideal until you realize that chip evacuation becomes a serious problem. In deep cuts, the chips have nowhere to go and pack into the kerf, causing heat buildup and premature bit failure. I once ran a down-cut bit at full depth in 3/4" birch plywood and the bit smoked after three passes. The workaround was switching to half-depth passes with a brief upward pull between each cut to clear the packed chips. Down-cuts are best for shallow finishing passes or when cutting laminates where top-surface chipping is the primary concern.
Compression spiral bits combine up-cut geometry on the lower portion and down-cut on the upper portion. The result is a clean surface on both the top and bottom of the material. This is the gold standard for laminated materials like HPL, melamine, and thin-sheet plywood where you need to avoid tear-out on either face. The catch is that compression bits are significantly more expensive—usually 2.5 to 3 times the cost of an equivalent up-cut or down-cut—and they wear faster on the up-cut portion because that section is doing all the chip evacuation work. If you're routing solid hardwood or doing heavy stock removal, a compression bit is overkill and a waste of money. Flute count is another area where people make wrong assumptions. Two-flute bits are standard for wood and plastics because the wider gullet provides maximum chip clearance. Four-flute or more bits are designed for metals and composites where you need finer chip breaking and a smoother cut. Using a four-flute bit in MDF at aggressive feed rates will overload the flutes, cause burning, and dramatically reduce bit life. The counter-intuitive part is that two-flute bits often produce a better finish in wood than four-flute bits, because the superior chip evacuation prevents heat buildup that degrades the cut surface. Shank diameter matters more than most people realize. A 1/4" shank bit deflects significantly more than a 1/2" shank bit at the same RPM and feed rate. If you're doing deep cuts or hard materials, the extra rigidity of a 1/2" shank can allow you to increase your feed rate by 30 to 50 percent without sacrificing finish. But 1/2" shank bits require a compatible collet, and not every router has that option. Check your equipment before you buy.
Get the Full Details
Here is the chip load calculation that actually matters. Take your bit's recommended chip load per tooth, multiply by the number of flutes, then multiply by your RPM. That gives you the feed rate in inches per minute. For a 1/4" two-flute up-cut in MDF at 0.003 inches per tooth chip load and 18,000 RPM, the calculation is 0.003 × 2 × 18,000 = 108 IPM. That number is your starting point, not your final answer. Adjust based on spindle load, sound, and chip appearance. Heavy curly chips mean you're cutting correctly. Fine dust means your feed rate is too high and you're rubbing instead of cutting. Chunky irregular chips mean your feed rate is too low and the bit is tearing material rather than shearing it. Depth of cut per pass is where most beginners destroy their bits. The general rule is 0.5 to 2 times the cutter diameter per pass, but this varies wildly by material and bit rigidity. For a 1/2" end mill in aluminum, stay under 0.25" per pass. In soft MDF, you can safely go up to the full 0.5" diameter. The limitation is not the bit—it's the deflection. A 1/4" end mill with 1" of flute length will flex noticeably under lateral load, and that flex translates directly into poor dimensional accuracy and premature failure. If you need deep cuts, use a shorter flute length or step down your radial engagement rather than pushing axial depth. Coating selection is another factor people overlook. Titanium nitride (TiN) coatings reduce friction and increase heat resistance, making them useful for aluminum and non-ferrous metals. Diamond-like carbon (DLC) coatings provide even lower friction and are better for abrasive materials like carbon fiber composites. Standard uncoated carbide is perfectly adequate for wood and plastics, and in some cases performs better because the coating can flake off in dusty environments and create contamination issues. Don't pay extra for coatings unless you have a specific material reason.
One practical tip that saves money: inspect your bits before each job. Look for chipped corners, built-up edge material, or worn flutes. A bit that has lost its sharpness will not just produce worse finishes—it will generate excess heat that can damage your workpiece and shorten the life of subsequent bits. I clean my bits between jobs by soaking them in brake cleaner for ten minutes, then brushing off residue with a nylon brush. This removes the polymerized resin that builds up in wood bits and restores cutting efficiency without needing to buy replacements prematurely. The biggest misconception in this space is that more expensive bits always perform better. They do in high-volume production environments where consistency matters. For hobbyists and small shops, a mid-range bit from a reputable manufacturer like Amana Tool or Whiteside will outlast cheap imports and perform within 90 percent of premium options at half the price. The savings compound quickly when you are going through multiple bits on a regular schedule. If you are just starting out, buy a small set: a 1/4" up-cut, a 1/4" down-cut, and a 1/2" compression bit. Those three will handle 90 percent of common routing tasks. Add specialized bits only when you encounter a specific application that the standard set cannot handle efficiently.