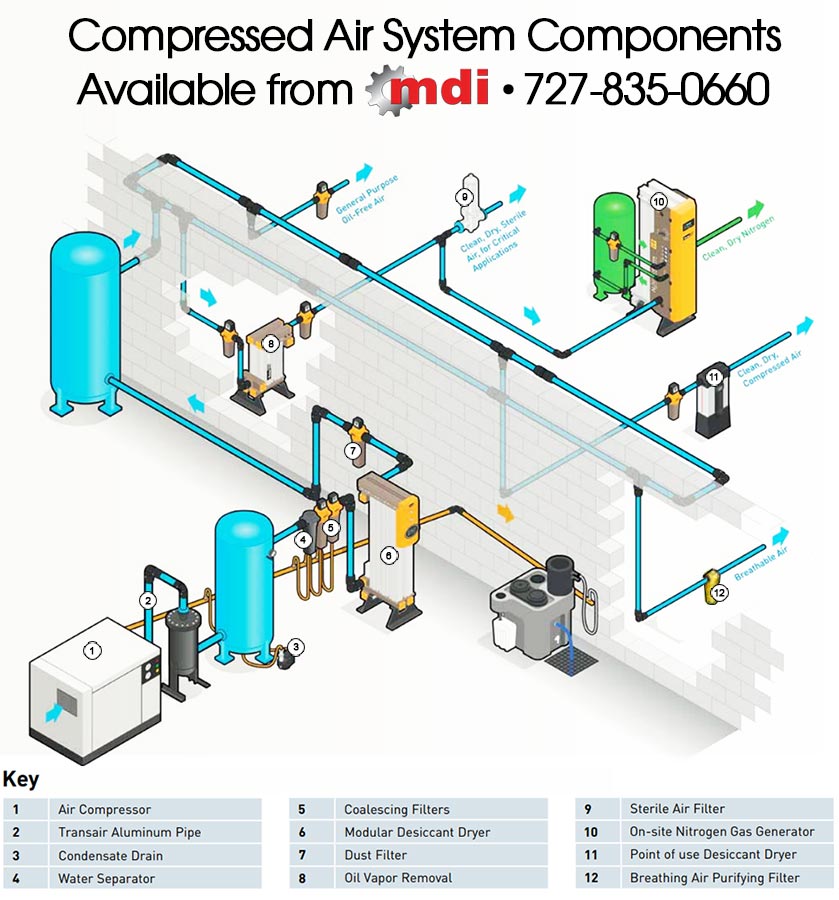
What You Actually Need When Designing a Compressed Air System
I still remember pulling an all-nighter five years ago because someone had sized a main header using the wrong units in a spreadsheet. The result was a 3-inch schedule 40 pipe running 200 feet with a pressure drop of nearly 15 psi at full load. The plant lost efficiency across three production lines before anyone noticed. That spreadsheet error is exactly why engineers keep a Compressed Air Piping Design Handbook open on their desk while doing preliminary layouts. The handbook isn't a novel you read cover to cover. It is a reference you pull when you need to size a line quickly and avoid the mistakes that cost money. You start by mapping every outlet, estimating the flow at each point, and laying out the approximate pipe runs. Then you use the pressure drop tables to check whether your selected pipe size can handle the demand without dropping below the minimum acceptable pressure at the farthest point. Most handbooks give you charts based on a 3 psi allowable drop for the entire system. That is a reasonable starting assumption for most industrial plants. One thing the handbook will not tell you clearly is how to handle loop systems versus dead-end mains. Loop mains are almost always better for pressure consistency, but they require more pipe and more valves. Dead-end mains are cheaper to install but create uneven pressure distribution. I learned this the hard way on a project where we used a dead-end main for a row of ten machines. The first two machines had stable pressure. The last two were starved and causing quality issues on the line. We cut the main, added a return branch, and turned it into a loop. Pressure equalized within 30 minutes of commissioning.
The friction loss formulas in the handbook are based on the Darcy-Weisbach equation and assume smooth pipe interiors. That assumption breaks down with older steel pipe that has internal corrosion or scale buildup. When you are working with existing infrastructure rather than new installation, you should derate your calculations by 25 to 30 percent to account for increased roughness inside the pipe. I started doing this automatically after I saw a plant engineer trust his friction loss table completely and then watch his pressure tanks cycle constantly because the pipes could not deliver what the math said they could. Velocity matters as much as pressure drop. Most handbooks recommend keeping velocity below 20 feet per second in the main header and below 30 feet per second in branch lines. Going above those numbers introduces erosion, noise, and unnecessary pressure loss. There is a counter-intuitive part here though: a larger diameter pipe does not always mean lower velocity if the flow is distributed across multiple branches early in the run. The trick is to think about the flow in each segment, not just the total system flow. A 6-inch main feeding a 2-inch branch at the first takeoff will have very different velocities in each segment even though the total volume is the same. Condensation management is another area where the handbook gives you general guidance but the real world is messier. Compressed air contains water vapor that condenses as it cools in the piping. If you run horizontal runs without drip legs and condensate drains, you will accumulate water in the low points. That water creates turbulence, increases pressure drop, and can even cause water hammer if it travels fast enough. I once traced a recurring water hammer issue back to a 150-foot horizontal run with no drip legs and a single drain at the very end. The fix was installing three drip legs with automatic drains at approximately 50-foot intervals. It reduced maintenance calls from weekly to quarterly on that circuit.
Sizing the receiver tanks is something the handbook covers but rarely explains well. The rule of thumb is roughly one gallon of receiver volume per cubic foot per minute of compressor capacity. That gives you a buffer against short-term demand spikes. In practice, I have seen plants with adequate receiver capacity still suffer pressure drops because the piping between the receiver and the point of use was undersized. The tank is only as useful as the pipe feeding it. A 500-gallon tank connected to a 1-inch line is practically useless during a high-demand event. When the handbook discusses materials, it usually compares steel, aluminum, and HDPE. Steel is strong and cheap but heavy and prone to corrosion on the inside. Aluminum is lighter and resists corrosion but is more expensive upfront and requires careful joint design. HDPE is corrosion-proof and easy to install but cannot handle high temperatures and needs proper support spacing. For most new installations in a dry indoor environment, I tend to recommend aluminum. It is fast to assemble, does not rust, and the fittings are reliable. If the plant has high humidity or outdoor runs, steel with proper drainage or HDPE with UV stabilization becomes a better choice. One common mistake I see repeatedly is ignoring the pressure drop across valves and fittings. The handbook tables usually list friction loss for straight pipe only. Fittings and valves can add 20 to 40 percent more pressure drop to your system. A fully open ball valve adds very little. A gate valve that is not fully open, or a poorly designed manifold, can add significant resistance. I started adding an equivalent length of 15 to 25 feet of pipe for each major valve and fitting into my hand calculations. It is a rough approximation but it keeps my designs from being overly optimistic.
Get the Full Details

The handbook is not a substitute for understanding your actual plant conditions. It gives you standard charts and formulas that work under ideal assumptions. Real plants have temperature variations, condensation, aging components, and modifications made by previous contractors who did not follow good practices. The most useful application of the handbook is to use it as a baseline, then adjust for the conditions you actually find on site. Measure the pressure at the compressor discharge, measure it at the farthest point, and compare the difference to your calculations. If they do not match, you either miscalculated or the system has an undocumented restriction somewhere. I also want to mention that the handbook methods assume steady-state flow. Many plants operate with intermittent demand patterns that create transient pressure waves. These transients are hard to predict with standard friction loss tables. If your plant has machines that draw large bursts of air simultaneously, like a paint booth cycling with a large robot arm, you may need a more detailed simulation or at least a significantly oversized main header. The handbook will not flag this risk for you. You have to recognize it from the process itself. If you are looking for a copy of a Compressed Air Piping Design Handbook, the most reliable sources are professional societies like ISA and ASME, or directly from compressed air equipment manufacturers who publish engineering guides. Some of these are free PDFs on manufacturer websites. A few are sold through technical book publishers. The content across all of them overlaps substantially. Pick the one that matches the pipe materials and fittings you are most likely to use in your next project.
The handbook is a tool, not a guarantee. Use it early in the design phase to size your mains and branches. Verify your assumptions on site during commissioning. Adjust as needed. The plants that run quietly and efficiently on compressed air are the ones where the piping was designed with the handbook as a starting point and then refined with real measurements, not the ones where the handbook was treated as gospel.


