What Compressed Gas Safety Training Actually Looks Like
The biggest mistake I see people make is treating compressed gas safety training like a checkbox exercise. You watch a video, sign a sheet, and move on. It doesn't work that way. I ran a compression station for about eight years and the people who took it seriously were the ones still working after their first shift. The rest ended up with lecture notes and a few bruises they didn't mention to anyone. Compressed Gas Safety Training covers regulator selection, cylinder handling, leak detection, venting procedures, and emergency response. That's the syllabus version. Here's what it actually involves on the floor.
Compressed Gas Safety Training for the Working Shop
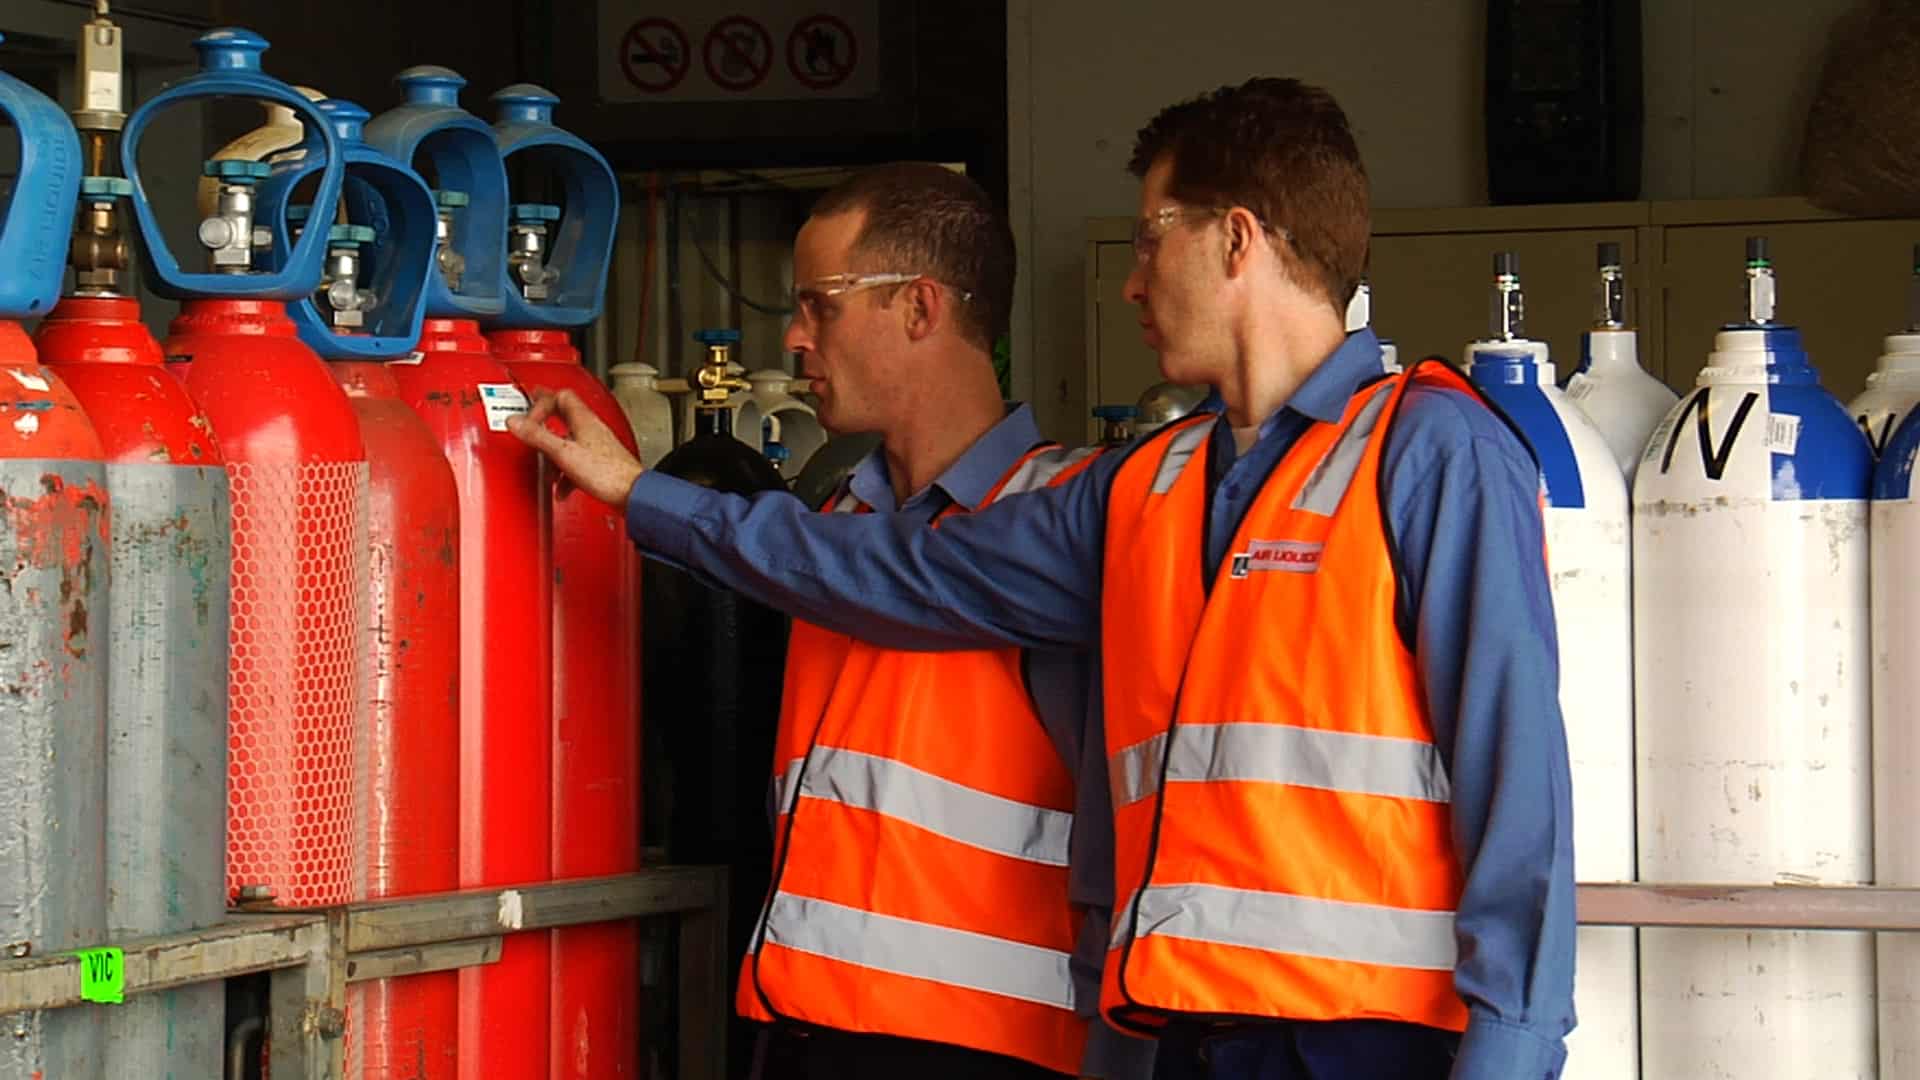
You start with the cylinder. Not the label, not the PSI rating on the valve — the cylinder itself. Most training programs skip the part where you inspect the shoulder stamp. That little area above the valve shows the manufacture date, test pressure, and certification standard. If you can't read a DOT-3AA stamp or identify a requalification date, you don't know what you're working with. I once inherited a rack of argon cylinders at a new facility. Someone had stored them outside for six months with the caps off. Two showed visible denting on the shoulder. One had a cracked valve seal that wouldn't compress past the third thread when I tried to swap the regulator. Nobody caught it during the incoming inspection. That cylinder had been sitting there since 2019 with a slow leak nobody noticed because the training said "keep them indoors." Indoor storage doesn't mean climate controlled. We lost about forty percent of our inventory that month replacing compromised valves. The workaround was simple — I started requiring a three-point inspection on every incoming cylinder: shoulder stamp check, valve threading test by hand, and a soapy water pass before connecting anything. It added maybe five minutes per cylinder. Worth it. Regulator choice matters more than people realize. Oxyacetylene setups use left-hand thread fittings for fuel gases. Hydrogen uses reverse threads too. A standard right-hand thread regulator can physically screw onto a hydrogen cylinder valve if you force it, and that's how you get a regulator off a pressurized tank flying across the room. Training materials usually mention this once in passing. It's the kind of thing that matters at 2 AM when you're working alone.
Here's a detail most programs don't emphasize enough: chain or strap the cylinder every single time, even if it's barely above ambient temperature. A 3000 PSI nitrogen cylinder tipped over breaks concrete. The tank itself becomes a missile. That's not theoretical. I've seen a 50-cubic-foot oxygen cylinder roll about eight feet after hitting a steel table leg, dent the leg, and stop only because someone's foot was in the way. Nobody was hurt but that could've been different by one angle of impact. Leak detection follows a specific method. Soapy water on every connection — regulator to cylinder, regulator to hose, hose to tool. Never use compressed air to check for leaks. Never use a flame. I had a coworker who used a lighter near a helium line once. He learned why that's wrong in the same afternoon he spent at the clinic getting his eyebrows evaluated. We tightened our protocol after that: mandatory soapy water pass documented with initials and date on the cylinder tag before any line goes live. Venting procedures are where most shortcuts happen. You don't crack a valve wide open to clear a line. You open it one-quarter turn at most, stand to the side of the valve outlet, and let it purge slowly. Opening a full-size cylinder valve quickly creates a friction heat event inside the valve seat. I've watched O-rings flash-combine from the heat of expanding gas. The regulator failed within a month of that incident because the thermal shock micro-fractured the internal seals. Slow opens are non-negotiable.
Get the Full Details

Understanding the difference between high-pressure and cryogenic systems comes up constantly in real-world settings. A 9000 PSI helium system behaves completely differently from a liquid nitrogen dewar. High-pressure systems store energy in compressed gas. Cryogenic systems store energy in phase change. Both are dangerous, but the failure modes are different. High-pressure failures tend to be explosive decompression events. Cryogenic failures are typically rapid expansion — liquid turns to gas at a ratio of about 694:1 for nitrogen. A sealed container full of liquid nitrogen will exceed its relief valve capacity and rupture well before the pressure becomes survivable. Training has to address both scenarios separately, not lump them together. The documentation piece is often treated as bureaucratic noise. It isn't. A proper training record tracks who received instruction, what topics were covered, when refresher training was completed, and what the evaluator signed off on. If an incident occurs and your documentation is incomplete, regulators don't care about intent. They care about whether you can prove the person at the bench was trained on the specific procedure that failed. I've seen incidents where the training file showed a generic gas handling course but the employee was assigned to a phosphine line that required additional hazmat-specific training. The gap cost the company a citations and a settlement. One thing worth knowing: gas compatibility charts aren't optional reading material. Acetylene reacts with copper above 15 percent copper content in the alloy. Brass fittings in an acetylene system are a legitimate explosion risk. I've seen it happen — a brass compression fitting on a low-pressure acetylene line developed a hot spot from a slow leak mixing with air, ignited, and blew the entire manifold. The training should make clear which materials are incompatible with which gases before you ever assemble a single joint.
PPE varies by gas type. For inert gases like argon and nitrogen, the main hazard is asphyxiation in confined spaces. A half-mask respirator won't help — these gases displace oxygen and you can't filter your way out of that. Only supplied-air protection works. For reactive gases like chlorine or ammonia, chemical cartridge respirators rated for those specific gases are required. The training needs to specify which PPE applies to each gas class in your facility. General "wear appropriate PPE" language is useless during an actual incident. Here's the uncomfortable truth about most compressed gas safety training programs: they're designed to pass an audit, not to prepare you for failure. The scenario-based portions are usually generic. Real training should include at minimum one hands-on emergency drill per gas class you work with. Simulate a regulator leak. Have the trainee isolate the cylinder, vent the line safely, and replace the faulty component while wearing the correct PPE. Time matters. Panic response matters more. The drill reveals gaps that a PowerPoint presentation never will. Refresher training isn't something to defer. OSHA recommends annual refresher for compressed gas handling. The actual interval depends on your incident history and operational changes. If you're adding a new gas to your floor, the existing crew needs updated training before that gas is connected. If you change suppliers and the cylinder valves shift from CGA-540 to CGA-510 fittings, that's a procedural change requiring retraining. Don't wait for the annual cycle to address active modifications.
The best compressed gas safety training I've ever participated in lasted three days and involved zero slides in the first two. We spent day one doing cylinder inspections until we could identify a compromised unit blindfolded. Day two was regulator disassembly and reassembly on eight different gas types. Day three was emergency response scenarios with real gauges and real cylinders at low pressure. The instructor was a retired fire marshal who'd responded to seventeen compressed gas incidents. He didn't need slides. The smell of that third-day scenario chamber — yes, they used safe odorants for training — stays with you longer than any handout ever could. If you're putting together a program for your facility, start with a hazard inventory. List every gas you handle, the pressure ranges, the storage configurations, and the downstream applications. Map the risks for each one separately. Then build the training around those specific hazards instead of a generic catalog. It takes more upfront work but it produces people who actually recognize the warning signs before something goes wrong.