Getting the Coverstar Cs3000 Running Properly
Most people buy a Coverstar Cs3000 and immediately hit a wall because the documentation doesn't quite line up with what actually happens on the bench. I spent about three weeks getting mine operational the first time around, partly because I jumped straight into wiring without reading the manual thoroughly enough, and partly because the manual assumes you already know how these controllers behave. Here's what I figured out the hard way. The official manual lives on the Coverstar website under their support or documentation section. It's usually tied to a specific firmware version, which matters more than people realize. If you're downloading it from a third-party site or a forum link someone posted in 2019, check the firmware version number on page one before you follow any of the instructions. I ran into a situation where an outdated manual had wiring diagrams for an older driver board that didn't match my machine. It cost me two burnt stepper drivers before I caught it. Always verify your controller board revision against the manual's specified range. If the official source is slow or the download page is down, you can sometimes find archived copies through Coverstar's dealer network. A quick call to whichever dealer sold you the machine usually gets them to email you the current PDF. They're generally responsive about that.
The Mechanical Setup — And Why It Matters More Than the Software
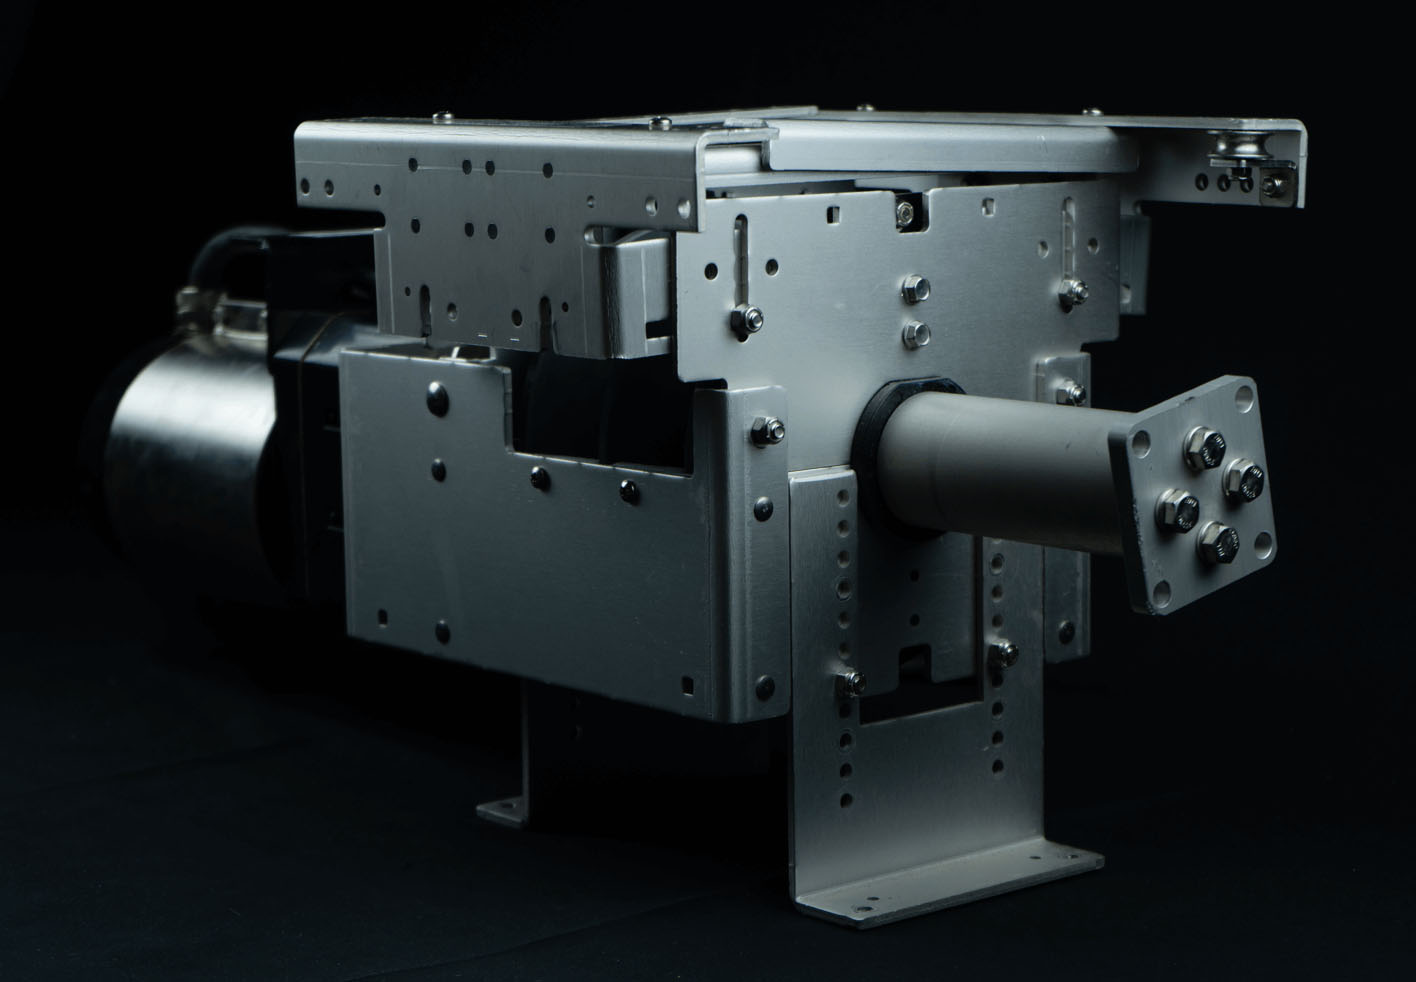
The manual walks you through assembly, but it glosses over a critical detail: rail squaring. The Cs3000 uses linear rails on all three axes, and if you torque the mounting bolts in a single pass, you'll bind the gantry. What actually works is torquing everything to about thirty percent initially, running the axes through their full travel by hand, checking for resistance spots, then going back and finishing the torque in a cross pattern. I once skipped this step and ended up with a consistent 0.15mm drift on the X-axis over a 600mm run. Took me four hours of shimming to fix something that ten minutes of proper torquing would have prevented. The Z-axis is another common failure point. The manual shows you mounting the spindle bracket and connecting the motor, but doesn't emphasize that the belt tension has to be checked before you close anything up. Loose belts on this machine cause step loss under load, and since the spindle can draw significant current when cutting dense material, you'll notice it most during deep passes. Dial it so there's maybe five to seven millimeters of deflection when you press the belt midway between the pulleys. Anything tighter and you're loading the bearings unnecessarily; anything looser and you're inviting missed steps.
Wiring and Controller Configuration
The Cs3000 typically ships with a parallel port or USB-based controller board, depending on the production year. The manual provides terminal block diagrams, but the real-world issue is cable management and grounding. I've seen ground loops cause inconsistent homing behavior on multiple machines, and the fix was always the same: star-ground everything to a single point on the frame, and keep the digital and analog ground paths separate until they meet at that one junction. When you connect the stepper drivers, double-check the phase order. The manual will tell you which wire goes where, but drivers shipped from the factory aren't always matched to the diagram if the batch changed. The quickest verification method is to disconnect the motor from the machine, power on the controller in jog mode, and watch the motor shaft spin in the expected direction for each axis. Reverse the A+ and A- connections on any motor that spins backward, then reseat and test again. Doing this before you bolt anything down saves a tremendous amount of debugging later. For the spindle, the manual covers both direct-connect and VFD-controlled setups. If you're using a VFD, the manual's wiring section for the PWM speed control signal is often the part people get wrong. The low-voltage signal from the controller needs a proper isolated connection to the VFD's analog input — tying it directly to earth ground on both ends can introduce noise that makes the spindle speed oscillate randomly during cuts. A simple optoisolator module between the controller output and the VFD input solved this on my setup.
Get the Full Details

Software and Calibration
The ControlStar software that ships with the machine handles the basic operation, but the first thing you should do after install is run a verification cut, not jump into production. The manual recommends a test pattern using a square and a circle to check for backlash and scaling errors. I'd add that you should also cut a simple pocket at full spindle speed with the material you actually plan to use. The software's step-per-mm values are calculated from factory motor and lead screw specifications, but real-world friction and belt stretch mean your actual values will differ slightly. A typical adjustment range is plus or minus one to two percent from the default. Homing sequence configuration is another area where the manual is adequate but not complete. By default, the machine homes to negative limits on all axes, which means your work zero is somewhere in the positive direction from the machine origin. This is fine for most setups, but if you plan to use a probing system or need to reference a specific fixture point, you'll want to adjust the home offset values in the software after your first successful homing cycle. The manual mentions this in a footnote but doesn't walk through the exact menu path clearly.
Known Limitations and When the Cs3000 Starts Showing Its Age
The machine is solid for light to medium-duty work, but it has clear boundaries. The rigid chain drive on the X-axis works well until you start pushing near the maximum feed rates the manual specifies, at which point vibration becomes noticeable and surface finish degrades. If you're doing finish work on hardwoods or composites, keeping feed rates at about eighty percent of the manual's maximum will give you noticeably better results. The Z-axis also has a limitation worth noting: the manual states a maximum cutting depth per pass that assumes reasonable material hardness. When cutting something like aluminum or dense plastics, you'll want to halve those per-pass depths to avoid servo overload alarms. The parallel port interface on older units is another bottleneck. Modern PCs don't include them, and USB-to-parallel adapters are notoriously unreliable for real-time CNC motion control. If you're running an older Cs3000 on a newer machine, budget for either a proper motion control card or a retrofit kit from Coverstar. The adapter approach might work for hobby-level projects, but it'll struggle with anything requiring consistent high-speed operation. Replacement parts availability varies by region and model year. Some driver boards and spindle assemblies are no longer manufactured as standard items, and Coverstar may substitute a newer equivalent. When that happens, the manual's troubleshooting section becomes less useful because the fault codes and behavior can differ between board revisions. Keeping a copy of the original manual for reference alongside whatever documentation you get for replacement parts is the practical move.
If your primary use case involves large-format work or continuous industrial operation, you might find the Cs3000's frame rigidity and duty cycle limiting. The machine is designed as a precision desktop/compact CNC, not a production workhorse. For that application, the next step up in the Coverstar lineup or a different brand built around a heavier cast-iron frame would be more appropriate. Knowing what the machine is actually good for — and where it starts to fall apart — saves more headaches than any amount of tweaking will fix.