Understanding and Maintaining the Cummins KTA19-G3 Natural Gas Engine
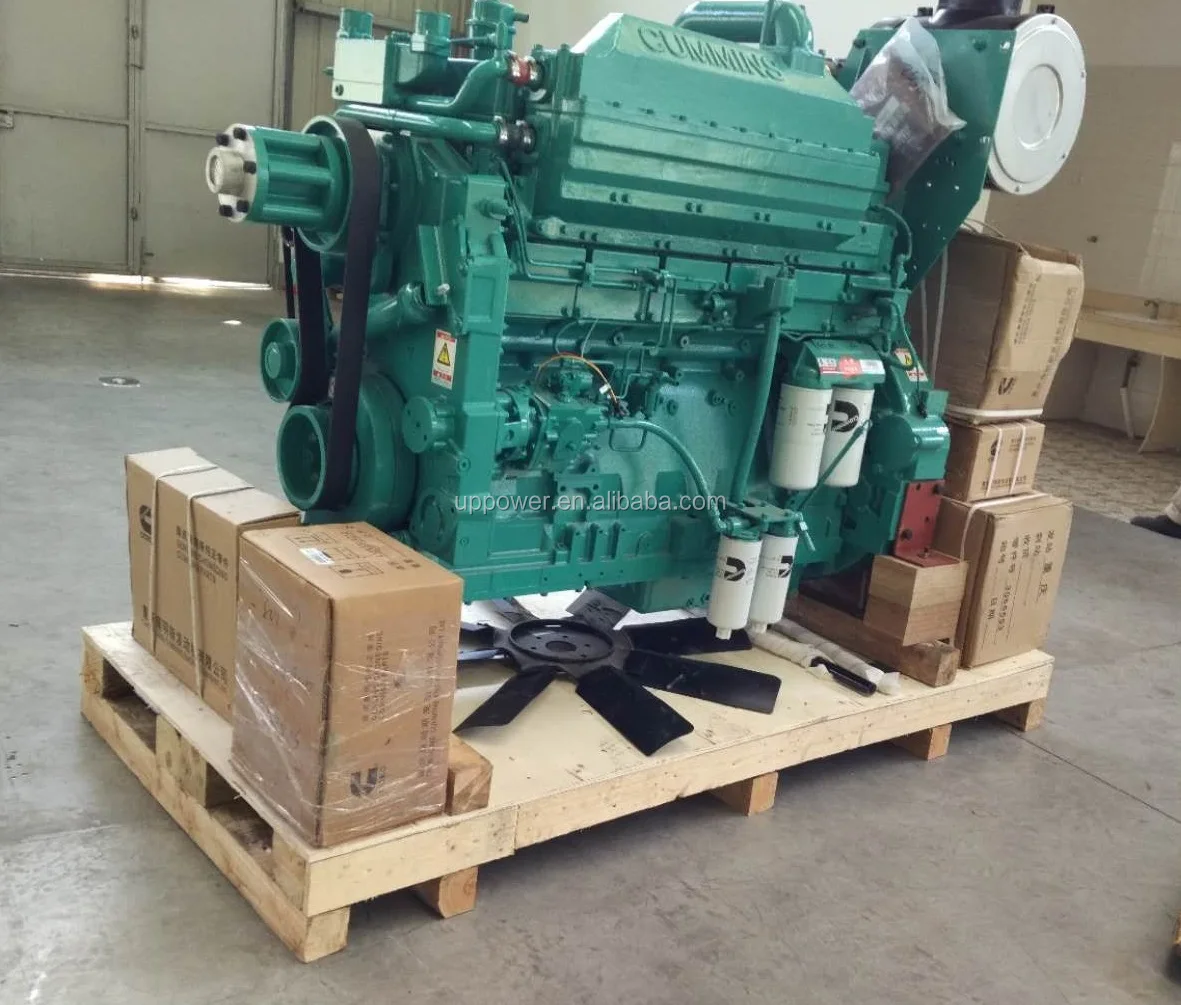
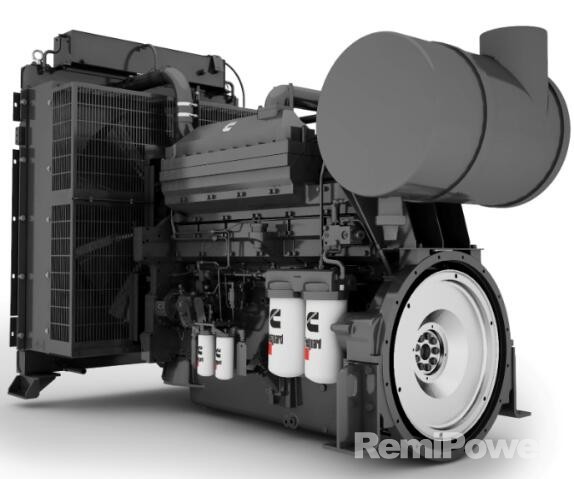
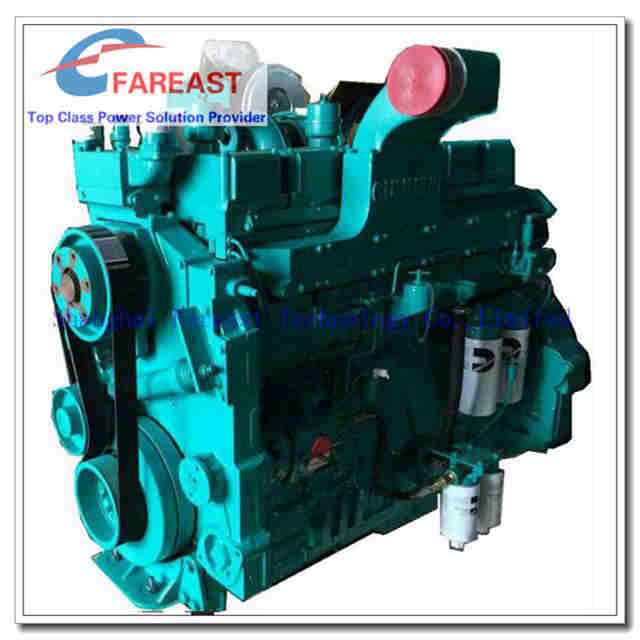
The KTA19-G3 is a 19-liter, naturally aspirated, lean-burn natural gas engine built by Cummins. It is most commonly found in stationary power generation packages from the late 1990s through the mid-2000s. Output ratings typically range from 150 to 250 kW depending on the generator package and configuration. It uses a four-stroke, six-cylinder in-line layout with a single overhead cam per bank, two valves per cylinder, and a port-injection gas system. The G3 designation refers to the third-generation combustion control module and gas delivery hardware. The G3 controller is the main thing that differentiates this engine from earlier KTA19-N models. It manages gas-to-air ratio, ignition timing, and knock detection through a dedicated electronic control unit. The system is fundamentally solid but it has some quirks that will bite you if you treat it like a modern digital engine. The G3 module communicates on a proprietary bus, and diagnostics require either a Cummins service tool or a properly wired serial interface. Using a generic OBD2 scanner will get you nowhere. The fault codes are specific: P0 codes for electrical issues, P2 codes for sensor problems, and P3 codes related to the gas valve assembly. I keep a printed pinout diagram from the service manual in my toolbox because the connector housing degrades over time and the wire numbers fade out. One thing beginners consistently get wrong is the gap between the ignition coil and spark plug. The specification calls for 0.020 to 0.030 inches, but in practice I have seen mechanics set it to 0.040 because they assumed more gap meant stronger spark. That weakens the flame kernel on lean mixtures and causes misfires under load. The fix is using a proper feeler gauge, checking each plug individually, and replacing coils that show carbon tracking on the insulator. Another issue is the gas valve calibration. The G3 expects a certain flow curve from the primary and secondary gas valves. When you swap in an aftermarket regulator or modify the gas train without recalibrating the valve stroke in the controller, the engine runs rich at idle and leans out under load. I encountered this on a 200 kW genset at a water treatment facility where the original gas valve had failed and been replaced with a compatible but slightly different unit. The engine ran roughly above 75 percent load and threw intermittent P2-11 codes. The workaround was pulling the G3 parameters, adjusting the valve offset in the service menu, and verifying the actual air-fuel ratio with a wideband O2 sensor at multiple load points. It took about three iterations and roughly 45 minutes total to get it stable. That is faster than replacing the entire gas delivery assembly, which would have cost nearly three times as much in parts and downtime.
Maintenance intervals on the KTA19-G3 are straightforward but not optional. Oil changes every 250 hours using Cummins CES 20081 or equivalent CJ-4 grade diesel engine oil. The oil filter should always be replaced at the same interval, and the filter housing gasket needs inspection because it hardens and leaks after about five years. Coolant is changed every 500 hours or annually, whichever comes first, using a pre-mixed 50-50 ethylene glycol solution with Cummins Coolant Supplement. Failure to add the supplement results in silicate dropout and water pump seal degradation within 18 months. The fuel filter on the gas train is a 5-micron unit that should be changed every 1,000 hours. I have seen operators extend this to 2,000 hours on clean pipeline gas and nothing bad happened, but on truck LPG or biogas installations that delay will clog the gas valve orifices and cause erratic idle. The timing system on this engine is a gear-driven single OHC per bank with a hydraulic tensioner. The recommended adjustment is every 2,000 hours or when removing the valve covers. The valve lash specification is 0.010 inches intake and 0.015 inches exhaust at operating temperature. If you check cold, add 0.005 inches to both. One practical tip that saves time: mark each rocker arm with a number before loosening them. The shims are not interchangeable between banks and the keepers fall into the valley if you are not careful. I use a magnetic tray and a small piece of tape with the cylinder number written on it. This cuts reassembly time from about 90 minutes down to roughly 35 minutes on a first attempt, and nearly eliminates the chance of mixing up components. Common failure points worth monitoring are the ignition control module and the knock sensor wiring. The knock sensors are piezo elements mounted in the block between cylinders three and four, and three and five. The wiring harness routes past the exhaust manifold and the insulation cracks after about eight years. I check the harness with a multimeter for continuity to ground every oil change. A cracked wire here causes false knock signals and the G3 pulls timing aggressively, which reduces power and increases exhaust gas temperature. Replacing the harness section costs around $180 in parts. Replacing the entire engine due to unaddressed knocking from incorrect timing maps runs considerably more.
The G3 controller itself is a known weak point in older packages. The electrolytic capacitors inside dry out after 12 to 15 years and cause startup failures or erratic sensor readings. The module is repairable by replacing the capacitors and reflowing the solder joints on the power board, but the cost of a refurbished unit from a source like Cummins Authorized Parts or a reputable aftermarket supplier runs between $600 and $900. A complete bench rebuild with new capacitors, optoisolators, and a fresh firmware flash takes about two hours of work and costs roughly $85 in components. I prefer doing the rebuild myself when the board is just capacitor-related because it is predictable. When the module has water damage or corrosion on the connector pins, replacement is the safer call. Performance testing after any major service should include a full load acceptance test. Run the engine at no load for ten minutes, then step the load in 25 percent increments and hold each for five minutes. Monitor exhaust gas temperature at each cylinder using a pyrometer, air-fuel ratio with the wideband, and engine RPM stability. Acceptable EGT variation between cylinders is plus or minus 25 degrees Fahrenheit. Variation beyond that indicates a carburetion or valve issue that needs further investigation. This test takes about 30 minutes and catches problems that a simple no-load run will miss entirely. The KTA19-G3 is not a high-revving or technologically advanced engine by modern standards. It does not have variable geometry turbocharging, common rail injection, or emissions systems that require diesel exhaust fluid. That is also its advantage. The mechanical simplicity means parts are available, diagnostics are accessible with basic tools, and the learning curve for competent maintenance is shallow. What it lacks in refinement it makes up for in durability. I have seen units running above 25,000 hours on a single overhaul with only scheduled maintenance. The ones that fail early almost always fail because of neglected fuel quality, incorrect ignition timing adjustments, or improper gas valve calibration after a repair. Track your operating hours, keep a logbook, and address small issues before they become catastrophic failures. That is the only real secret to getting long service life out of this platform.
Get the Full Details