How to Actually Use a Dial Caliper Without Making Stupid Mistakes
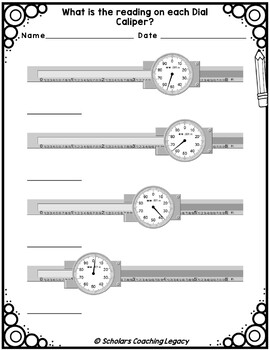
A dial caliper is a measuring tool with a rotating dial face that shows fractional readings alongside the main scale. You slide the jaw along a ruled beam, and the dial gives you a quick readout in thousandths of an inch or hundredths of a millimeter. It sounds trivial. It isn't, if you rely on it without understanding where it drifts. I'm going to walk you through the process of using one properly, and then I'll share a Dial Caliper Worksheet you can print and keep at your bench. I put it together because the ones I found online were either outdated or missing the part about zeroing under measurement pressure, which is something most people get wrong.
Dial Caliper Worksheet
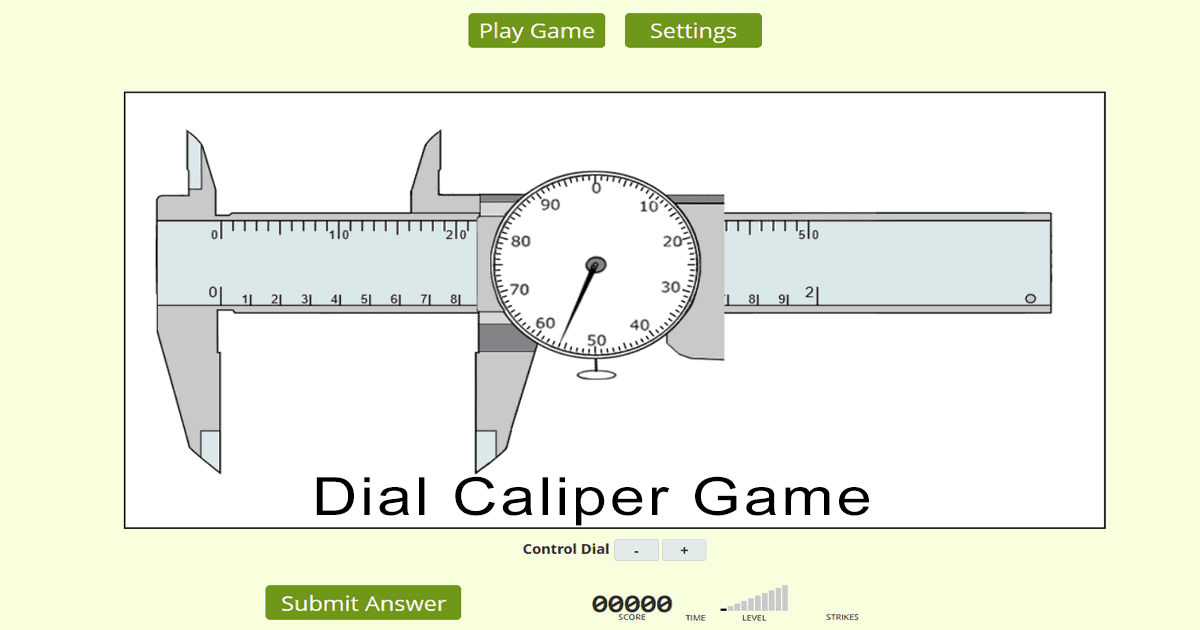
The worksheet covers the basic reading method, common error sources, calibration checks, and a quick-reference chart for zero verification. You can download it from the link below. Before that, let's talk about how the thing actually works in practice. The main beam has a linear scale. The sliding jaw moves along it. The dial is connected to a gear train that translates jaw movement into rotational display. When you close the jaws on an object, the dial shows you the fraction of a unit while the beam scale gives you the whole number. Here is the method. Close the jaws gently on the workpiece. Do not force them. Take up just enough contact to feel resistance, then stop. Lock the thumb screw if yours has one, remove the caliper from the part, and read it. Reading while the tool is still touching the workpiece introduces parallax error from the angle you're looking at the dial face. Hold it level with your eye, not from above or the side.
For inch calipers, the beam is typically marked in inches with subdivisions of one tenth, and the dial reads in thousandths. A metric caliper has millimeter graduations on the beam and the dial reads in hundredths of a millimeter. If your dial has 100 divisions and one revolution equals one millimeter, each tick is 0.01 mm. That is the standard. Some cheaper models have 50-division dials where each tick is 0.02 mm. Check your tool before you trust it.
Get the Full Details

The Zero Problem
This is where most people fail. A dial caliper does not stay at zero forever. Temperature changes, impact from dropping it on the floor, wear on the rack and pinion, and even just normal use will shift the zero point. You need to check it before every measurement session and re-zero if needed. To check zero, close the jaws completely. The dial should read exactly zero and the beam's zero mark should align with the zero of the dial scale. If it is off by even a small amount, you can usually adjust it by loosening the dial face retaining ring and rotating the face until the needle points to zero. Not all dial calipers allow this. Some are sealed. If yours is sealed and zero is off, you have two options: apply a correction factor to every reading, or replace the tool. A correction factor is acceptable for shop-floor work where tolerance allows it. It is not acceptable for gauge-proof inspection work. I learned this the hard way. I was measuring bearing housings on a batch run, and the parts kept coming in slightly out of spec. I blamed the CNC program. I blamed the material. I spent three hours chasing a phantom issue before I closed the caliper jaws and noticed the dial was reading 0.003 off zero. The tool had drifted from being dropped on the concrete floor two days earlier. I should have checked it. Nobody told me to check it. I just assumed it was fine because it looked fine.
Common Pitfalls That Have Nothing to Do with the Tool Itself
First, measuring temperature. Steel expands and contracts. A part that measures 25.00 mm at 20°C will read different at 30°C. The change is small but real. For precision work, calibrate everything to 20°C reference temperature. If you are in a hot shop and the part feels warm to the touch, let it sit until it reaches ambient. Holding a warm part with your hands transfers heat to it and changes the reading as you measure. Second, jaw wear. The measuring faces of the jaws can develop wear patterns from repeated use. Over time they become uneven. A worn jaw might give you a consistent reading on one part and a different one on another, even if both are the same size. Inspect the jaw faces regularly. If you see rounding or flat spots, the caliper needs service or replacement. Third, the locking screw. If your caliper has one, use it. Tighten it after you take the measurement, then remove the tool and read. If you leave the screw loose and drag the caliper across the part surface while reading, you will get inconsistent results every time. This sounds obvious. It is not. I see people do it constantly.
When a Dial Caliper Is the Wrong Tool
Dial calipers are generally accurate to about ±0.001 inches or ±0.02 mm. That is good for general machining and layout work. It is not good for tight-tolerance gauge work. If your specification calls for ±0.0005 inches, a dial caliper is not the right instrument. Use a micrometer or a digital caliper with higher resolution instead. Also, dial calipers struggle with depth measurements on deep, narrow holes because the beam tends to flex. An inside micrometer or a bore gauge is more appropriate there. Digital calipers have their own issues too, mostly battery failure at inconvenient times and sensitivity to metallic dust and coolant contamination on the sensor strip. Dial calipers don't have batteries. They don't short out. They just need occasional cleaning and lubrication of the gear train. That is their main advantage over digital. They keep working when the shop environment is dirty.
Calibration and Maintenance
Clean the measuring faces before every use. A small chip of metal or a speck of dust between the jaws will throw off your reading by enough to matter. Use a soft cloth and mineral spirits or a dedicated tool cleaner. Do not use compressed air to blow debris off the beam. It pushes particles into the rack and pinion mechanism, which accelerates wear. Wipe it down instead. Lubricate the beam occasionally with a light machine oil or a synthetic slideway lubricant. A thin film is enough. Wipe away any excess. Too much oil attracts chips and grit, which turns your smooth sliding action into a grinding one. For calibration, use gauge blocks if you have them. Check the caliper at several points across its range, not just at zero. A caliper might read correctly at zero but have a scale error at the far end. Record your findings. If the error is within the manufacturer's stated tolerance, you can continue using it with a correction factor. If it exceeds tolerance, send it for service or replace it.
Download the Worksheet
The Dial Caliper Worksheet I mentioned is a single-page reference that covers reading the scale, zero verification steps, common error sources, and a quick calibration checklist. It is formatted for standard letter-size paper. Save it, print it, tape it to your bench. Here is the download link. Download Dial Caliper Worksheet (PDF) If you find errors in it or have suggestions for improvement, let me know. I am happy to revise it. I built this for myself first, and I figured if it helps someone else avoid the same mistakes I made, that is worth something.


