So You Need the Edwards 65 Ton Ironworker Manual
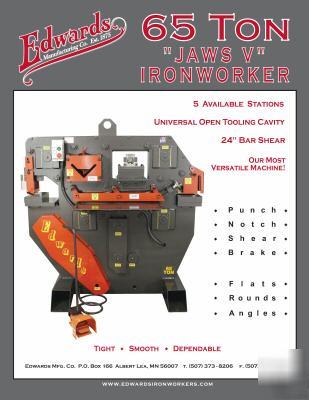
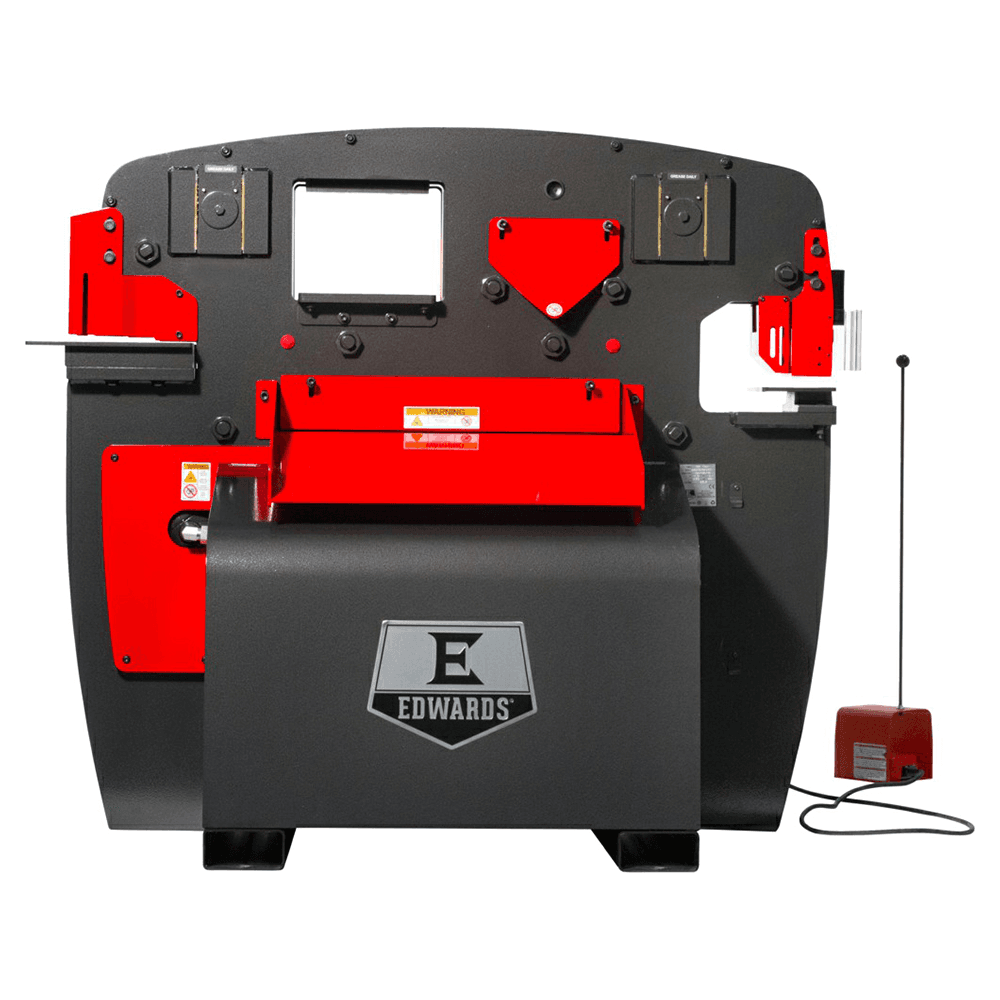
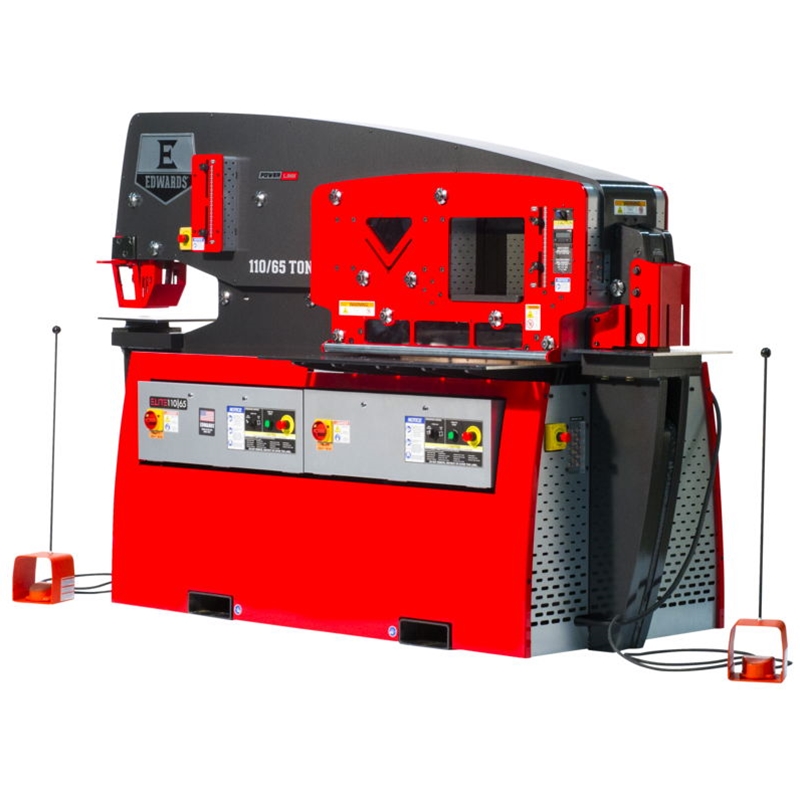
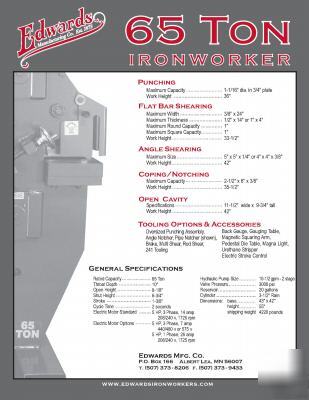
Finding the right manual for an Edwards 65 ton ironworker isn't as straightforward as you'd think. Edwards Manufacturing Company (based in Elwood, Indiana) produced these machines across multiple production runs, and the manuals vary significantly depending on the year of manufacture and the exact configuration. I learned this the hard way when I pulled a manual off a parts website and found the hydraulic schematic didn't match the pump assembly on the actual machine I was working on. Took me three hours to realize the serial number on the data plate was from a later production run than the manual's revision date. The manual you're looking for covers the combination machine functionality - punching, shearing, and bending operations on a single hydraulic unit. For the 65 ton model specifically, it details the ram capacity, die specifications, stroke length, and the hydraulic system pressure ratings. Most original manuals are around 40 to 60 pages, with separate sections for the punch and die setup, shear blade adjustment, bending shoe configurations, and the hydraulic maintenance schedule. If you're trying to locate a copy, Edwards has historically made these available through their website or by request through their parts department. You'll need your machine's serial number. Without it, you're guessing, and Edwards won't send you the right one. The data plate is typically located on the right side of the machine frame near the hydraulic reservoir. If that plate is missing or illegible - which happens more often than you'd expect on older shop equipment - your next best bet is to check the manual's part number against the component castings on the machine itself.
There are also third-party sources. Industrial manual archives and some equipment dealers compile scanned copies. I've had luck with those, but the scan quality varies. Some are clean PDFs, others are photographed at weird angles with pages curled. Factor in at least an extra thirty minutes if you're working through a poor scan while trying to read a hydraulic pressure setting. Here's something the manual doesn't emphasize enough: the 65 ton rating is nominal. Under real shop conditions, especially when you're punching multiple holes in succession, the hydraulic fluid temperature rises and the effective tonnage drops slightly. I've seen operators try to push the machine past its stated capacity by cycling it rapidly, then wonder why the punch dies were binding in the material. Let the hydraulic system rest for a few minutes between heavy punching jobs. The fluid cooler on these units works, but it's not designed for continuous high-load operation. This detail costs me a bent punch die once - not the kind of expense you budget for on a Tuesday afternoon. Another thing beginners miss is the relationship between the shear blade gap and the die clearance. The manual gives you the specs, but it doesn't walk you through the real-world adjustment process. When you change blade settings for different material thicknesses, you need to adjust both the top and bottom die clearance proportionally. I usually set the shear gap first, then check the punch die clearance by doing a test punch on scrap material of the same thickness you'll be working with. The cut edge should be clean with about ten to fifteen percent burr on the bottom. More burr than that and your clearance is off, which also shortens die life significantly.
The hydraulic system on these machines is straightforward - a gear pump, relief valve, directional control valve, and cylinder arrangement. But the filter location and the drain plug positions vary between production years. The manual covers this, but the diagrams can be cramped. I keep a magnifying glass and a flashlight for the tight spots, especially when tracing lines on the schematic during a troubleshooting session. One specific edge case I ran into: the manual references a specific O-ring kit for the cylinder rebuild, but Edwards updated the cylinder design mid-production without a clear note in the later printings. The new cylinder used a different seal profile. I discovered this when the replacement seals leaked within a week of installation. The workaround was to measure the old seal grooves before removing them and cross-reference with the current kit numbers rather than assuming the manual's part list was current. For maintenance, the manual recommends checking hydraulic fluid every hundred operating hours and replacing it annually under normal conditions. If your shop runs the machine harder than that - and most fabrication shops do - you're looking at fluid changes every six months. Use the fluid grade specified in the manual. Different viscosity ratings affect the machine's cycle speed and tonnage output. I've seen people skip this because the fluid looked fine, but viscosity breakdown doesn't always show visually. If you're working with a machine that's had previous owners or unknown service history, the manual becomes even more critical. You need to verify that whoever worked on it last actually followed the procedures. Missing shims under the ram guides, over-torqued fasteners on the shear blade bolts, improperly seated punch dies - these are the kinds of things that accumulate over time and cause problems that seem to come out of nowhere.
Get the Full Details
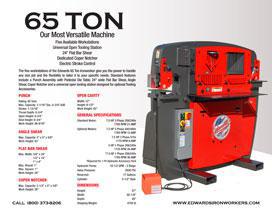
The bending section of the manual covers the standard bender attachments. The 65 ton model typically comes with a pair of bending shoes and a gooseneck die. The instructions for setting up bends are adequate, but the manual assumes you already know basic metal forming principles. It doesn't teach you how to account for springback across different material grades. Mild steel, hot rolled versus cold rolled, different temper conditions - they all behave differently. A 90-degree bend in one piece of stock might come out at 87 degrees in another piece from the same batch. That's normal, but if you're new to this equipment, it's easy to think something is wrong with the machine when it's just material variation. I'd recommend keeping a logbook alongside the manual. Track your fluid changes, die replacements, any adjustments you make, and any issues you notice. It makes troubleshooting infinitely easier later, and it helps you identify patterns - like if a particular die starts wearing faster than expected, or if the hydraulic system seems to lose pressure more quickly after certain types of work. For the actual document, start with the Edwards website parts and support section. If you can't find it there, contact their parts department directly with your serial number. They're generally responsive. Avoid paying suspiciously high prices for manuals on auction sites - most of these are publicly available through proper channels, and people charging premiums are usually just reselling free documents.
One final note on the machine itself: the 65 ton rating sounds substantial, but it's not a heavy structural steel bender. It's designed for angle iron, channel, round bar, and flat stock in the lighter gauge ranges. Attempting to use it for anything beyond its intended scope is where most damage occurs. The manual will tell you the material specifications, but it won't stop you from trying to bend something that shouldn't be bent on that machine.