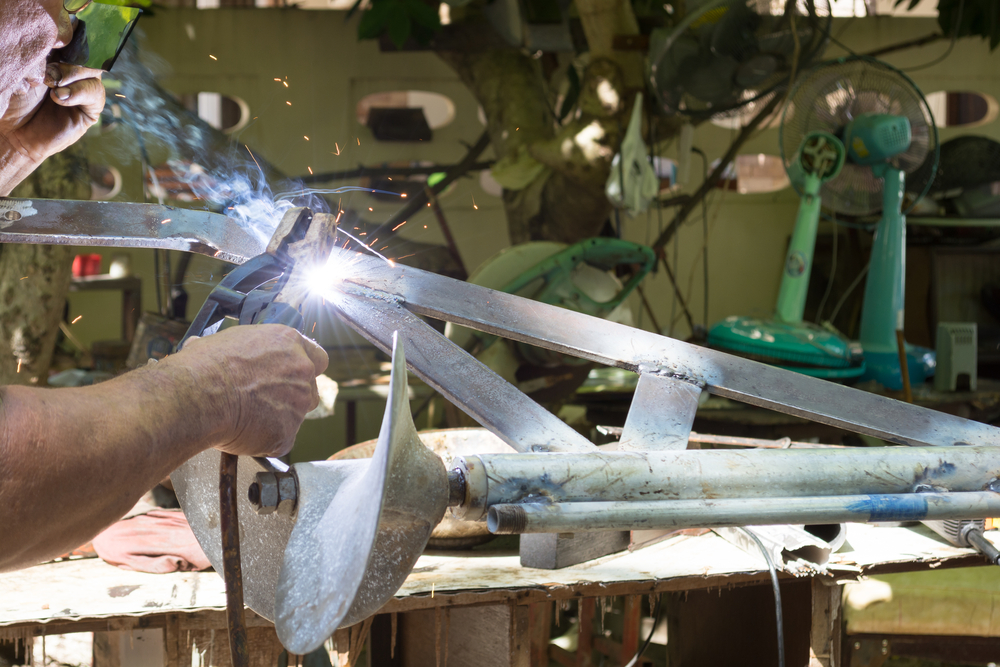
Getting Into Submarine and Marine Vessel Welding
Most people looking at electric boat welding training aren't interested in cosmetic welds on a fishing vessel. They're looking at submarines, salvage craft, and specialized naval ships where weld integrity is literally a matter of whether the hull holds. This is not a field you fumble your way into.Electric Boat Welding Training: What It Actually Involves
The training path splits into two main directions. Military route goes through the Navy's Welding Specialist "E" school and then on to more advanced programs. The civilian route runs through maritime technical colleges and direct-to-shipyard apprenticeships. Both end up teaching the same codes, but the military version hits harder on procedural discipline from day one. The core curriculum covers GTAW and GMAW primarily. Aluminum TIG work on 5083 and 6061 alloys. Stainless steel welding on 316L for saltwater environments. The qualification process runs through AWS D1.1 and ASTM standards, and if you're heading toward nuclear submarine work, you'll also touch into ASME Section IX. That book is thick and every procedure is tracked like a legal document.I learned this the hard way during my third year working on a commercial submarine repair project. We were welding a new valve flange assembly onto a 316L piping system, double-wiggle GTAW with argon backing. About halfway through the first complete pass on a 6G joint, I noticed a series of micropores forming along the root. Not the kind you can grind out and redo without consequence. The pores were tight, distributed, and they traced back to a small moisture pocket that had collected in the fit-up gap between the flange and the pipe — something the pre-weld inspection checklist never flagged because it's technically a fit-up issue, not a welding issue. The workaround was straightforward but required stopping the whole procedure. I had to re-bevel the joint, dry the area with a propane torch set to the lowest possible flame, wipe it with acetone, and then reassemble with a thin nitrogen purge running through the pipe during welding. That added about four hours to the job. The alternative would have been grinding out the defective weld and starting over, which on a pressurized component in this position could have cost a full day. I chose the purge method. The joint passed X-ray on the first try. After that, I made sure moisture checks were part of my personal pre-weld routine, not just something someone else verified. Understanding the codes matters more than most beginners think. AWS D1.1 covers structural welding, which is where most marine fabrication falls. But once you get into pressure vessels and submarines, ASME Section IX governs the procedure specifications and welder qualifications. The difference isn't academic. ASME requires documented procedure qualification records, specific base metal tests, and a level of parent material verification that AWS doesn't always demand. If you're welding on a boat that sits below the waterline at depth, ASME is your standard. If it's a deck structure, AWS D1.1 is probably sufficient.
The 6G pipe weld test is the gatekeeper. It's the same position test used for the nuclear submarine program and the deep-sea submersible industry. You weld a 6-inch schedule 80 pipe in the horizontal-fixed position, using either GTAW for the root pass and GMAW for the fill and cap, or all-GTAW depending on the specification. The acceptance criteria for radiography under ASME requires zero cracks, zero incomplete fusion, and essentially no porosity above a certain threshold. A single linear indication larger than a fraction of an inch in the weld zone is a reject. This is why the training emphasizes consistent travel speed, proper filler rod technique, and absolutely stable arc length. One thing nobody warns you about until you're actually doing the work: aluminum changes behavior when it gets warm. The thermal conductivity drops as the base metal temperature rises, which means your heat input per unit length increases even if your amperage stays the same. On a 5083-H321 plate that's been sitting in direct sunlight, the same welding parameters that produced good results on a cold piece will give you burn-through on the third pass. The solution isn't to reduce amperage across the board. It's to slow your travel speed slightly on the hot piece while keeping the same electrode angle and arc length. I found this out while welding a hull patch in late July on a boat that had been stationary for three days. The first two passes looked fine. The third pass went straight through the plate at the midpoint. After that, I started checking material surface temperature with an infrared thermometer before I set up the welder, and adjusted parameters accordingly. Back purging is another detail that separates trained welders from people who've watched a few YouTube videos. When you weld stainless steel pipe, the inside surface is exposed to atmosphere unless you seal the ends and introduce inert gas. Without back purging, the interior of the weld root oxidizes immediately. That oxide layer is the first place corrosion starts, and in a marine environment saltwater gets into those micro-oxides within weeks. The proper setup uses copper backing bars or inflatable plastic dams depending on the pipe diameter, and argon flow rates between 5 and 15 cubic feet per hour for the purge side. You verify the purge with indicator tape or a simple oxygen meter — something as cheap as a $30 welding-grade oxygen meter from a supply house will tell you whether your purge is adequate.
NDT education is part of the training, not an afterthought. Visual testing comes first and is where most welders fail. A welder should be able to look at a completed weld and identify undercut deeper than 0.01 inches, excessive reinforcement, and crater cracks without any equipment. Liquid penetrant testing follows for surface-breaking defects, and radiography for subsurface issues. Ultrasound is used for thicker sections where radiography becomes impractical. During training, you spend roughly as much time learning to read the NDT results as you do producing the welds. That's because the shipyard quality engineers don't care how good your technique is. They care whether the weld passes inspection. There's a practical trade-off between welding speed and inspection probability that most training programs gloss over. Pulsed GTAW on aluminum produces cleaner welds with less spatter and better control of the puddle, but it's slower than spray transfer GMAW. For a production shop building dozens of identical assemblies, GMAW might be the better choice despite the higher reject rate. For a one-off repair on a pressure component where the weld will be tested and logged, pulsed GTAW is worth the extra time. Knowing which path your employer expects and preparing accordingly is something experienced welders figure out quickly. New trainees often don't. The certification process itself follows a structured sequence. You start with basic code qualification, then move to special position testing, then to project-specific procedure qualification records if you're working on something like a submarine hull section. Each qualification has an expiration window — typically two years of documented activity before you need to requalify. If you go six months without welding to code, some programs require a reassessment even if your two-year window hasn't closed. Employers in this space don't tolerate expired qualifications.
Get the Full Details
Cost estimates for a complete training path range from $8,000 to $25,000 depending on the program and whether you go through a union apprenticeship, a technical college, or a direct shipyard program. Union apprenticeships tend to be the most thorough but also the most demanding, usually requiring three to five years to complete. Technical college programs can get you qualified in eighteen to twenty-four months with less hands-on hours but faster completion. Direct shipyard programs are rare and usually require you to already have welding experience before they'll train you for marine-specific work. The biggest bottleneck in this field is the shortage of qualified welders willing to work in the conditions. Submarine and salvage welding often takes place in confined spaces, at elevation, and sometimes in saltwater-adjacent environments where the air quality is poor. The pay reflects that — starting wages for qualified marine welders typically run $28 to $35 an hour, with experienced welders on submarine projects making $45 to $60 an hour plus benefits. But the work schedule can involve extended dock time with long hours and no flexibility. You don't enter this for a balanced life. You enter it because the work is technically demanding and the pay is better than most welding specialties.