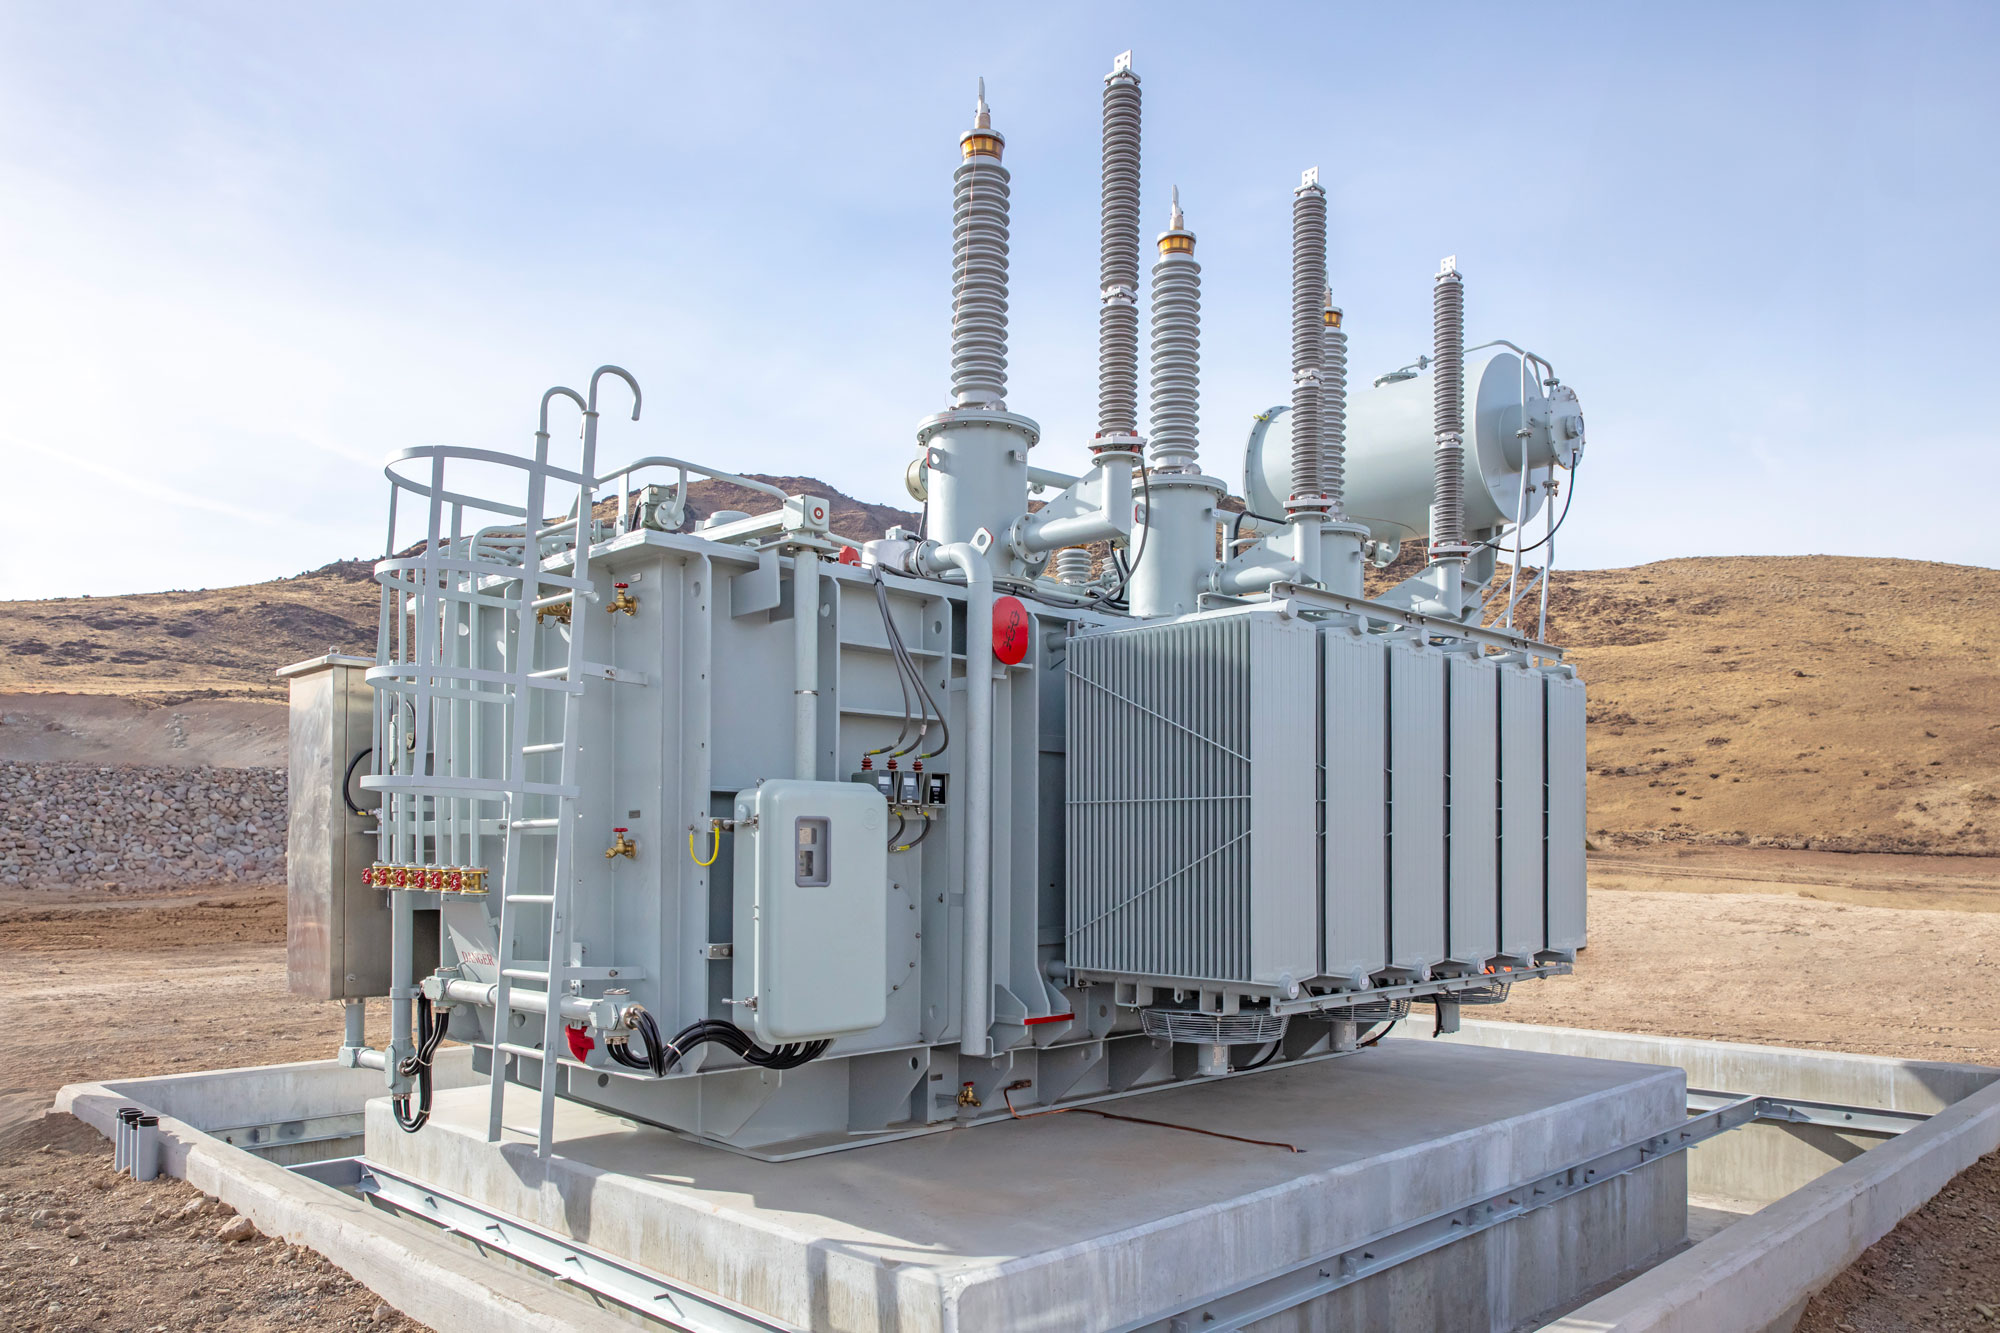
Testing Rotating Machines Without a Full Load Bank
You do not need a massive resistive load bank to evaluate a machine. I learned that the hard way. A few years back I was brought in to diagnose a 75 kW induction motor that kept tripping on thermal overload during seasonal commissioning runs at a water treatment facility. The plant could not afford a full mechanical load. They needed a quick answer, not a three-week delay waiting for external equipment. I built a simple dynamometer using a second 75 kW motor mechanically coupled to the first one through a flexible coupling and a torque transducer. The driven motor ran as a generator, dumping power through a bank of three-phase resistors sized for about 80 amps at 400 volts. It cost roughly two days of parts and labor. The original problem turned out to be a degraded shaft grounding path causing bearing currents, not any issue with the motor itself. Without that test setup, we would have just swapped the motor and moved on, leaving the real fault intact.
Common Grounding Issues in Electrical Machines And Transformers
Bearing currents are one of those things that never make it into basic textbooks but show up constantly in the field. Variable frequency drives are the usual culprit. The high-frequency common-mode voltage from the inverter finds a path to ground through the motor bearings, and over time that erodes the bearing raceways. You will see fluting patterns on the races if you look. The fix is straightforward: use insulated bearings on the drive end, install a shaft grounding brush, or switch to a sine-wave filter between the VFD and the motor. I have also seen situations where people assume a transformer core is properly grounded because the nameplate says so, but the actual ground strap corroded loose inside the enclosure five years ago. A continuity check across the core-ground terminal and the tank will tell you immediately whether the path is still intact. Do not skip that step when you are performing routine maintenance. It takes about thirty seconds.
Reading No-Load and Short-Circuit Test Data Correctly
Beginners often treat the no-load and short-circuit tests as pure calculation exercises. In practice, the measurements are more sensitive than most people expect. A typical no-load test on a distribution transformer might show a wattmeter reading of 40 watts on a 50 kVA unit. That 40 watts is your core loss. The current draw will be around three to five percent of rated current, and the power factor will be very low, usually below 0.2. Because the power factor is so low, even a small error in the wattmeter reading or the voltage measurement can swing your calculated core loss by several percent. The short-circuit test is equally unforgiving. You are applying just enough voltage to drive rated current through the windings while the secondary is shorted. On a small transformer that might be only 5 to 10 percent of rated voltage. The wattmeter now reads copper loss. At these low voltage levels, instrument accuracy becomes the limiting factor. Using class 0.5 meters instead of class 1.0 meters can save you from significant error in the equivalent circuit parameters you derive from the test data. Here is a practical tip that most people miss: always record ambient temperature during the short-circuit test. Copper resistance changes by about 0.4 percent per degree Celsius. If your test bay is ten degrees cooler than the standard reference temperature of 25 Celsius, your measured copper loss will be artificially low. Apply the standard temperature correction formula before using the data for any thermal rating calculations. The adjustment is routine and prevents you from incorrectly classifying a transformer as operating below its thermal limit.
Get the Full Details
Phase Conversion and Transformer Connections in Real Installations
Scott-T connections still come up when someone needs to convert three-phase to two-phase or vice versa. I ran into this at a small manufacturing site that had vintage two-phase machinery imported from an older European installation. The supply was three-phase. Rather than replace all the equipment, we installed a Scott-T transformer bank to create the missing phase. It worked cleanly, but the balance between the two secondary outputs depended heavily on precise tap selections and matching load characteristics on both phases. An unbalanced load will shift the phase angle away from the ideal ninety degrees, and the auxiliary transformers can overheat if one phase carries significantly more current than the other. For rotating machines, the starting method matters far more than people typically consider. Direct-on-line starting on a large motor draws six to eight times the rated current, which can cause visible voltage dips on the same feeder. Star-delta starting reduces the inrush current to roughly one-third of direct-on-line, but the torque also drops to one-third. That is acceptable for pump and fan loads where startup torque demand is low, but it will stall a conveyor or a compressor. Variable frequency starters solve this by controlling both voltage and frequency from zero, but they introduce their own set of issues with harmonic distortion and filter requirements.
Protection Coordination That Actually Works
Differential protection on transformers sounds simple in theory. You compare the current entering and leaving the windings through matched CTs, and any difference trips the relay. The reality involves several details that catch people out. CT ratio mismatches between the high-voltage and low-voltage sides must be compensated, either through CT choice or relay settings. Magnetizing inrush current from transformer energization can appear as a differential current and cause a false trip. Most modern relays use second harmonic restraint to distinguish inrush from actual faults, but you need to verify that the restraint threshold is set appropriately for your transformer size and system conditions. Overcurrent protection coordination between the primary and secondary devices is another area where shortcuts create problems. I have seen installations where the downstream breaker would trip before the upstream transformer protection during a sustained fault, leaving the entire transformer isolated from the wrong end of the system. A proper time-current curve overlay showing both devices on the same graph will reveal whether there is adequate discrimination. This analysis usually takes under an hour and prevents months of troubleshooting when a fault does occur. For motors, the thermal overload relay needs to match the actual motor service factor and load profile. A general-purpose relay set to the nameplate full-load current works fine for steady applications, but cycling loads or frequent starts require a more sophisticated motor protection relay that tracks the thermal model in real time. These relays cost more but prevent the annoying nuisance trips that lead operators to disable protective functions entirely.
Diagnostic Testing You Should Be Doing Annually
Winding resistance testing between phases should be within one percent of each other on a healthy machine. Larger deviations point to connection problems, loose terminations, or internal winding faults. Megohmmeter testing of insulation resistance gives you a baseline number, but trend analysis over multiple years is far more useful than any single reading. A drop of twenty percent from your previous year's measurement on the same winding at the same temperature warrants investigation before it becomes a failure. Partial discharge testing on medium-voltage transformer windings is increasingly common and practical. It detects insulation defects that have not yet caused a breakdown. The equipment is expensive to own, but many companies offer this as a contracted service at reasonable daily rates. A single partial discharge event detected early can prevent a transformer replacement that would cost ten times the test fee. Power quality logging on the supply side of important motor drives is another annual task that pays for itself. Harmonic distortion, voltage unbalance, and transient events are difficult to diagnose without recorded data. A week of continuous logging with a power quality analyzer will typically reveal issues that casual spot-checking completely misses. One installation I worked on had chronic VFD failures that traced back to a nearby arc furnace causing voltage sags and harmonics. The fix required a dedicated filter bank, but identifying the source took us two weeks of logged data analysis.
When to Replace Instead of Repair
There is no universal rule, but a damaged transformer winding repair that costs more than sixty percent of a new unit is rarely worth attempting. The mechanical integrity of old windings degrades even after rewinding, and the new insulation materials may not match the thermal class of the original design. For rotating machines, rotor bar fractures in cast aluminum rotors are generally a replacement decision. Weld repairs on rotor bars are possible but unreliable under full load cycling conditions. Stator rewinds are more justifiable since the laminations themselves often remain serviceable, provided the core insulation has not degraded from prolonged overheating.