Why We Keep Using These Old-School Training Boards Anyway
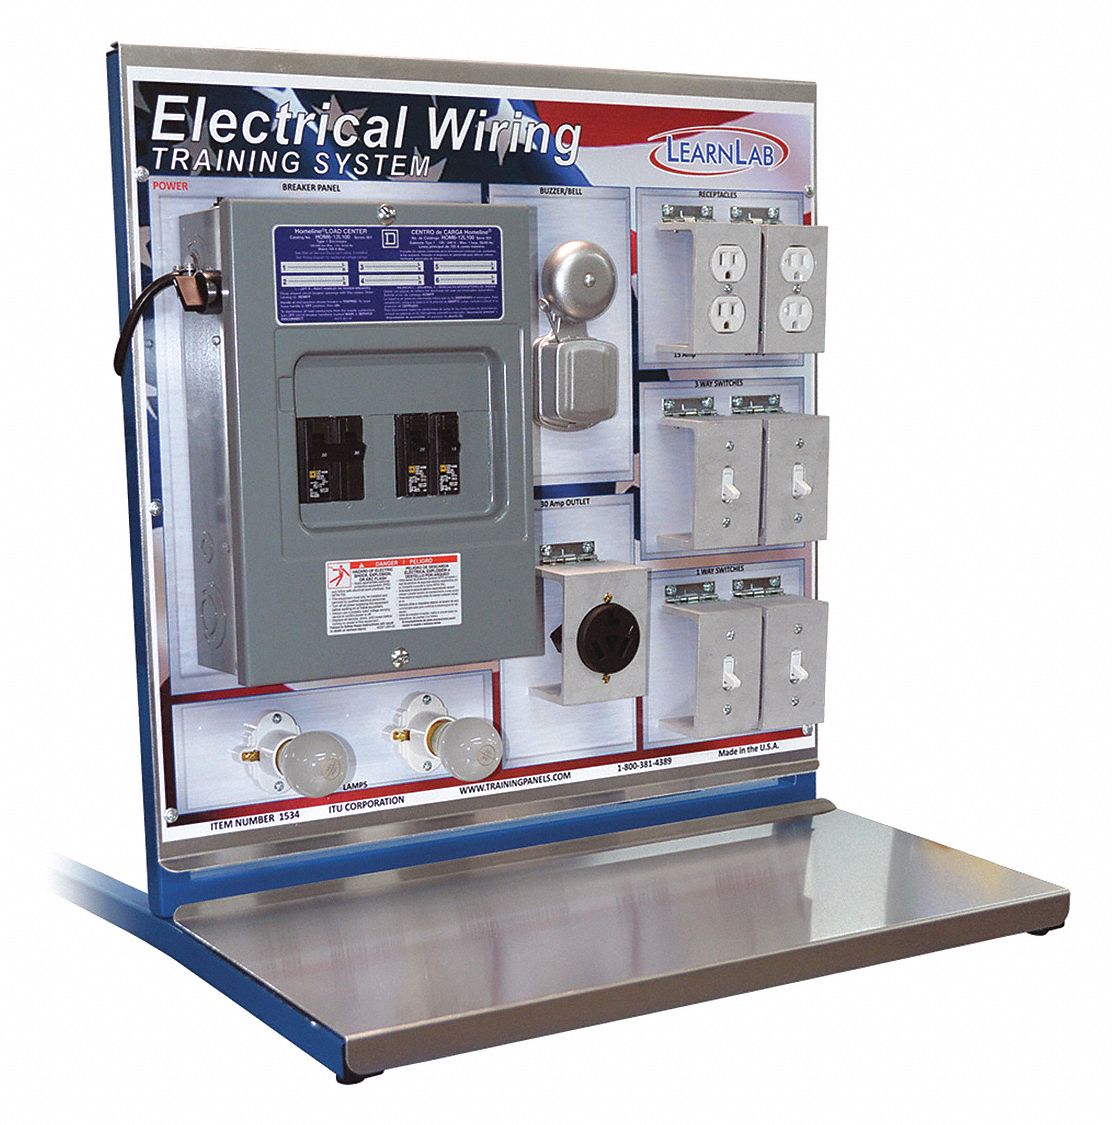
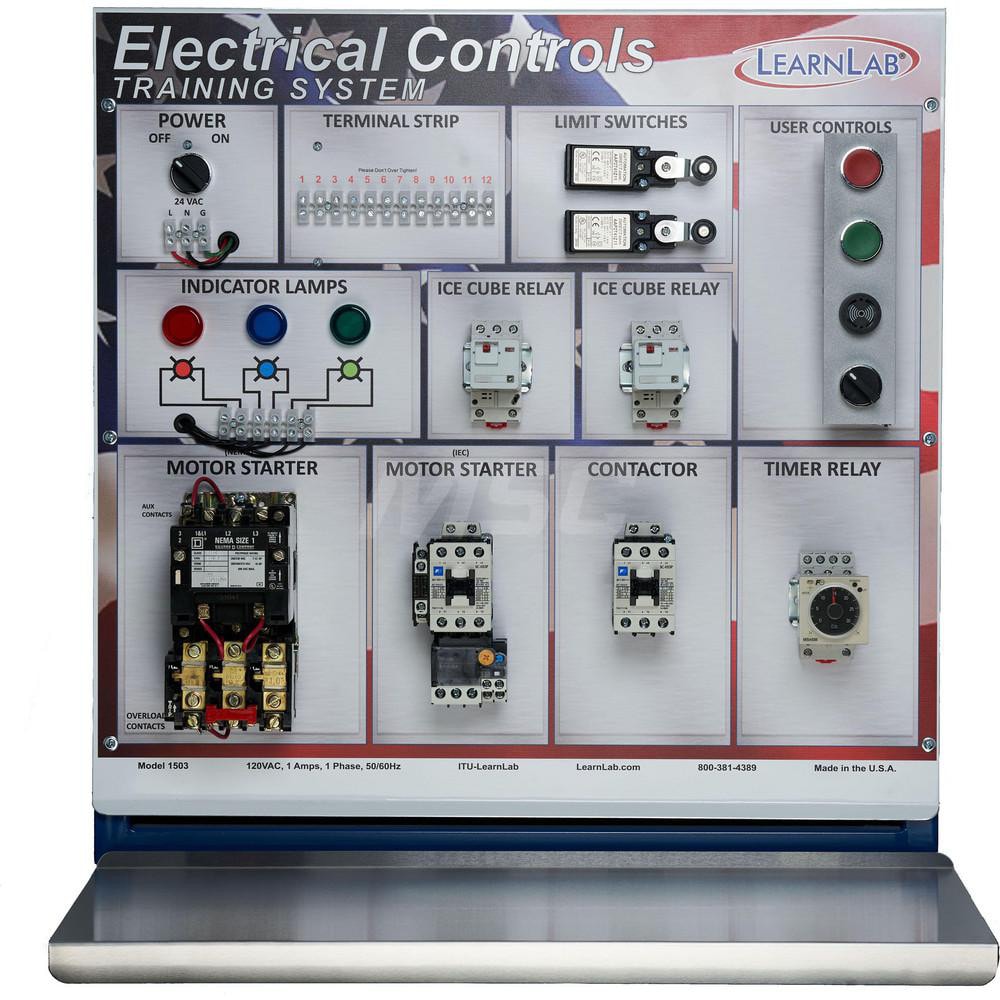
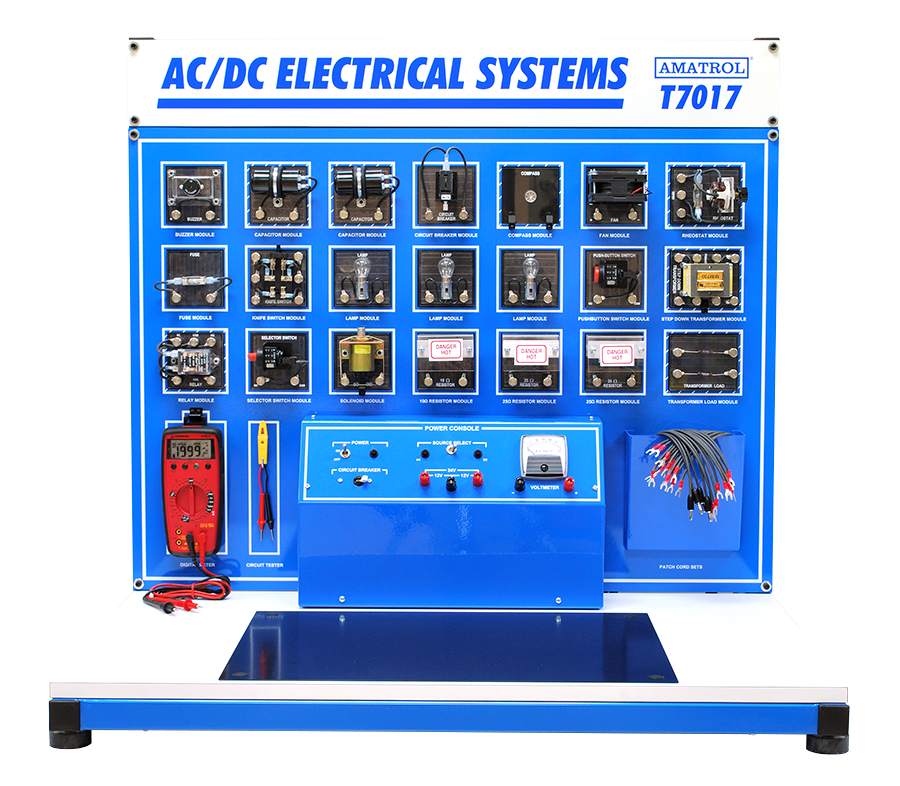
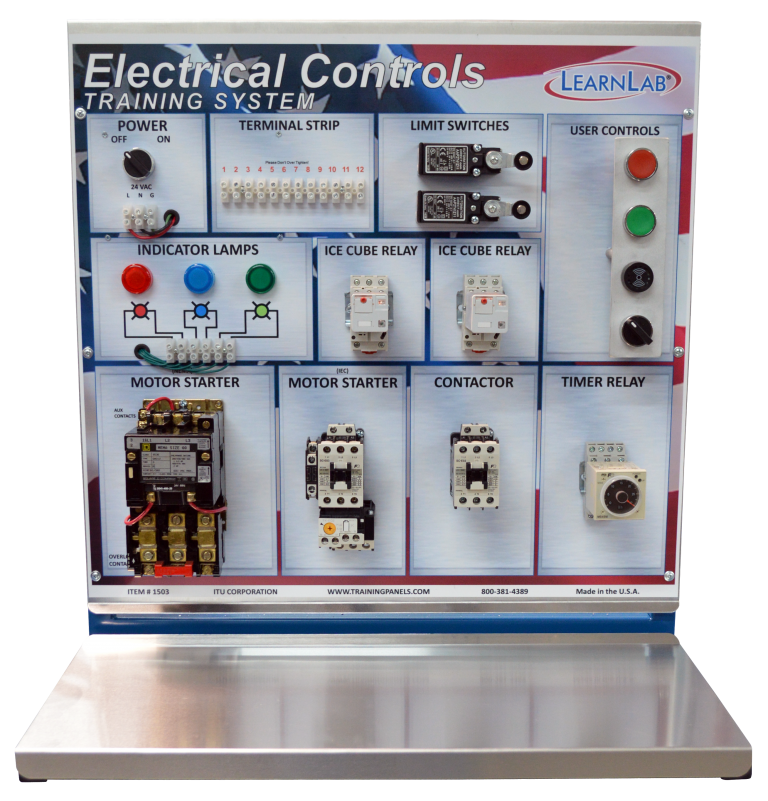
Electrical Troubleshooting Training Boards are exactly what they sound like: a physical panel wired with intentional faults that you have to find using multimeters, clamp meters, and your own patience. Most people go into this thinking it will be a straightforward exercise. It isn't, and that is the point. Before you touch anything, pull the manual. Every board has a fault map or at least a description of where the intentional faults are hidden. If you skip this step, you will waste an hour measuring continuity across perfectly good terminals and then feel like an idiot. I learned that the hard way on my second day with a mid-range unit from a company that no longer exists. The manual was a three-page PDF that had been scanned at 72 DPI. Useless. I had to trace every wire by color and terminal number instead, which took about forty-five minutes longer than it should have but taught me the panel better than any shortcut ever could. Here is the basic workflow. Power off the board. Set up your DMM on continuity or resistance mode. Trace the circuit from the source to the load, checking voltage drops and continuity points. Then power on and measure voltage at key nodes. The faults are usually open circuits, shorted connections, or incorrect wiring — something that a schematic comparison will reveal. Keep your schematic on the bench. Write down every measurement. If a reading doesn't match the expected value, mark it and move on. Don't chase ghosts.
The equipment you actually need is a quality digital multimeter, a clamp meter for live current measurements, and a set of test leads that don't fall apart after three uses. I've seen trainees try to use $8 gas station meters. It doesn't work well. A Fluke 87V or a Klein MM400 will save you from yourself.
The Real Skills These Boards Build
The training boards force you to work through the same decision loop you'll use on a real job site. You observe. You hypothesize. You test. You either confirm or eliminate. Repeat until the fault is isolated. The loop itself is simple. Doing it under time pressure with a board that has three hidden faults and someone breathing down your neck is a different story. One thing most training programs get wrong is the pacing. They throw five faults into a single board and expect you to solve them in an hour. That's not troubleshooting. That's scavenger hunting. A realistic industrial panel has one major fault and maybe one minor one. Stick to boards that simulate that ratio, or create your own realistic scenarios by setting only a couple of intentional issues. I once encountered a board where the "fault" was actually a loose terminal block screw, not a deliberate miswire. The training manual listed it as an intentional fault but never mentioned which terminal. I spent twenty minutesReplacing components before I realized the real problem was mechanical, not electrical. My workaround was to gently tug on every wire at its termination point while measuring continuity. The moment the reading fluctuated, I found the bad connection. That board taught me more than any schematic review session ever has. Loose terminations kill more circuits than bad components.
Get the Full Details
Advanced Nuances Beginners Miss
Most people learn to troubleshoot boards by following the schematic from top to bottom. That's fine for simple circuits. But real-world panels rarely behave linearly. Parallel branches, relay interlocks, and feedback loops mean the fault can hide anywhere, including in areas the schematic makes look healthy. The trick is to divide and conquer. Split the circuit in half and measure at the midpoint. Determine which side has the anomaly, then split that section again. This binary search approach usually cuts your troubleshooting time from two hours down to fifteen minutes on a moderately complex board. Another thing nobody warns you about: phantom voltages. When you set a high-impedance DMM to voltage mode and probe an open circuit that runs parallel to a live conductor, you'll often read a ghost voltage — anywhere from a few volts to nearly line voltage. It's capacitive coupling. Beginners see this and assume a live fault exists. It doesn't. The workaround is simple. Switch to resistance or continuity mode with power off, or use a low-impedance meter that bleeds off the induced voltage. If your board has fluorescent ballasts or VFD outputs nearby, phantom voltages will appear frequently.
The Honest Downsides
Training boards have real limitations. They can't replicate the environmental factors of an actual job site — heat, vibration, moisture, aging insulation. A board fault is always a clean, deliberate wiring error. Real industrial faults are messy. A motor overheats and the overload trips. A contactor welds shut because of arcing from years of use. A ground fault appears only when it rains. The board can't teach you any of that. Another limitation is cost. Good boards run $2,000 to $8,000 depending on complexity. Cheaper units from unknown manufacturers often have faults that are too obvious or circuits that don't match any real-world standard. I've used boards where the "three-phase motor" was wired so simply that no actual industrial panel would ever look like it. That gives trainees a false sense of confidence. If you're investing in a board, verify that the circuits represent real industrial configurations — motor controls, PLC I/O, distribution panels, not just basic lighting circuits. For sites that can't justify the expense, the alternative is building your own troubleshooting panels from scrap components and old control panels pulled from decommissioned equipment. It's cheaper, more realistic, and forces you to deal with actual manufacturer documentation. The downside is it takes time to build, and the faults are only as good as whatever you intentionally put in them.
A Practical Setup Recommendation
If you're setting up a training program, start with a single-phase control circuit board before moving to three-phase. Include at least one ladder logic element so trainees see how relays and timers interact. Add a motor circuit with overload protection. Throw in a simple PLC I/O station if the budget allows. Keep the number of intentional faults between two and four per session. More than that turns the exercise into a punishment, not a lesson. Schedule each session for ninety minutes maximum. After that, cognitive fatigue sets in and the learning value drops off sharply. Document every fault you find. Build a personal reference log. The patterns repeat across different boards and different real-world systems. After enough sessions, you'll start recognizing the symptoms before you even pick up the meter. That's when the training actually sticks.