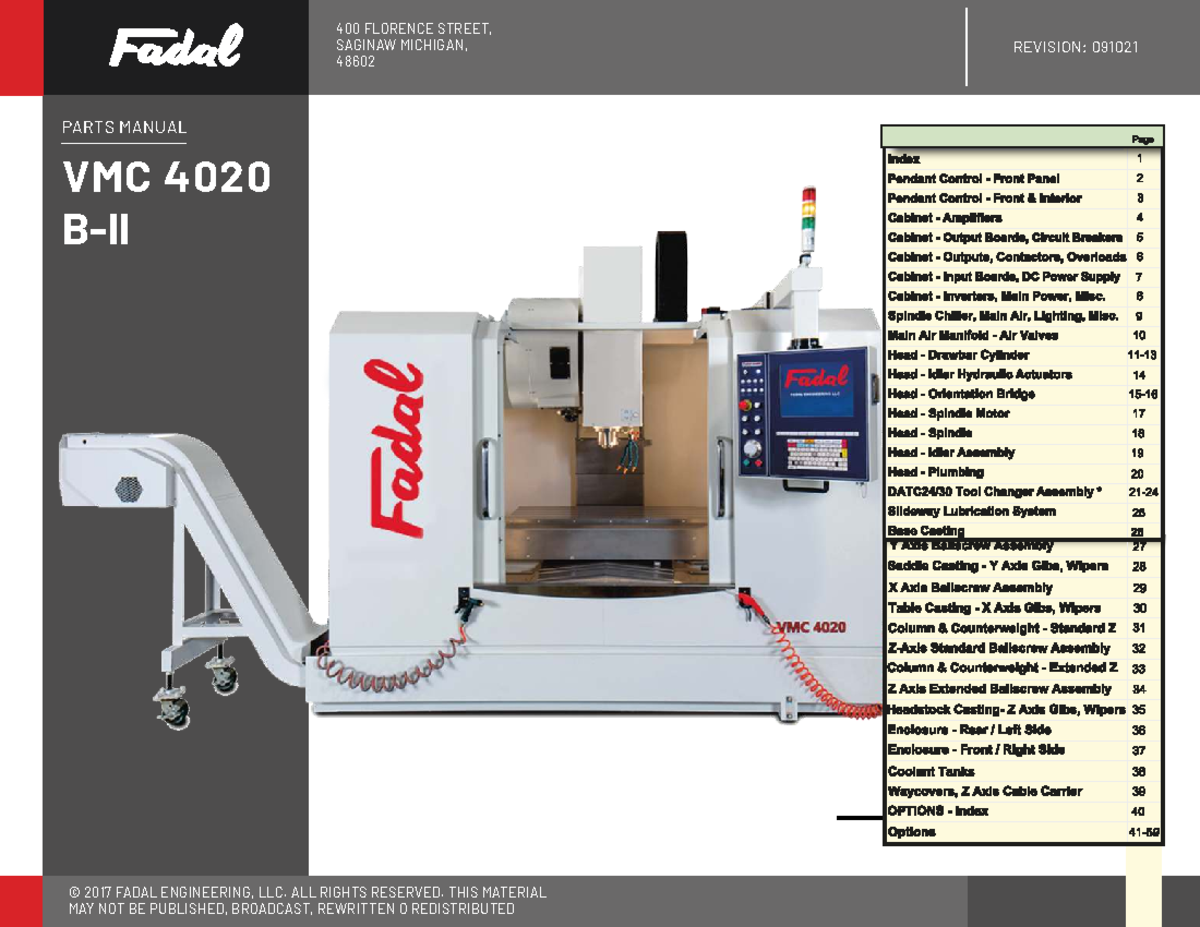
What you need to know before opening the Fadal Vmc 4020 User Manual
The manual is a reference document, not a tutorial. It tells you where buttons are and what codes do. It does not tell you why your X-axis is drifting after three years of production runs or how to hear that the linear guides are about to fail. I have spent more time with these machines than I care to admit. The Vmc 4020 is a solid workhorse. It is also finicky if you treat it like a consumer appliance. You will find the official documentation at Fadal's site or through their customer support portal. If you need the exact Fadal Vmc 4020 User Manual, search their support section or contact a local distributor. Third-party copies circulate online, but they are often older revisions that miss the Fanuc 0i-M updates from the late 2010s. Stick to current versions if you can.
Running the machine versus reading about it
The manual assumes you have clean air, stable voltage, and fresh Wayon oil. Your shop probably has none of those things consistently. I learned this the hard way when my X-axis started exhibiting positional error after a power flicker during a thunderstorm. The backup battery in the Fanuc control dropped below threshold, and the parameter set for backlash compensation reset to factory defaults. I spent two hours hunting through the manual before I found the actual parameter number (1851) that controls X-axis screw pitch compensation. The workaround was loading a saved parameter file from my own backup, which I had only made because I read somewhere that these machines can lose settings during brownouts. Most operators never think to do that. Here is what the manual does not emphasize enough: linear guide preload matters more than you think. The Vmc 4020 uses recirculating ball bushings on all three axes. When the preload springs fatigue, you get micro-play that shows up as chatter marks on aluminum, not as a visible wobble. You can feel it in the cut, not in the display. I use a dial indicator on the spindle nose, locked in position, and watch for movement when I manually rock the table. If there is more than 0.0005 inches of play, I adjust the preload nuts before the manual suggests anything else. Another thing beginners miss: spindle taper cleaning is not optional. The manual mentions it once in the maintenance section. I have seen operators run tool holders against an air nozzle and call that cleaning. It is not. Use a proper taper cleaning swab with solvent, then inspect under bright light. A single carbon particle in the BT40 taper causes tool runout that increases exponentially with RPM. At 8,000 RPM, that runout translates to vibration that ruins surface finish on steel. At 12,000 RPM on aluminum, it can break a tool holder entirely. I check tapers daily now. It takes four minutes. It saves hours of troubleshooting.
Common parameters that need attention
The parameter list in the manual is comprehensive but dry. Parameter 1006 controls servo gain tuning. Factory settings favor stability over responsiveness. If you are running high-speed contouring on 6061 aluminum, you might want to bump the gain up by 15 percent. Do it in small increments. Test with a simple arc cut. Listen for hunting or overshoot. The manual warns about instability but does not give a practical threshold. Parameter 1851 sets screw pitch error compensation. I mentioned this one earlier. If your machine has been in service for more than five years, this parameter needs periodic verification. Load a laser interferometer and compare actual position to commanded position. The manual provides the procedure, but it does not tell you that thermal growth can shift compensation values by 0.001 inches over an eight-hour shift. I run the compensation routine twice a day during summer months when the shop temperature swings. Parameter 813 controls rapid traverse override scaling. The manual says it ranges from 10 to 100 percent. In practice, I set it to 80 percent for production runs and drop to 60 percent for first-off verification. This prevents catastrophic crashes when a program has an error that the simulator did not catch. The manual does not discuss operator psychology, which matters more than you think.
Get the Full Details
Limitations of the system
The Vmc 4020 is a good machine. It is not perfect. The Fanuc 0i-M control lacks modern features like cloud connectivity or predictive maintenance alerts. You get what you pay for. If you need real-time OEE tracking, add a third-party solution like Shopfloor Analytics or OSIsoft PI. The manual does not mention this because it is outside the scope of the base system. Hydraulic chuck pressure drops over time. The manual gives a maintenance schedule. I follow it religiously, but I also monitor pressure with a gauge on the tool changer. If pressure falls below 800 PSI, I replace seals before the manual suggests inspection. This prevents tool dropouts during high-speed drilling. The manual does not discuss the cost of a single dropped tool in a production environment. Coolant pump failure is the most common cause of downtime. The manual covers replacement procedures. I keep two spare pumps on the shelf at all times. This cuts repair time from eight hours to two. The manual does not discuss inventory management, which matters more than you think.
Where to find help when the manual is not enough
Fadal's technical support is responsive but busy. Have a parameter file backup ready before you call. The manual mentions backup but does not explain that these files can become corrupted if you save them to a USB drive that is not formatted correctly. I use FAT32 formatting and verify checksums after each save. This prevents data loss during system updates. Local training programs exist in most industrial areas. Find a certified Fadal trainer if you can. The manual covers basics, but it does not teach you how to hear that a linear guide is failing before it seizes. I learned this from a trainer who had worked with these machines for twenty years. He could diagnose axis problems by sound alone. This skill does not appear in any manual. Online forums and user groups exist. Search for Vmc 4020 discussions on CNC-related sites. The manual does not cover edge cases like using high-viscosity Wayon oil in winter months. I learned this from an operator who switched to synthetic fluid when temperatures dropped below 50°F. This prevented sludge formation in the lubrication system. The manual does not discuss fluid chemistry, which matters more than you think.
Final thoughts on daily operation
The manual is a starting point. Daily checks matter more than monthly maintenance. I inspect tool holders, clean tapers, and verify axis backlash before each shift. This takes fifteen minutes. It prevents hours of troubleshooting later. The manual does not emphasize this enough. Keep a logbook. Record parameter changes, maintenance actions, and unusual symptoms. The manual suggests documentation but does not explain that these logs become invaluable when diagnosing recurring problems. I have used my logbook to trace a spindle vibration issue back to a single bearing replacement that was done incorrectly. This insight comes from experience, not from reading. These machines are workhorses. They require work. The manual tells you how. It does not tell you why. I have learned the why through trial and error. You can learn it faster if you pay attention to the details the manual leaves out.