The Practical File Guide For Knife Making
Files are where most beginners waste time in knife making. You buy a set, you start grinding with them, and you realize halfway through that the file is glazed over and you've been pushing harder instead of smarter. I learned this the hard way on a W1 spring steel blank that should have taken two hours to shape. It took six. A proper file guide isn't about listing every file type ever manufactured. It's about understanding which file cuts efficiently on which material, when to stop and change strategy, and how to keep a file cutting so you're not fighting it the whole time.
File Guide For Knife Making: What Actually Matters
Knife making files fall into three useful categories: roughing files for removing material fast, second-cut files for refining shape, and smooth or dead-fine files for final surface prep before heat treatment. Most of your work happens in the first two. The third category is for people who sand their blades before tempering, which is fine if you like sanding. The file cut designation matters more than most makers realize. Single-cut files have parallel rows of teeth and produce a finer finish but cut slower. Double-cut files cross-hatch the teeth pattern and remove material aggressively. When you're defining bevels on a thick blank, double-cut is the default. When you're cleaning up those bevels and getting ready for sharpening, single-cut does the job with fewer deep scratches to fight later. File hardness is the next thing people get wrong. A file is made from high-carbon steel and is hardened to around 62-65 HRC. That means it can cut softer steel. If you're working with tool steels in the 55-60 HRC range after pre-hardening, a standard file won't bite properly and you'll just burnish the surface. This is exactly what happened to me with a CPM-3V blank that had been normalized and was still too tough. I was trying to refine the blade profile and the file was skating across the metal like it was coated. The workaround was straightforward: I annealed the blank down to around 200-220 HB, did all the filing and shaping, then re-hardened it for heat treatment. Total extra time was about four hours including cool-down and a furnace cycle. Not ideal, but it saved the piece.
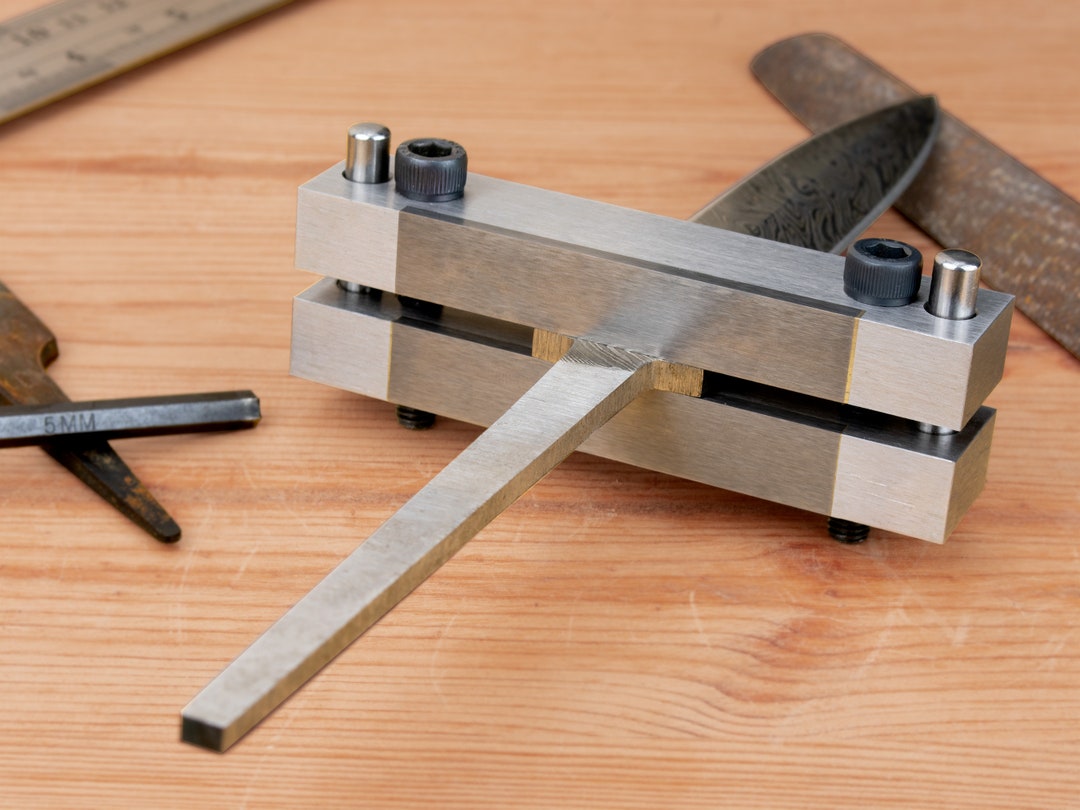
File shape matters too. A flat mill file removes stock on flat surfaces. A half-round is genuinely useful because you get both a flat side for broad work and a curved side for concave grind work or swedge lines. A triangular file handles grooves and corner work. A knife maker's specialized file set often includes a drawfile, which pulls across the edge to create a flat reference surface before sharpening. I keep a drawfile in my kit specifically for this. It's one of those tools that sounds obscure but cuts sharpening setup time down significantly.
Get the Full Details

How to Use Files Without Wasting Hours
The fundamental technique is push strokes, not dragging. You press down on the forward stroke and lift slightly on the return. Dragging a file backward glazes the steel and loads the teeth with swarf almost immediately. You'd be surprised how many people file backward instinctively because it feels like it's doing something. It's not. File dressers or wire brushes are mandatory. A needle file dresser is the cheapest tool in this entire discussion and it extends file life by an order of magnitude. Load a file with steel chips and it cuts nothing. Run it through the dresser, strike it against a hard surface to dislodge the load, and it's cutting again. I dress my files every ten to fifteen minutes of active use on any medium-carbon steel. On harder steels, the interval drops to five minutes. There's a reason you don't file cold-worked or pre-hardened spring steel with anything but a diamond file. Regular files wear down almost as fast as they cut. Diamond-coated files stay aggressive and they cost three to five times more per file. The math works out if you're doing repeated projects on hard stock. If you're making one knife a month from mild steel, regular files are fine.
Progression is where the time savings hide. Going from a coarse 8-10 inch double-cut file directly to a smooth file is a trap. Each file stage should remove roughly the same amount of material that the previous stage left behind. If your coarse file marks are two thousandths deep, your second-cut file needs to eliminate all of that before you move on. Skipping stages means you're polishing away deep scratches later instead of just filing the outline and bevels cleanly the first time around. A typical progression for a kitchen knife blank goes: coarse double-cut for bevel introduction, second-cut for shape refinement, then a single-cut or drawfile for final surface prep. That's it. You don't need twelve files. Avoid filing the same spot repeatedly without changing angle. It creates dips and low spots that are nearly impossible to fix later. Rotate your work angle gradually through each stroke sequence. This applies especially to the edge bevels. File from the spine toward the edge at a consistent angle, move slightly along the blade length, and come back. You'll cover the whole surface evenly without creating valleys in the metal.
When Files Are the Wrong Tool
I need to be blunt about this. Files are slow. If you're trying to shape a thick blade blank from scratch, an angle grinder with a flap disc or a belt sander does in twenty minutes what a file does in two hours. Files exist for refinement, not initial shaping. I use a grinder to get within a thousandth or two of the final profile, then files take over for precision and surface quality. Anyone telling you to file a blank from raw stock is either romanticizing the process or working with something thin enough that filing is actually reasonable. Files also struggle on stainless steels like 440C or S30V in any hardness above 20 HRC. The chromium carbides in these steels abrade regular file teeth rapidly. Diamond files handle them but at a significantly higher cost per cut. If you're working with difficult steels, budget for diamond-coated tools or reconsider your process and do more grinding work upfront. Another limitation nobody mentions: files can't follow curves tighter than their own radius. A flat file will leave flat spots on a curved bevel. A half-round file has a minimum inner radius determined by its curve. If you're defining a complex hollow grind or a fine swedge, files will skip and chatter. That's where rasps and rifflers come in, but they're specialty tools for specific jobs, not general-purpose knife making files.

The File Guide Everyone Should Keep Handy
Keep a simple reference card near your bench. List the file type, cut designation, tooth pitch, and recommended use. Update it as you learn what works for your material mix. I started with a generic chart from a hardware store. After about fifty knives, I replaced it with my own notes showing which files stayed sharp longest on which steels, which dressers worked best, and which file shapes I actually reached for versus which ones just sat in the box. That personal version is far more useful than any printed guide. The core of a functional file kit for knife making is manageable: a 10-inch double-cut mill file, a 10-inch second-cut mill file, a 10-inch single-cut mill file, a half-round second-cut file, a triangular file for detail work, and a drawfile. Add a needle file set for tiny corrections and a diamond file if you work with hardened or difficult steels regularly. That's twelve to fifteen files total. More than that and you're collecting, not building knives.