What Actually Happens During Fire Pump Certification
You show up with your flow test equipment, connect the discharge lines, and run the pump through its approved test sequence. That is the surface-level description. The reality is that most fire pump certifications take longer than expected because technicians underestimate how much time the setup and teardown require, especially when dealing with hydrant connections or testing at the street main. A typical certification visit for a standard diesel-driven fire pump takes about three to four hours from start to finish. Electric motor pumps can go faster if you have good access and a reliable power source, maybe two to three hours. The NFPA 25 testing protocol is methodical and there is no real shortcut through it. The core of the work revolves around proving the pump delivers rated flow at rated pressure. You run tests at zero pressure (churn), twenty-five percent flow, one hundred percent flow, and one hundred fifty percent flow. Each data point matters. The inspector is not looking for perfection on every single point but they are looking for consistent deviation within acceptable tolerance bands. Your pump curves, maintenance logs, and the actual test results all need to align or you will get flagged. One thing most beginners do not pick up from a classroom session is how temperature affects your readings. Water temperature changes the viscosity and that shifts your performance numbers slightly. On a hot summer day when the pump is sitting in direct sunlight, the water in your test header can be ten to fifteen degrees warmer than the suction source. That warmer water moves slightly differently through the impeller and volute. It will throw off your flow calculations if you are not accounting for it. I started carrying a digital thermometer and logging the water temperature at each test point instead of assuming standard conditions. That alone fixed what looked like recurring calibration issues on my older centrifugal pump kits.
Setting Up the Test Loop Correctly
Your test water path needs to be properly sized. Using an undersized discharge hose is one of the most common mistakes I see. If your test header or hose is too small for the flow rate you are trying to achieve, you create artificial pressure that makes the pump look worse than it actually is. For a 500 gpm pump, you generally need at least four inch supply and test lines. Anything smaller and you are measuring your own restrictions instead of the pump performance. The flow meter also needs to be calibrated. I keep a portable calibrated orifice plate and a ultrasonic flow meter as cross-reference tools. When the two readings disagree by more than five percent, something is wrong and I do not sign off until I figure out which instrument is drifting. The pressure gauges on the pump panel are never trusted directly for certification purposes. They are operational gauges, not test gauges. You need a calibrated test gauge installed on the discharge side with a known calibration certificate. Most jurisdictions require the gauge to be calibrated within the last twelve months. I carry two test gauges so one is always available if the primary needs recertification or breaks in the field.
Reading the Pump Curve Like Someone Who Has Done This a Hundred Times
A non-overloading horsepower curve on a centrifugal fire pump is one of those details that catches people off guard. Some pump curves show horsepower rising continuously as flow increases. If you are running at one hundred fifty percent flow and the motor is already near its full load amp rating at rated conditions, you can trip the overload during the higher flow test. This is not a pump defect. It is a design characteristic. I once spent two hours troubleshooting what looked like a failing motor only to realize the curve on the nameplate data was a flat horsepower type and the motor was actually sized correctly for normal operation. The 150 percent flow point just pushed it over the edge. The solution was documenting the curve type, verifying the FLA against the test results, and noting that the tripping was within design parameters rather than a malfunction. Churn pressure is another area where things go sideways. The pump should not exceed its maximum allowable working pressure at churn. If the churn pressure is dangerously high, you have a relief valve issue or the pump curve does not match the installed hardware. I had a situation once where a newly rebuilt pump had churn pressure that exceeded the casing rating by nearly twenty percent. The vendor had installed the wrong impeller diameter. We caught it during the certification test before the system ever saw service. That one test prevented a catastrophic failure downstream.
Get the Full Details

The Documentation That Actually Matters
Your certification report needs to include the pump make, model, serial number, motor specifications, rated flow and pressure, the actual test results at each flow point, the water temperature, the suction and discharge pressures recorded, the flow meter calibration details, and the test gauge calibration certificates. Missing any of those elements will get your report sent back. I keep a standardized checklist printed in my truck that I fill out on site. It takes about five minutes to complete properly and it saves a follow-up visit that would cost me a half day. Sometimes the pump house itself becomes part of the problem. Low suction pressure from a damaged prime, air entrainment in the suction line, or a clogged strainer will make a perfectly good pump fail its certification. I encountered a pump that could not maintain prime during the test because a foot valve was partially closed from sediment buildup in the supply tank. The pump performed within tolerance once we cleaned the strainer and repaired the foot valve. The initial test failure would have looked like a pump problem if I had not checked the suction side first. Always verify the water supply side before blaming the pump.
When Certification Fails and What to Do
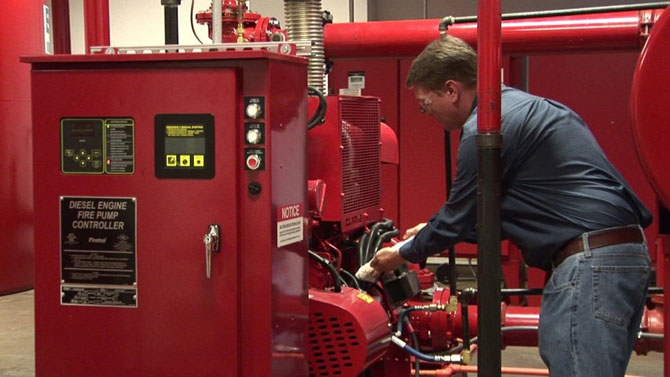
A failed certification is not the end of the process. It is a diagnostic event. Common failure reasons include worn impellers, damaged casing wear rings, incorrect motor speed due to voltage drops, or deteriorated pressure switch settings. The first step is to review the test data and compare it against the original pump curve. If the flow at rated pressure is significantly lower than the curve predicts, wear is the likely cause. If the pump cannot reach rated pressure at all, check the prime and suction conditions first before tearing anything apart. There is also the scenario where the pump passes all the hydraulic tests but the controller fails its inspection. Controller testing includes checking for jockey pump operation, pump start sequencing, alarm signals, and transfer switch functionality. I have seen controllers that passed the initial inspection fail six months later because the battery charger went bad and the standby battery dropped below the minimum voltage threshold. Including controller checks as part of your standard certification workflow prevents surprise failures during the annual reinspection. The entire process is repetitive enough that complacency sets in quickly. I do not skip steps even on pumps I have certified a dozen times before. Every installation has different piping configurations, different water sources, and different environmental conditions. The ones that cause problems are the ones you assume are the same as last year.