Where Six Sigma Actually Came From
The history here is more straightforward than most people expect, but the attribution gets muddled because so many later frameworks borrowed the name without acknowledging the source. The first person to introduce the principle of Six Sigma was Bill Smith, a reliability engineer at Motorola, around 1986. He was working on product quality metrics at the time and noticed a gap in how defect rates were being measured across their manufacturing lines. The idea wasn't born from academic research. It came from practical frustration with inconsistent output. Smith developed the methodology while at Motorola's Defense Electronics Division. He realized that traditional quality control standards—typically settling for three sigma levels—left too much variation unaddressed. Pushing defect rates down to the six sigma threshold meant targeting no more than 3.4 defects per million opportunities. That level of precision was considered unrealistic by most people in manufacturing at the time, but Smith had the statistical backing to show it was achievable with the right process controls.
First Person To Introduce The Principle Of Six Sigma
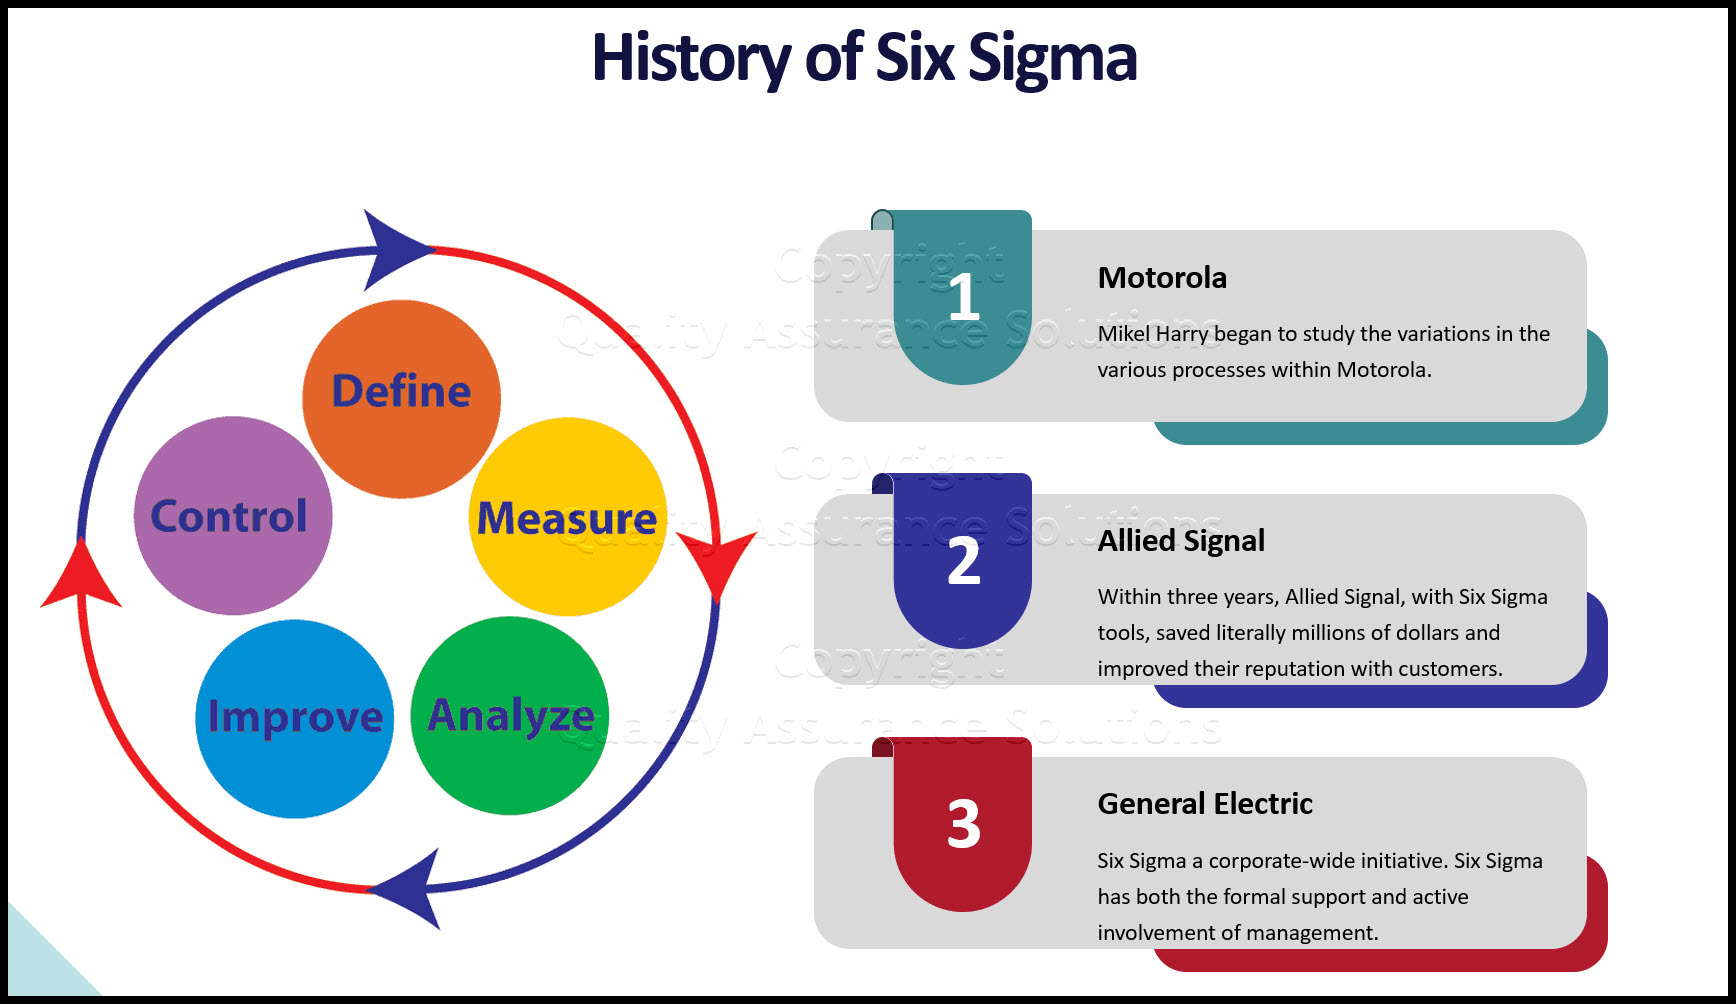
Bill Smith is credited as the first person to introduce the principle of Six Sigma, though his contribution is often overlooked in favor of later popularizers. Motorola formally adopted the framework in 1987, and Smith worked closely with then-CEO Bob Galvin to roll it out company-wide. The program didn't gain mainstream attention until Jack Welch brought it to General Electric in the early 1990s, which is why many people incorrectly credit Welch with originating the concept. Smith died in 1993, long before Six Sigma became the household business term it is today. The core principle Smith introduced is simple in statement but rigorous in execution. It's not just about reducing defects. It's about understanding process variation and controlling it systematically through defined phases. The methodology that grew from his work eventually became known as the DMAIC framework—Define, Measure, Analyze, Improve, Control—which gave practitioners a structured path to follow when tackling quality problems. Smith didn't write a formal academic paper on it. He built it through internal Motorola documentation and training materials that were later published in various forms. I spent several years working with Six Sigma implementations in mid-size manufacturing environments, and one thing I can say with confidence is that the original intent behind Smith's work is almost always diluted by the time it reaches corporate rollout. Organizations tend to treat Six Sigma as a certification program rather than a problem-solving discipline. People get belts—yellow, green, black—without actually applying the statistical methods correctly. I've seen projects flagged as "successful" because the team filled out paperwork properly, not because they reduced variation in any meaningful way.
Here is a practical example of where things go wrong. A factory I consulted for was running a injection molding line that produced consistent dimensional defects. Their green belt team went through the full DMAIC cycle over four months. They defined the problem, collected data, ran hypothesis tests, and implemented a solution. The project was celebrated. But when I looked at the actual process capability indices before and after, Cp and Cpk values had barely moved. The real issue was that the mold temperature controller had a calibration drift that the team never addressed because it fell outside their defined scope. The workaround was to bring in a maintenance technician who had been on the line for twelve years. He identified the drift in an afternoon. The statistical analysis the team had produced was technically correct but practically useless because it was analyzing symptoms rather than root causes. This is a common failure mode that people who only learn Six Sigma from training courses miss entirely. Another counter-intuitive point that beginners rarely grasp: Six Sigma does not work well in environments with low volume and high customisation. The methodology assumes repeatable processes with sufficient data to run statistical analysis. If you are producing one-off custom components where each job has unique parameters, the standard Six Sigma approach breaks down. I encountered this at a job shop that tried to force Six Sigma onto their CNC machining operations. They had maybe five units per product line per month. The data sets were too small to draw statistically significant conclusions. What worked for them instead was a combination of standardised work instructions and visual management—essentially lean manufacturing principles without the heavy statistical layer. Mixing the two approaches gave them better results than six sigma alone. The original framework also had assumptions about organizational culture that Smith took for granted at Motorola. He had executive sponsorship, a willingness to invest in training, and a culture that accepted data-driven decision-making as normal. Most organizations that adopt Six Sigma lack one or more of these elements. Without genuine leadership commitment, the methodology becomes a box-ticking exercise. Without training that goes beyond surface-level certification, practitioners apply tools mechanically without understanding when not to use them. Both failures trace back to the same root cause: treating Six Sigma as a toolkit rather than a management philosophy.
Get the Full Details

If you are looking into this for practical application, start by reading the original Motorola internal documents if you can find them, or works by Mikel Harry who worked alongside Smith and helped formalise the methodology. Harry's writings from the early 1990s give a clearer picture of Smith's original thinking than most modern Six Sigma textbooks do. The modern versions have been stripped of much of the statistical depth and repackaged as generic improvement frameworks. That is not to say they are worthless. They are useful for standardising improvement efforts across large organisations. But they are not the same as what Smith originally designed. The practical takeaway is that the principle itself remains sound. Understanding variation and reducing it systematically is still one of the most effective approaches to quality improvement in manufacturing and many service industries. But the way it is taught and implemented has drifted significantly from Smith's original intent. Being aware of that gap helps you apply the method more honestly rather than going through the motions.