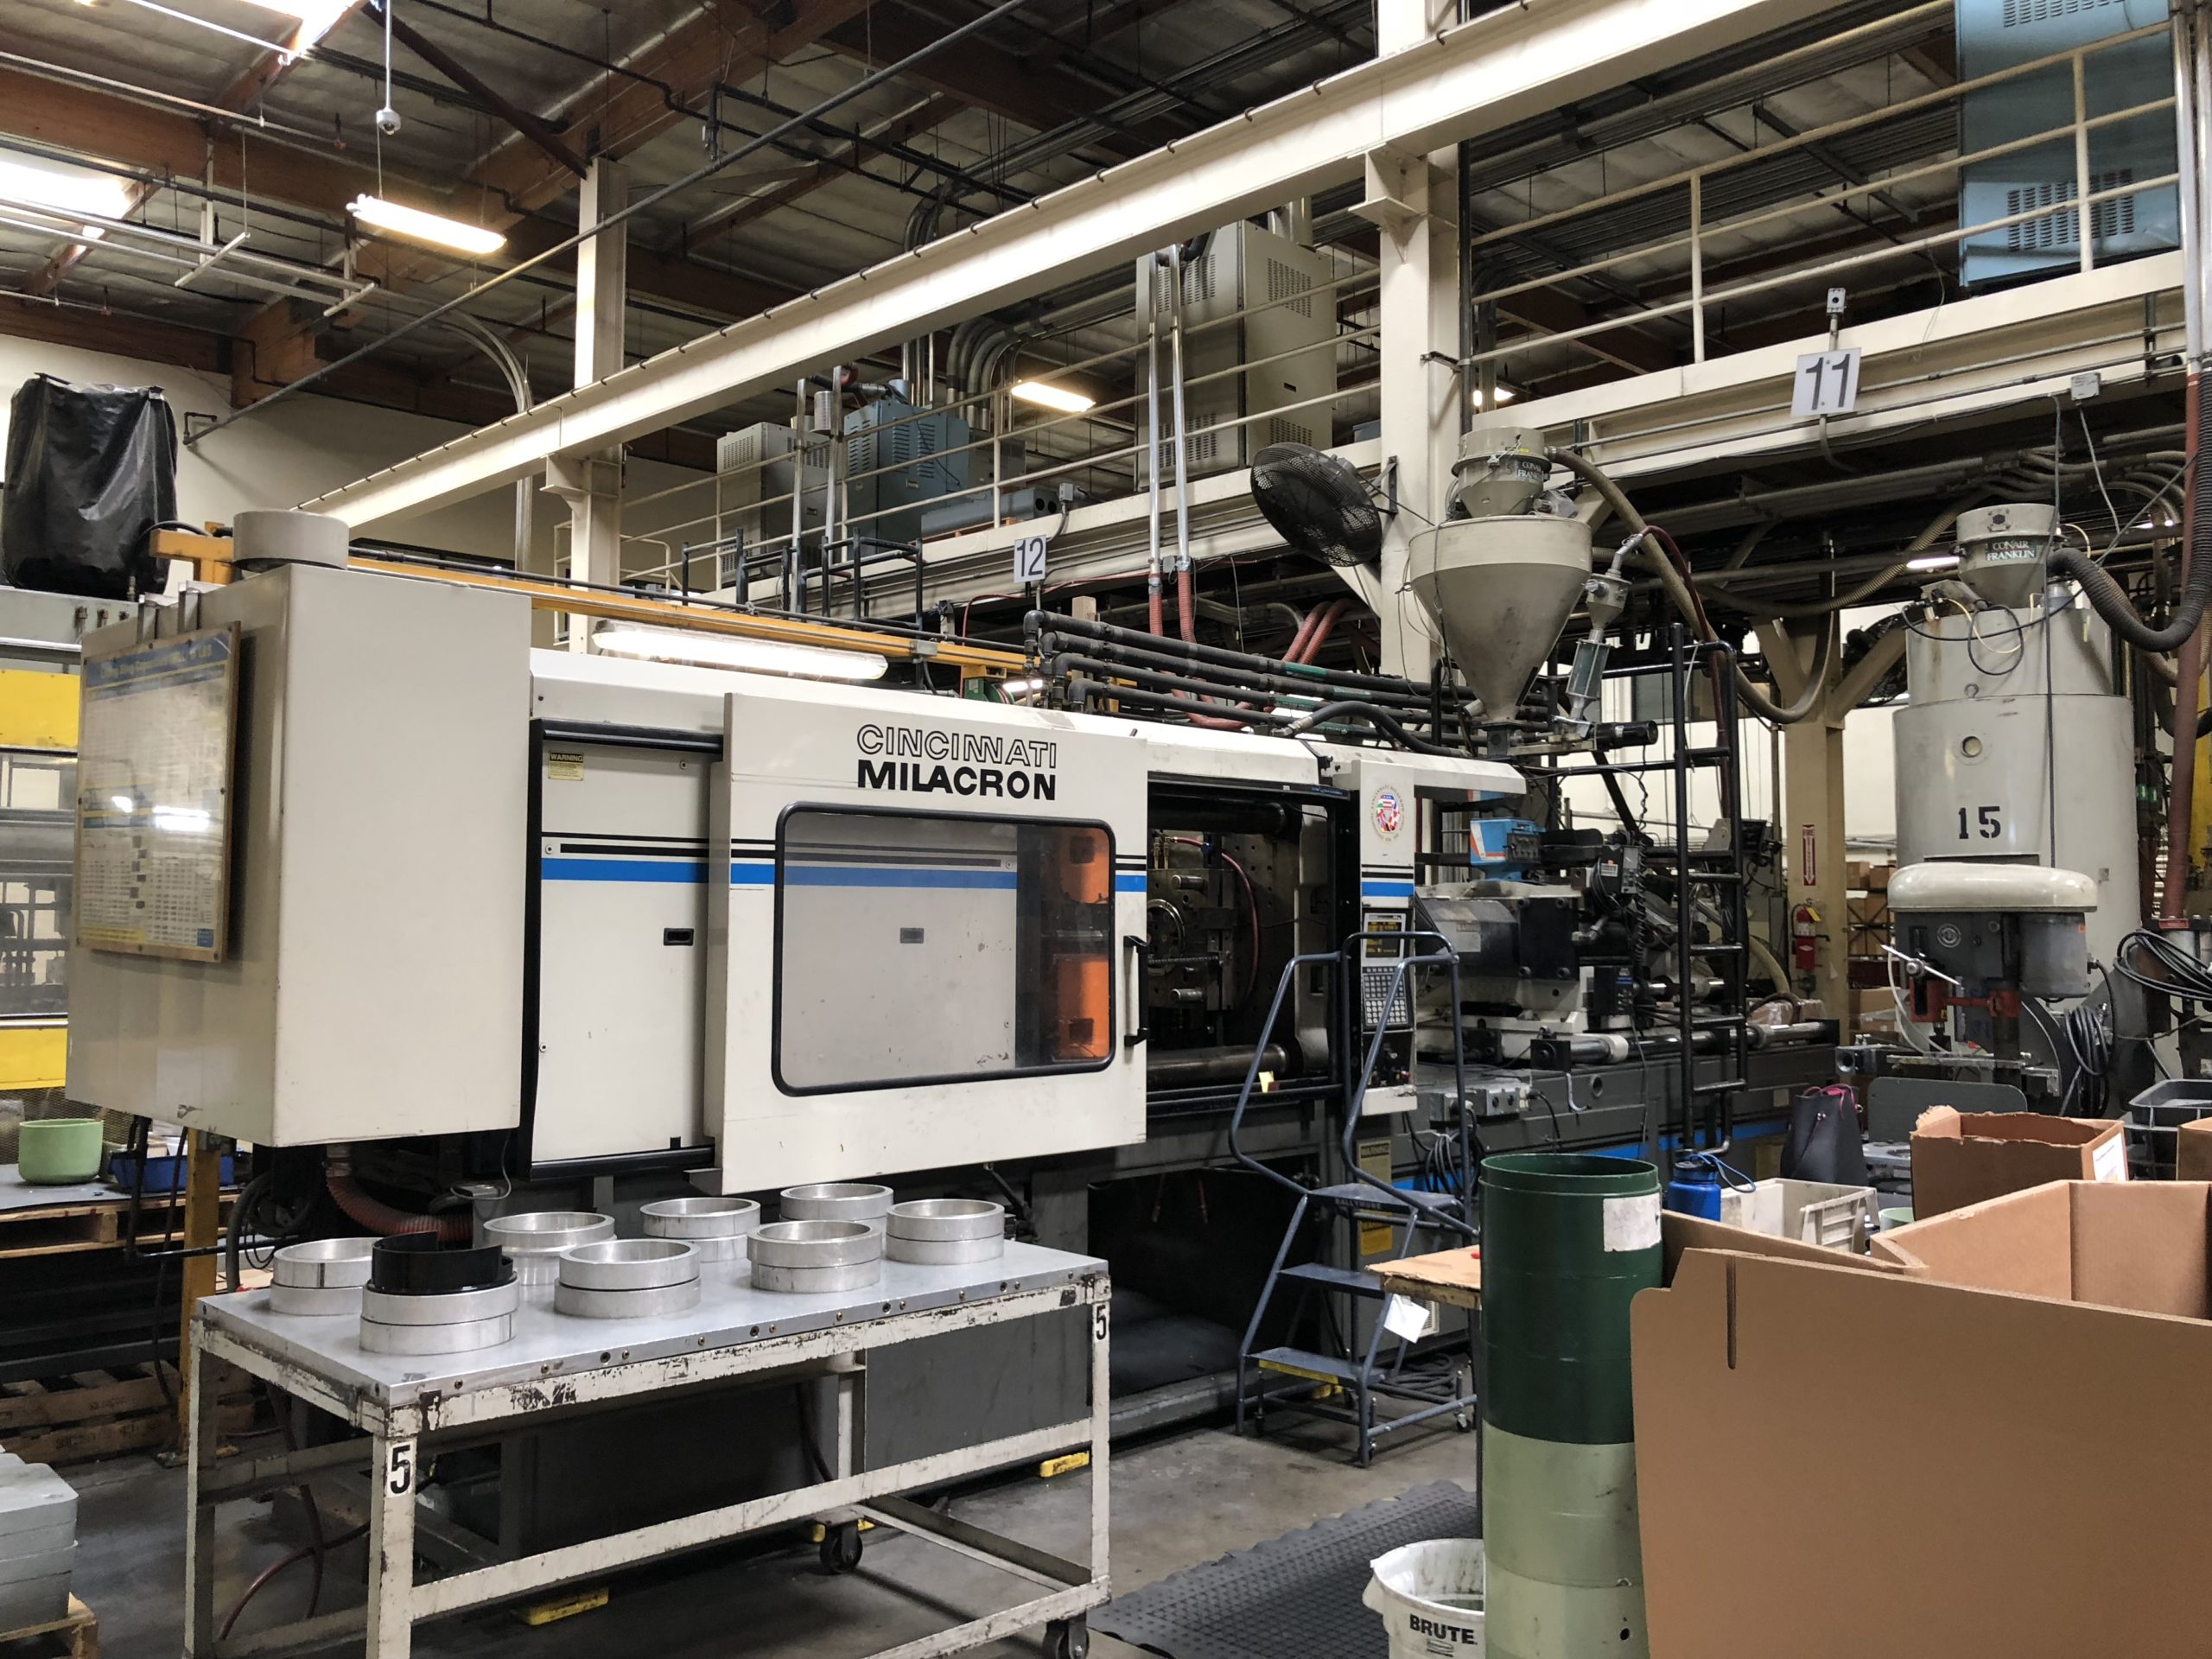
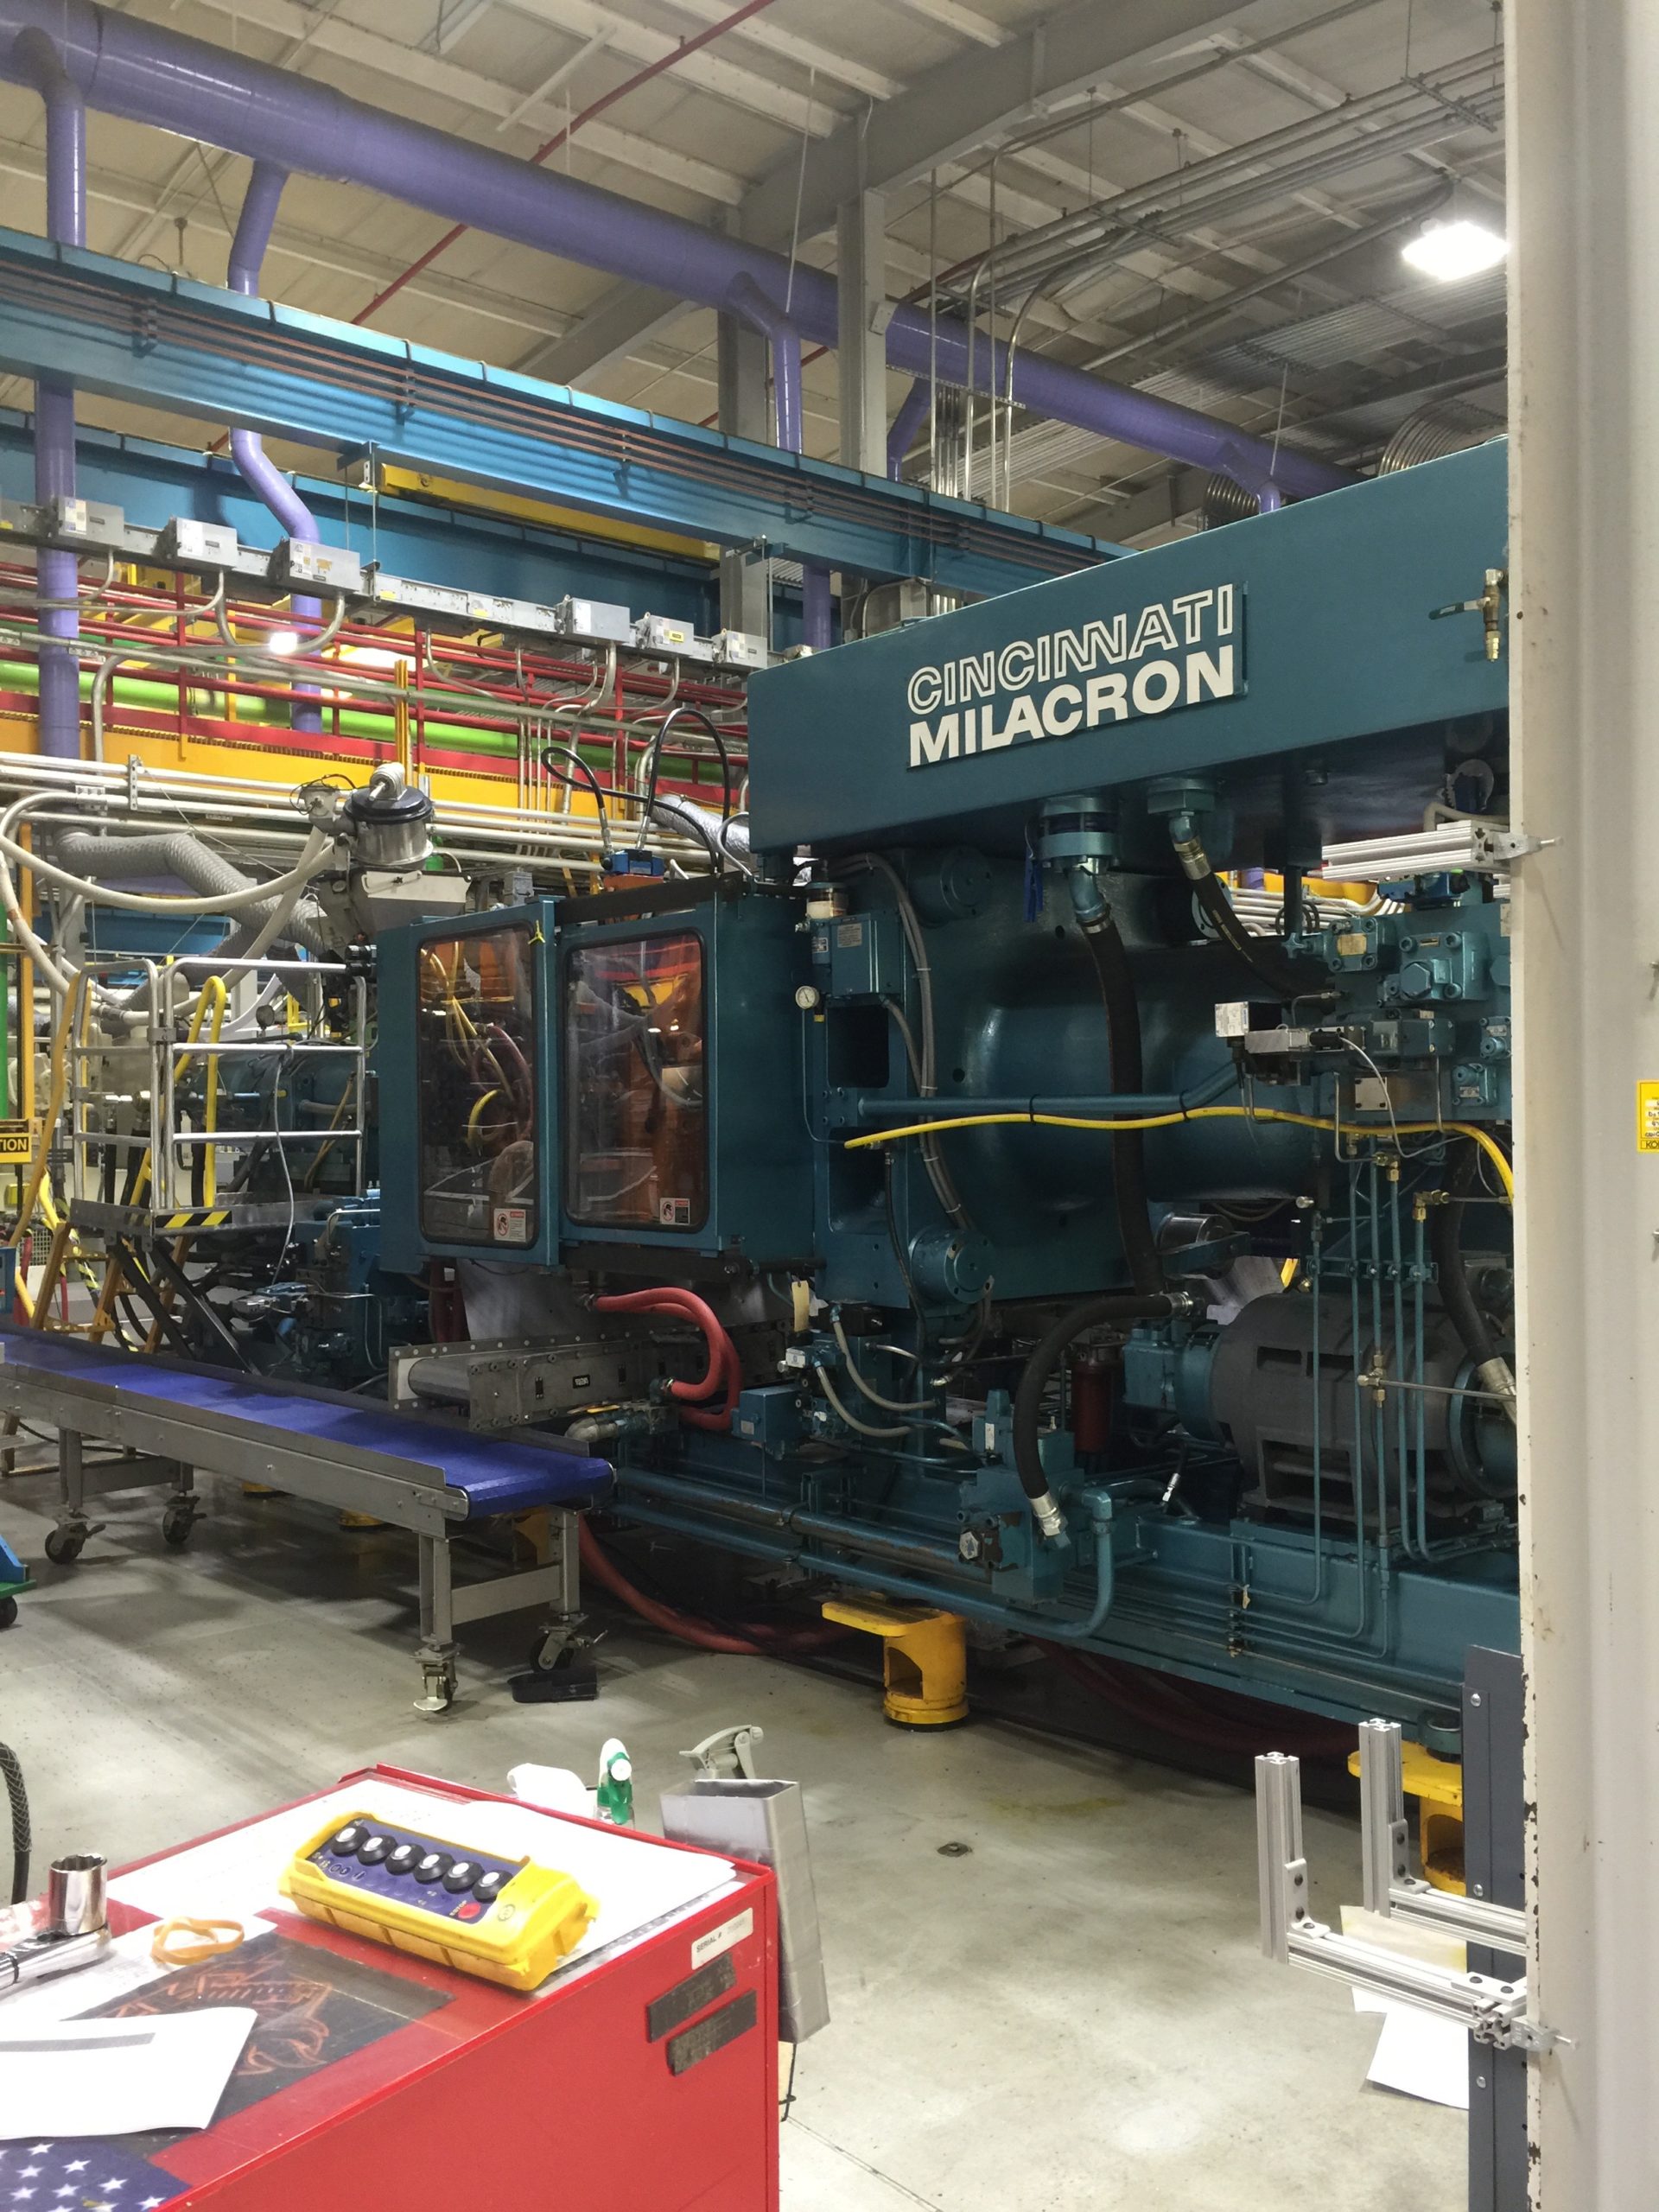
Working With Older Milacron Injection Molding Equipment
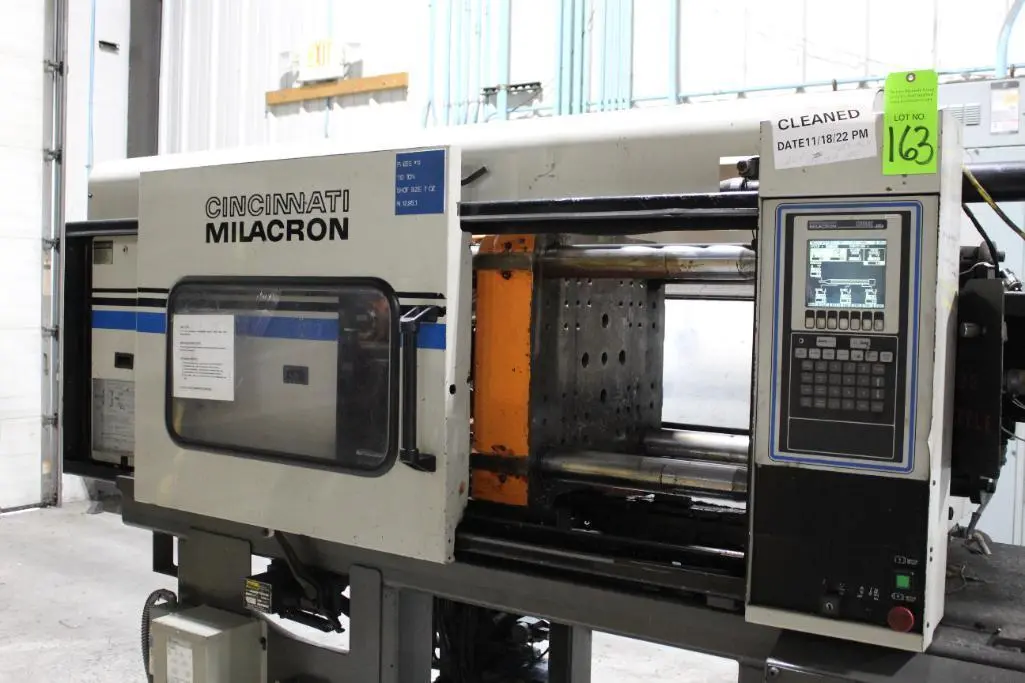
The controls on a Cincinnati Milacron injection molding machine are not complicated, but they are particular. I have spent enough time at these units to know that the difference between a smooth shift change and a two-hour diagnostic session usually comes down to one thing: whether the operator actually reads the fault log before touching anything. Most of the Milacron machines still running in North American job shops are the older hydraulic series — the 150 ton through 500 ton range, controlled by either the legacy 8038 system or the later E-Control interface. The newer electric models exist, but you will rarely see them outside of high-volume medical or packaging lines. The hydraulic units dominate because they are built like tanks and the replacement parts market is still active.
For Cincinnati Milacron Inyection Control Setup and Calibration
Setting up a Milacron machine for a new mold starts with the same sequence every time. You enter the mold data, set the nozzle radius, position the tie bars, and then run the dry cycle. That part is straightforward. What most people get wrong is the shot calibration. The machine needs to learn the actual plasticated volume, not just trust the theoretical calculation based on barrel diameter and screw stroke. I remember pulling a call last spring from a facility in Ohio that could not hold weight tolerance on a simple polypropylene tray. The machine kept cutting short shots and the operator had been chasing the cushion setting for three days. We got there, ran a net shot weight test, and found the actual shot weight varied by 4 percent from cycle to cycle. The problem was not the cushion. It was the check ring on the screw. Wear had created a backward leak path and the plastic was slipping past the ring during the plastication phase. The machine thought it was building a full shot, but it was actually recirculating the same material over and over. Replaced the check ring assembly, recalibrated the shot, and the weight variation dropped to under 0.5 percent. Took about forty minutes total. That kind of issue is invisible on the screen. The fault codes do not flag it. You have to weigh the shots and look at the data.
Common Fault Codes and What They Actually Mean
The Milacron fault system is organized into numbered codes that map to specific subsystems. Hydraulic faults start around the 200 series, electrical faults in the 300s, and mold-related faults in the 400s. A fault code like 215 might tell you "hydraulic pressure deviation," but that is the machine describing the symptom, not the cause. The actual problem could be a worn pump, a stuck relief valve, a clogged filter, or even air entrained in the oil. Walking in and replacing the pump because the code says pressure deviation is how you waste money and delay production. The 306 fault — servo amplifier alarm — shows up more often than it should on older units. Usually it is a dirty encoder feedback cable or a loose connector on the servo drive board. I keep a small bag of contact cleaner and a multi-meter in my tool box for exactly this scenario. Nine times out of ten the fix is cleaning the connector pins and reseating the cable, not replacing the drive module that costs eighteen hundred dollars.
Get the Full Details
Hydraulic System Maintenance That Matters
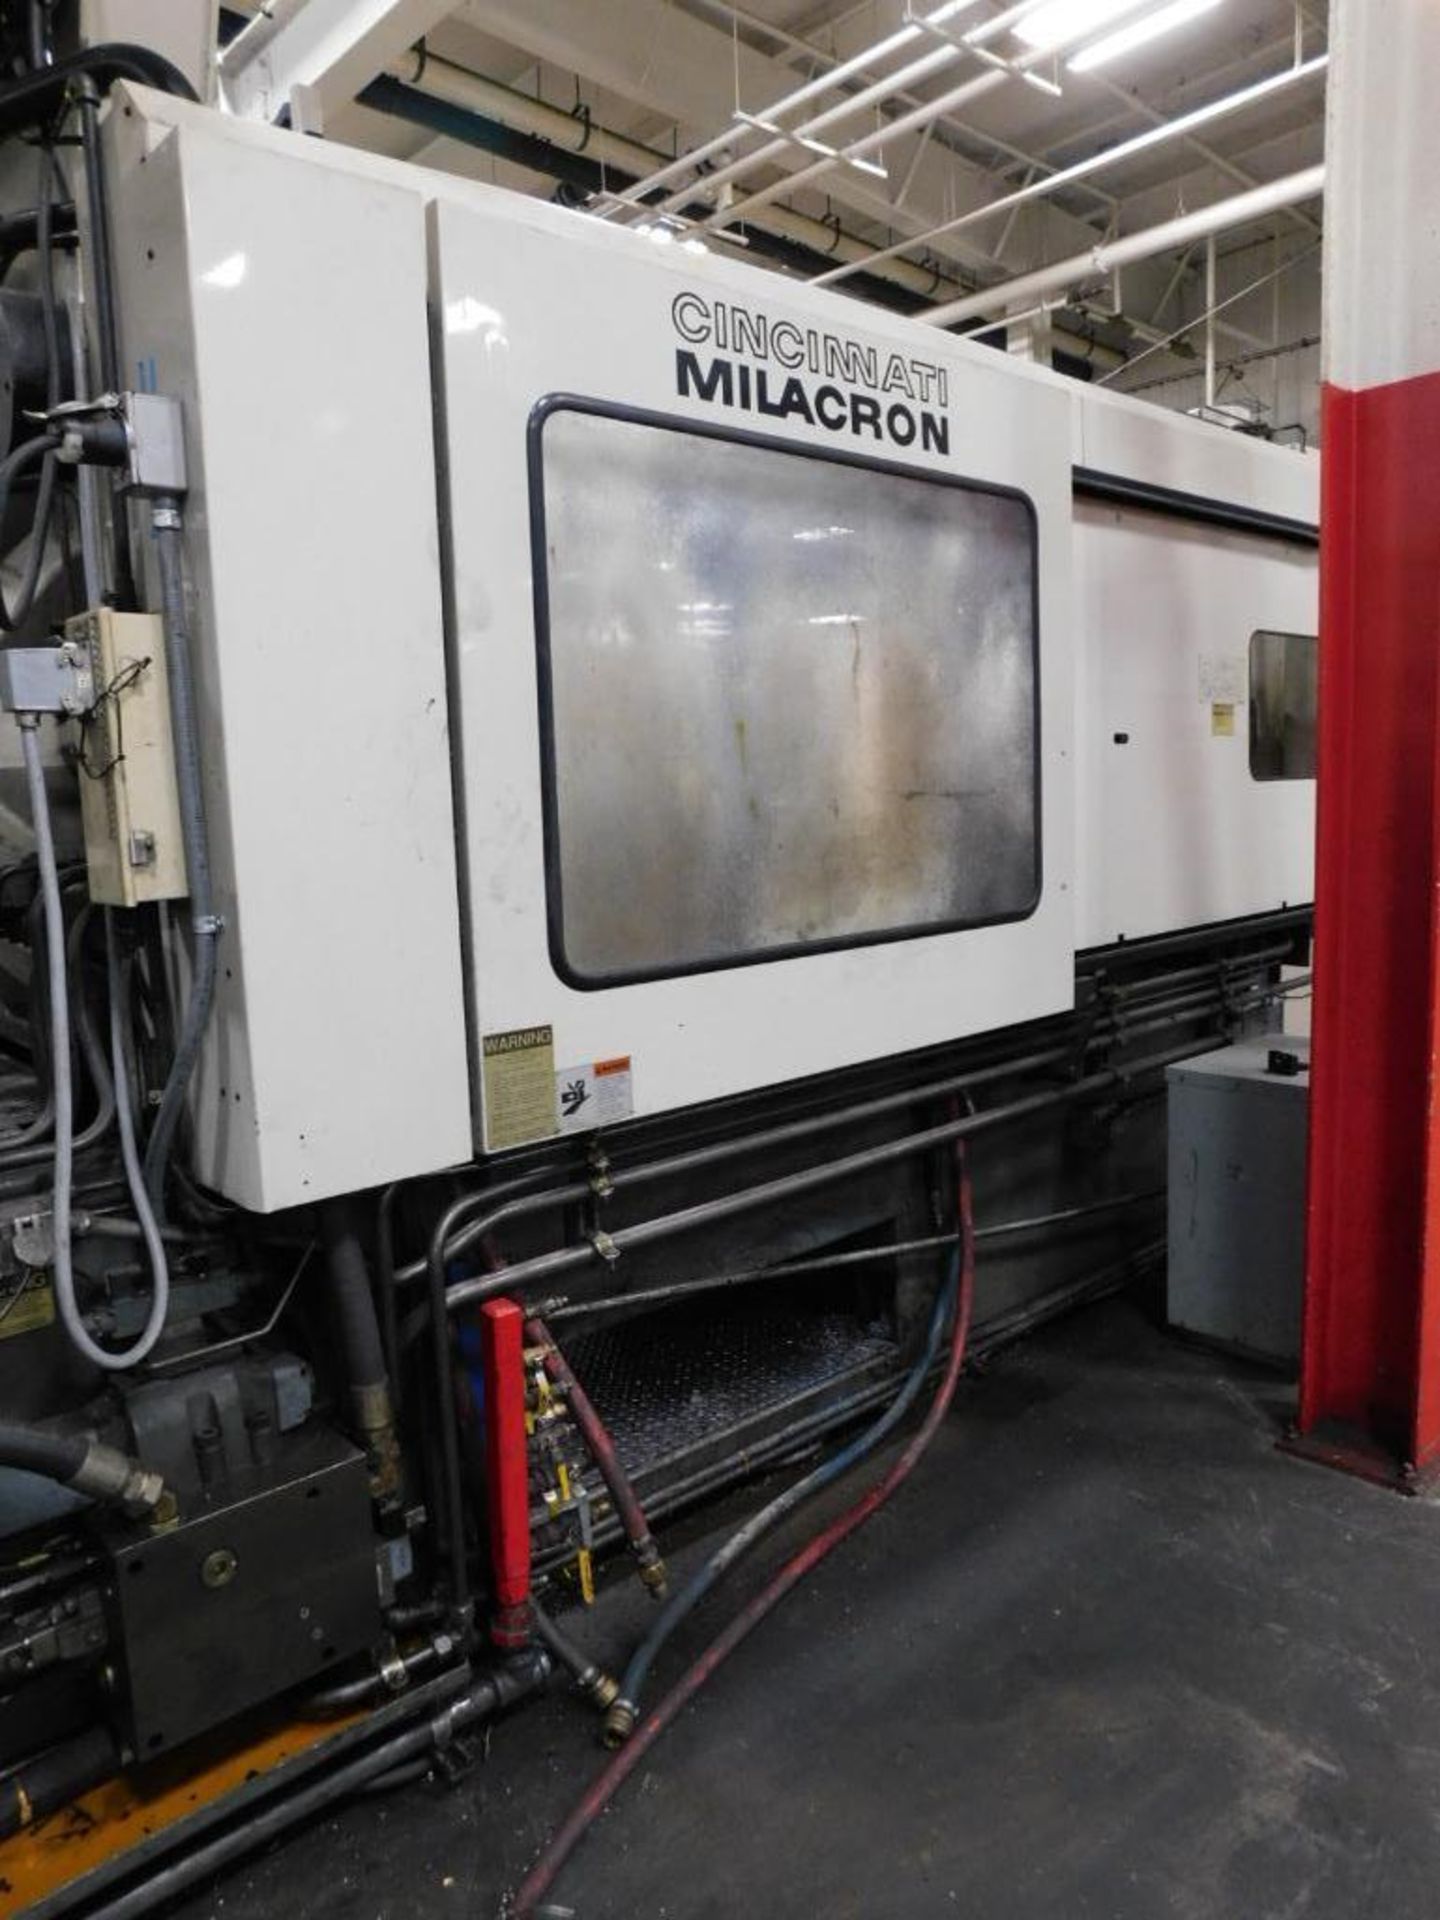
Milacron hydraulic systems run at approximately 1500 to 2000 psi depending on the model. The oil temperature needs to stay between 130 and 150 degrees Fahrenheit for consistent viscosity and proper seal performance. If your chiller is struggling and the oil runs hot, you will see slow cycle times, pressure drift, and accelerated seal degradation. The machine does not warn you about this until something fails. It does not have a gradual degradation alert system. Change the hydraulic fluid every two years on a heavily used machine. Not every three. Two years. The additive package breaks down and the oil loses its anti-wear properties. Use the viscosity grade specified in the manual — usually ISO 46 for most of their hydraulic units. Going heavier because you think it will protect the pump better is a mistake. Thicker oil creates more heat and slower response, which is exactly what you do not want on an injection molding cycle. The filters matter more than people realize. There are usually two filter locations: the suction strainer on the pump inlet and the pressure line filter downstream. The suction strainer catches the large debris. The pressure filter catches the smaller particles. If you skip changing the pressure filter, those particles bypass straight into the servo valves. Servo valves are precision components with clearance gaps measured in microns. One speck of metal and you are looking at a valve that sticks open or closed intermittently. That causes the pressure oscillation faults that keep technicians up at night.
screw and Barrel Considerations
The screw is the heart of the injection unit and the most expensive single component after the mold itself. Milacron screws come in different compression ratios depending on the material they are designed for. A standard general purpose screw has a compression ratio around 2.8 to 3.2 to 1. If you are processing PVC or other thermally sensitive materials, you need a lower compression ratio screw, typically around 2.0 to 2.5 to 1, to reduce shear heat. Running a general purpose screw on PVC will degrade the material and you will see black specks and loss of mechanical properties. The machine does not care which screw you have installed. It will run fine and produce garbage parts. Barrel heating zones are controlled by thermocouples and ceramic heater bands. Over time the heater bands degrade and draw more amperage. A band that should be drawing 4 amps at full power might be drawing 7 amps after five years and still maintaining temperature. The machine does not monitor amperage draw on individual zones. You have to do it yourself with a clamp meter during preventive maintenance. A zone pulling significantly more current than the others is about to fail and will cause temperature instability during the cycle. Replace it before it drops out mid-shift.
Electrical System Quirks
The older Milacron controllers use relay logic boards alongside the PLC. Those relays are mechanical devices with finite lifespans. A relay that clicks every time the mold closes and opens will last maybe five to seven years under heavy production use. When a relay starts failing, it does not always go completely open or closed. Sometimes it chatters. You get intermittent faults that appear and disappear. The machine runs fine for a day and then throws a random fault that you cannot reproduce. That is almost always a relay or a loose terminal on the power distribution board. Check the terminal torques during your annual maintenance. Vibration loosens connections over time. A loose neutral on the control transformer can cause all sorts of weird behavior including random controller resets and display glitches. I have seen techs replace entire control panels only to find the problem was a half-turn loose screw on the terminal block.
Mold Protection Setup
The low-pressure mold protection setting is one of those things that every operator knows about and nobody sets correctly. The function is simple: the platen moves at reduced pressure and speed during the initial mold closing phase. If the mold is not perfectly clean or a insert is left inside, the machine stops before damaging the mold. The problem is that if you set the protection pressure too low, the machine will abort the cycle on every normal close because the air in the parting line creates resistance. If you set it too high, it provides no protection at all. The correct approach is to set the low-pressure transition point at about 80 percent of the full closing distance and the protection pressure at roughly 5 to 10 percent of the normal closing pressure. Test it by placing a piece of tissue paper or safety wire across the parting line and running a cycle. The machine should stop and signal a fault when contact is made. Adjust from there. This takes about three minutes and prevents ten thousand dollars in mold repairs.
Material-specific Notes
Cincinnati Milacron machines handle a wide range of materials without special modification. The real limitations come from the condition of the equipment, not the material itself. However, abrasive filled materials like glass-filled nylons or mineral-loaded polypropylenes will wear the screw and barrel faster. If you run these materials full-time, plan on inspecting the barrel bore and screw flight roots every six months for wear patterns. A mirror finish inside the barrel that has become dull or shows longitudinal scoring is a sign of abrasive wear. At that point you are losing injection pressure consistency and the machine will struggle to maintain shot-to-shot repeatability. Corrosive materials like PVC and some flame retardant blends require more frequent cleaning and inspection of the nozzle and check ring assembly. Residual material left in the barrel after shutdown can carbonize and cause problems the next time you start up. Always purge with a compatible cleaning compound before shutting down if you have been running PVC or similar materials.
When to Call a Professional
Some issues on these machines are straightforward for someone who knows the equipment. Others require specialized diagnostic tools and knowledge of the control architecture. If you are dealing with intermittent electrical faults that you cannot trace, servo drive tuning problems, or anything involving the mold temperature controller integration, it is usually faster and cheaper to bring in someone who works on Milacron systems regularly. The trial and error approach on these machines costs more in lost production time than professional service calls. The controls have evolved since Milacron was independent. Emerson, who acquired the division, has pushed software updates and hardware replacements for legacy systems. Most of the machines still in operation can be maintained and repaired without major upgrades. The key is understanding how the system works and catching problems before they become production stoppages.