Getting Your Flow Rate Numbers Right
Most people I see online mixing up the simple stuff with the complex stuff when it comes to rate of flow calculations. They plug numbers into a formula and get a result that looks reasonable on paper but falls apart the moment they try to apply it to an actual system. I'm going to walk through what you actually need, where things go wrong, and what I've learned dealing with this over the years.Formula For Rate Of Flow
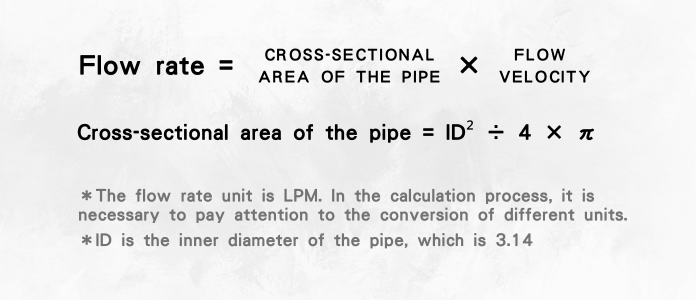
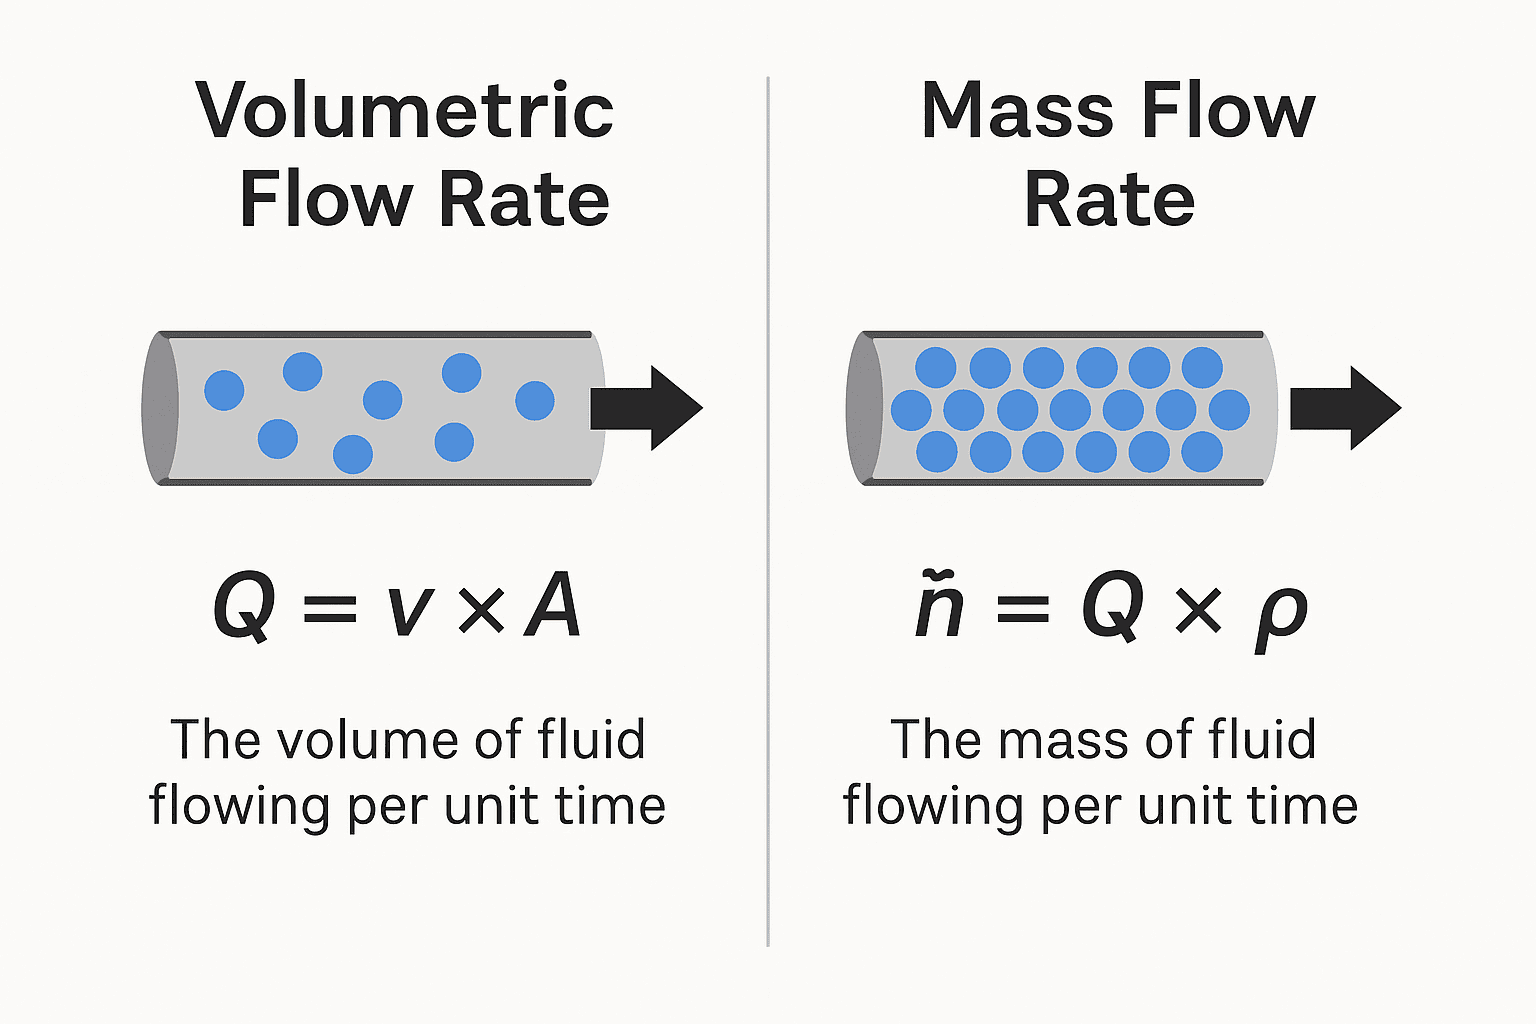
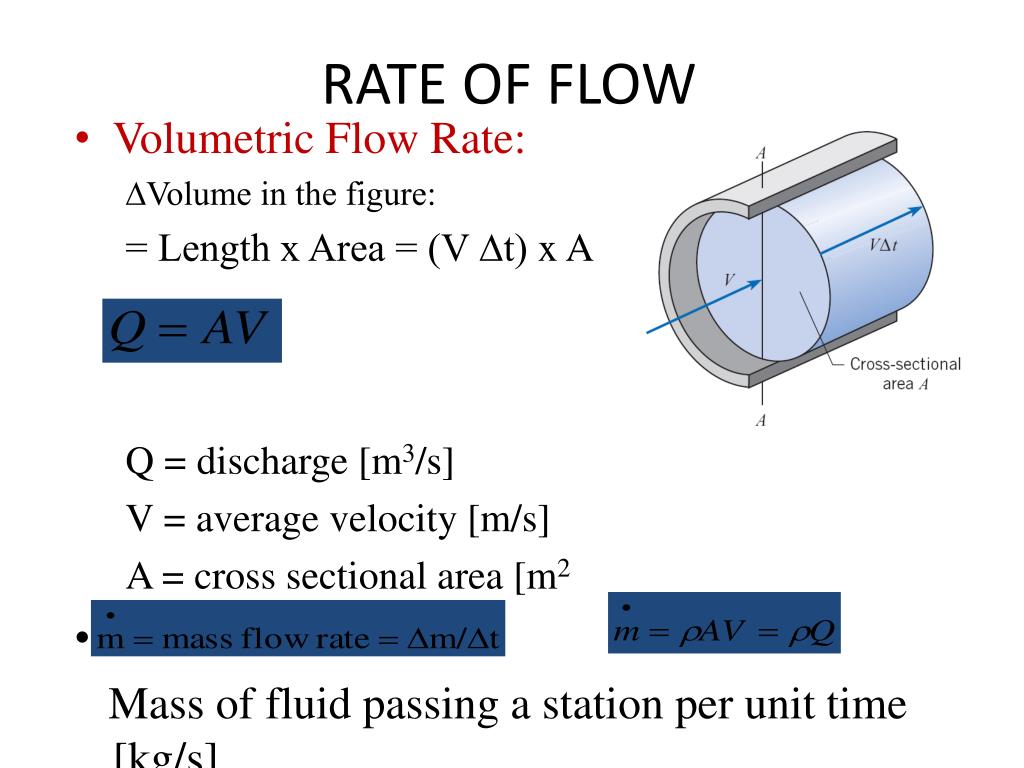
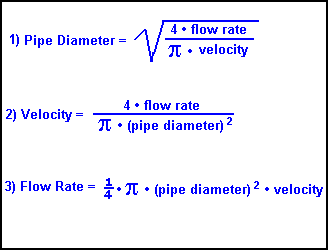
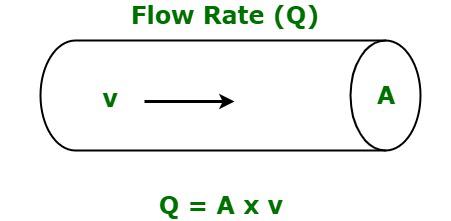
The base equation is Q = A × v, where Q is the volumetric flow rate, A is the cross-sectional area of the pipe or channel, and v is the average fluid velocity through that area. That's it. It's not exciting, but it's also the foundation everything else builds on. If you're working with mass flow rate instead of volumetric, you multiply by density: = × A × v. Units matter enormously here. I've seen people calculate flow rates in cubic meters per second and then immediately convert to gallons per minute without checking their intermediate steps, which introduces rounding errors that compound when the formula gets fed into a larger model.The formula for rate of flow assumes the velocity profile is uniform across the cross-section, which it never actually is in real piping systems. What you measure with most instruments is a point velocity, usually at or near the centerline where the flow is fastest. You then apply a correction factor or assume a ratio based on the flow regime. For fully developed laminar flow in a circular pipe, the average velocity is exactly half the centerline velocity. For turbulent flow, the relationship gets messier and depends on the Reynolds number and pipe roughness. Here's the practical part. If you're using an ultrasonic clamp-on meter, you're measuring velocity at a specific point or integrating across multiple paths depending on the device class. A single-path meter in a 4-inch pipe might give you a reading that's off by 10 to 15 percent if the flow profile isn't fully developed, meaning you need at least ten pipe diameters of straight run upstream and five downstream. If you don't have that, your number is basically a guess with fancy packaging. I dealt with this on a project last year where a client was getting wildly inconsistent flow readings on a chemical transfer line. Turns out the upstream elbow was only three diameters away from the sensor. Once we repositioned the meter and added a flow conditioner, the readings stabilized within about 2 percent. Took us two weeks and a lot of troubleshooting to figure out what was actually wrong. For open channel flow, the formula changes because the cross-sectional area depends on the fluid depth, which is a variable you have to measure separately. Manning's equation is the standard approach there, and it introduces a roughness coefficient that varies enormously depending on whether your channel is concrete, dirt, grass-lined, or something more exotic. Pick the wrong Manning's n value and your calculated flow rate can be off by 30 to 50 percent. Concrete channels typically sit around 0.012 to 0.015, while natural streams with weeds and debris can run 0.04 or higher.
When the Simple Formula Breaks Down
Compressible fluids are the first place where Q = A × v stops being useful on its own. Gases change density with pressure and temperature, so the volumetric flow rate at one point in a system is not the same as at another point even though the mass flow rate stays constant. If you're sizing gas lines or calculating throughput through a restriction, you need to account for the compressibility factor, usually denoted as Z, and the pressure-temperature conditions at your measurement point. I've watched engineers use liquid flow formulas for steam systems and wonder why their numbers didn't match the flow meters. The error margins were enormous, sometimes factor of three or four.Venturi meters and orifice plates are common flow measuring devices that rely on differential pressure. The formula connects the pressure drop across the restriction to the flow rate, and it includes a discharge coefficient that accounts for energy losses and the actual velocity profile. That discharge coefficient isn't a fixed constant. It varies with Reynolds number, especially at low flow rates where the flow regime changes. Orifice plate manufacturers provide charts and tables for this, but if you're eyeballing a generic formula from a textbook, you're introducing uncertainty into your measurement. Another thing people miss is that the formula for rate of flow gives you the volumetric rate at the conditions where velocity and area are measured. If you need the flow rate at standard or base conditions, like standard cubic feet per minute or normal cubic meters per hour, you have to apply a pressure and temperature correction. That correction uses the ideal gas law modified with a compressibility factor for real gases. At low pressures the difference between real and ideal behavior is negligible, but at anything above 10 bar or so, ignoring compressibility starts to matter. We had a natural gas custody transfer application where the discrepancy between real and ideal gas calculations accounted for a measurable financial difference at the end of the month. The compressibility factor saved us from shipping free product. If you need a downloadable reference, most engineering handbooks like the Crane Technical Paper 410 have the standard formulas compiled with the correction factors built in. The NIST Engineering Handbook is also freely available online and covers the fundamentals without the commercial bias. I keep a copy of the Crane handbook on my desk because it's faster to reference than digging through papers during a problem. The formulas themselves are well established and haven't changed much, but the surrounding guidance on when to apply them and what the pitfalls are is worth more than the equations alone.