Stress and Strain: The Basics You Actually Need
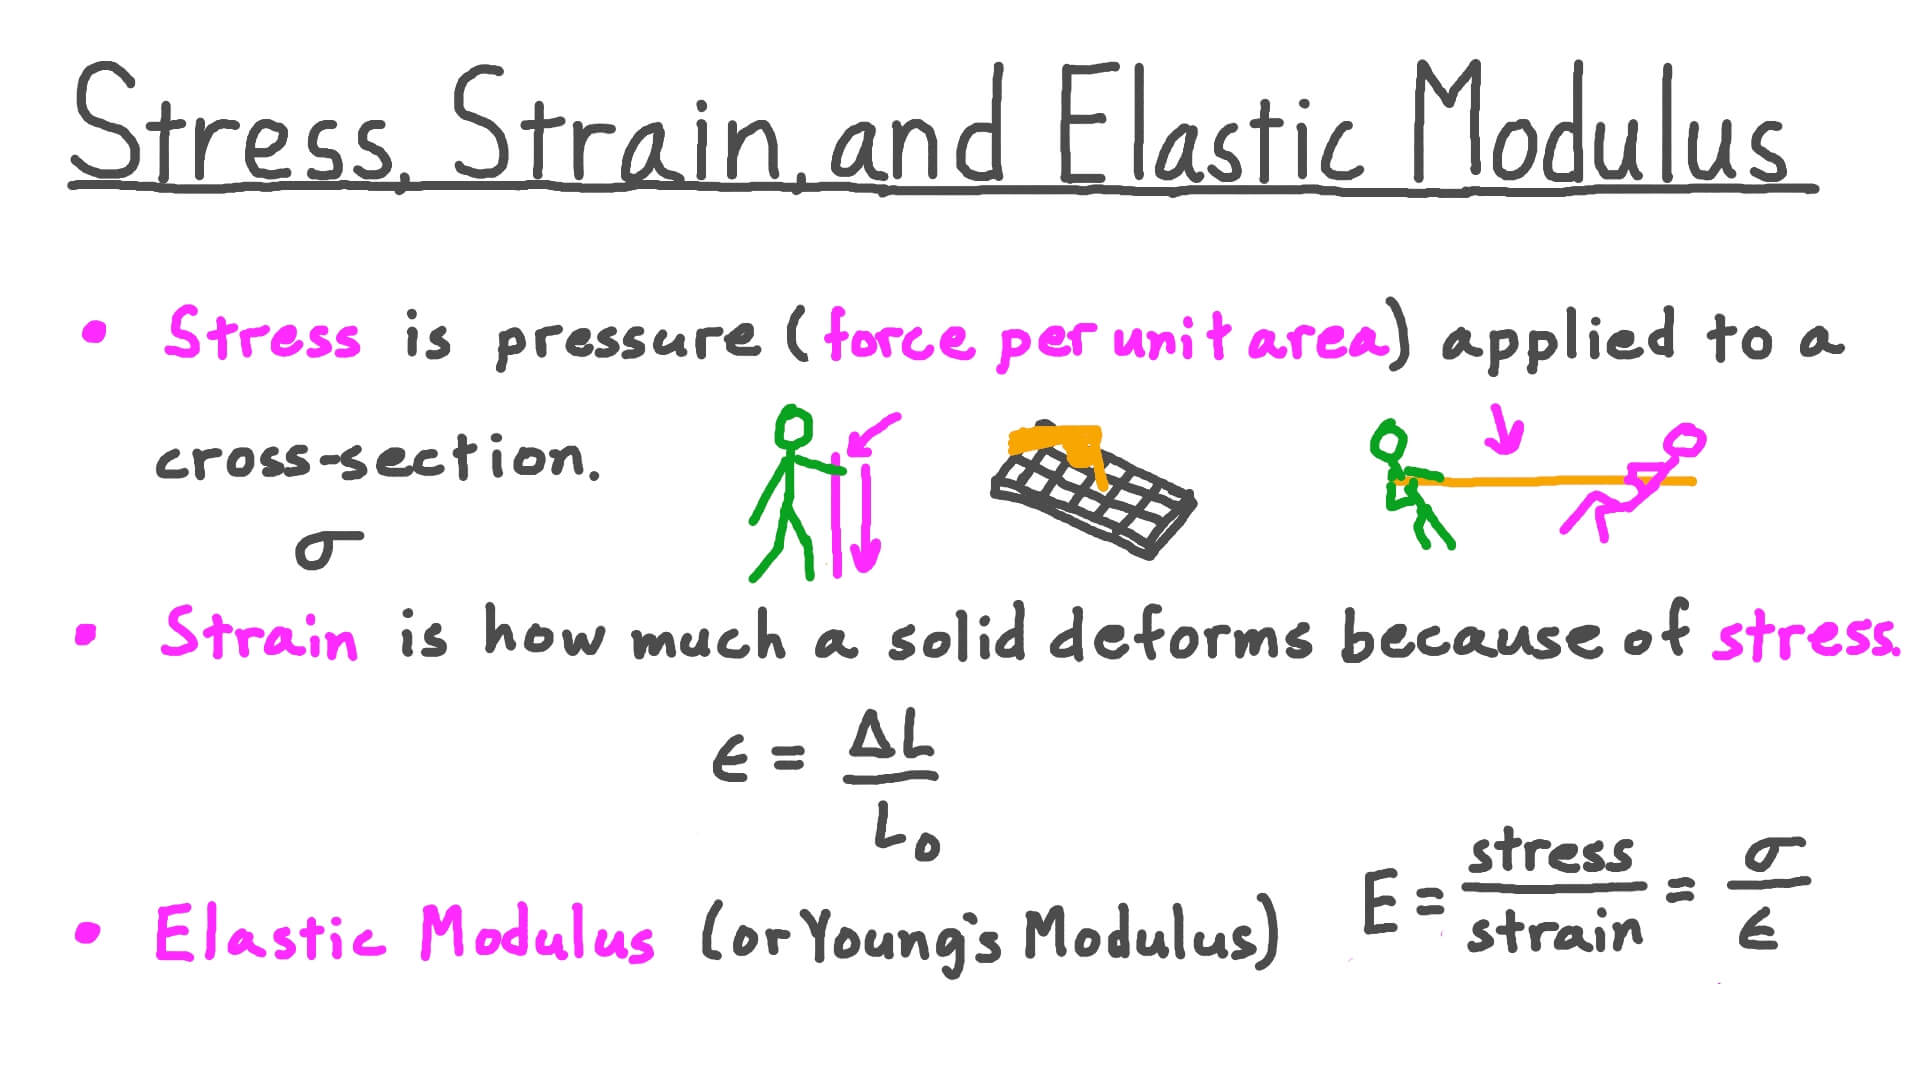
Stress is force per unit area. Strain is deformation relative to original length. That is it. Everything else comes from those two definitions. The
Formula For Stress And Strain
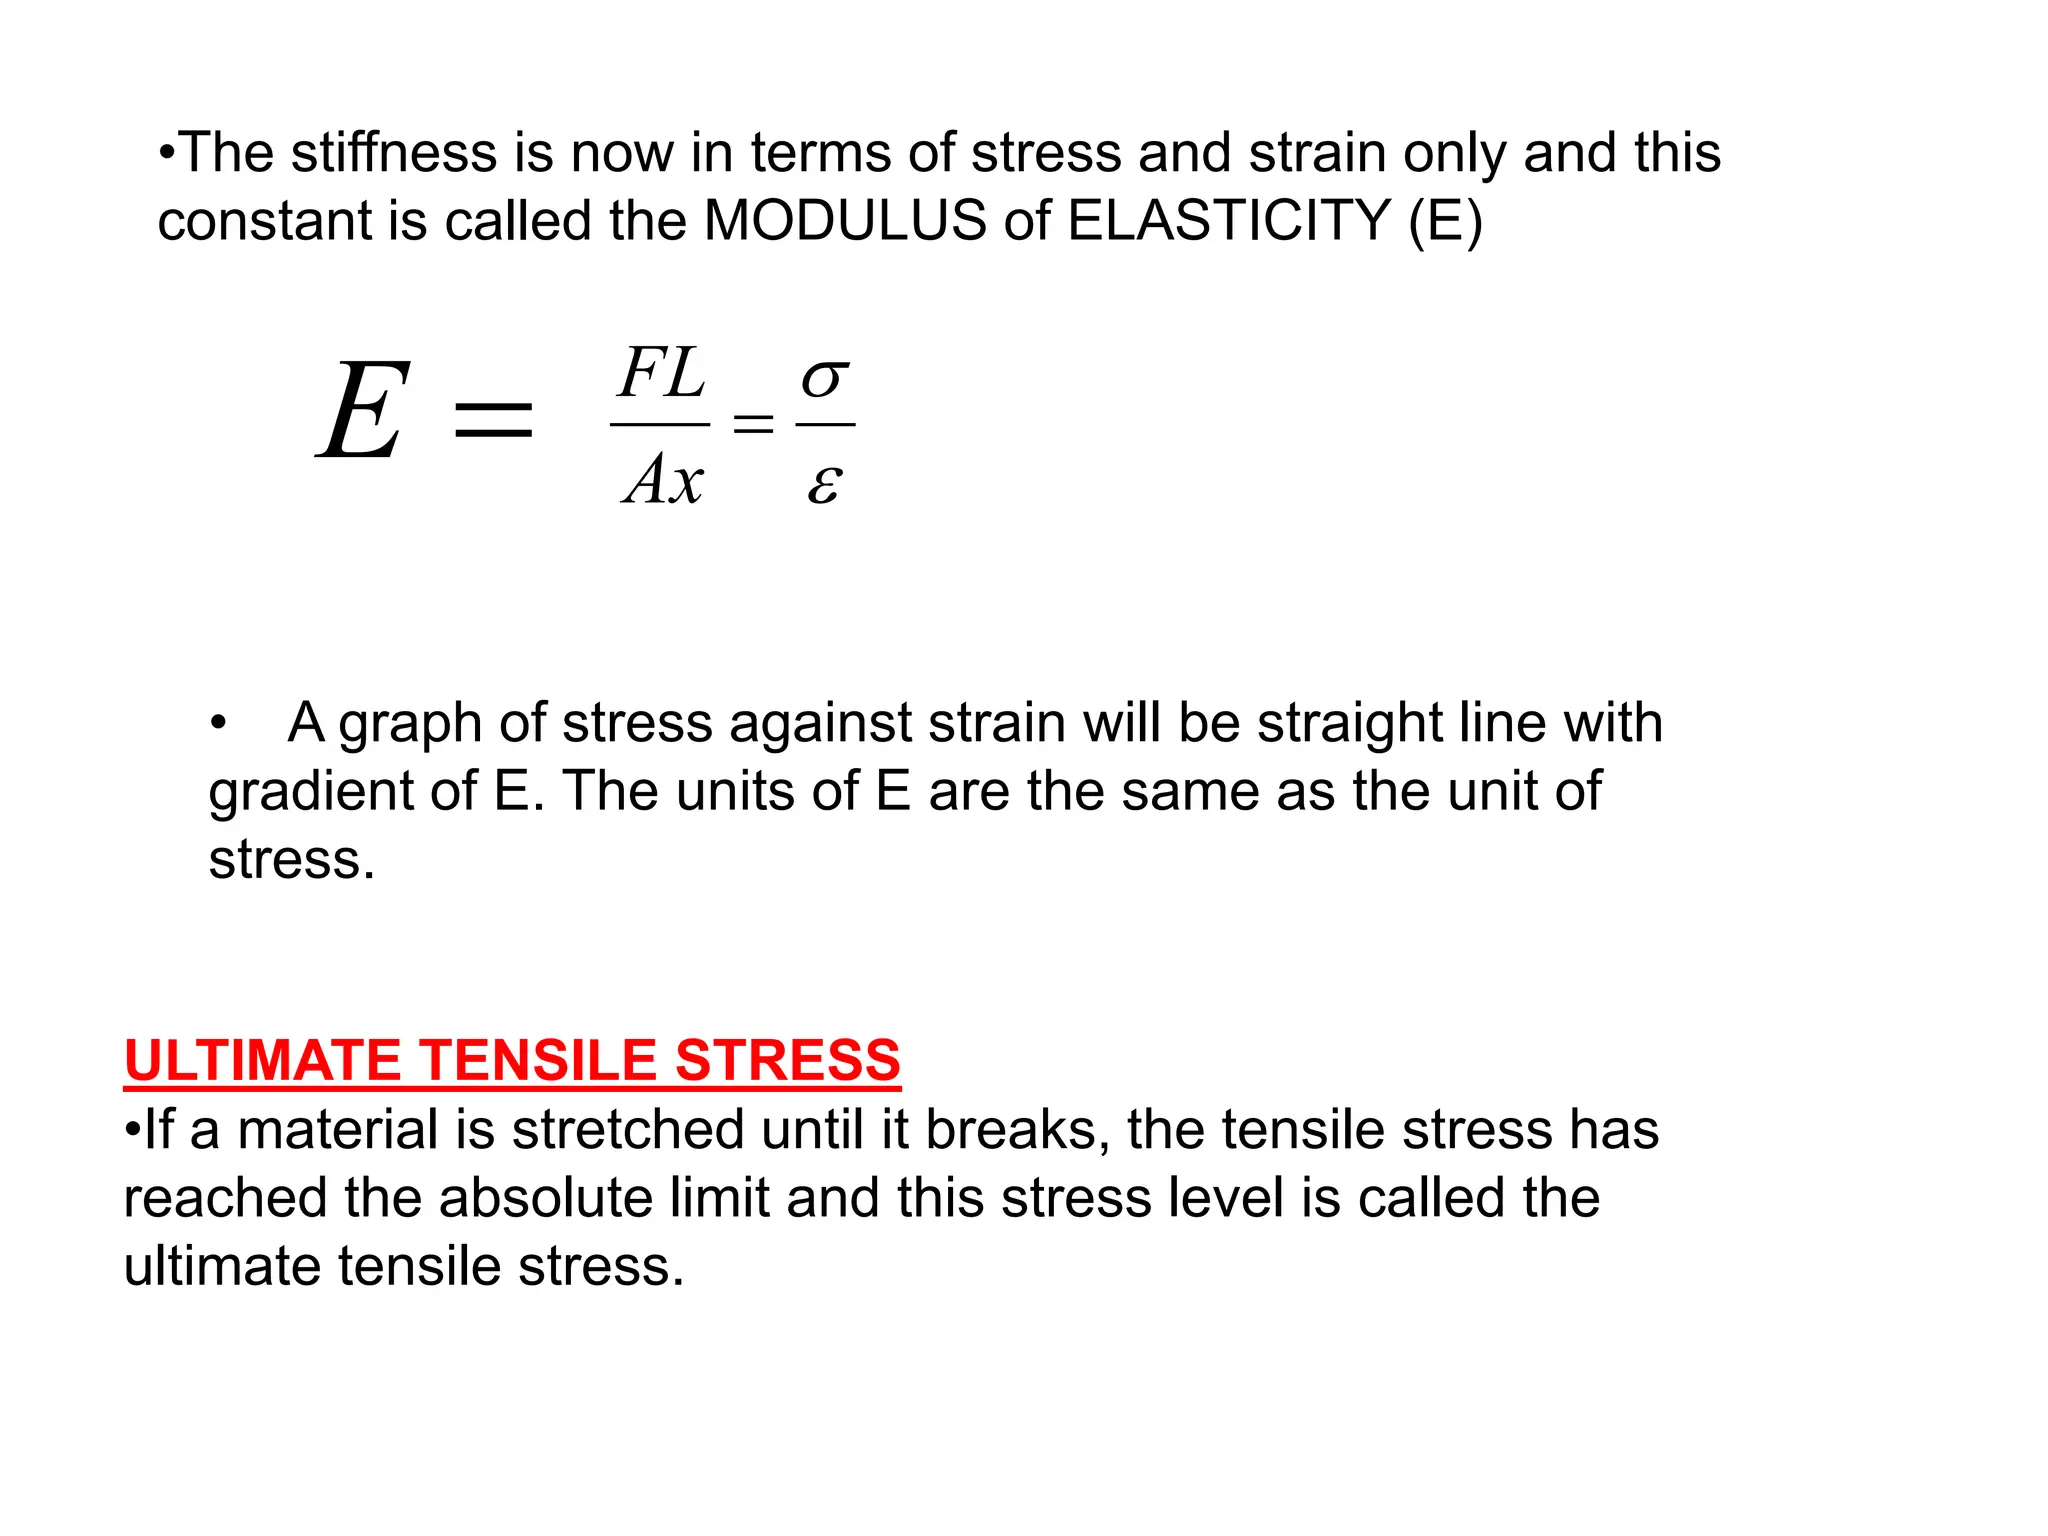
comes in two parts. Engineering stress equals applied load divided by original cross-sectional area. Sigma equals F over A naught. Engineering strain equals change in length divided by original length. Epsilon equals delta L over L naught. True stress and true strain are different because they account for the specimen shrinking as it stretches. I will get to that.How The Test Actually Works
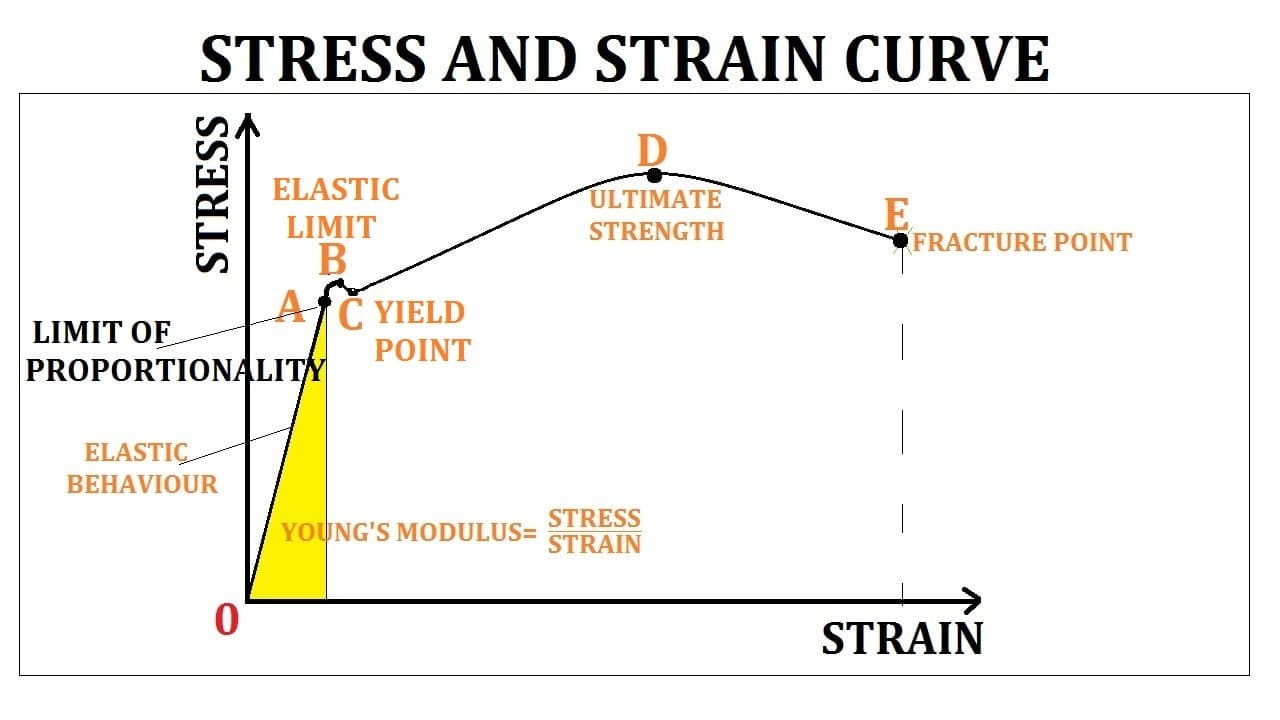
You put a specimen in a tensile machine. The grips hold it. The crosshead moves at a constant rate. The load cell records force. The extensometer records displacement. The machine spits out a curve. Your job is to read that curve and not fool yourself. The standard curve has an elastic region, a yield point, a plastic region, necking, and fracture. Young's modulus is the slope of the linear elastic portion. Yield strength is where plastic deformation begins. Ultimate tensile strength is the peak stress on the curve. Elongation at break is how much it stretched before it failed.
Where People Mess It Up
The most common error is using engineering stress and strain past the necking point. After necking starts, the cross-section is no longer uniform. The original area formula becomes meaningless. You get lower apparent stress values that do not reflect what the material is actually doing. If you need post-necking data, convert to true stress and true strain. True stress equals force divided by instantaneous area. True strain is the integral of dL over L, which simplifies to the natural log of current length divided by original length. The conversion is straightforward for the uniform deformation region before necking. After necking begins, the math gets messy because the strain is no longer uniform along the gauge length. You need digital image correlation or similar techniques to track local deformation accurately.
Get the Full Details
A Real Problem I Faced
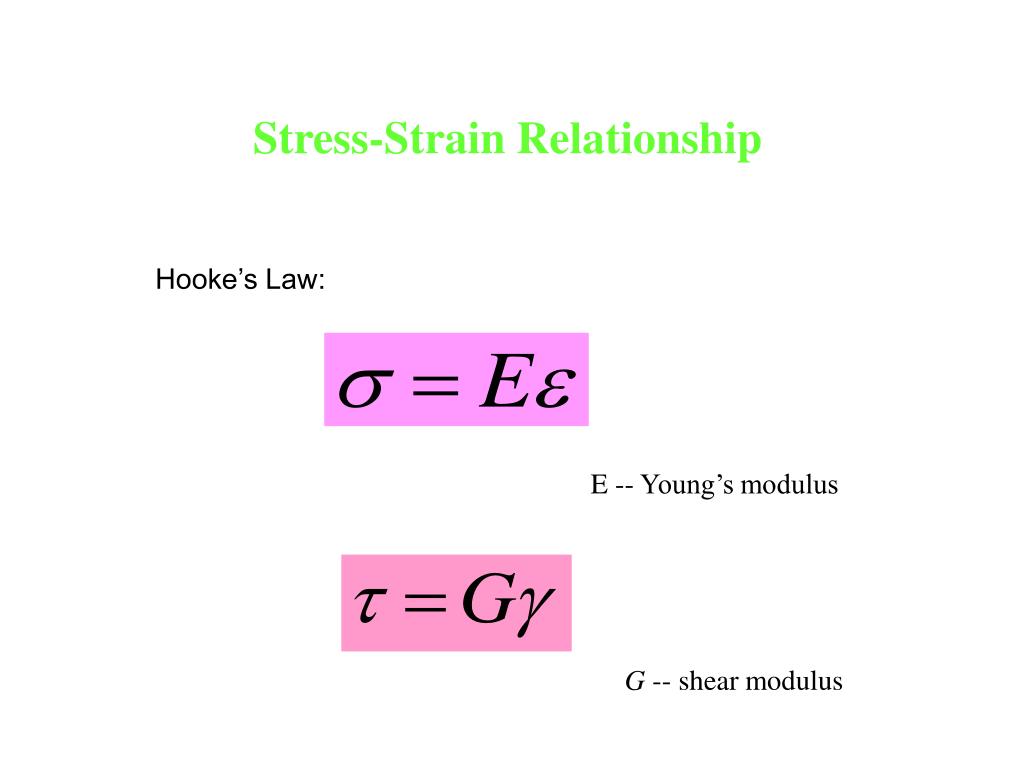
I was testing thin aluminum sheets, roughly half a millimeter thick, for a automotive bracket application. The specimens were breaking right at the grip edges instead of in the gauge section. Every single one. The load was dropping off abruptly, and the strain readings were garbage. The initial fix was to sand the grip surfaces and use softer jaw faces. That helped but did not solve it completely. The real fix was switching to a different specimen geometry with a longer tapered transition zone. It moved the stress concentration away from the grip interface. We also reduced the grip pressure to the minimum needed to prevent slippage. Once we did that, the fractures happened in the gauge section where the data mattered. The modulus and yield values stayed consistent across all samples. That geometry change alone cut our scrap rate from about forty percent down to under five percent. Young's modulus is not a design limit. It tells you stiffness, not strength. A ceramic and a polymer can have very different moduli and still both be brittle. Modulus does not predict whether something will yield or fracture. Yield strength and ultimate strength do that. The yield point is not always sharp. Some materials, especially low-carbon steels, show a clear upper and lower yield point. Most other metals just have a gradual transition from elastic to plastic behavior. For those, we use the offset method. We draw a line parallel to the elastic slope starting at a specified strain offset, usually zero point two percent. The intersection with the stress-strain curve gives the yield strength. This convention exists because there is no natural yield point for many materials. It is arbitrary but universally accepted. If you report a yield strength without saying what offset you used, someone else cannot compare your number to theirs. Always specify the offset.
When The Standard Approach Breaks Down
The engineering stress-strain approach fails for materials that undergo large deformations before failure. Rubber, soft tissues, and some polymers can stretch several hundred percent. Engineering strain becomes a poor descriptor because the reference length changes so dramatically. True strain handles large deformations better since it is based on incremental changes. For these materials, hyperelastic constitutive models are more appropriate. Ogden, Mooney-Rivlin, and Neo-Hookean models are commonly used. They require parameter fitting from experimental data and do not rely on the small strain assumptions behind Hooke's law. Another case where the standard model breaks is at high strain rates. The stress-strain curve you get at a quasi-static test speed can look very different from one obtained at impact loading rates. Metals generally show increased flow stress at higher strain rates. Polymers are even more sensitive. If your application involves dynamic loading, a static tensile test will not give you the right material properties. You need split Hopkinson bar testing or a servo-hydraulic system capable of high strain rates. The equipment is expensive and the data analysis is more involved, but skipping it will give you wrong answers for high-rate applications.
Practical Tips That Matter
Calibrate your extensometer. I have seen people skip this because the machine claims to be accurate. The load cell calibration may be fine, but the extensometer can drift or get mounted incorrectly. A misaligned extensometer reading on the modulus can throw off your elastic analysis entirely. It takes about ten minutes to verify with a certified gauge block. Do it before every test batch. Measure the cross-sectional dimensions at three points along the gauge length and average them. Specimens are not perfectly uniform. Using a single measurement can introduce error into your stress calculation, especially for low-strength materials where the absolute stress values are small and the relative error matters more. For the aluminum sheets I mentioned, the thickness variation across a single specimen could account for up to three percent difference in calculated stress. That is significant when you are comparing materials within a tight tolerance band. Report your strain rate. The modulus is generally independent of strain rate for most metals in the elastic region, but the plastic behavior is not. Two tests on the same material at different crosshead speeds can produce different yield strengths and different elongation values. If you do not report the strain rate, nobody can reproduce your conditions. Just state the crosshead speed and the original gauge length. Anyone can calculate the approximate engineering strain rate from those two numbers.

The Formula Recap
Engineering stress sigma equals F over A naught. Engineering strain epsilon equals delta L over L naught. True stress sigma true equals F over A instant. True strain epsilon true equals ln of L over L naught. Young's modulus E equals stress divided by strain in the elastic region. These formulas assume uniform deformation and a prismatic specimen with constant cross-section. When those assumptions do not hold, you need different approaches or corrections. That covers the essential framework. The details you need depend on what material you are testing and what question you are trying to answer. The formulas above work for most metals under standard tensile test conditions. Beyond that, the specifics matter more than memorizing equations.