How Gas Turbines Actually Work In Practice
Most people learn about the ideal Brayton cycle in school and think they understand gas turbines. They don't. The thermodynamic cycle is clean on paper. Real engines are messy, and the fundamentals shift depending on whether you're dealing with a small aero-derivative unit or a 300-megawatt industrial frame. A gas turbine engine compresses incoming air, mixes it with fuel, ignites it, and extracts work from the expanding hot gases. That is the textbook description. In practice, the compression stage alone consumes roughly forty to fifty percent of the gross power produced by the turbine section. The net output is what matters for any application, and that number changes dramatically with ambient conditions.
Fundamentals Of Gas Turbine Engines
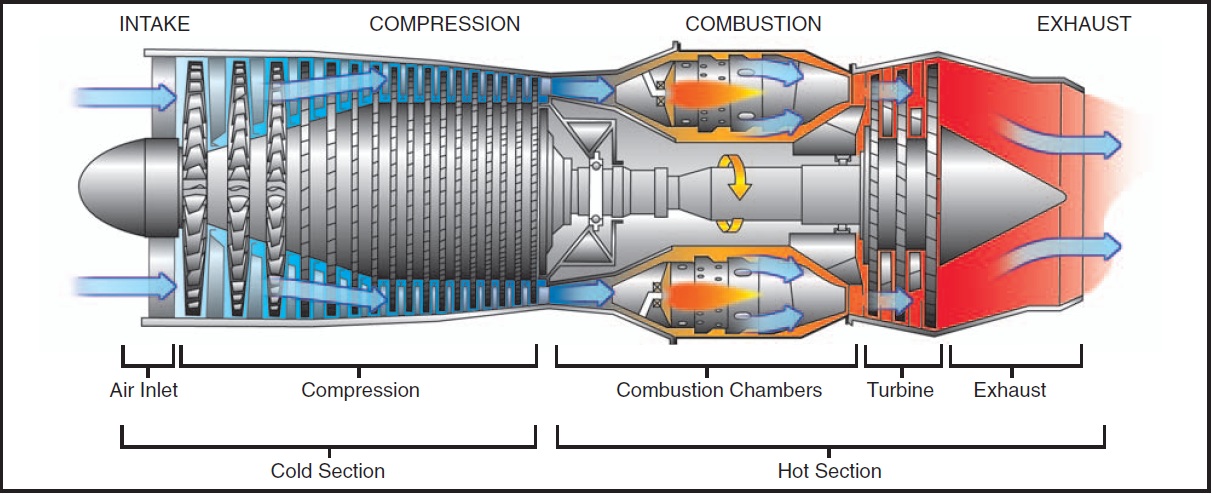
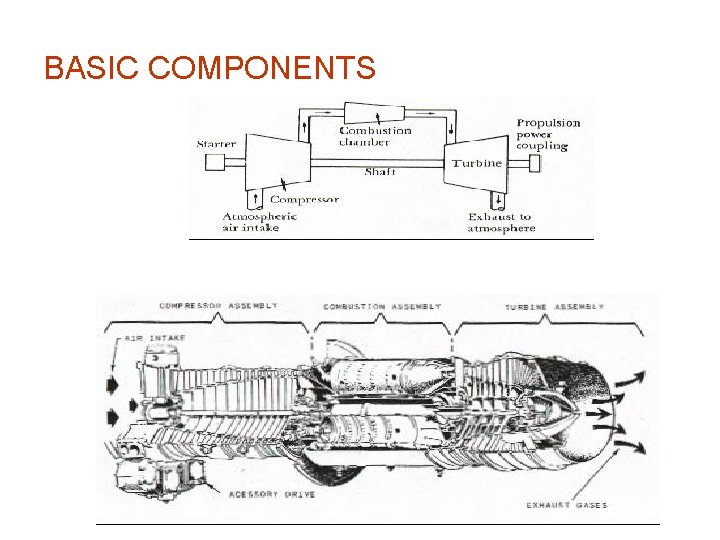
The core components are the compressor, combustion chamber, turbine, and exhaust. Air enters the intake and passes through axial or centrifugal compressors that raise the pressure significantly. Pressure ratios in modern engines range from about eight-to-one in older designs to over forty-to-one in newer heavy-duty units. The compressed air then enters the combustor, where fuel is injected and burned at near-constant pressure. The resulting high-temperature, high-velocity gas expands through the turbine stages, driving both the compressor and the output shaft. Thermal efficiency improves as the turbine inlet temperature rises and as the compression ratio increases. That is straightforward. What most people miss is that there are hard material limits on turbine inlet temperature. Single-crystal superalloys and advanced thermal barrier coatings push the boundary, but you cannot simply increase temperature indefinitely. The first-stage turbine blades in a typical heavy-frame industrial engine operate at temperatures exceeding one thousand four hundred degrees Celsius, while the metal itself may be sitting near its melting point. Cooling air bled from the compressor flows through internal passages in the blades to keep them from failing immediately. That cooling air does not participate in combustion, which means every kilogram of cooling air is a kilogram not contributing to power output. There is a constant trade-off happening here that textbook diagrams never show. Part-load performance is another area where fundamentals and reality diverge. Gas turbines are notoriously inefficient at partial load. A unit rated at three hundred megawatts at design conditions might drop to less than thirty percent thermal efficiency when running at fifty percent load. The compressor approaches surge boundaries, the combustion dynamics change, and excess air simply gets vented. For base-load power generation this is manageable. For peaking plants or applications with frequent load cycling, it becomes a serious operational headache. Some operators use steam injection (ITC) to restore part-load efficiency, but that adds complexity and requires a water treatment system.
I spent several years working on site modifications for a fleet of aging Frame 6C gas turbines, and one particular issue stands out. We were seeing unexpected blade coating degradation in the first turbine stage after roughly eight thousand operating hours. The standard interval was twelve thousand hours, so we were losing margin we didn't have. Initial suspects were fuel impurities and excessive inlet particle loading, but samples came back clean. The actual cause turned out to be a combination of low-frequency combustion oscillations around the two-hundred-hertz range and minor variations in the coating application process from the previous rebuild shop. The oscillations created cyclic thermal stress that fatigued the thermal barrier coating faster than expected. We addressed it by adjusting the fuel-air distribution nozzles to dampen the oscillation and specified a different coating thickness tolerance on the next rebuild. The issue was not in the fundamentals. It was in the details that no manual covers.
Get the Full Details

Starting And Control Sequences
Gas turbines do not self-start. An external starter motor, typically electric or hydraulic, spins the rotor up to a minimum speed where ignition can occur. Once the combustor fires and the turbine produces enough torque to overcome the compressor drag, the engine becomes self-sustaining. The control system then gradually opens the fuel valve to accelerate the unit to rated speed. This entire sequence usually takes between thirty and ninety seconds depending on the engine size and whether it is hot or cold. Hot starts and overtemperature events during acceleration are real risks. If the fuel is introduced too quickly before the combustion is stable, the turbine inlet temperature can spike beyond design limits in a matter of seconds. Modern digital control systems monitor (exhaust gas temperature) at multiple thermocouple locations around the circumference and enforce strict temperature rise rate limits during startup. The spread between the hottest and coolest thermocouple reading, known as delta-T, is also monitored. A large delta-T during operation indicates uneven combustion or airflow distribution and can trigger automatic derating or shutdown.
Maintenance Realities
Heavy maintenance overhauls on industrial gas turbines are expensive and time-consuming. A full hot gas path inspection on a Frame 7FA-class engine typically requires removing the exhaust casing, extracting the combustor cans or liner assembly, and inspecting or replacing all stationary and rotating blade rows. The standard interval has stretched from four years to eight years or more on well-maintained units, but that depends heavily on fuel quality, inlet filtration, and operating profile. Inline air filtration is critical. Particulate matter erodes compressor blades, reducing efficiency by one to two percent per year if unchecked. A one percent efficiency loss translates to roughly three to five megawatts of lost output on a large unit, which is significant revenue loss over the lifetime of the engine. Compressor washing is a routine but often misunderstood procedure. Online washing using water or chemical solutions can recover some of the lost efficiency between scheduled overhauls. The typical recovery is one to three percent in heat rate improvement, performed every one to three months depending on contamination levels. However, washing too aggressively or too frequently can damage compressor blade coatings and promote corrosion. There is a narrow window that depends on the specific compressor design and the type of contaminants present. One limitation worth noting: gas turbines are extremely sensitive to altitude and ambient temperature. Power output decreases by approximately one percent for every hundred meters of elevation gain above sea level, and by roughly two to three percent for every ten degrees Celsius increase in ambient temperature above standard day conditions. This is not a defect. It is physics. Anyone sizing a gas turbine for a location in the desert or at altitude needs to derate accordingly, or they will be disappointed at commissioning. Some manufacturers offer upgraded compressor or turbine components to mitigate this, but the fundamental relationship between air density and mass flow remains unchanged.
The exhaust system is often overlooked. Heat recovery steam generators (HRSGs) in combined cycle configurations expose the gas turbine exhaust cone to thermal cycling every time the unit starts and stops. This creates fatigue cracking over time, particularly at the transition pieces and casing seams. We saw this on a combined cycle plant where exhaust casing cracks developed after about fifteen thousand hours of cycling operation. The fix required a custom reinforcement sleeve and a modified startup ramp rate to reduce thermal shock. Planning for that kind of issue upfront saves considerable downtime later. Instrumentation accuracy is another practical concern. Exhaust thermocouples in gas turbines operate in a harsh environment and drift over time. A single out-of-spec thermocouple can cause the control system to misinterpret the average temperature and either overfuel or underfuel the combustor. Regular calibration and cross-checking against adjacent readings is essential. Some sites have run with a degraded thermocouple for months without realizing it, accumulating unnecessary thermal stress on turbine components. Combustion technology continues to evolve. Dry low NOx (DLN) combustors are now standard on most new industrial and aero-derived engines. They achieve very low emissions without relying on water or steam injection, which simplifies the overall system. But DLN combustors introduce their own challenges. They are more susceptible to combustion instability and lean blowout, particularly during startup and low-load operation. The control system must manage fuel staging carefully across the entire operating range. A misadjusted fuel distribution can lead to elevated NOx and CO emissions simultaneously, which is harder to troubleshoot than a simple rich-burn problem.

If you are getting into this field, start with the basic thermodynamics but do not stop there. The real work happens in the gap between the ideal cycle and what the hardware actually delivers. Fuel composition, inlet air quality, ambient conditions, control system tuning, and maintenance history all interact in ways that are difficult to predict from first principles. The best operators treat every engine as a unique system and keep detailed records of how it responds to different conditions over time. That empirical knowledge tends to be more useful than any textbook.