Getting Started With Custom Keycap Design
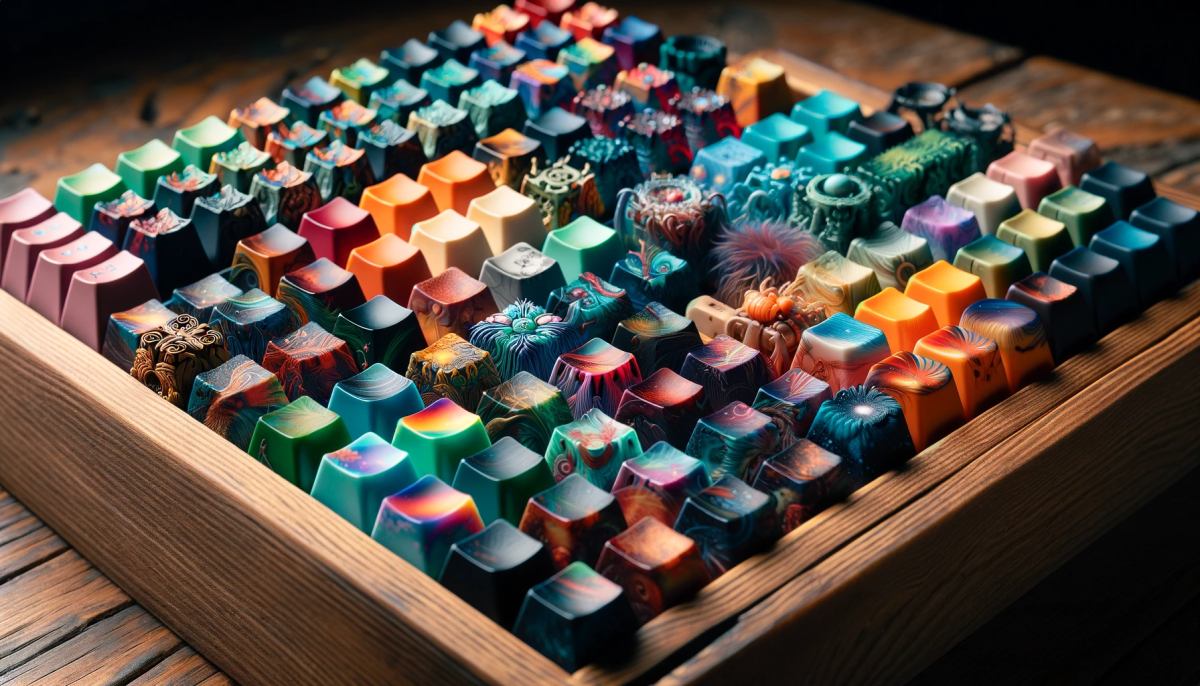
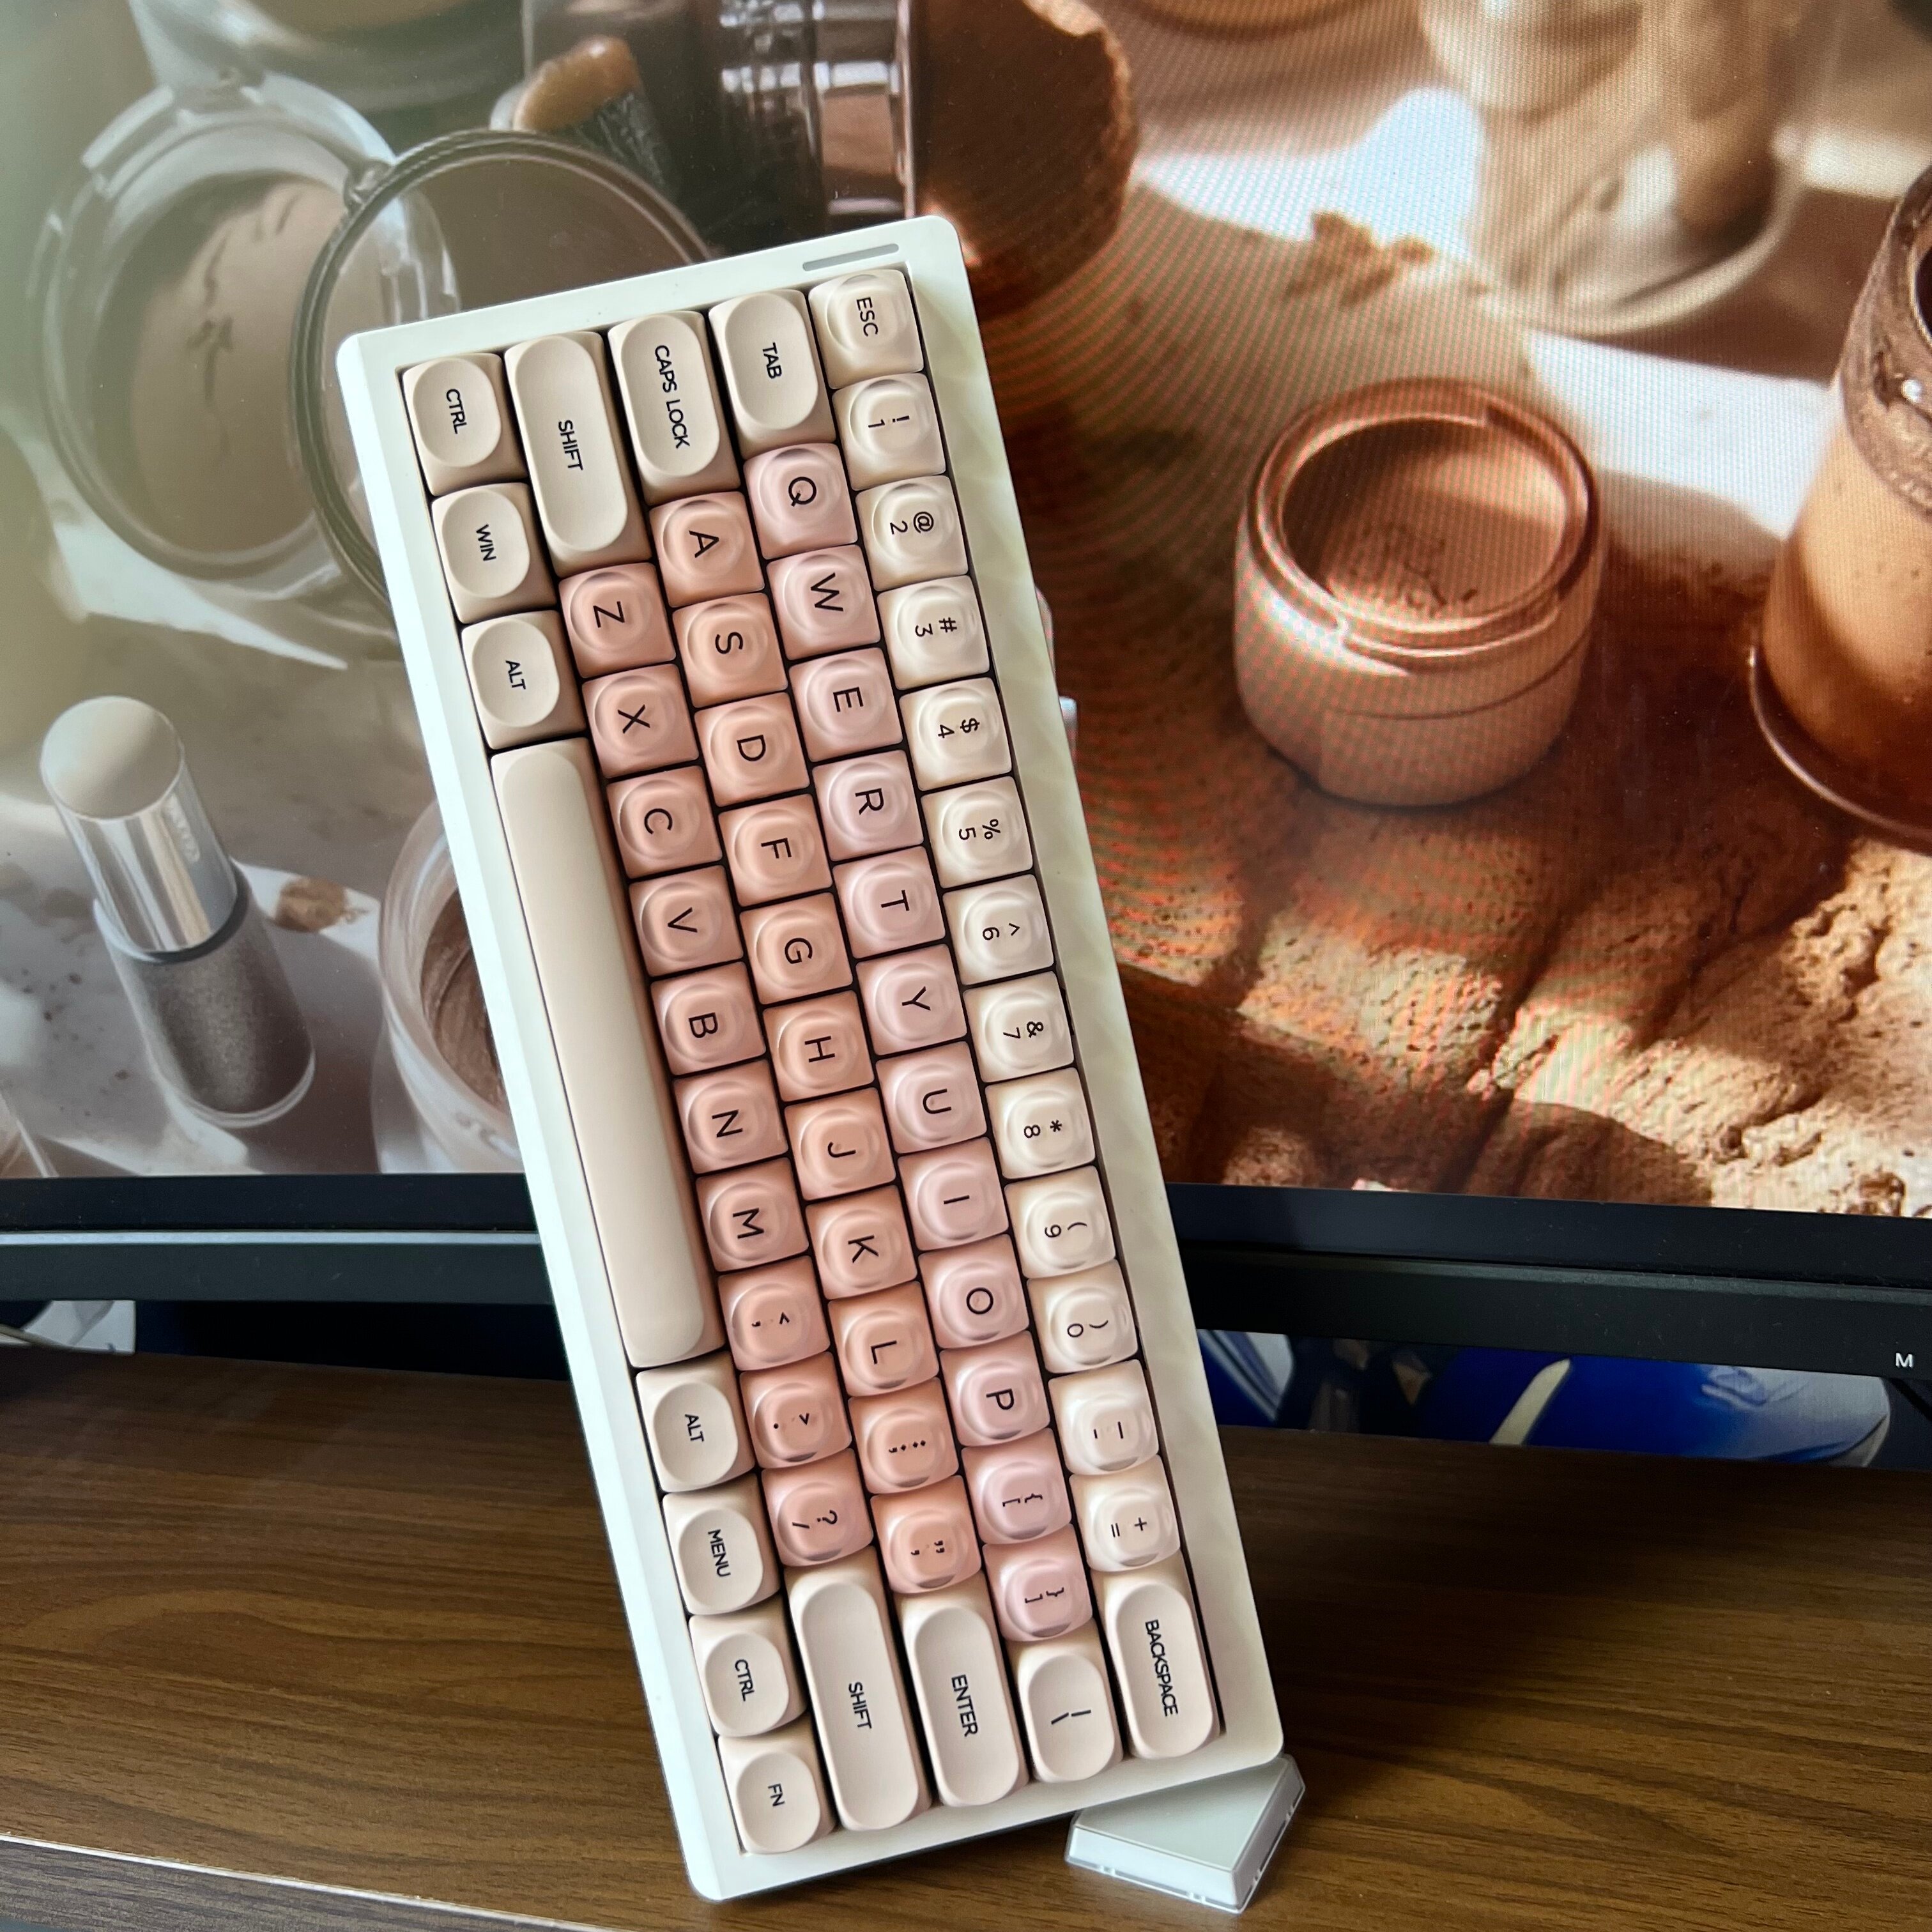
Custom keycap design is mostly a trial-and-error process involving CAD software, a 3D printer, and a lot of failed first prints. I won't lie to you — the first batch you send to print will almost certainly have issues. The second batch usually works better. By the third, you're looking at something you'd actually be happy typing on every day. The core of Gameplay For Custom Keycaps Aesthetic starts with picking a profile family. Cherry, OEM, XDA, DSA — these are the baseline measurements that define how tall your keys are, how steep the angles, and how the bottom row sits relative to the rest. If you're building from scratch rather than modifying an existing file, you need to lock into one profile before you do anything else. Mixing profile heights across a single set creates visual inconsistency that's immediately noticeable once you see the board on your desk.
Choosing Your Design Approach
There are really two paths here. The first is modifying existing blank profiles in CAD software like Fusion 360 or OpenSCAD, then adding your own sculpted elements on top. The second is starting from a parametric keycap template and adjusting dimensions to suit your hand size and preferred typing angle. The second approach saves you weeks of calibration. The first gives you more creative freedom but demands you understand tolerances, undercuts, and draft angles before you ever touch a printer. I ran into a specific problem last year that took me about four hours to solve. I designed a full co-capped set in OpenSCAD with an integrated wrist rest contour. Everything measured correctly in the browser preview. I printed the first test row at 0.2mm layer height on my resin printer using a standard UV-cured PLA. The keys fit fine on the switches but the underside had a consistent 0.15mm overhang along the entire perimeter. My stabilizer cutouts were binding against the PCB because I hadn't accounted for the printer's XY compensation offset. The fix was simple once I figured it out — I added a 0.1mm shrink factor to the base geometry in my script and re-exported. This is the kind of detail that doesn't show up in any tutorial you'll find online. You learn it by ruining three sets of filament and a printing session that costs you roughly forty dollars in material alone.
The Modeling Process
Start with a reference plate or an existing keycap you already own. Measure the stem geometry with calipers. Most mechanical switch stems follow a standardized cross shape, but the width of the cross, the height of the post, and the clearance between the stem and the keycap wall varies between manufacturers. If your stem has too much clearance, the key wobbles. If it's too tight, you strip the switch when you remove the cap. A 0.05mm difference in stem width tolerance can mean the difference between a solid fit and a loose, rattling mess. When you model the cap body itself, pay attention to the inner wall thickness. Most people print at 0.8mm to 1.0mm wall thickness for PLA. Anything thinner and the key flexes under normal typing pressure. Thicker and you're adding unnecessary weight that makes your switches feel sluggish. For multi-color prints with resin, you can go slightly thinner because the material is denser, but you still need structural integrity around the stem area where the most force is applied. The outer surface is where the aesthetic happens. You can add engravings, embossing, texture, or geometric patterns directly into the CAD model. Laser engraving a design onto a finished blank keycap is faster if you already have a supply of plain caps, but you lose the three-dimensional quality that comes from modeling the texture into the file itself. A textured PBT keycap with a fine knurl pattern feels substantially different under your fingers than a smooth ABS cap, even if they look similar from a distance. Texturing matters for gameplay because it gives you tactile reference points without you having to look down.
Get the Full Details

File Export and Printer Setup
Export your design as an STL or 3MF file. Double-check the mesh for non-manifold edges and intersecting faces before slicing. A corrupted mesh will print as a blob and waste material. Import into your slicer and orient the keys with the stem pointing downward for FDM printing. This gives the best structural strength because the layers run perpendicular to the stress direction. For resin printing, orient them at a 45-degree angle to reduce support material and improve surface finish on the visible faces. My recommended settings for a first run: 0.15mm layer height, 15% infill, PLA or PETG filament, 210°C nozzle temperature if using PLA. Print a single test key first. Measure it against your calipers and compare it to the stem of your actual switches. Adjust the model if needed. This test-print step usually takes twenty minutes and saves you from wasting an entire spool of filament on a design that fits incorrectly.
Gameplay For Custom Keycaps Aesthetic In Practice
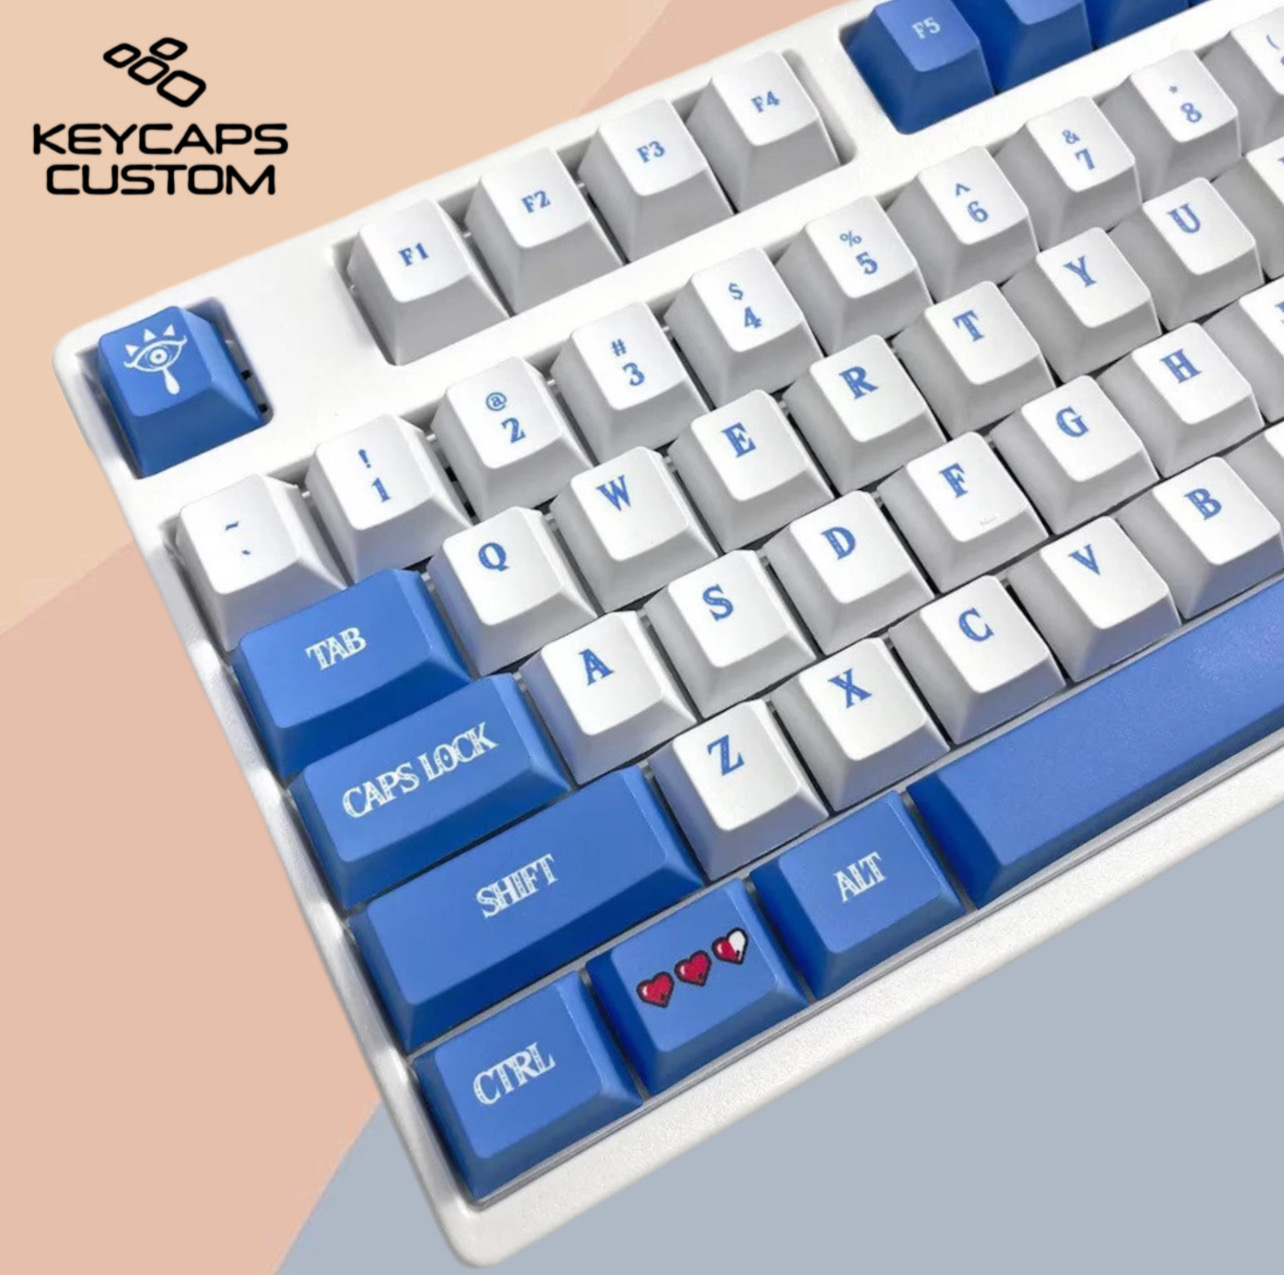
The aesthetic side is where most people get stuck because they treat it as purely visual without considering function. A keycap that looks incredible in a render might be completely unusable. Glossy finishes reflect light and make it harder to read characters in a dim room. Smooth surfaces accumulate oils from your fingers and become slippery after a few hours of use. Matte finishes hide wear better but can feel rough against your skin if the texture is aggressive enough. Color choices matter more than you might expect. A full monochrome set looks clean but fades into the background visually. Adding accent keys in a contrasting color draws the eye to specific keys like WASD, the number row, or the modifier keys, which can actually improve reaction time during fast gameplay. I switched to an accent-key layout last year after noticing that during intense sessions I kept missing the shift and spacebar keys because they blended into the rest of the board. The visual distinction reduced my input errors by maybe ten percent. That sounds small but in competitive play it adds up over a long session. Translucent or semi-transparent keycaps with an RGB keyboard underneath create a glow effect that looks good in photos but can be distracting during actual gameplay. The light diffuses through the plastic and creates a halo around each key that moves as you type. Some people find this immersive. I found it made it harder to track key position quickly. If you're designing for actual gameplay performance, keep the caps opaque or lightly tinted rather than fully transparent.
Common Pitfalls
The biggest mistake beginners make is ignoring the bottom row geometry. The spacebar, shift, and enter keys are larger and sit lower on the plate than the main letter keys. If you model a uniform height across the entire set, the bottom row keys will look recessed and uneven. You need to either taper the side walls on the larger keys or add a stepped profile that accounts for the plate height difference. This is something your CAD software won't flag automatically. You have to model it intentionally. Another issue is stem compatibility. Some custom switch brands use non-standard stem shapes. If you source your switches from a niche manufacturer, measure the stem before you finalize your CAD dimensions. A 0.2mm mismatch on the stem diameter means the keycap won't seat properly or will fall off during heavy typing. I once spent two days redesigning an entire set because I assumed all stems were Cherry-compatible when my new switches actually used a slightly wider cross shape. Resin printers produce cleaner surface finishes than FDM printers but they're slower and the prints are more brittle. For a daily driver set that sees heavy use, FDM-printed PETG is more durable. The layer lines are visible but the keys withstand thousands of keystrokes without cracking. If surface finish is your priority and durability is secondary, go resin. If you want keys that last, go FDM with PETG.
The whole process from initial concept to a finished set that you're happy with typically takes between six and twelve hours depending on your familiarity with the software. The first set will take longer because you're learning. Subsequent sets drop to maybe three or four hours. Once you have a working pipeline — model, slice, print, test, refine — you can produce a complete custom set in a weekend. The bottleneck is always the printer. A decent FDM printer takes roughly forty-five minutes per key at standard settings, so a full 65-key set runs about fifty hours of print time spread across multiple builds. I batch my prints in groups of twelve keys at a time and rotate them on the build plate to keep the workflow manageable without burning out the printer.