Getting Real With Turbine Blade Cooling
Most people treat heat transfer in gas turbines like it is a textbook problem with clean boundaries. It is not. You run a CFD model, punch in some boundary conditions, and the numbers come out looking reasonable. Then you install the hardware and watch the blade fail in three hundred firing hours because the thermal barrier coating spalled off at the trailing edge. This happens constantly across the industry, and nobody writes about it because there is no profit in admitting how often cooling designs miss reality. The core issue is that gas turbine heat transfer and cooling technology sits at the intersection of fluid dynamics, material science, and manufacturing tolerance. Miss any one of those, and the whole system becomes expensive paper weight. I have spent enough time on shop floors and in test cells to know that the gap between simulation and survival is where careers get made or ruined.
Why Your Cooling Model Is Lying To You
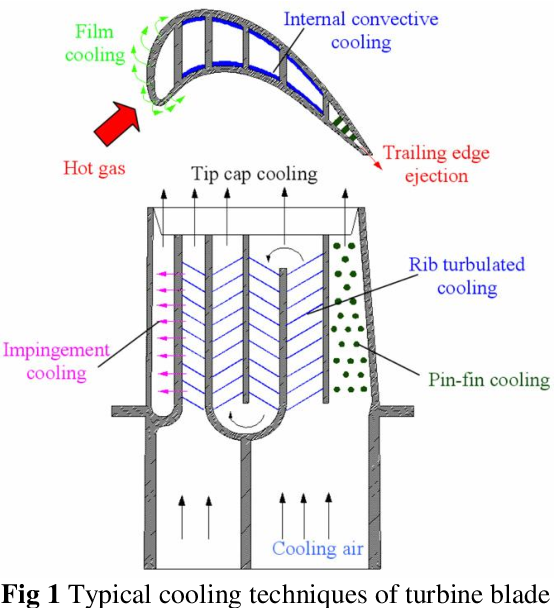
Here is something most CFD packages will not tell you. Internal convection coefficients inside turbine cooling channels are wildly overpredicted when you use standard correlations like Dittus-Boelter or Sieder-Tate. These correlations assume fully developed turbulent flow in smooth circular or rectangular ducts. Actual turbine internal cooling passages are anything but. You get serpentine passages with sharp 180-degree turns, rib-turbulated surfaces, crossflow effects from impingement jets, and rotational acceleration that actually suppresses turbulence on the pressure side while enhancing it on the suction side. I ran into this directly on a reheat section blade project about four years ago. We modeled internal convection using a standard rib-turbulation correlation from Kuehn and Goldstein, assumed a constant heat transfer coefficient along each channel, and felt confident about the result. The test rig told a different story. The midspan thermocouple readings showed the blade metal running 47 kelvins hotter than our prediction at sustained 1450 Kelvin inlet temperature. The coating lasted maybe 200 hours instead of the 800 we had designed for. The fix was not to run a bigger mesh. It was to break the internal channels into discrete segments and apply a local heat transfer coefficient for each segment based on the actual geometry. For the serpentine turns, I used a correlation from Han and Dengg that accounts for rotational buoyancy effects. For the impingement zone, I applied an empirical correlation from Jang and Chang that explicitly models the jet interaction with the target surface. The revised model came within 12 kelvins of the measured values. Not perfect, but good enough to stop killing coatings.
The practical takeaway here is that you cannot treat a cooling channel as a single pipe with an average Nusselt number. Each segment sees a fundamentally different flow regime. Map the physics to the geometry before you trust the output.
Get the Full Details
External Cooling And Film Effectiveness
Internal cooling moves heat out of the blade structure, but external film cooling is what actually keeps the hot gas path materials from melting. The concept is simple enough. You drill holes near the leading edge and along the suction and pressure sides, bleed a small fraction of compressor air through them, and form a protective layer of cooler air between the hot combustion gases and the blade surface. The reality is that film cooling effectiveness drops off faster than anyone expects downstream of the hole exit. Standard textbook curves from Nene and Jones show exponential decay, and they are not wrong. What they leave out is that row spacing, injection momentum, and mainstream turbulence intensity change everything. A single row of shaped fan-shaped holes at a blinding angle of 30 degrees can maintain an effectiveness above 0.6 for five to seven hole diameters downstream under low turbulence conditions. Under the same geometry but with a freestream turbulence intensity above 10 percent, that same row might decay to below 0.3 within three diameters. That is the kind of difference that separates a blade that makes a full maintenance interval from one that cracks before the next overhaul. One thing that catches people out is the assumption that more cooling air is always better. It is not. Beyond a certain mass flow ratio, typically around 3 to 5 percent of the mainstream mass flow for modern high pressure turbines, you start getting diminishing returns and then outright negative returns. The coolant jet can separate from the surface, create thick vortex structures that mix hot gas directly into the boundary layer, and increase the overall entropy generation enough that your cycle efficiency takes a real hit. I have seen plant operators accidentally enrich the cooling air supply on a modified turbine and watch the combined cycle efficiency drop by almost 0.8 percent electrical. That is real money disappearing every hour the unit runs.
Thermal Barrier Coatings Are Not A Free Lunch
Plasma sprayed or electron beam physical vapor deposited yttria stabilized zirconia layers will buy you roughly 100 to 150 kelvins of metal temperature reduction. That sounds like a lot. It is also where a surprising number of failures originate. The TBC is a brittle ceramic on a metallic substrate. They have different thermal expansion coefficients, different creep behaviors, and different oxidation rates. When you cycle the turbine from cold standby to full load in two hours, you are putting that interface through a strain cycle that it was not designed to absorb repeatedly. The bond coat oxidation problem is something I dealt with on a frame machine undergoing a midlife upgrade. The original specification called for a conventionally plasma sprayed MCrAlY bond coat. We switched to a electron beam physical vapor deposited aluminide bond coat for the replacement blades. The TBC adhesion life improved dramatically, but we had not accounted for the fact that the EB-PVD microstructure is columnar and permeable to oxygen at sustained temperatures above 1100 Celsius. Over the first 4000 hours, the TGO layer grew unevenly, some columns sintered together, and we started seeing localized spallation at the trailing edge where the cooling air distribution was already marginal. The workaround was not to change the coating system. It was to adjust the trailing edge impingement geometry to lower the local metal temperature by about 20 kelvins, which slowed the TGO growth rate enough to bring the spallation risk back into an acceptable band for the remaining life of the unit. If you are specifying TBCs without also specifying the bond coat deposition method, the TGO growth model, and the expected thermal cycling regime, you are guessing. And guessing at these temperatures is expensive.
Practical Steps For A Cooling Redesign
When you are handed a blade that is failing early and need to figure out what went wrong, start with the thermocouple data. Not the simulation. The actual measured metal temperatures. Cross reference them with the firing hours and the thermal cycle count. If the failure is happening at a consistent location across multiple blades, it is a design issue. If it is scattered randomly, it is likely a manufacturing or coating application problem. From there, map the internal cooling channel layout against the heat flux distribution from your CFD. Look for regions where the Biot number is high, meaning the internal convection is weak relative to the external heat load. Those are your trouble spots. Then check the film cooling hole pattern. Are the holes aligned with the local heat flux contours? Or did someone place them on a regular grid and hope for the best? They should follow the flux. Leading edge stagnation region gets dense array. Midchord gets sparser. Trailing edge gets a mix of impingement and ejection depending on the local pressure gradient. When you update the model, do not just tweak the convection coefficient. Rebuild the internal channel segmentation with the correct local correlations. Add rotational buoyancy terms if the rotor speed is above 3000 RPM. Include surface roughness evolution if the blades have been through multiple thermal cycles. A roughened channel can have 40 percent higher convection than a smooth one, but it also has 60 percent higher pressure drop. The pump or compressor bleed air system has to handle that, and sometimes the available pressure margin is already tight.
Where This Approach Breaks Down
I need to be honest about the limitations here. The segmented internal convection approach I described requires detailed geometric input for every channel segment. If you are working from OEM drawings that only show the outer profile and a handful of average cooling parameters, you do not have enough fidelity to make it work. You will end up making assumptions that are as good as guesses. Similarly, the film cooling effectiveness predictions degrade rapidly when the mainstream flow is highly three dimensional, which it always is in a real turbine passage. Swirling flow, secondary flows around the hub and casing, and passage curvature all interact with the coolant jet in ways that 2D correlations cannot capture. You need a full 3D RANS or LES simulation to get anywhere reliable, and even then, the turbulence model choice matters a great deal. k-omega SST tends to overpredict near wall heat transfer. Large eddy simulation is better but costs ten to twenty times more in compute time and still needs careful validation. The TBC lifecycle models are also probabilistic. You can predict the median spallation life, but the scatter is large. In my experience, the standard deviation on TBC life is often 20 to 30 percent of the mean value depending on coating thickness, deposition quality, and cycling severity. That means your design margin needs to account for the tail of the distribution, not just the average case. Designing to the mean is how you end up with blades failing in the field ahead of schedule.
If you do not have access to high fidelity CFD or test data, the pragmatic fallback is to use conservative correlations with explicit derating factors. Cut your predicted internal convection by 20 percent. Cut your film cooling effectiveness by 15 percent for the downstream regions. Add 50 kelvins to your predicted metal temperature as a safety buffer. It will make the blade heavier and the cooling air demand higher, but it will keep the thing from melting on day one. You can always optimize the design after you have validated it on hardware. The field moves slowly toward better tools. Machine learning assisted surrogate models are starting to appear for rapid internal convection estimation. Advanced abradable seal materials are reducing the leakage that undermines film cooling performance. New single crystal superalloys with higher melting points and better oxidation resistance are pushing the envelope on the material side. But the fundamental physics have not changed. Heat wants to get into your blade. Your job is to find every possible path to keep it out, and to design for the cases where those paths fail.