How to Actually Use the Splicing Manual Without Ruining Your Belt
The first thing you need to understand is that the Goodyear Conveyor Belt Splicing Manual isn't a novel you read cover to cover. It's a reference document you pull apart under a harsh work light at 4 AM when three hundred tons of material per hour stops moving because your splice failed. Treat it that way. Reference, not reading. The manual is organized by belt construction—fabric ply, steel cord, hybrid—and each construction type has its own procedure. If you're splicing a 5-ply polyester-nylon belt using instructions meant for a steel cord belt, you're not just wasting time. You're creating a failure point that will open up under load somewhere around the midpoint of the splice. I learned this the hard way on a granite quarry line in 2019. We had a 36-inch-wide, 5-ply belt on the main feed conveyor. The original splice had delaminated near the tail pulley, and I was pulling the manual from a weathered binder that had been around since 2004. I followed the cold cure step by step, used the right plies, cut the ends at a 6:1 ratio, applied the adhesive, waited the correct time between coats, and vulcanized it at the specified temperature for the recommended duration. Everything looked textbook. The splice held for eleven days. Then it opened again at the same spot, and this time it was worse. The failure wasn't in the splice itself—it was in the belt preparation. What I'd missed is that the manual specifies a different surface treatment depending on whether the belt has a fabric cover or a bare carcass exposure. Our belt had a thin fabric cover over the ply edges from years of tracking wear, and I hadn't abraded those edges down to bare ply before applying the adhesive. The glue bonded to the worn fabric skin instead of the actual ply material. That skin peeled away under tension like a layer of dried paint, and the splice failed with it. I went back, ground the edges properly down to clean ply, re-prepped, and re-spliced. That second splice has held for over two years across multiple belt replacements on the same line. The fix was stupidly simple. The fact that I missed it the first time wasn't because the manual was unclear—it was because I was rushing and treating the surface prep section as optional guidance rather than a requirement.
Goodyear Conveyor Belt Splicing Manual: Where People Go Wrong
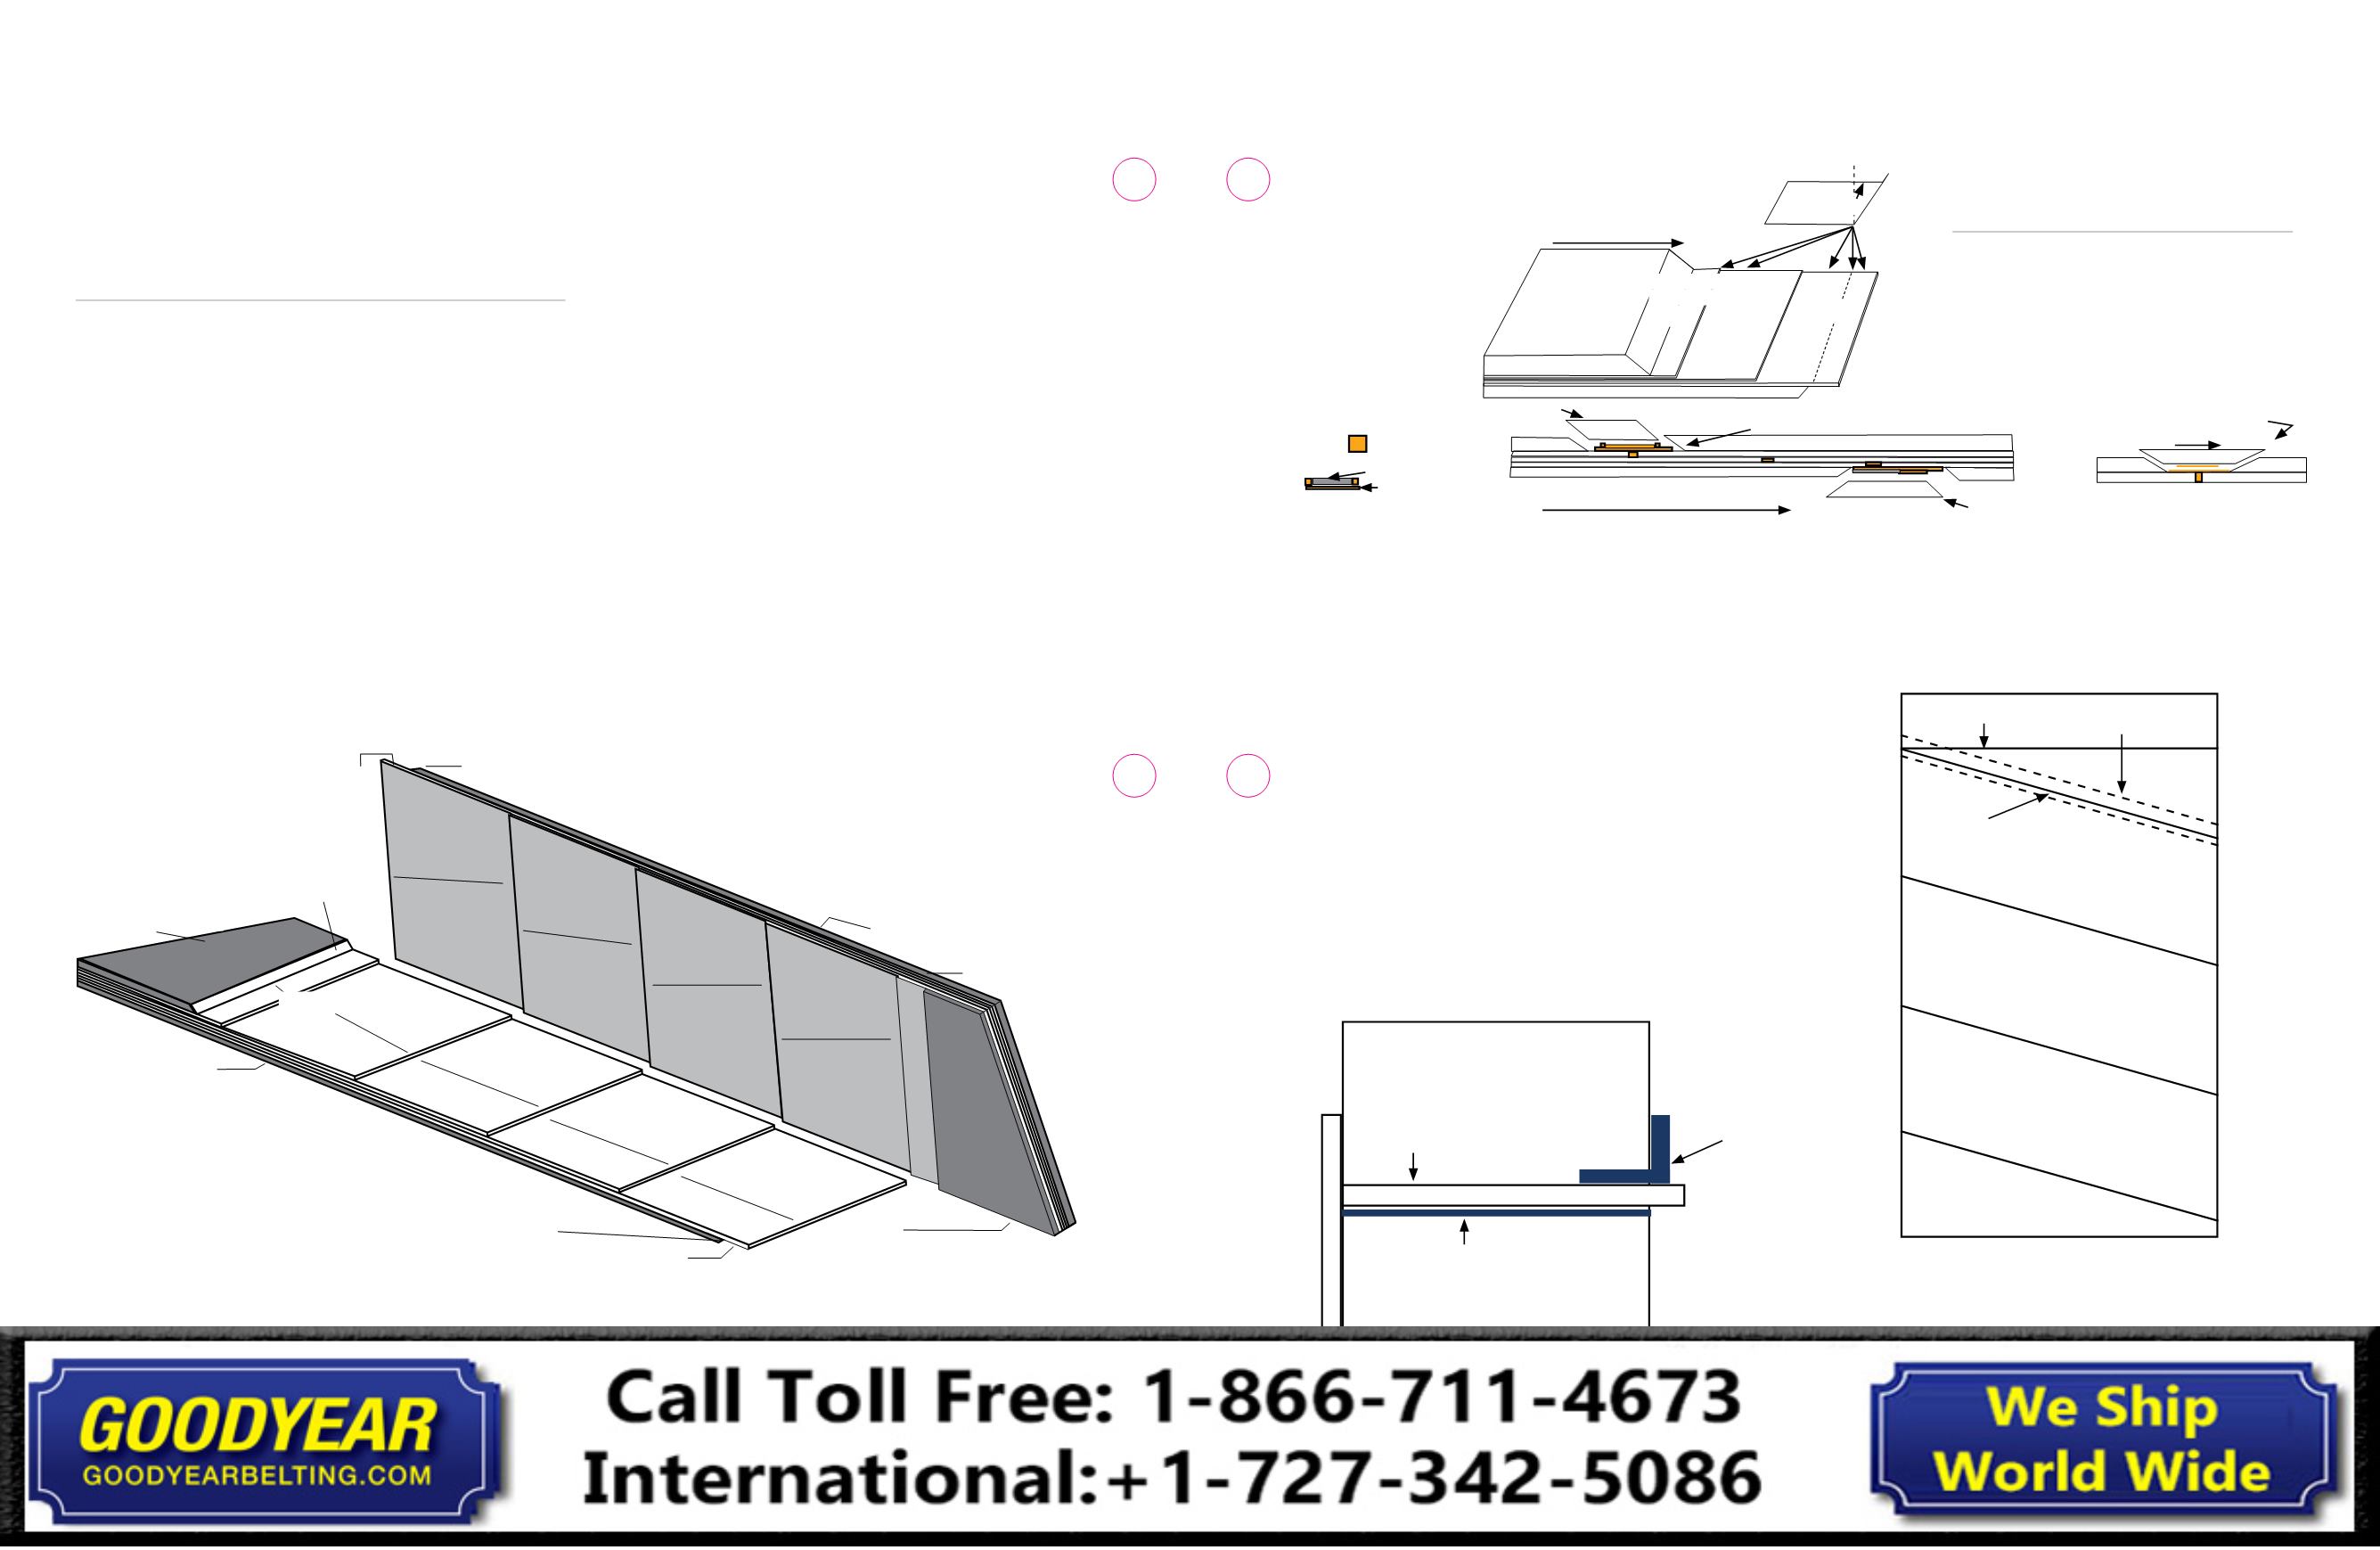
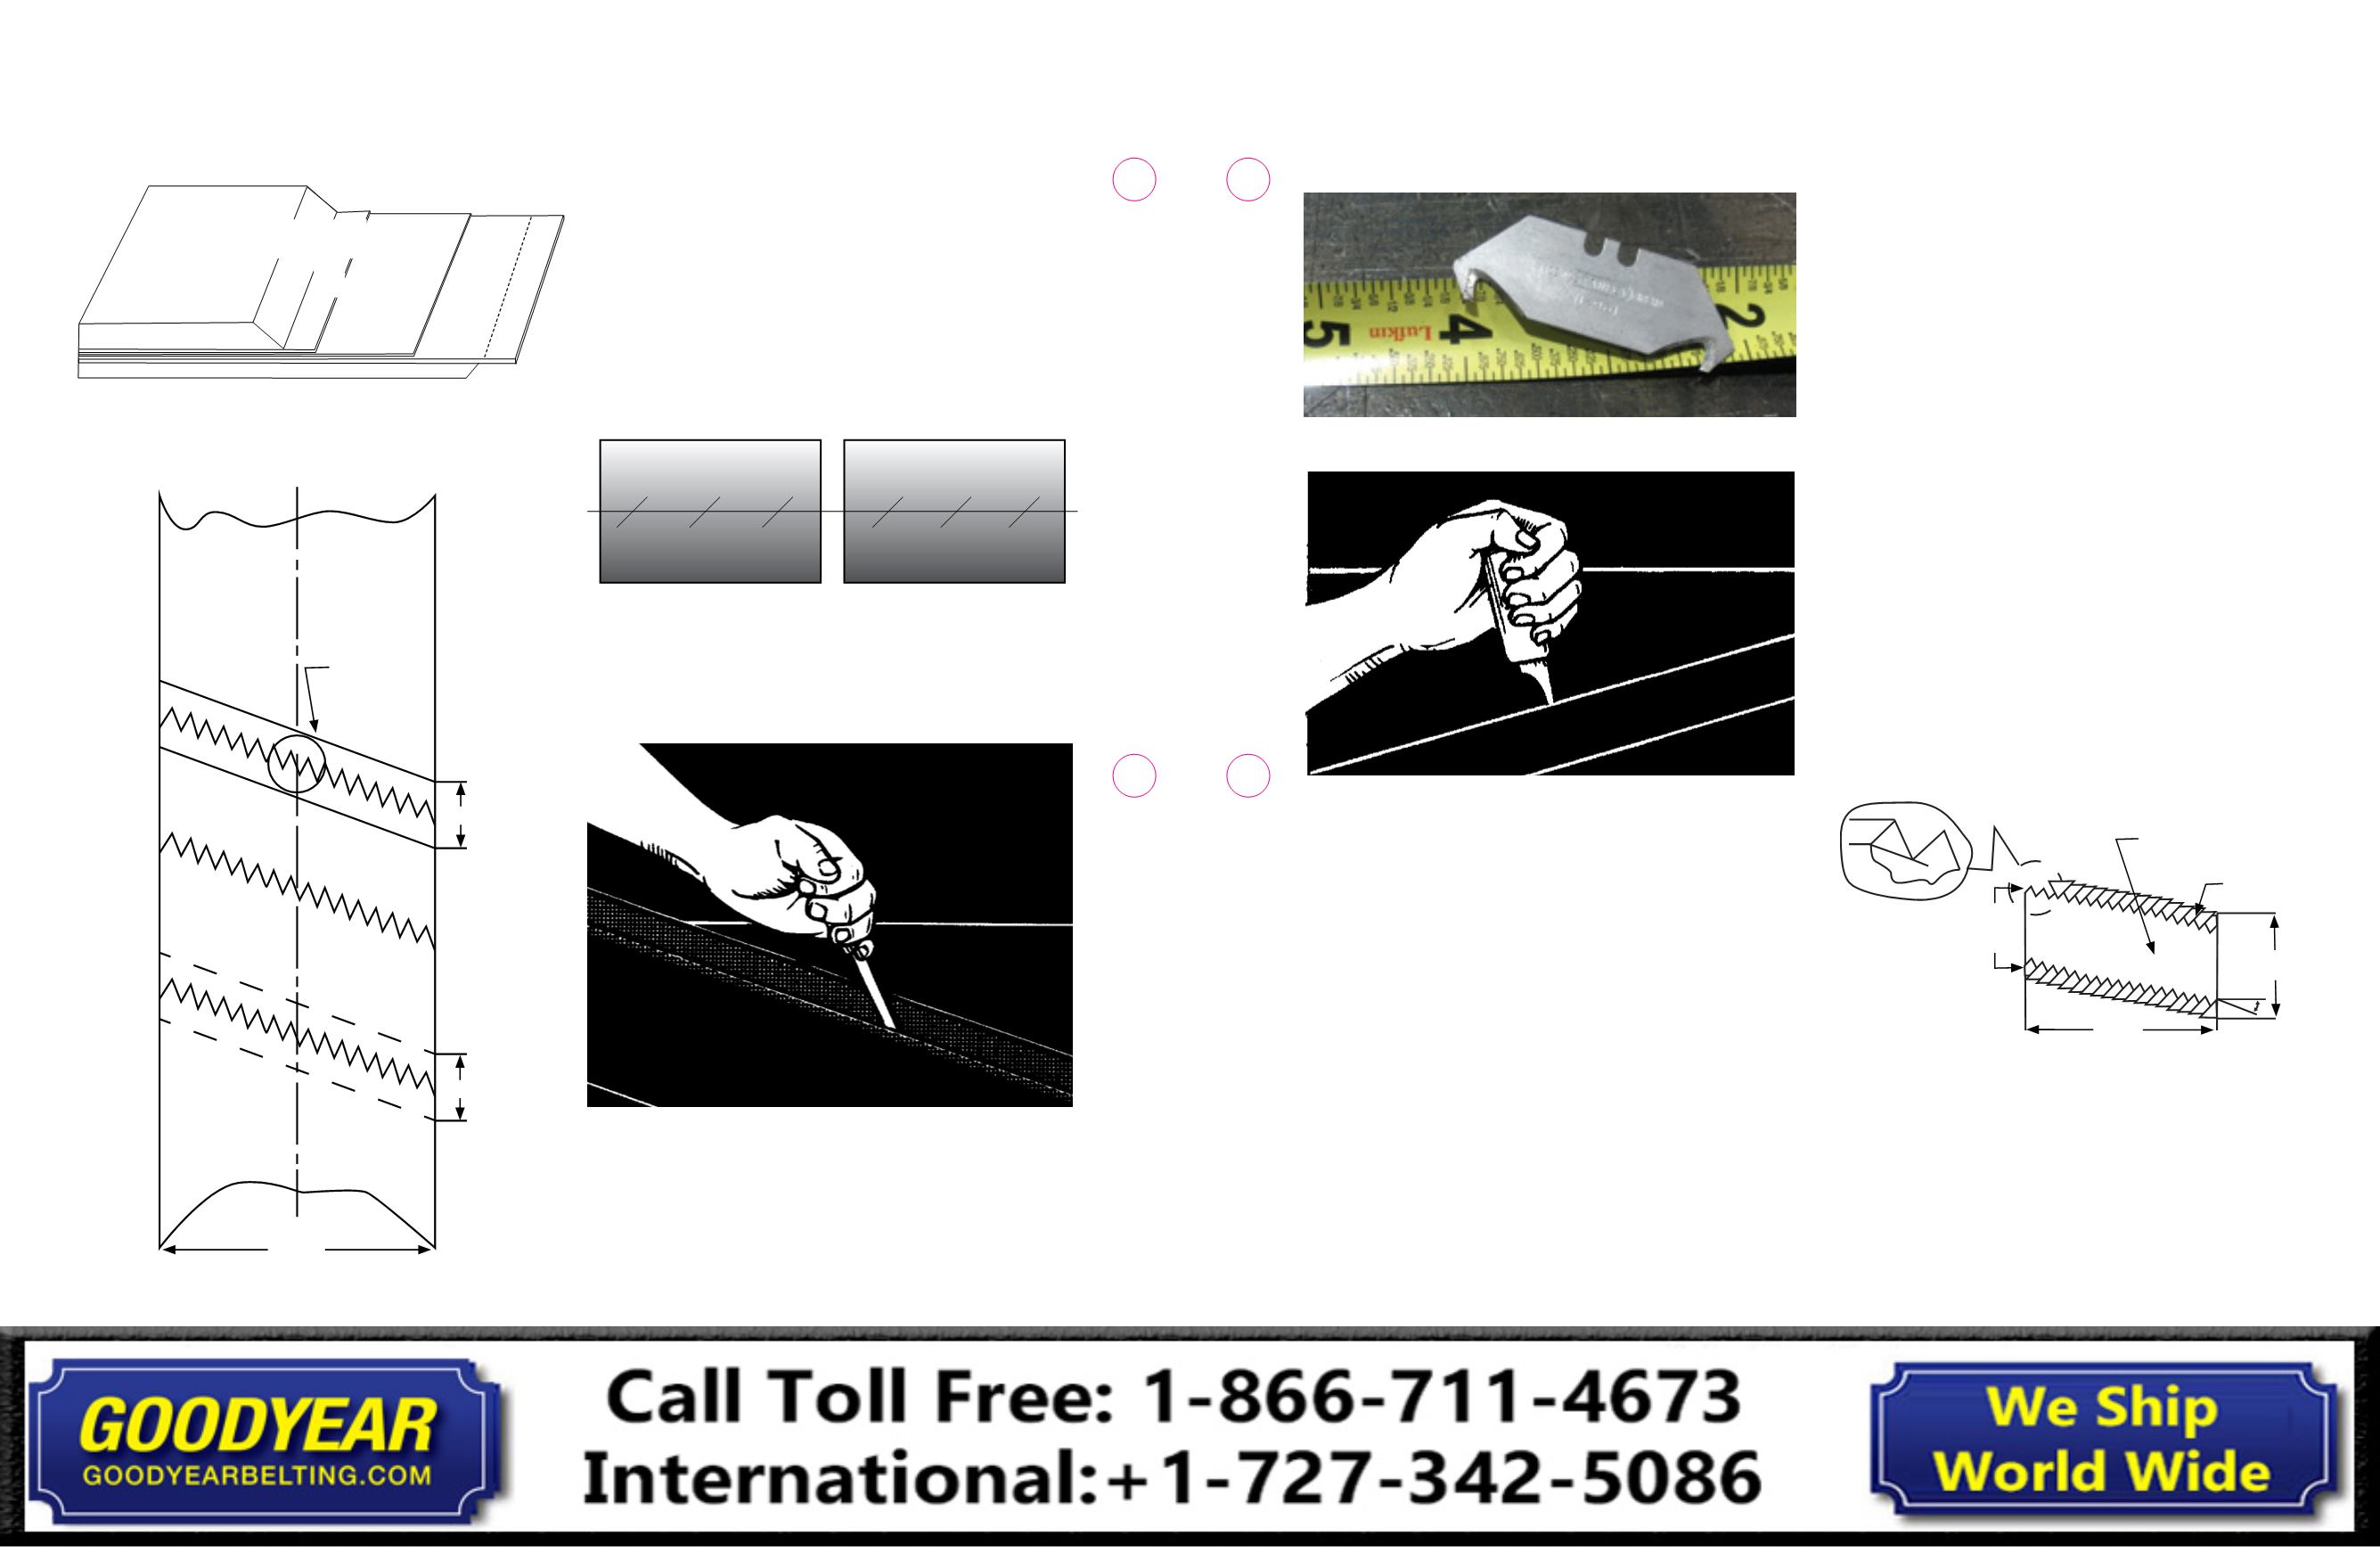
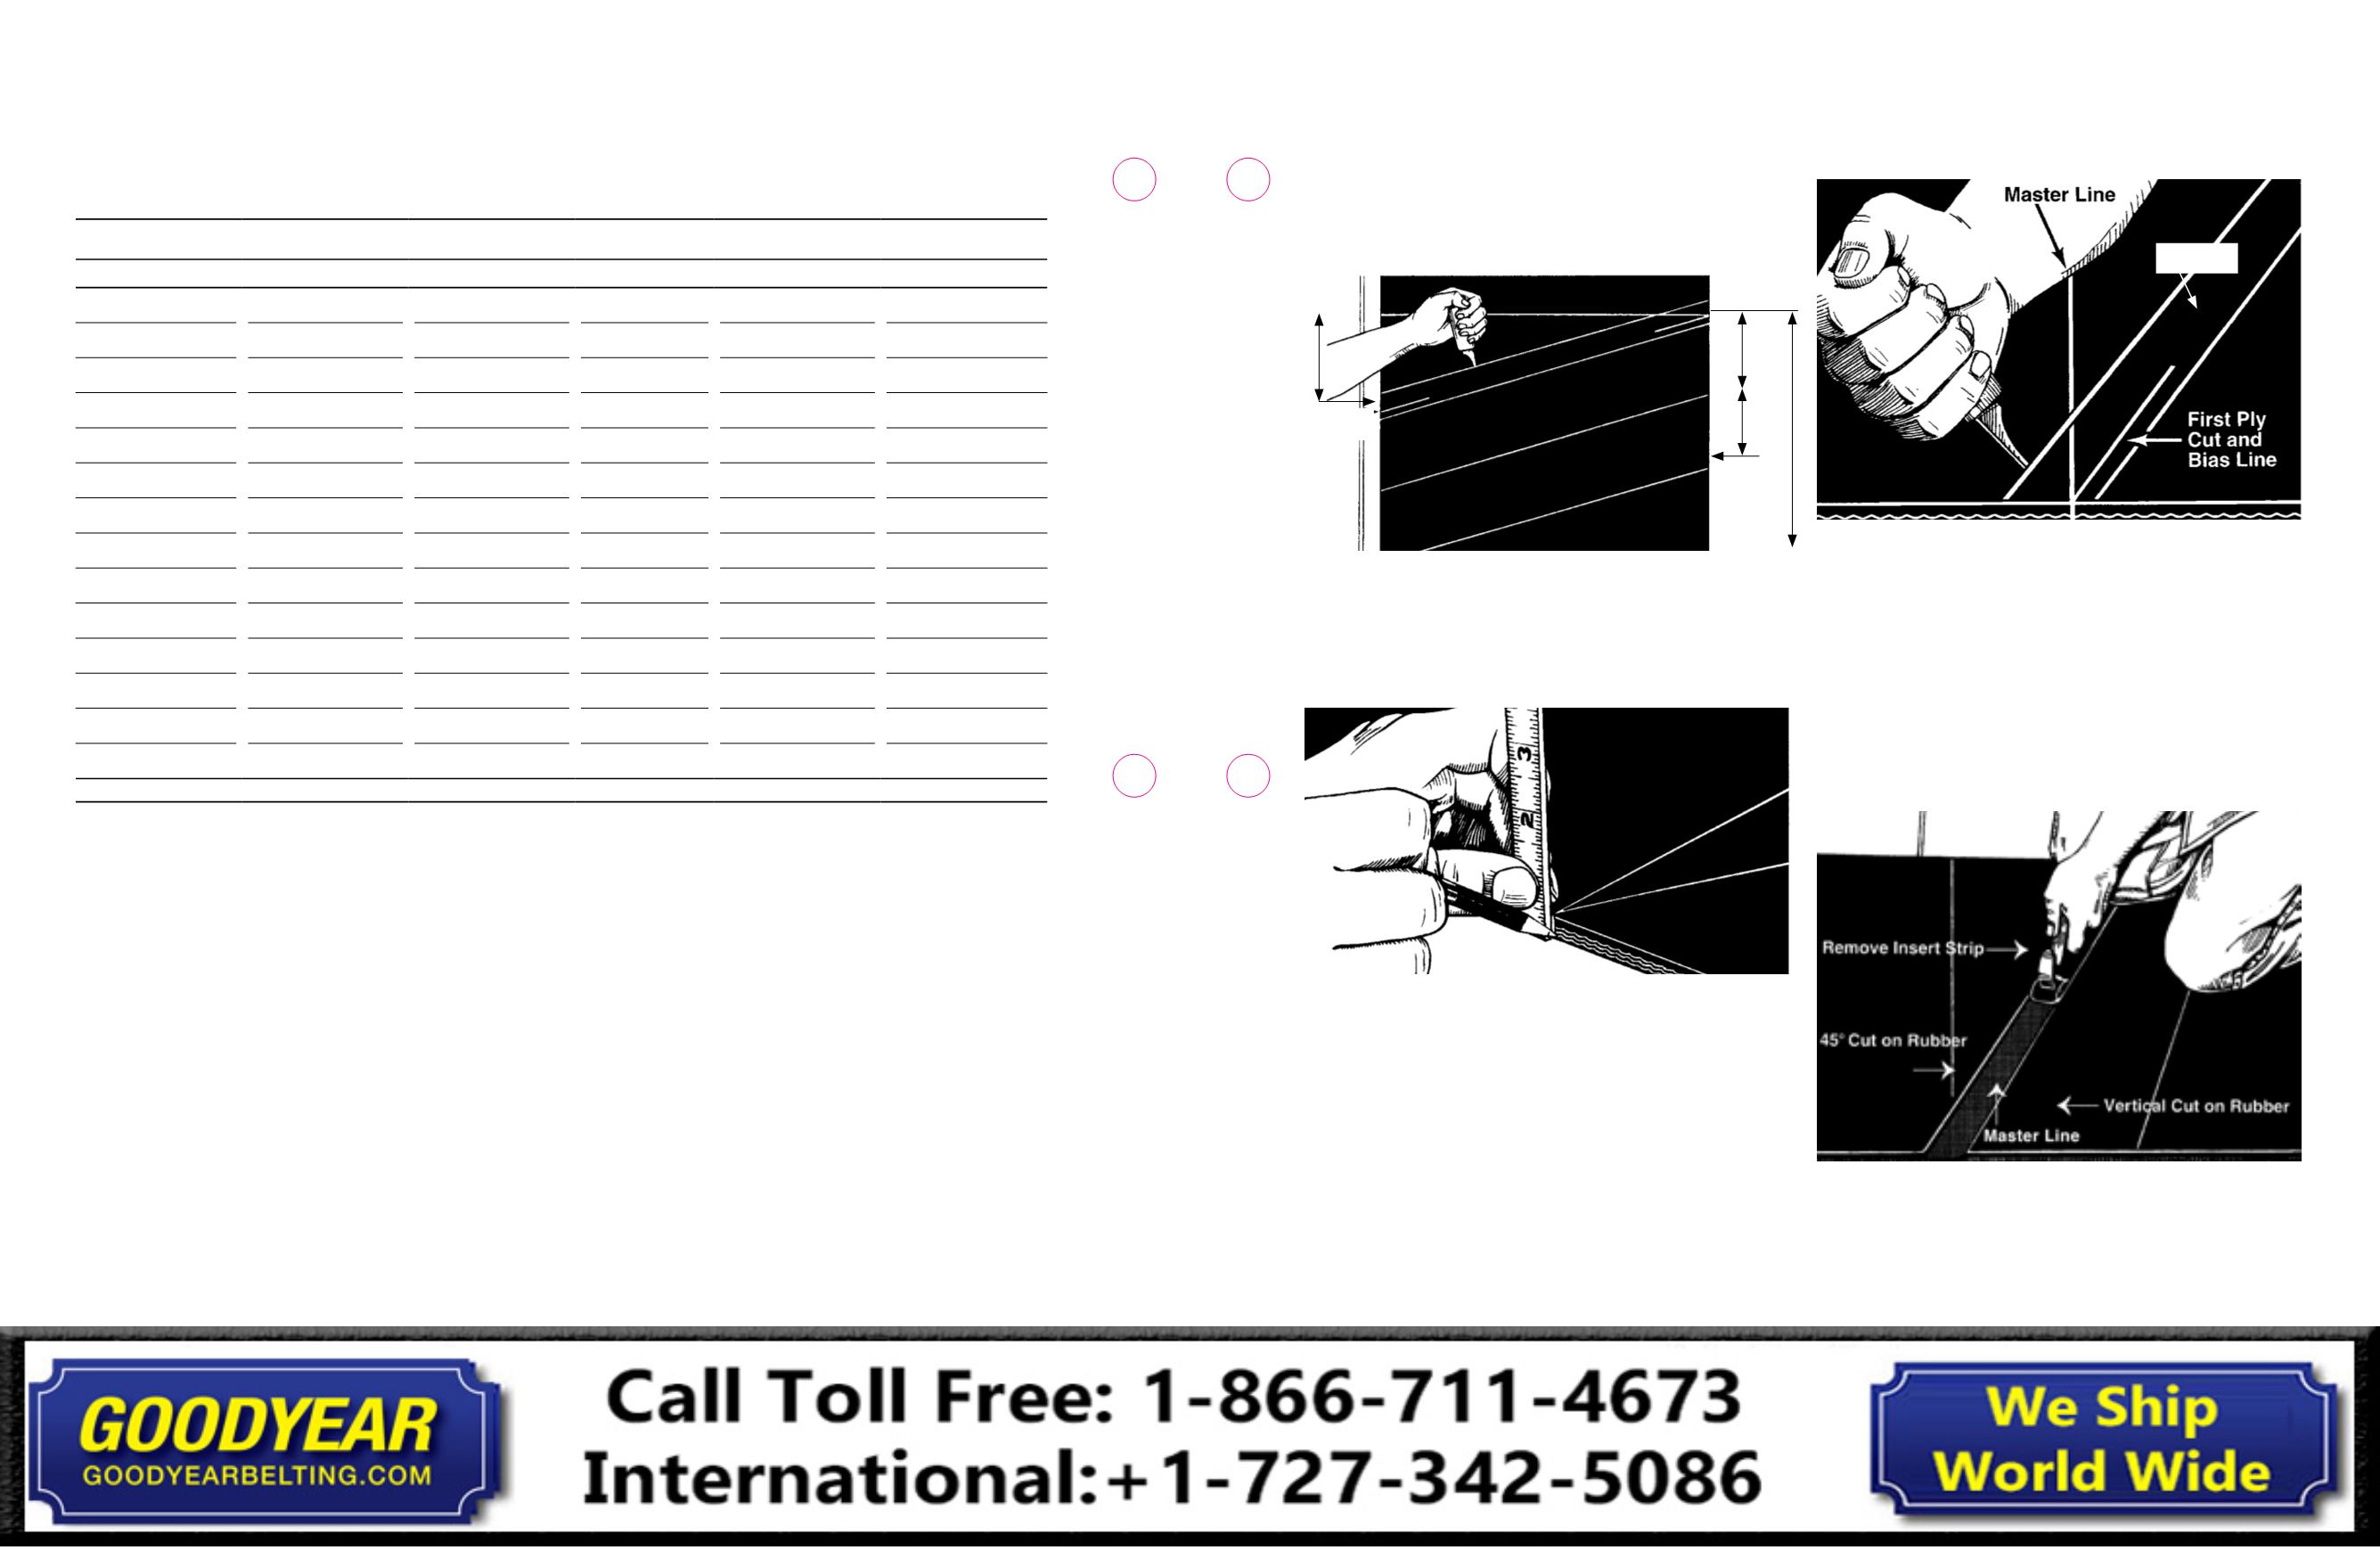
Step one is always belt inspection and planning, not cutting. The manual dedicates an entire section to evaluating whether a splice is even viable. Most people skip this. They see a broken belt and immediately start measuring for the splice length. Before you make a single cut, check the belt condition at least six feet away from the planned splice location on both sides. Look for frayed plies, separations between cover and carcass, water damage that's softened the fabric, or any area where the tension members are exposed and corroded. If the belt is degraded in those zones, a splice will fail there regardless of how well you execute the procedure. The workaround is to cut out the damaged section and splice in a new piece of belt, even if the original break was clean. You're buying insurance against a second failure two months later. The splice ratio matters more than you think. A 6:1 ratio means the taper length should be six times the belt width. For a 36-inch belt, that's 216 inches of taper. This isn't arbitrary. The longer the taper, the more evenly the tension distributes across the splice interface. A shorter ratio concentrates stress at the end of the splice, which is exactly where delamination starts. I've seen people cut a 4:1 ratio to save time and material on a wide belt. It looks fine for a few weeks. Then the tension cycle from the pulleys fatigues the adhesive bond at the taper termination point, and the splice peels open like a book. Don't do this. The manual's ratio is a minimum, not a target you can shorten. Vulcanization temperature windows are tighter than most splicers realize. The manual typically specifies a range—often between 275 and 300 degrees Fahrenheit for hot splices on fabric belts. The problem is that what the gauge reads and what the belt actually experiences are two different things. The temperature probes in vulcanizing presses measure the platen surface temperature, not the belt core temperature. On a thick belt, say 2 inches or more, the outer layers can be at spec while the center is still below the curing threshold. I've worked jobs where the press gauge showed 290°F the entire cycle, but when we pulled the belt and inspected the core of the splice afterward, the adhesive in the middle layers was tacky and under-cured. The fix was slowing down the heat-up phase, holding at a lower temperature for a longer period to let the heat penetrate evenly, then ramping to the full cure temperature. It adds time to the cycle but prevents the hidden failure that shows up six months into service when the under-cured adhesive slowly creeps under constant load.
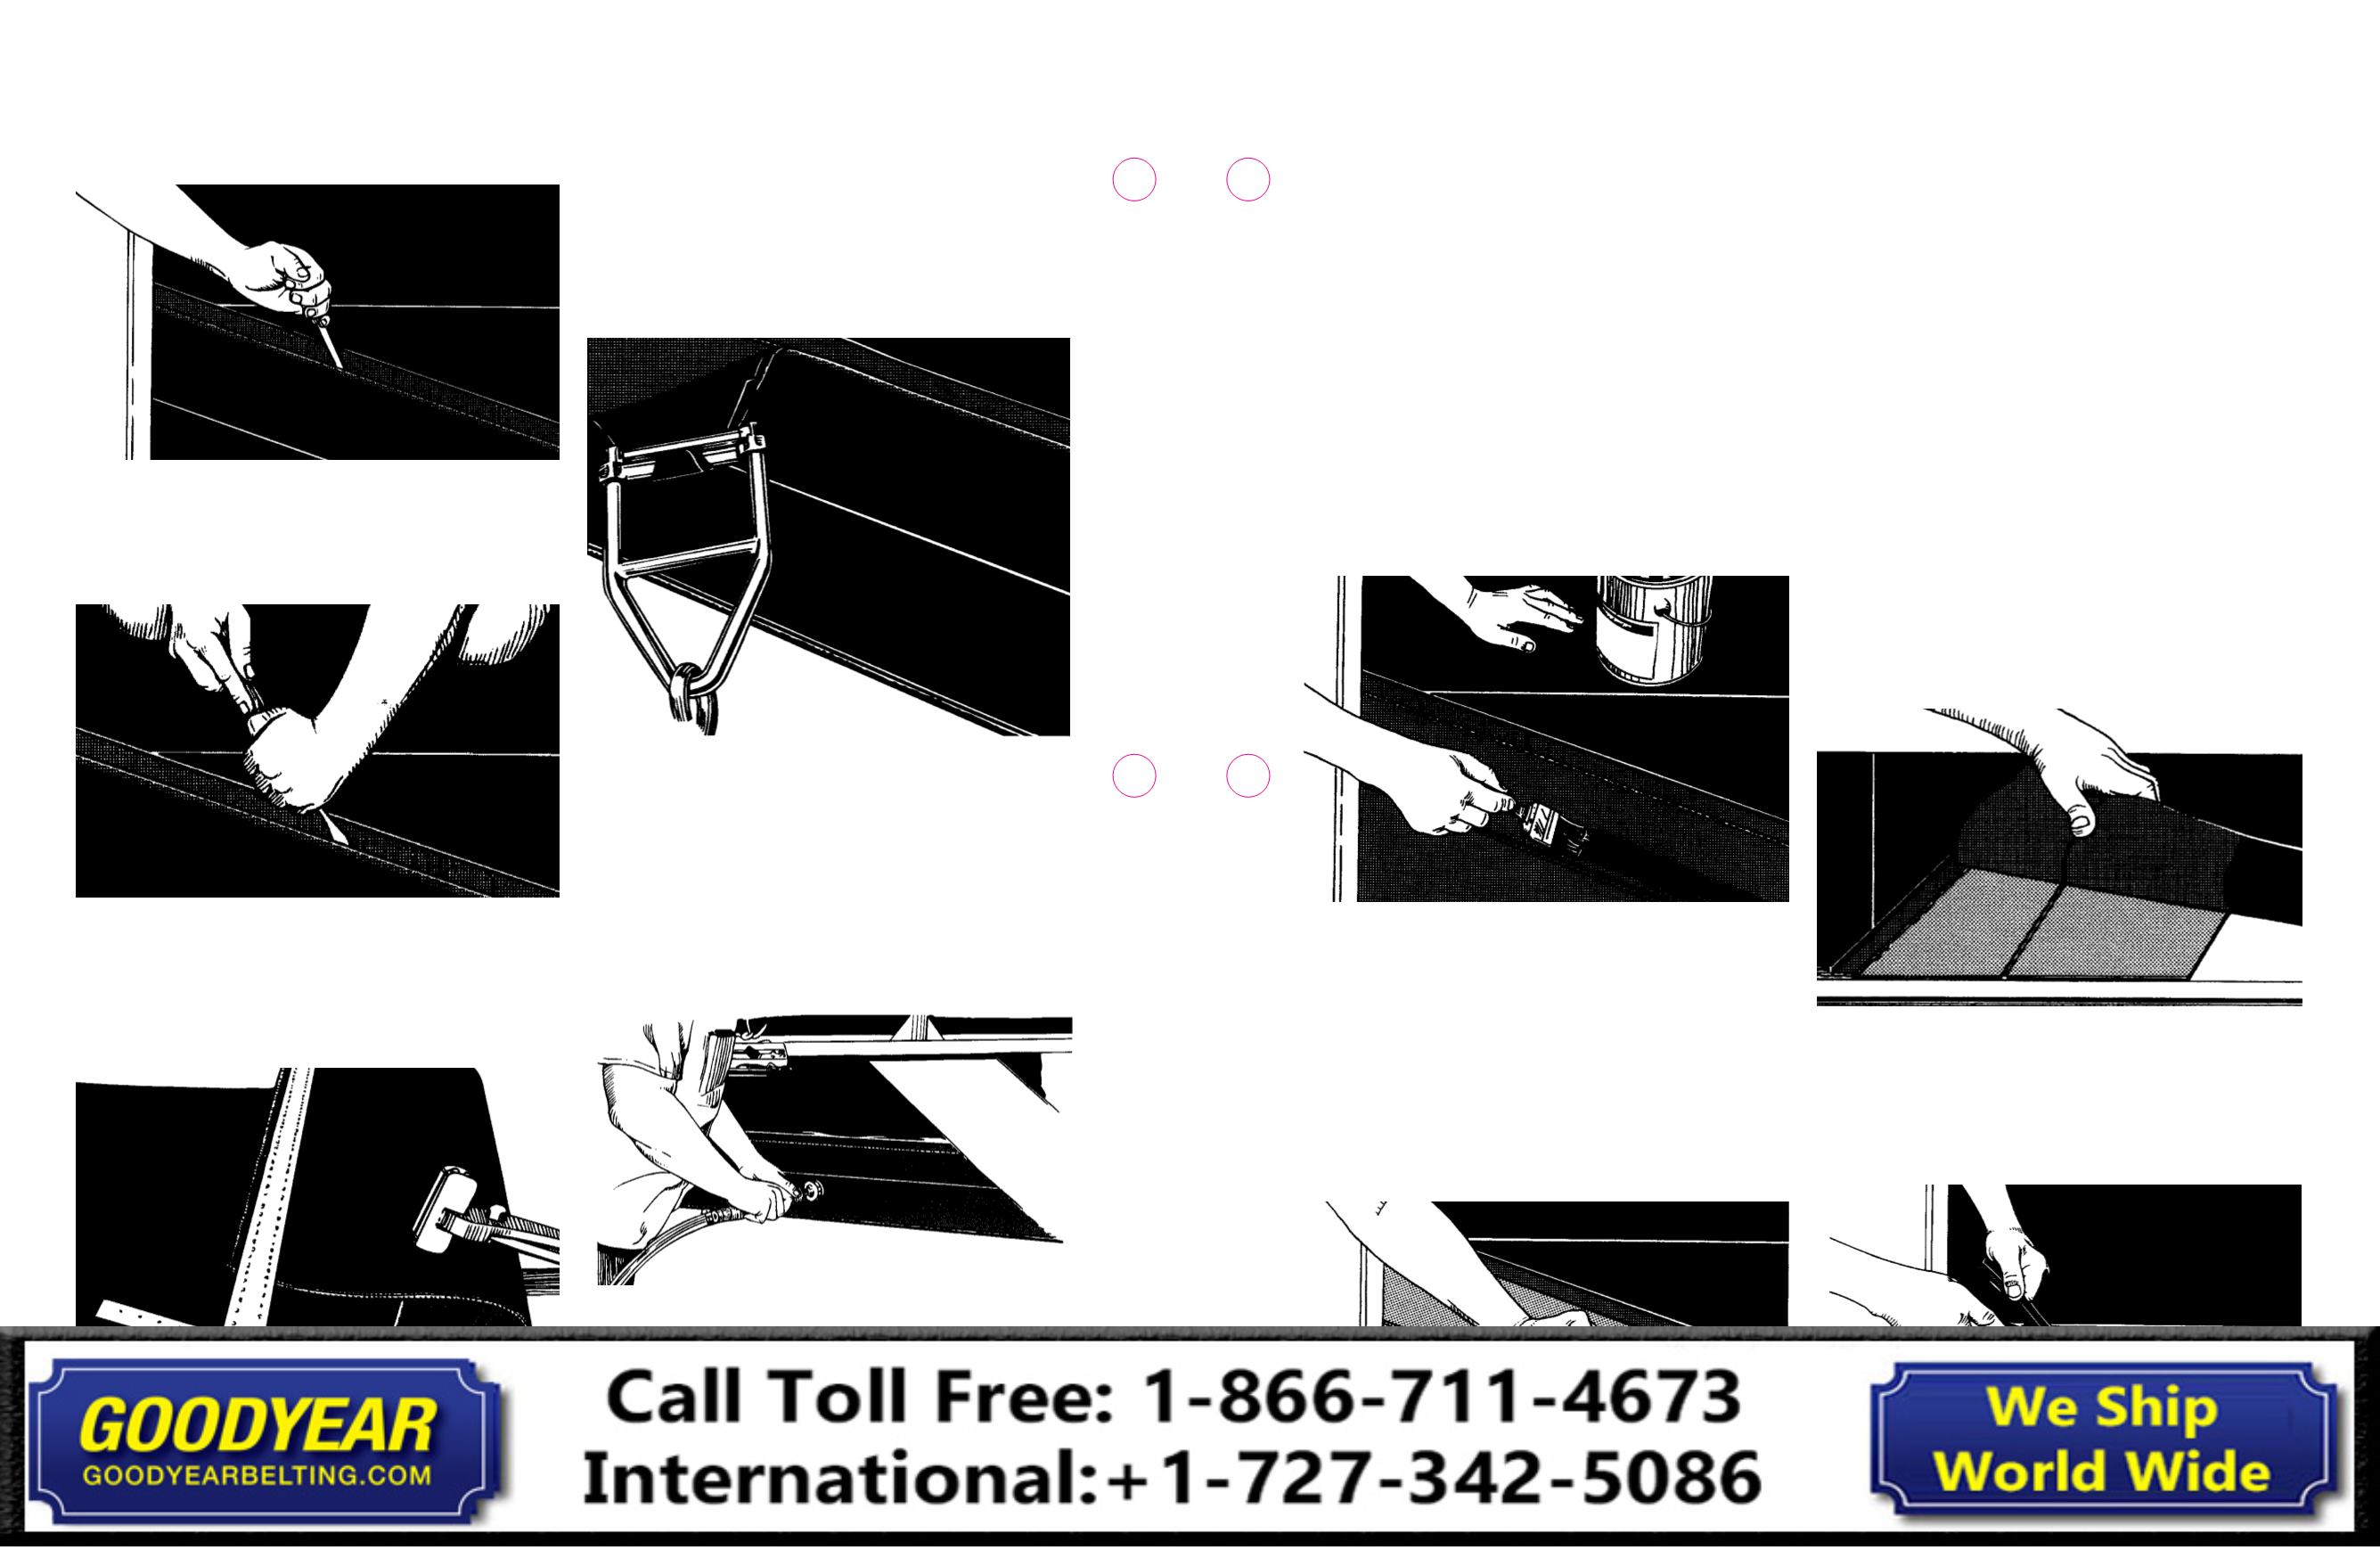
Cold cure splices are not a shortcut for production environments. The manual covers cold cure methods extensively because they have their place—emergency repairs, locations without power for vulcanizing equipment, or belts that can't tolerate the heat of a hot splice. But cold cure adhesives have a longer full cure time, typically 24 hours at recommended temperatures, and their final bond strength is generally lower than a properly executed hot splice. I had a situation where a cold cure splice was called for because the belt was near sensitive electrical components and heat wasn't feasible. We followed the manual precisely—surface prep, two thin adhesive coats with proper flash-off time between each, clamping at the specified pressure for the full cure duration. The splice held initially but began to degrade after about eight months of intermittent high-load cycling. The adhesive had absorbed some moisture during the cure window despite our precautions, and that moisture slowly weakened the bond. A hot splice in that scenario would have been more durable, but we didn't have the option. The lesson is that cold cure is acceptable when the manual says it's acceptable, but don't use it as a default just because it's faster to get the belt moving. If the application involves heavy loads, sharp materials, or continuous operation, plan for a hot splice. Ply alignment during the splice is where most rework happens. When you're laying up the alternating butt joints—the standard technique described in the manual—you need each ply to land exactly where it's supposed to. A ply that's offset by even a quarter inch creates a weak point because the joint lines don't distribute stress evenly across the splice width. I've seen splicers rush this step and end up with plies that are slightly staggered. The splice passes the initial inspection and holds for a while, but the misaligned joints become stress concentrators. Under repeated flexing around pulleys, those joints separate from each other rather than sharing the load. The workaround is to use registration marks on both sides of the belt before you start cutting the taper, and to verify alignment after each ply is laid down, not just at the end. It takes five extra minutes per ply and saves you from cutting out and redoing a splice you thought was done. The manual assumes you have the right tools. This sounds obvious but it's worth stating directly. Proper splice cuts require sharp belt knives—dull knives crush the fabric instead of cutting it cleanly, which compromises the adhesive bond. Ply removal tools need to be flat and thin enough to get between plies without tearing them. Pressure blankets or inflatable bladders for hot splice curing need to be in good condition—pinholes or uneven thickness create cold spots in the vulcanization. If your tools are worn or inadequate, the manual's instructions won't save you. Replace or repair your tools before you start the splice. I once worked with a crew that was using a kitchen knife to cut belt plies because their proper tool had broken. The splice lasted three weeks. Don't be that crew.
Get the Full Details
Documentation is not paperwork—it's evidence. The manual recommends recording the splice date, belt type, splice method, temperature profile, and the names of the splicers. Most people fill this out on a clip board and file it somewhere that gets lost. Keep these records on the belt itself or in a dedicated log that travels with the belt through its lifecycle. When a splice fails—and they do, eventually—you need to know exactly what was done, at what temperature, for how long, and by whom. That information determines whether the failure was a procedure error, a material defect, or an application issue that no splice method could prevent. Without the record, you're guessing, and guessing is expensive when the belt is down.
When the Manual Doesn't Cover Your Situation
Sometimes you'll encounter a belt construction or a field condition that the manual doesn't address directly. I've dealt with belts that had been previously spliced and repaired multiple times, where the overlap zones created uneven thickness that made a standard splice impossible. In those cases, the manual's standard procedure doesn't apply cleanly. The approach is to remove all previous splice material, restore the belt to a uniform cross-section, and then follow the manual for a new splice on clean belt. It uses more material and takes longer, but trying to splice over old splice remnants is a guaranteed failure. Another edge case is splicing belts in conditions below the manual's stated minimum temperature. Adhesive chemistry changes at low temperatures. The flash-off time between coats increases, and the cure reaction slows significantly. If you can't control the ambient temperature, extend all timing intervals and consider using an insulated blanket to maintain temperature during the cure. The manual gives baseline times for standard conditions—adjust them empirically if you're outside those conditions, and monitor the result closely. The Goodyear Conveyor Belt Splicing Manual is thorough but it's written for someone who has the fundamentals down. It won't teach you to read belt construction or understand why each step exists. Those come from doing the work and failing when you skip steps. The manual is your procedure. Your experience is what tells you when the procedure needs adaptation and when it needs to be followed exactly. Both matter.