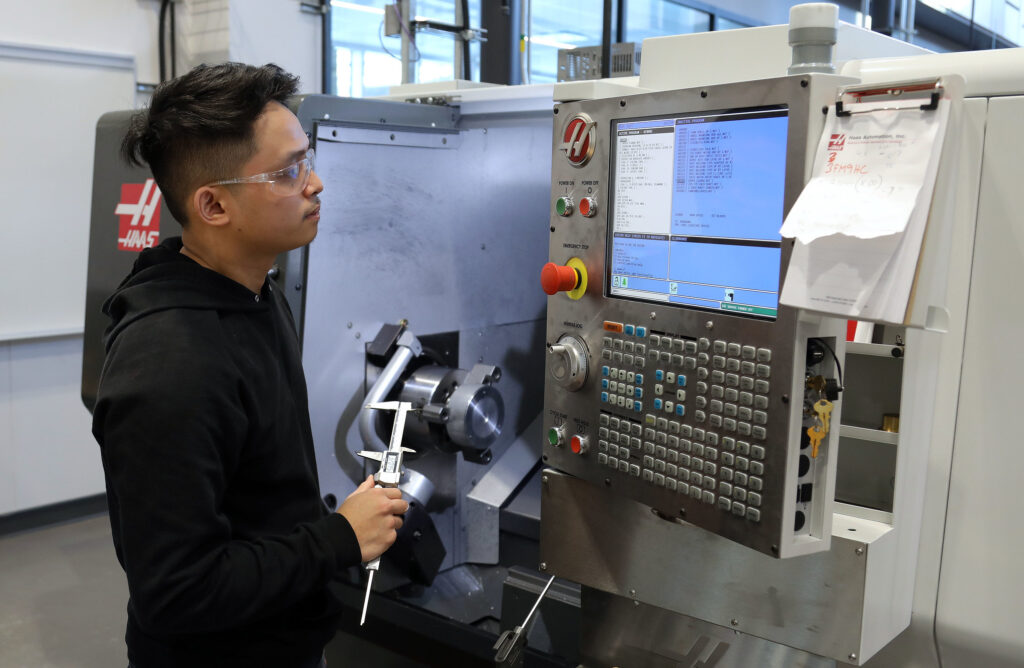
What actually happens when you try to learn Haas control programming
The Haas control isn't particularly hard to learn once you stop treating it like a mystery. Most training programs online sell you on the idea that you need to buy a $4,000 textbook and take a week-long class. You don't. You need to understand G-code, yes, but more importantly you need to understand how the Haas interface handles things differently than a Fanuc or Mazak machine. That single difference is where most people get stuck. I spent about three weeks teaching myself on a vintage TF-1 control before moving up to the UA and current VF-series controls. The first program I ever cut on a real machine was a simple bracket that took me four hours to run because I kept second-guessing the work coordinate system setup. That's normal. It happens to everyone.
What you actually need for Haas Cnc Programming Training
You don't need expensive training to learn the basics. What you need is: a Haas manual (the free PDFs on their website are thorough), a simulator if possible, and some actual machine time. The Haas simulator at haascnc.com/services/support/ca-m-x-simulator.html is completely free and runs on your computer. It won't replace real machining time but it will save you from crashing machines while you're learning G43, tool length offsets, and the difference between absolute and incremental programming on a Haas specifically. The G-code itself is 90% ISO standard. The other 10% is Haas-specific macro B programming, fixed cycles that behave slightly differently, and the way the control handles parameter settings. Start with the manual. Read it cover to cover before you ever touch a machine. I know that sounds extreme but it cuts weeks off your learning curve because the manual answers questions before you even know to ask them.
The practical path most people should follow
Step one: learn the basics of milling G-code on paper. G0, G1, G2, G3, G40, G41, G42, G43, G49, G54 through G59, G80 through G89, M03, M05, M08, M09, M30. That's basically the entire vocabulary you need for 80% of Haas programming work. Write out simple programs by hand. Put them in a notebook. Calculate your cuts on graph paper if that helps you think clearly. Step two: load the Haas simulator and type those same programs in. Watch the toolpath. Verify the numbers match what you calculated. This is where you'll find your mistakes before they become expensive mistakes on real metal. Step three: get on a real machine with someone who knows what they're doing. Even two days of supervised machine time is worth more than three months of solo simulator work. The feel of dry runs, the sound a tool makes when it's cutting correctly versus when it's struggling, the way chip load changes with different materials — none of that translates through a screen.
Get the Full Details

A problem I ran into that wasn't in any manual
On a VF-2 roughly five years ago, I was running a program with multiple G54 work offsets. The part had two setups and I had set G54 for the first and G55 for the second. Everything looked correct in the simulator. On the machine, the second setup was running about 0.004 inches off in the Y-axis direction. I checked the offset table three times. I checked the program three more times. I even re-probed the workpiece from scratch. The issue turned out to be that the machine had been used the day before by someone running a Fanuc-style program that included a G92 command. G92 doesn't just set a coordinate temporarily on a Fanuc. On a Haas, if you use G92, it modifies the actual work offset register, not just the active one you're currently using. The previous operator's G92 had shifted G54's Y value by 0.004 and nobody noticed because the first setup still looked fine. The workaround is simple: never use G92 on a Haas. Use G10 L20 to set work coordinates instead. It's explicit, it's clean, and it doesn't have hidden side effects on other offset tables. I now include a G10 L20 block at the top of every program I write as a habit. It costs nothing and it prevents exactly this kind of problem.
Common pitfalls that cost people time and material
Tool length compensation direction. On a vertical Haas, G43 moves the Z axis positive by the tool length offset value. This is standard but beginners sometimes get confused when switching between top-of-part and bottom-of-stock referencing. Make sure you know which your program assumes and stick with it consistently across all tools in a given setup. The rapid override switch. New programmers tend to leave the rapid override at 100% until they're confident. Good practice. Then they forget to dial it back and make a fast approach move that comes in too hot. There's a soft limit called G00 override that most people don't notice until they've already made contact with the part. Set it to 25% for your first few tool approaches and work your way up as you verify the program is correct. Circular interpolation radius vs. angle. When programming G2/G3 arcs, you can specify either I/J/K offsets or R values. I/J/K is more precise for full circles and certain edge cases where the radius would be ambiguous. R is simpler for basic arcs but can produce unexpected results if your arc crosses the quadrant boundary in certain configurations. I use I/J/K whenever possible now, even for simple arcs, because it removes ambiguity from the math.
What the training landscape actually looks like
There are paid courses, community college programs, and a lot of free content. The paid ones range from legitimate to borderline scam depending on who's teaching. If someone is selling a course that promises you'll be machining production parts in three days, move on. Realistic timeline is two to four weeks of dedicated effort to reach competent beginner level, and several months before you're truly confident running complex parts alone. Haastraining materials are good. Their documentation is better than most machine tool manufacturers. The operation manual for your specific model is the single best resource available. For the UA control the manual is over 600 pages and covers everything from basic manual data entry to macro B programming, probe cycles, and error code diagnostics. Read it before you pay for anything else. Gantry alignment and backlash compensation. Most beginners skip this entirely. It's not glamorous but machine backlash affects positional accuracy directly. Running a ballbar test and loading the backlash parameters into the control can improve repeatability from around +/-0.001 to +/-0.0005 on a well-maintained VF-series machine. If you're holding tolerances tighter than 0.002 you need to understand this. It's not programming but it's part of what makes your programs actually produce good parts.
When simulation won't help you
The simulator catches syntax errors and shows you the toolpath. It cannot tell you if your feeds and speeds are reasonable for the material you're cutting. It can't warn you that your tool reach will hit the fixture. It can't verify that your clamping won't interfere with the tool path. All of that requires either real machine time or an advanced CAM package with collision detection, which is a separate skill set entirely. If your shop already uses CAM software like Mastercam or Fusion 360, learning to post-process Haas-specific output is probably more valuable long-term than hand-writing G-code. The industry is moving that direction. But understanding the raw G-code underneath makes you better at debugging post-processed programs when they go wrong, which they inevitably will.
Bottom line
Start with the free manual. Run the free simulator. Get on a machine as fast as possible. Keep a notebook of what you learn from each program, especially the mistakes. The Haas control is straightforward once you understand its specific quirks, and the biggest quirk is simply that it's not exactly Fanuc despite looking similar on the surface. Program, run, verify, repeat. That's the whole thing really.