
Getting Started with the Haas HS-1 Operator's Manual
Most people looking at the Haas HS-1 Manual are either new operators, shop managers trying to onboard someone, or a machinist who's tired of guessing which button does what at 11pm when the machine won't run. The manual for the HS-1 is not a dense 600-page engineering document like some other CNC manufacturers produce. It's functional, about 120 to 150 pages depending on the revision, and it covers everything from powering the machine up to troubleshooting alarm codes. Here's what you need to know about it, how to find it, and the parts that actually matter when you're standing at the control panel trying to figure out why your part keeps running oversized.
Haas HS-1 Manual download and access
Haas publishes their manuals directly on their website. Go to haascnc.com, navigate to the support or documentation section, and search for "HS-1 manual" or "HS-1 operator's manual." You'll get a PDF for free. No registration wall, no email gate. This is one of the reasons Haas has such a large installed base in training programs and small job shops — the documentation is openly available. The manuals are broken into at least two documents: the operator's manual and the programming manual. Get both. The operator's manual tells you how to run the machine. The programming manual tells you how to write G-code for it. They are separate because people run these machines without ever writing their own programs, and vice versa. If you can't find the current revision on the Haas site, your factory outlet dealer can pull it. Some older editions had minor differences in the touch-off procedure and the tool length measurement setup, but nothing that breaks the core process.
What's inside the manual and why the order matters
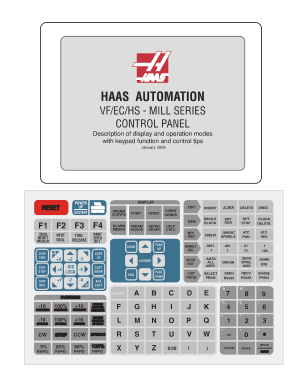
The operator's manual starts with safety. This is not filler. The HS-1 has a 40-taper spindle, a 25 HP continuous motor, and enough force to turn a bad setup into an expensive conversation with your insurance adjuster. The safety section covers chip guard interlocks, emergency stop wiring, and why you should never reach into the enclosure while the spindle is still rotating after a program ends. Next comes the control panel walkthrough. The HS-1 uses the Haas Nano control with a 15-inch color display. The buttons are laid out logically but there are enough mode selectors that a new operator will cycle through them by accident at least once during their first week. The manual maps each button and switch with a diagram and description. Read it. Don't skip it. The axis movement section explains jog speeds, incremental stepping, and absolute positioning. A counter-intuitive detail most people miss: the HS-1 has two jog speed ranges, and the range you're in determines whether the incremental step size is measured in thousandths or in ten-thousandths of an inch. If you're trying to dial in a .0005" offset and it feels like the axis is jumping in huge increments, you're probably in the coarse jog range. Switch to fine. The manual notes this but it's easy to overlook when you're focused on getting the part loaded.
Get the Full Details

The tool management section covers the 12-station cartridge magazine. The HS-1 uses a double-arc tool holder system. Tool holders are the BT40-style shape but with Haas-specific tool pull stud dimensions. Make sure you're using the correct tool holder type. I learned this the hard way when a vendor quoted me tool holders for a 45-taper spindle because they assumed HS-1 meant 45-taper. The tool holders didn't seat, the pull force was wrong, and the spindle taper was at risk. You can identify the right tool holders by checking the part number on the tool holder shank — anything starting with Haas's standard BT40-HT designation is correct. The manual lists compatible tool holder specs on page 67 in the 2018 revision.
Tool setting and work coordinate setup
This is where most people burn time. The HS-1 has built-in tool probing with the optional touch probe, but if you're running without it you're using the tool setter on the machine table or manual measurement. The manual walks through both methods. The manual method is slower but cheaper, and most first-time users end up here. When you set tool length offsets using a tool setter, the procedure is straightforward: park the tool over the setter, lower it until it triggers, record the Z position, and assign the offset value. The control does the math. What the manual doesn't emphasize enough is that the tool setter itself needs to be checked periodically. I had a situation last year where a parts supplier was sending us reject parts with inconsistent Z heights across a batch of 40 pieces. The X and Y were fine. The Z was drifting by .003" over the run. We tracked it down to the tool setter having a chip packed under its sensor plate. The setter was reading slightly short every time, and the control was compensating by adding length that wasn't really there. Cleaning the plate and re-running the tool setter calibration fixed it. Check your tool setter before you blame the program. For work coordinates, the HS-1 uses the standard G54 through G59 system. The manual shows you how to set each one using the edge finder or a probe. The practical tip that saves hours: set all six work offsets at the start of a job, not just the one you're using. If you're running multiple setups or a part that flips, you'll need the others and setting them all at once when everything is cold and true is much faster than scrambling mid-shift when something trips and you lose your offset.
Running a program from start to finish
The manual covers the standard workflow: load the program, set up the part, dry run or first-run techniques, then run production. The dry run section deserves attention. The HS-1 has a single block skip, optional stop, and feed hold. Use all three on the first run of any new program. Set the override to 25% or lower for the first pass. Watch the chip color and sound. Then walk away and come back. Most people skip the walk-away step and miss things that only become obvious after a few cycles. One thing the manual mentions but doesn't really drill home: the HS-1's rapid rate is 400 ipm on all three axes. For a machine this size, that's adequate but not fast. If you're programming aggressive clearances or high-speed traverse moves, the machine won't keep up with what you might expect from a larger Haas model. The control will scale back automatically, but the cycle time impact is real. Keep your clearance heights reasonable and your tool paths tight. The manual has a section on program optimization that gives concrete examples of how moving from absolute to incremental coordinates in certain contexts can save a few seconds per hole, which adds up on high-count parts.
Common alarms and what the Haas HS-1 Manual says to do
The alarm section runs from alarm 001 through about alarm 400 depending on revision. The most useful alarms to memorize are the ones that stop production unexpectedly. Alarm 021 is a tool magazine position mismatch — the control thinks the tool is in one pocket and the encoder says it's in another. The manual says to press reset, manually index the magazine to the correct position, and reload the tool. In practice, this alarm happens most often after a power cycle if the magazine didn't complete its homing sequence. Make sure the machine finishes its full startup cycle before loading tools. Alarm 053 is an overload on one of the axes. On the HS-1 this is usually the Z axis and it means the cutting force exceeded the drive limit. The manual recommends reducing feed rate, taking lighter cuts, or checking for binding. The real-world fix is often simpler: check that the way covers aren't packed with chips and that the Z-axis ball screw isn't starved for lubrication. The auto-lube system on the HS-1 is small and clogs more often than people realize. Check the lube pump reservoir every shift and clean the distributor blocks monthly. Alarm 144 is a spindle overload. This one is serious. The manual tells you to check the cutting conditions and reduce load. If it's happening at idle or with no cut engaged, it could be a spindle bearing issue or a drive problem. Don't ignore it and don't just keep resetting it. Spindle repairs on an HS-1 are not cheap. The manual includes a troubleshooting flowchart on page 198 in the latest revision that helps you distinguish between cutting overload and mechanical failure. Follow it.
Maintenance schedule from the manual
The maintenance section is the most important part of the manual for long-term reliability. It's also the part people skip. The HS-1 has a daily checklist, a weekly checklist, and a monthly checklist. The daily items take about five minutes: check coolant level, check way lube level, clean the chip conveyor, inspect the tool holders for wear, and wipe down the way covers. The weekly items are more involved: clean the air filter on the spindle cooler, check the hydraulic pressure if equipped with an ATC (the HS-1 standard magazine is pneumatic), inspect the belt tension on the spindle drive, and verify the axis backlash compensation values haven't drifted. The manual gives you the specs for each check. Monthly maintenance includes cleaning the chip conveyor chain and sprockets, checking the accuracy of the axis positioning with a laser or dial indicator, and inspecting the spindle runout. If you run the machine hard — eight hours a day or more — do the monthly checks every two weeks. The manual's intervals assume light to moderate use.
Limitations the manual doesn't emphasize
Every machine has limits and the HS-1 is no exception. The 40-taper spindle handles light to medium cutting well. It will struggle with aggressive material removal in steel or titanium. If you're planning to run heavy plunges or high material removal rates in tough alloys, the HS-1 will hit the power and rigidity wall. The manual states the motor specifications clearly but doesn't draw attention to the fact that the spindle bearing preload and the overall column rigidity place this machine in the entry-level to mid-range category. For aluminum and soft materials, it's fine. For production milling of 4140 or Inconel, look at the HA-4 or the VF series with the higher power options. Another limitation: the 12-tool magazine is small. If your part requires more than 12 tools, you're either reloading manually between runs or you need to restructure the program. The manual shows you how to manually reload tools, but this adds downtime. For high-mix shops this is a real constraint. The controller, while functional, is not as fast as the newer Haas controllers. Program download times are slower, and complex macro programming can feel sluggish. The manual covers the capabilities but doesn't compare them to newer hardware. If you're writing complex subroutines or using advanced macro B features, the response time is noticeable. Simple G-code programs run fine.
Where to go when the manual isn't enough
The Haas manual is solid for standard operations. When you hit edge cases — and you will — the next resources are the Haas technical support line, the factory outlet where you bought the machine, and the online forum community. The Haas Forums have a dedicated HS-1 section where machinists share setups, alarm histories, and modifications. Not everything is there, but the practical knowledge that never makes it into the printed manual is usually discussed there. Another resource is the programming manual. It covers G-code, macro B, canned cycles, and the full instruction set. If you're writing your own programs or modifying existing ones, this document is as important as the operator's manual. The two complement each other. The operator's manual keeps the machine running. The programming manual keeps the programs correct. The Haas HS-1 Manual is a decent reference, but it works best when you treat it as a living document you return to, not something you read once and file away. The real value is in the sections you revisit when something goes wrong at 10pm and you need to know whether the alarm code is something you can fix or something that needs a call to the service line.


